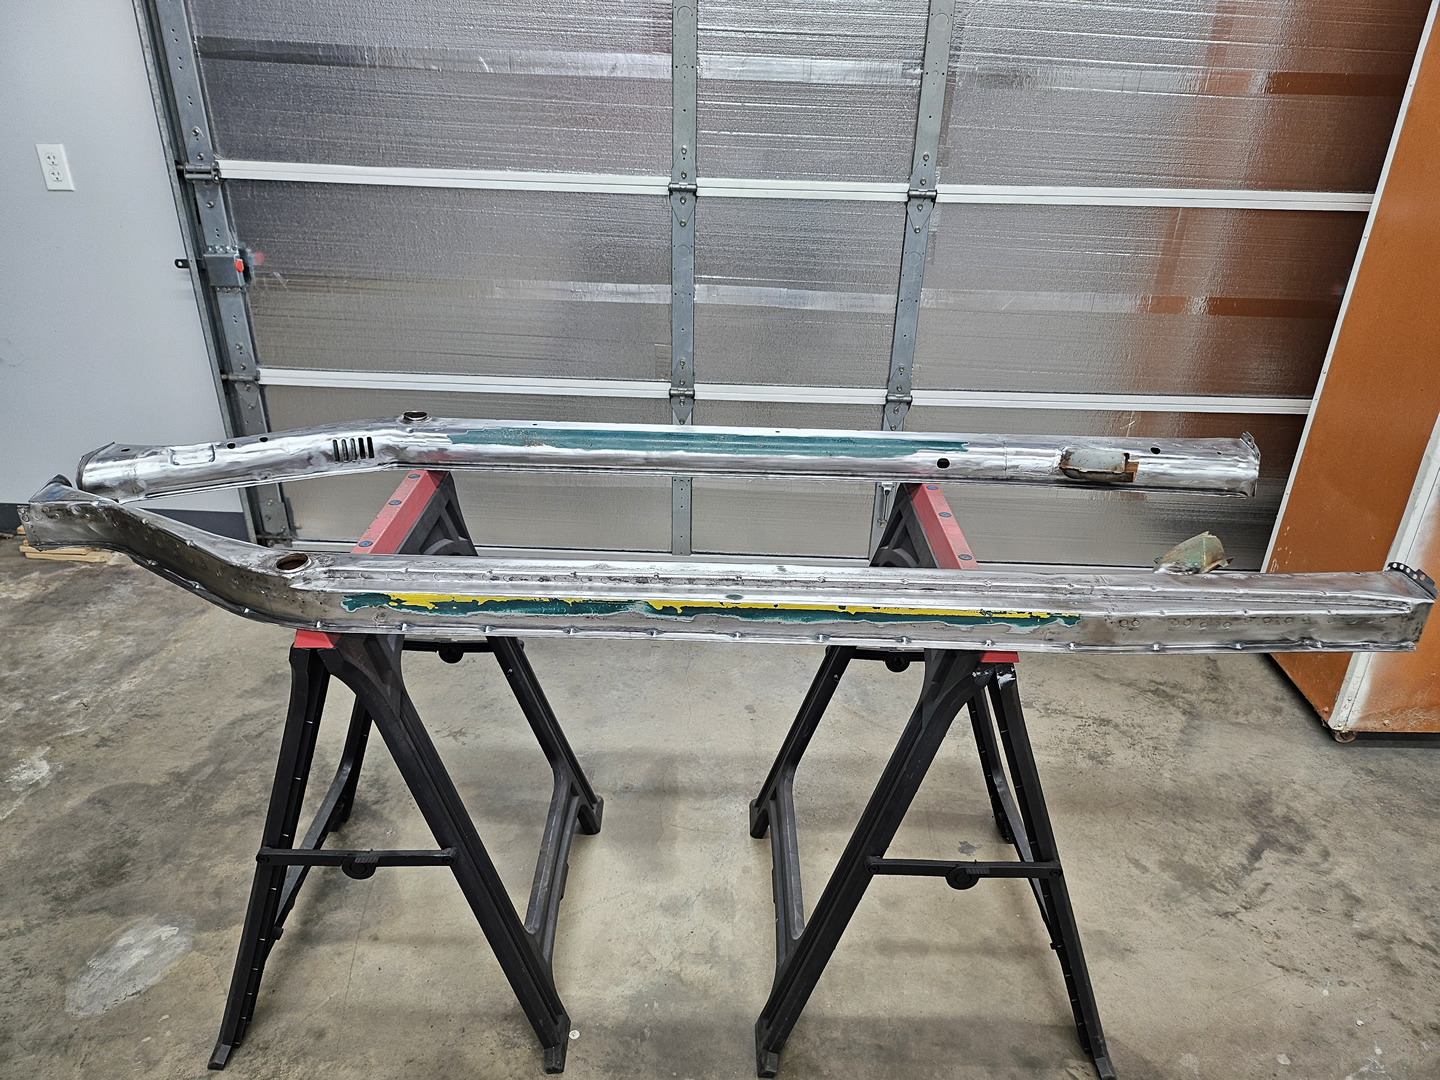
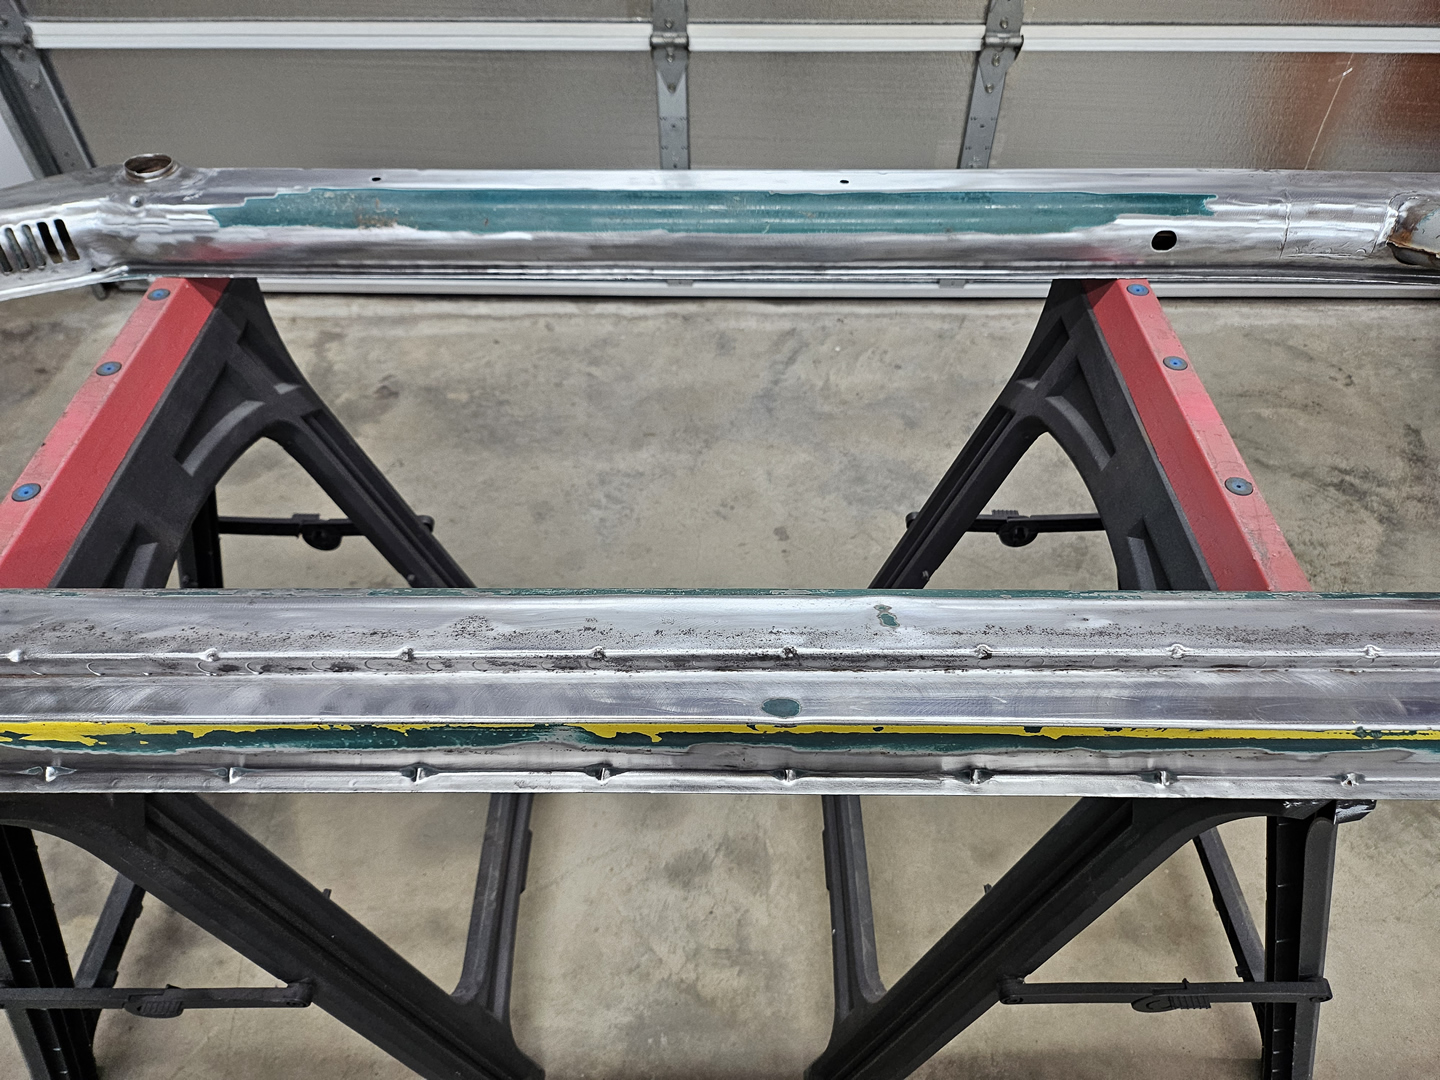
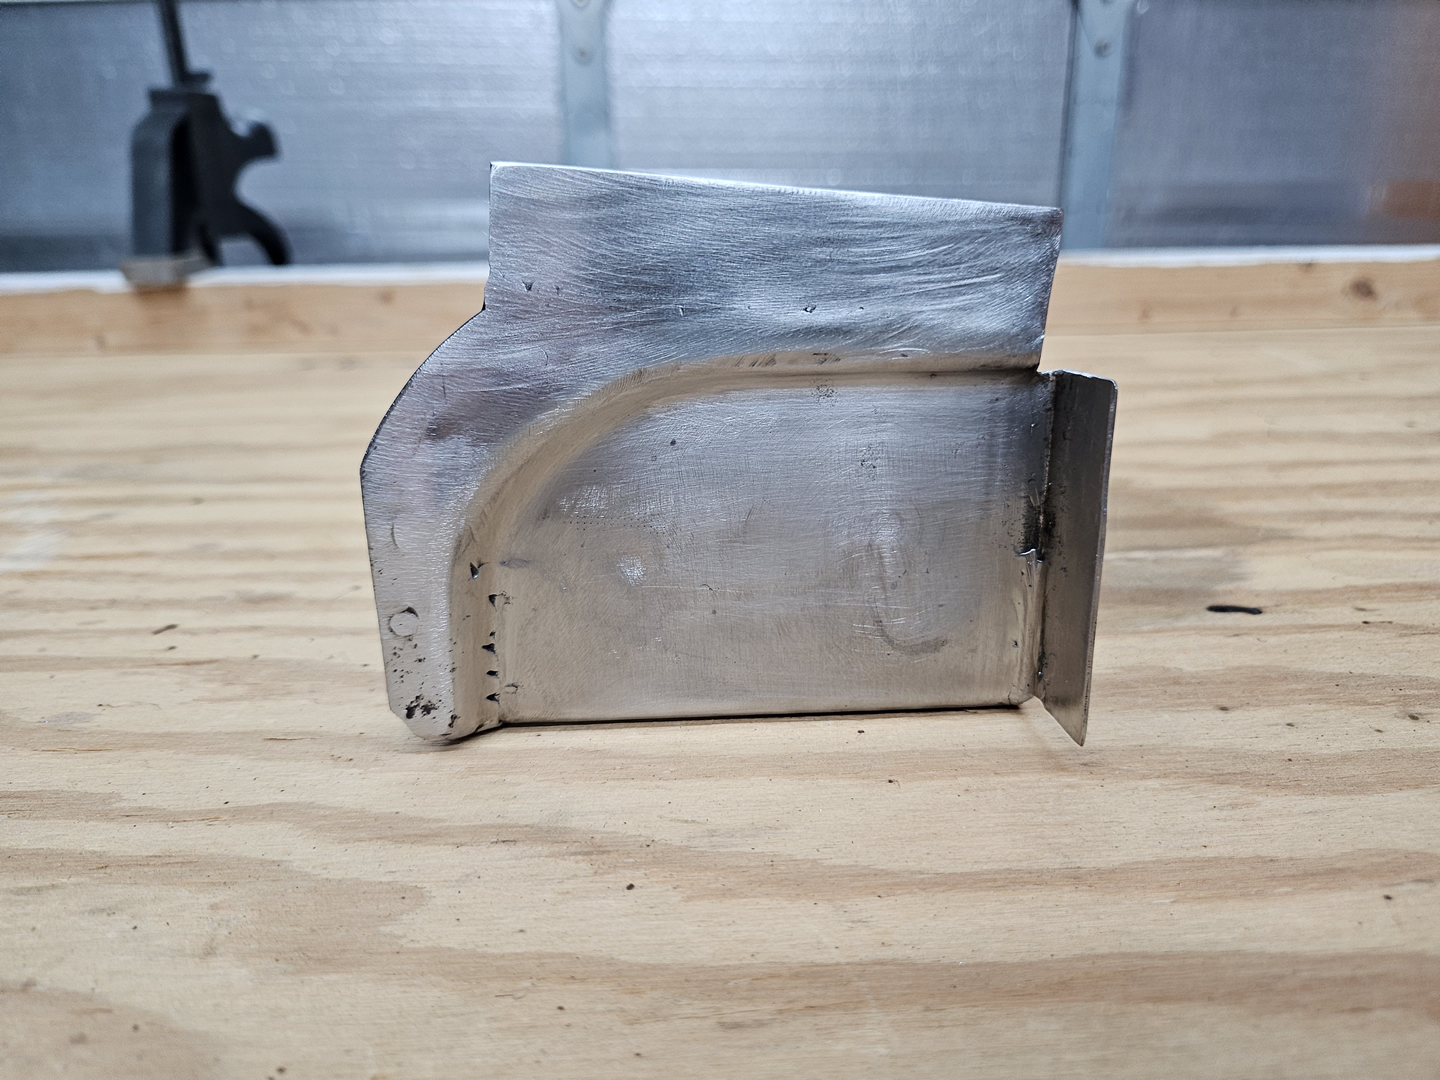
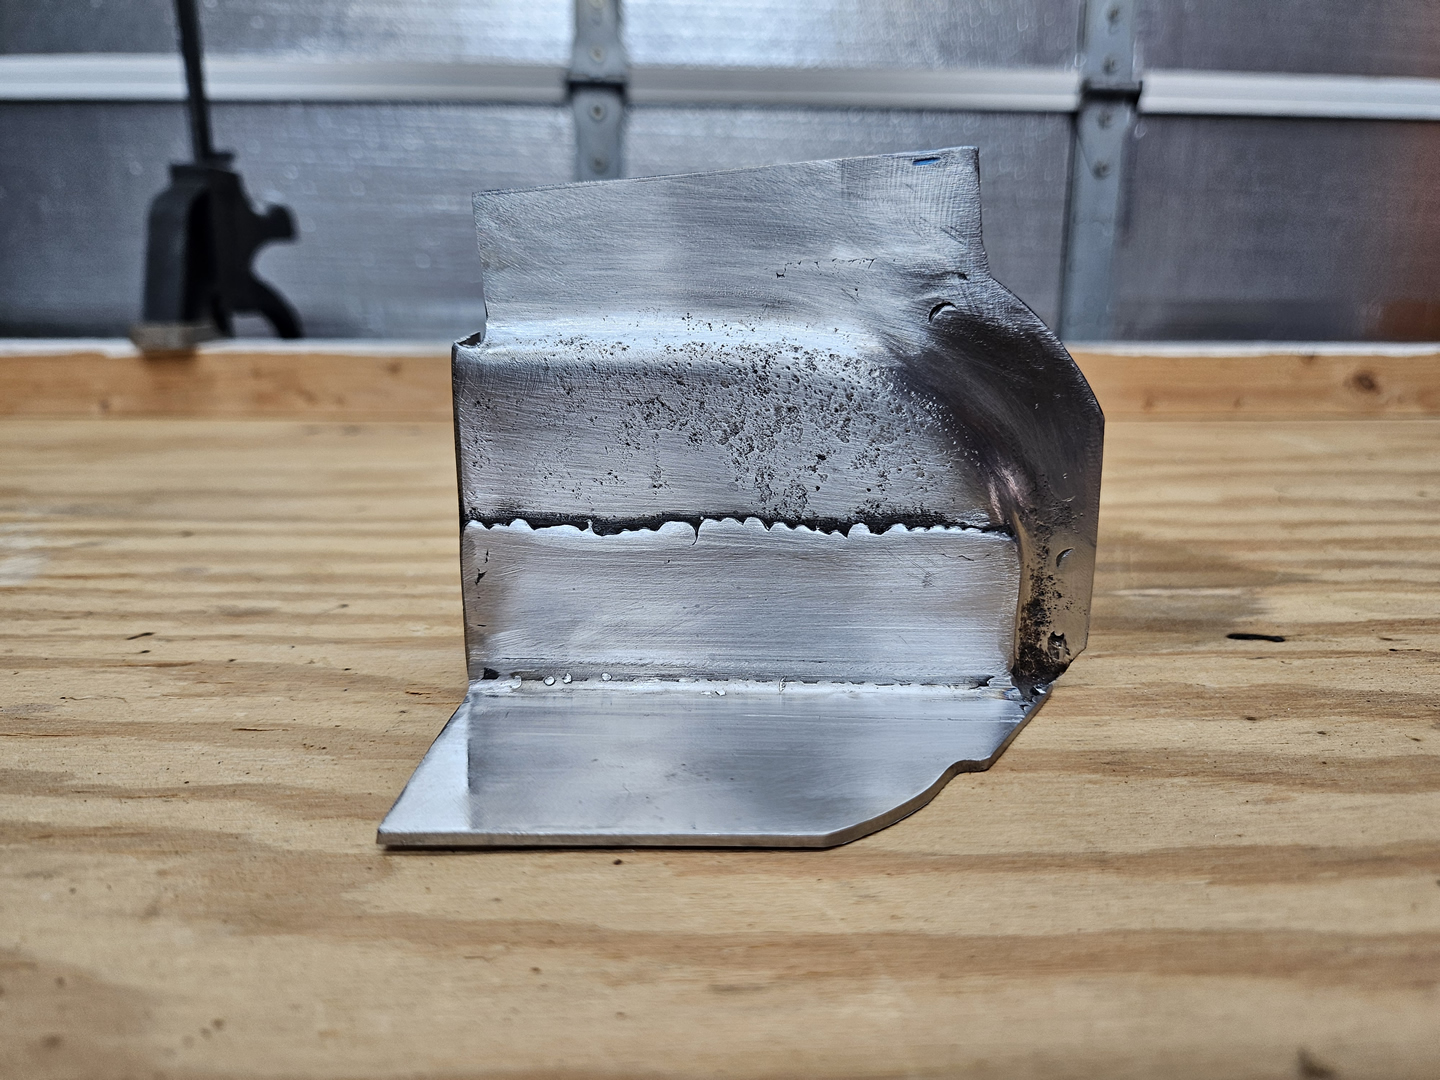
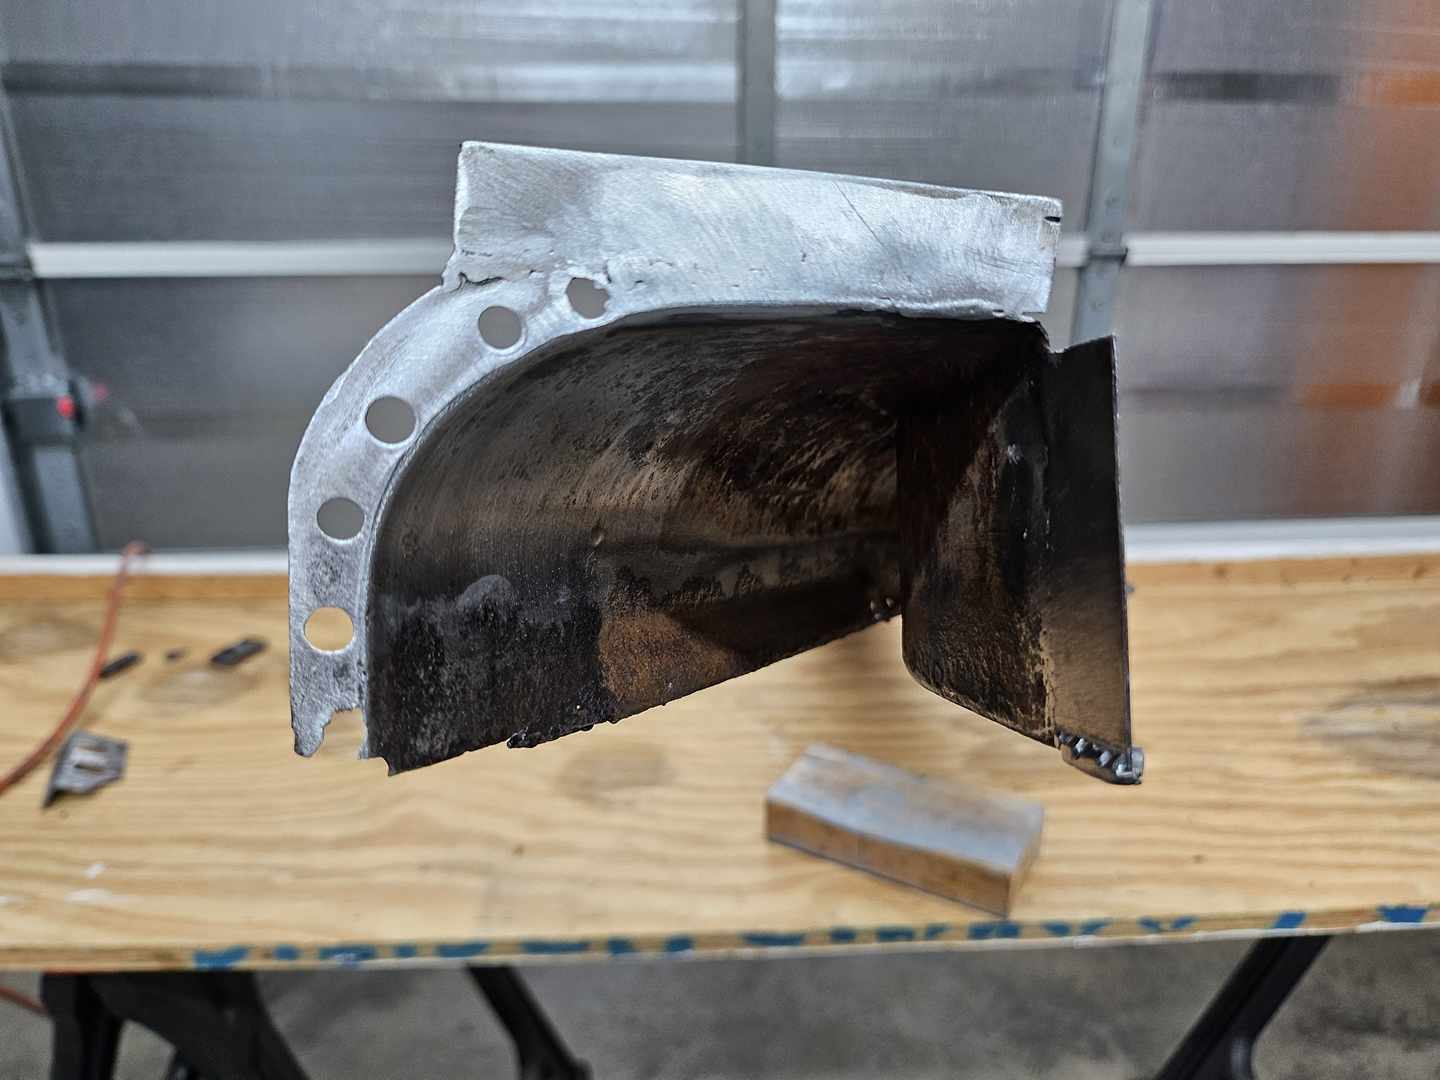
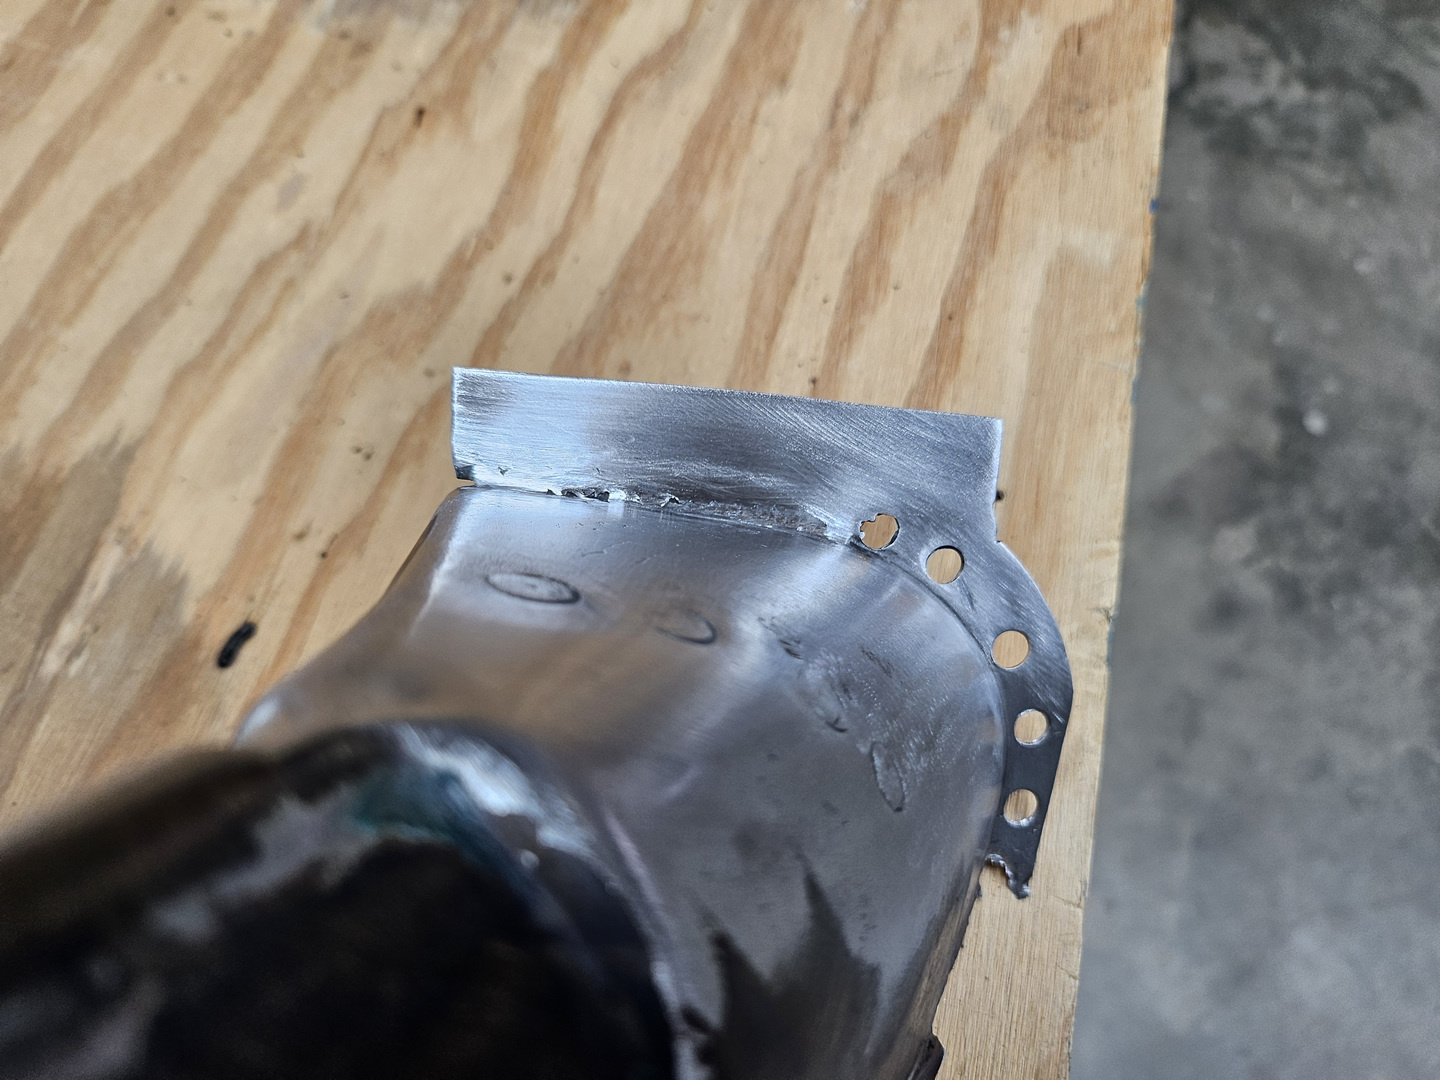
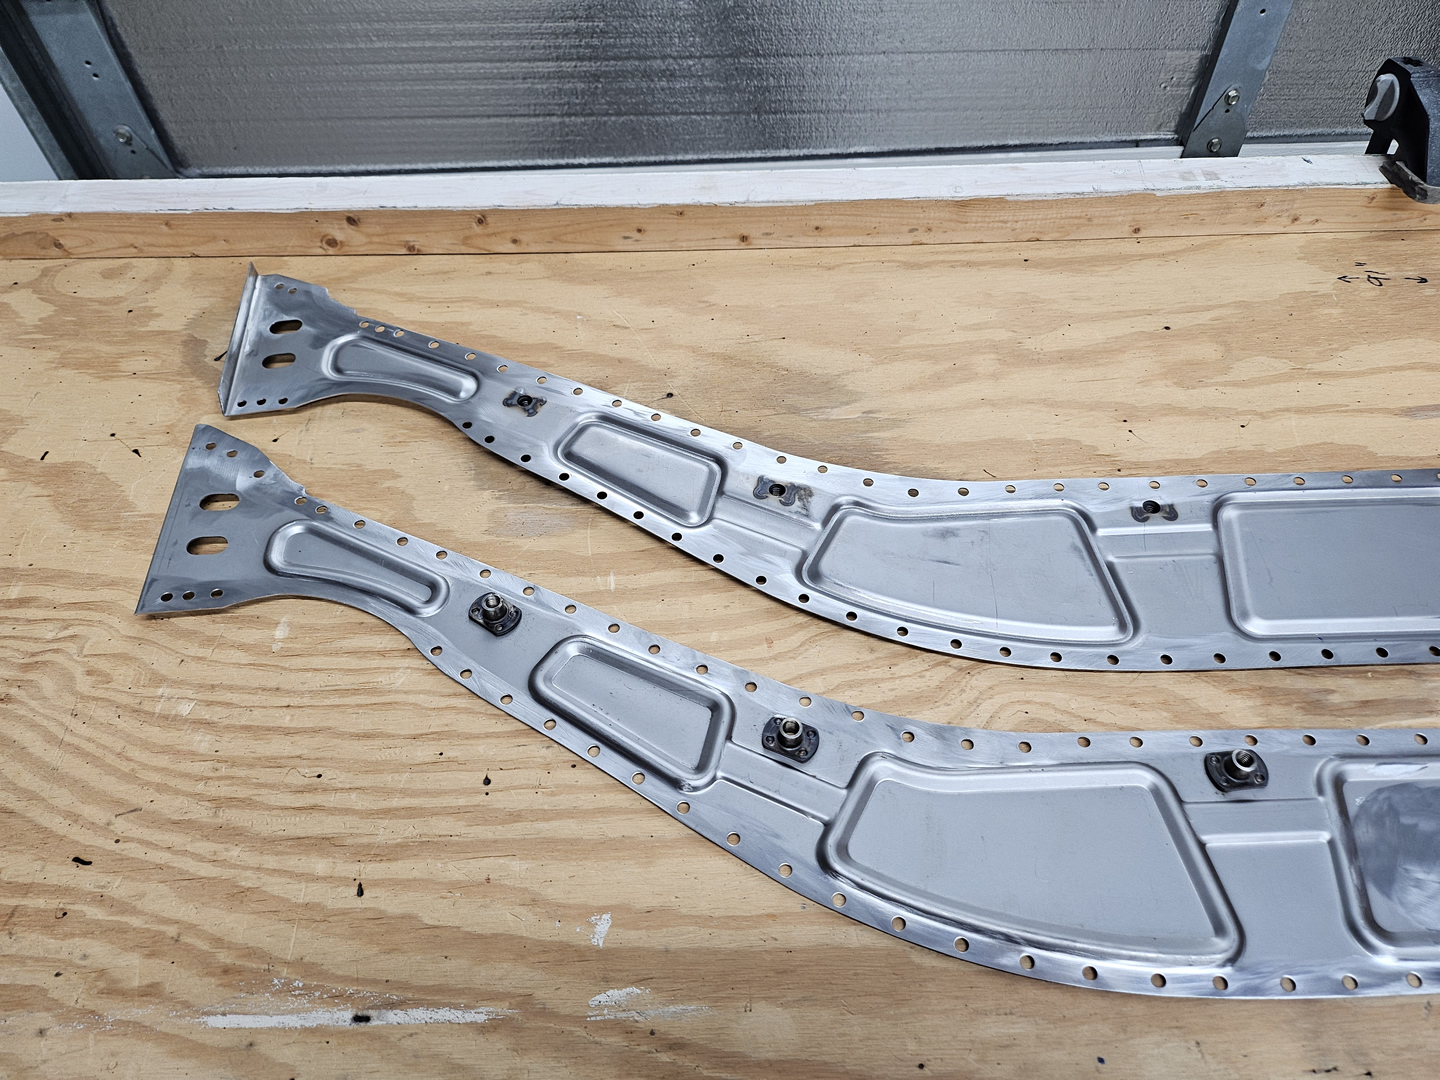
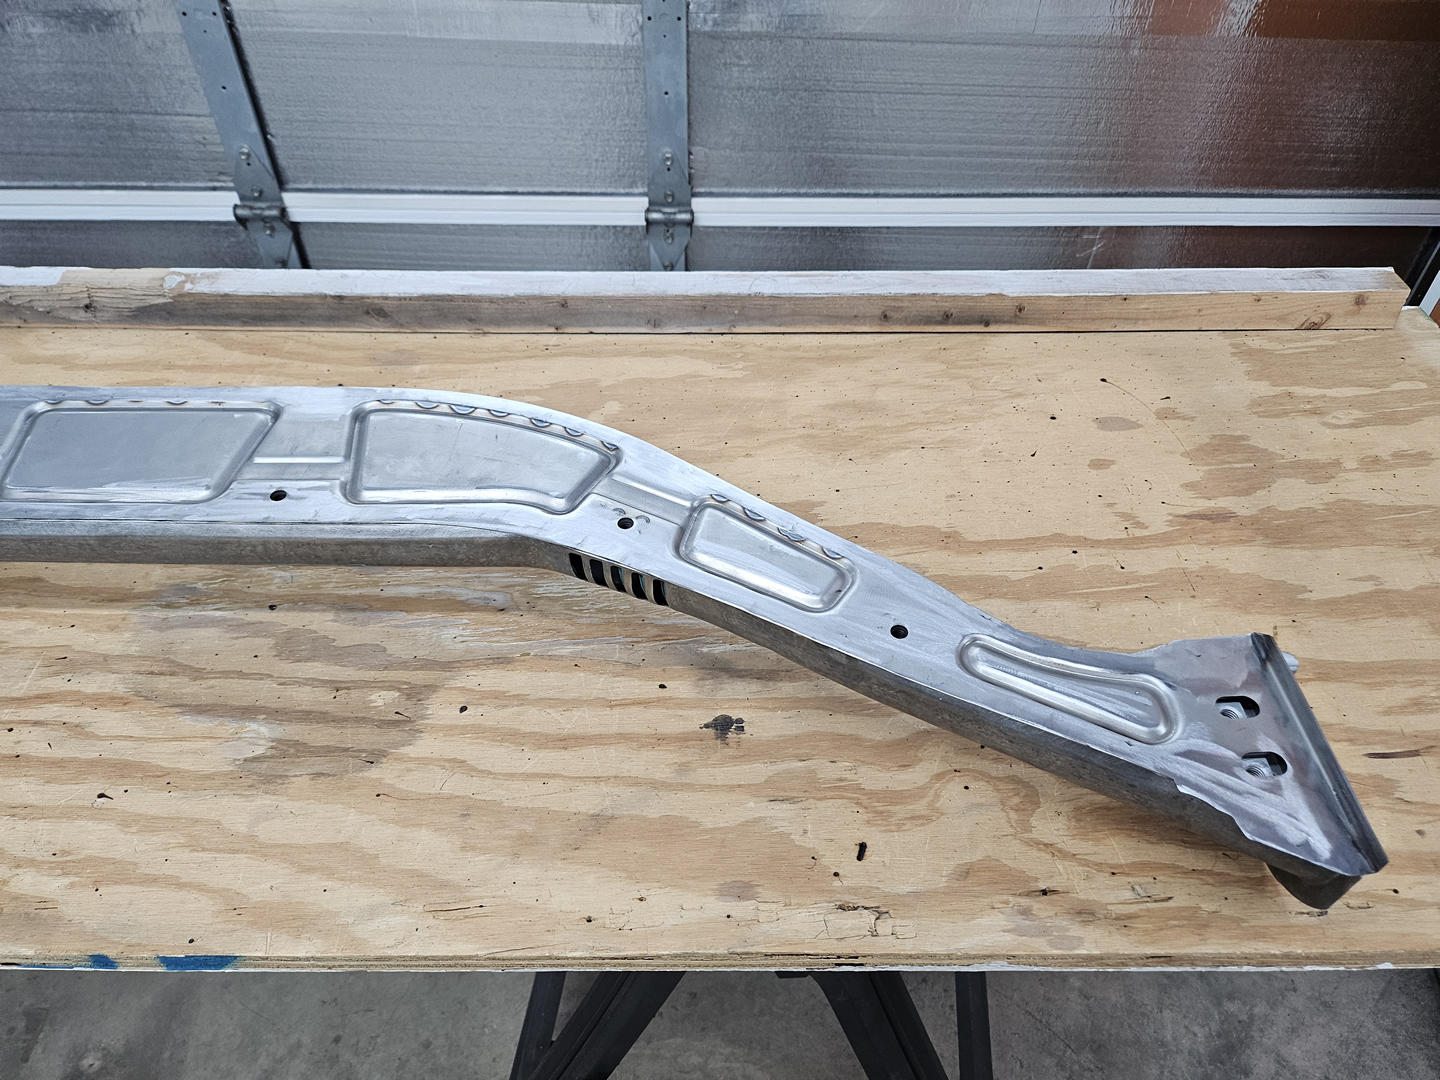
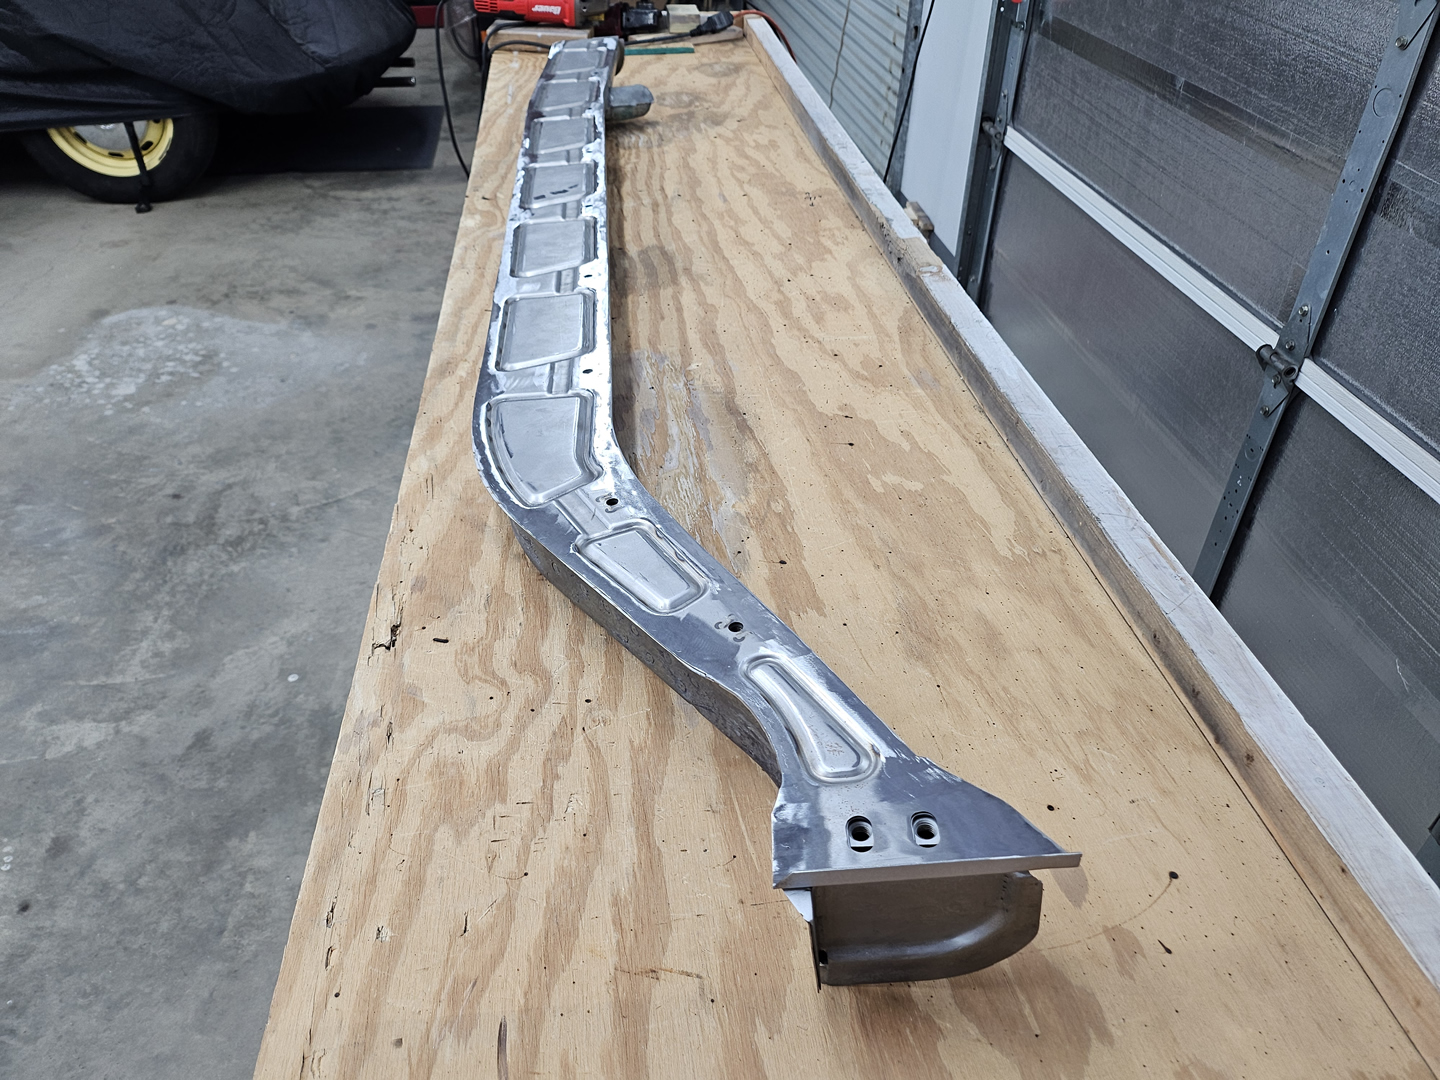
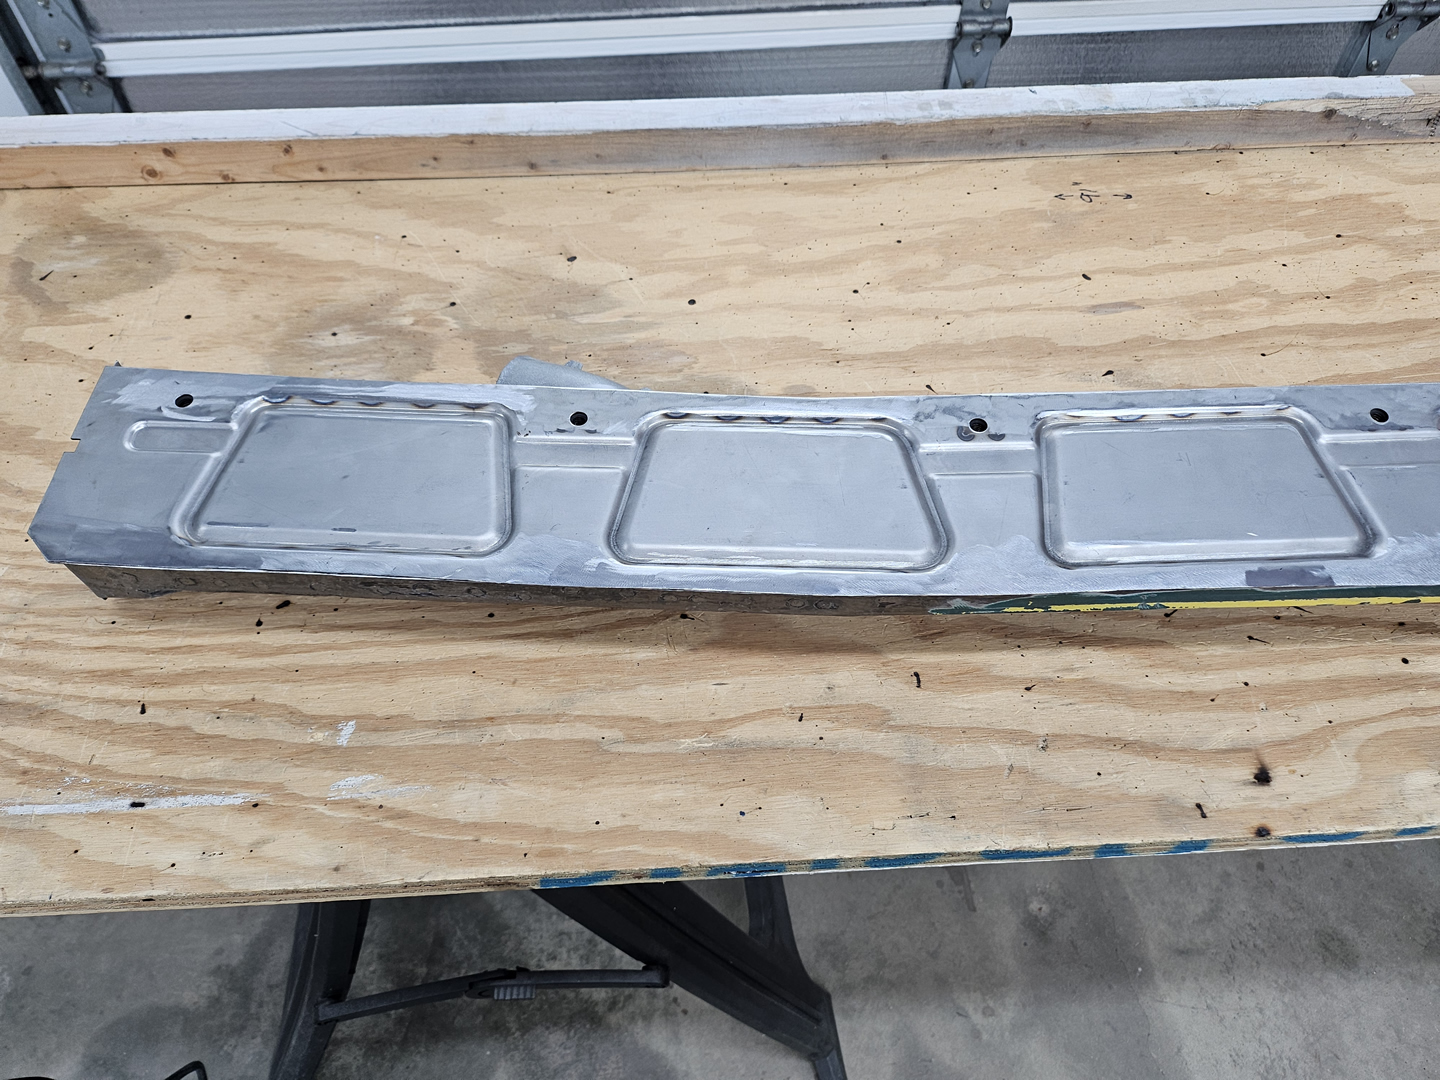
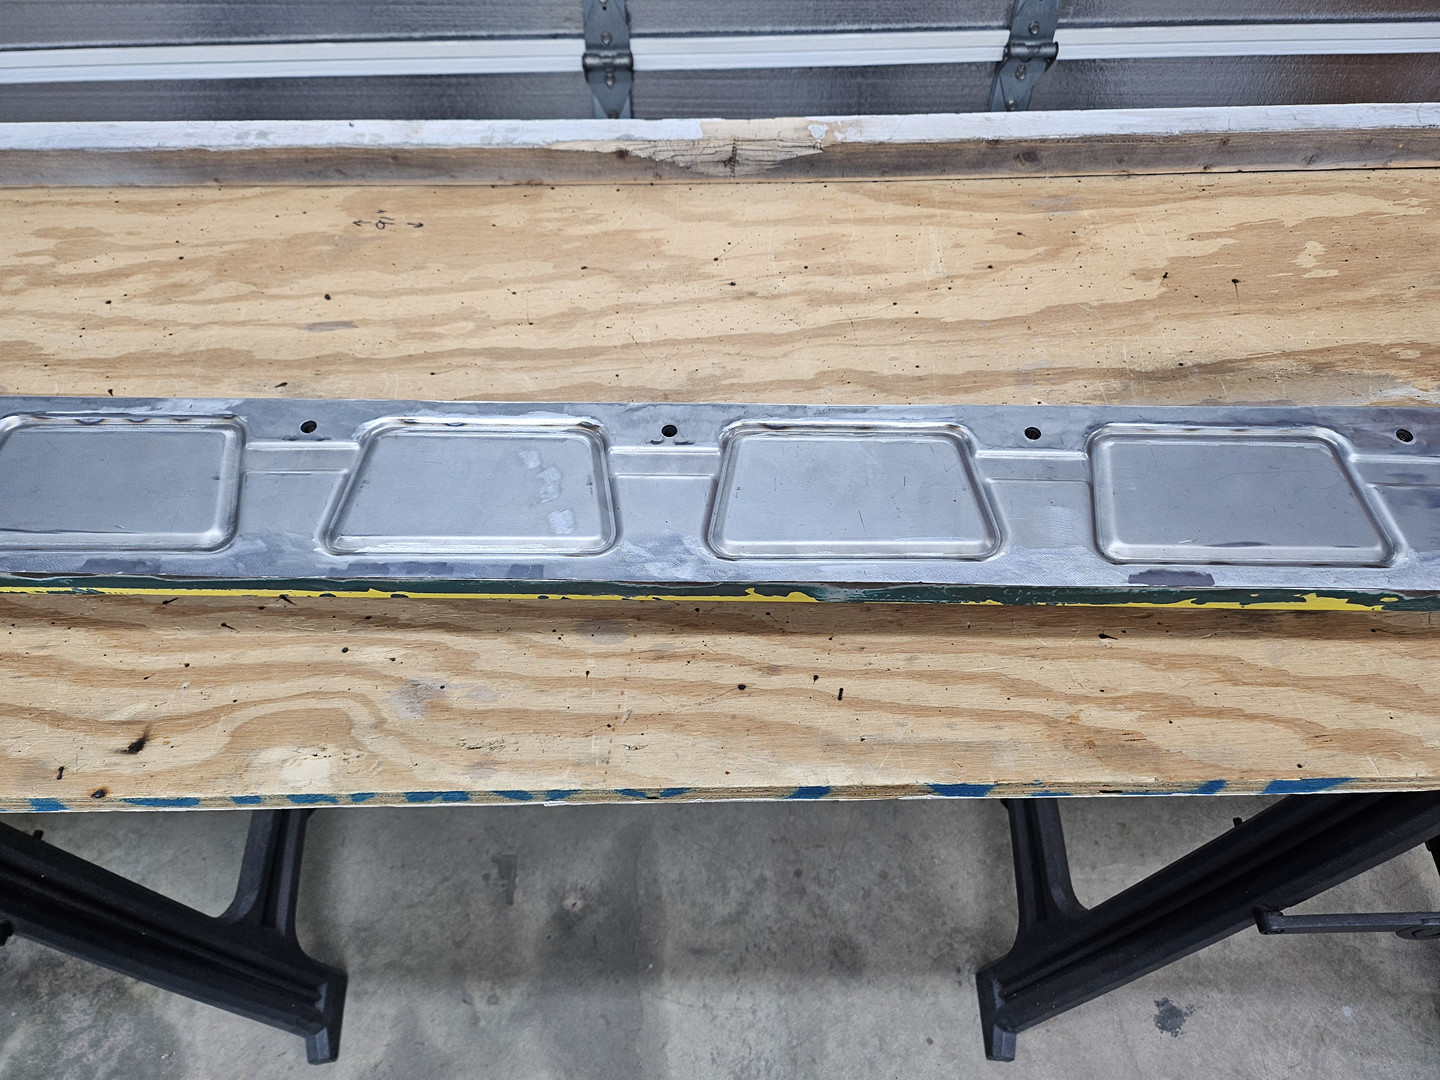
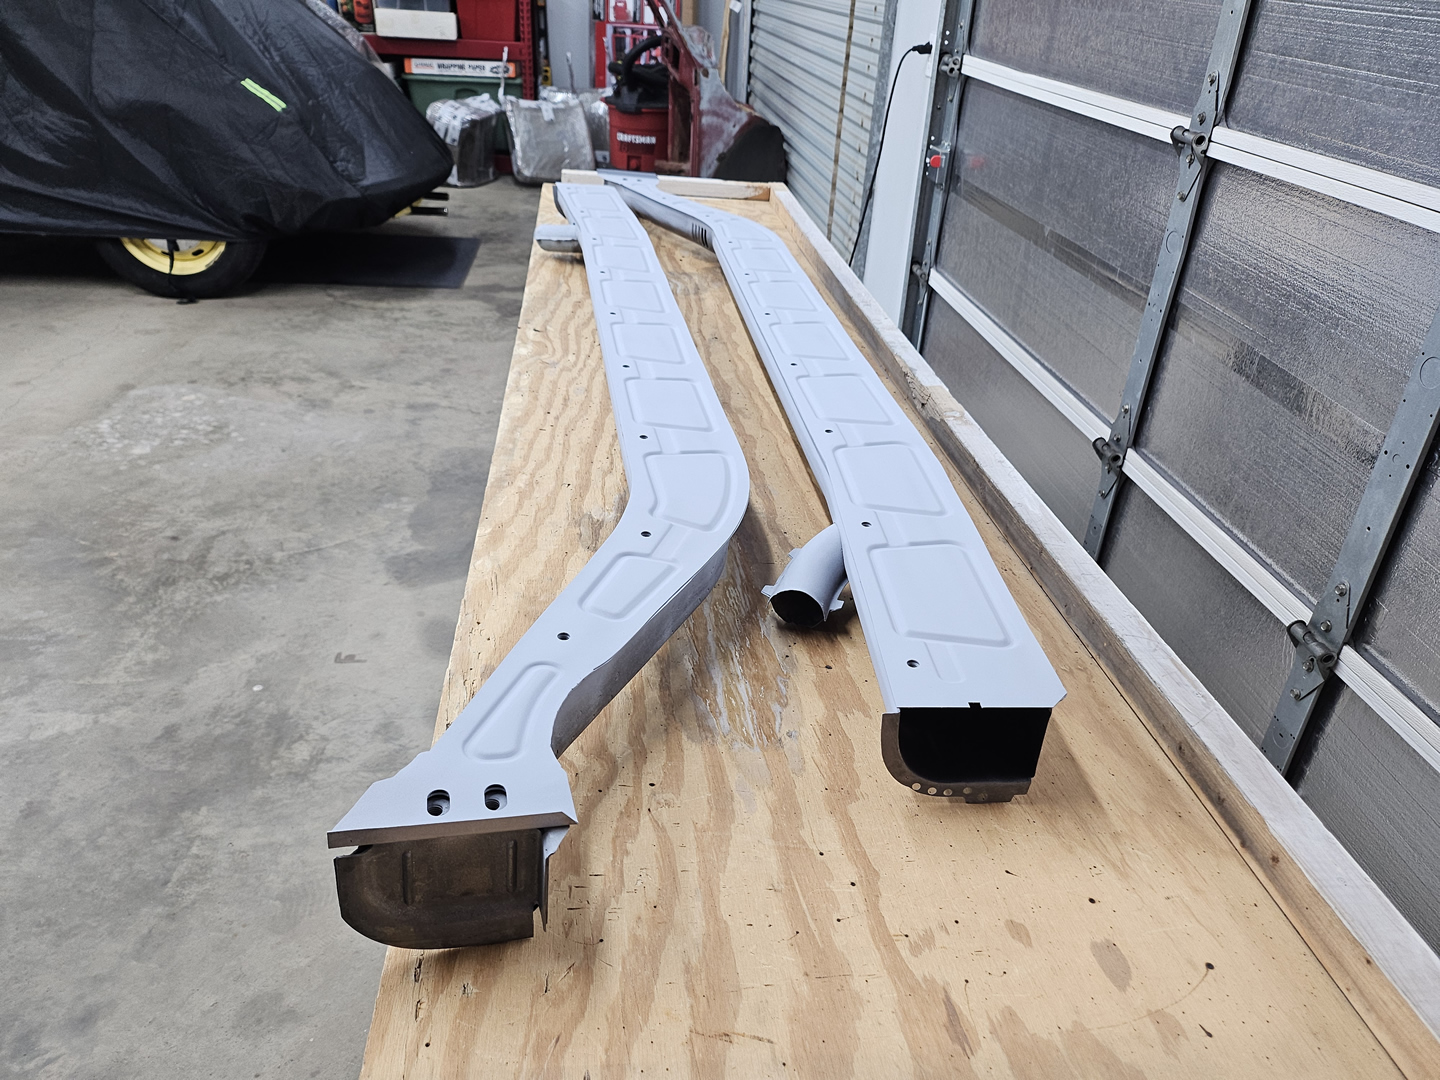
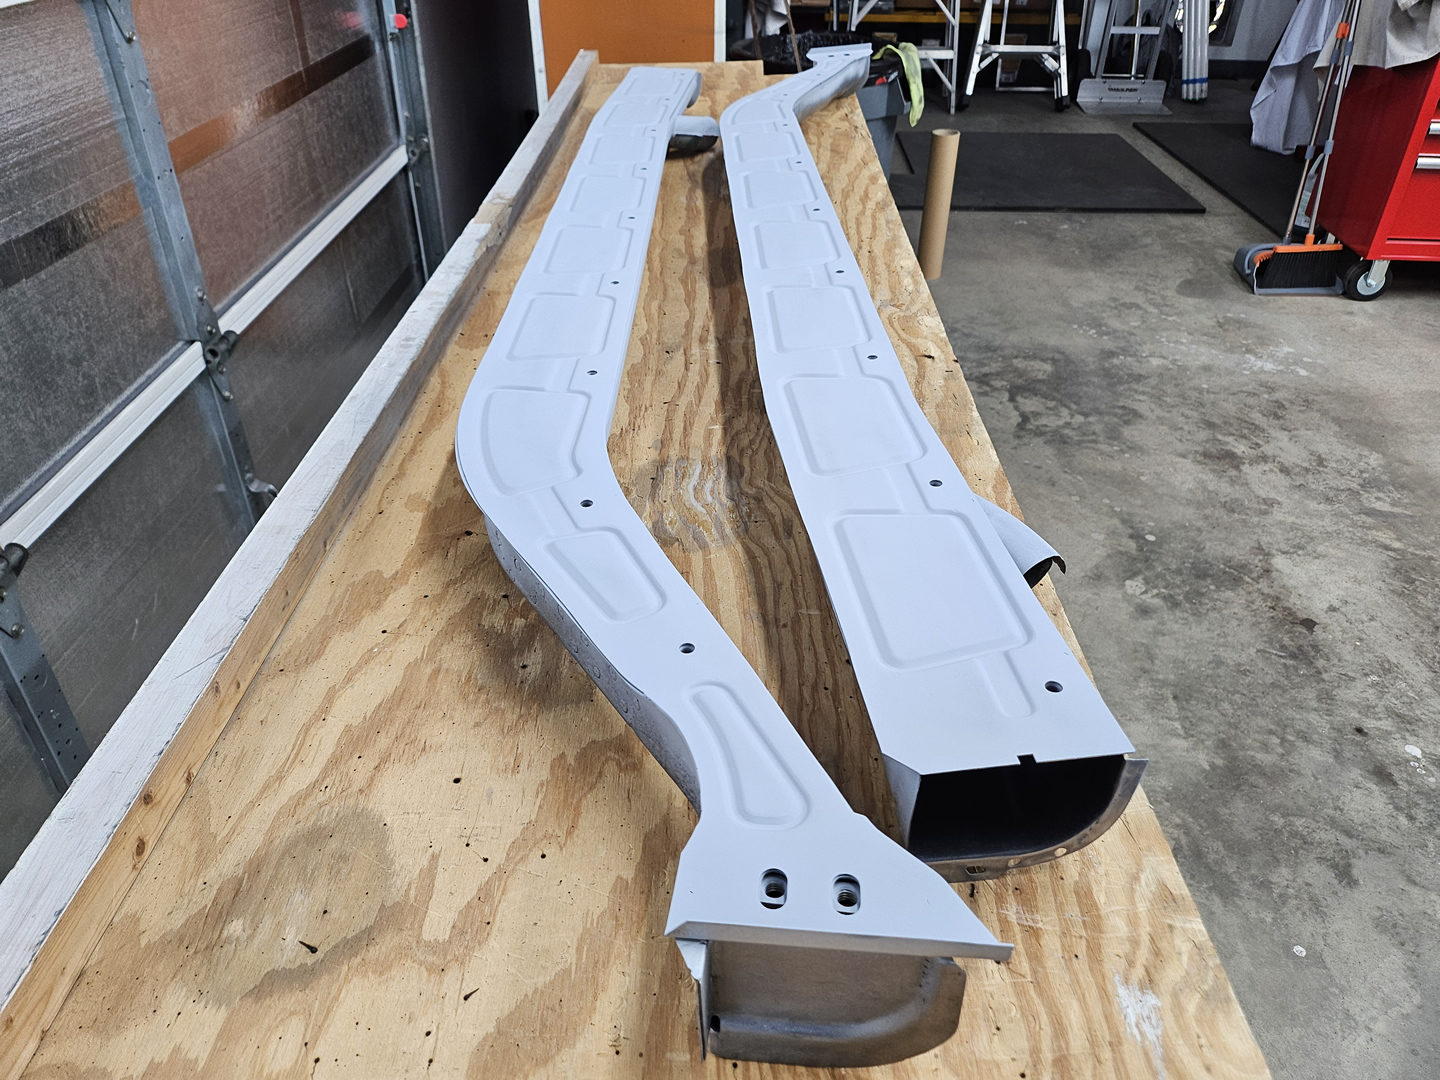
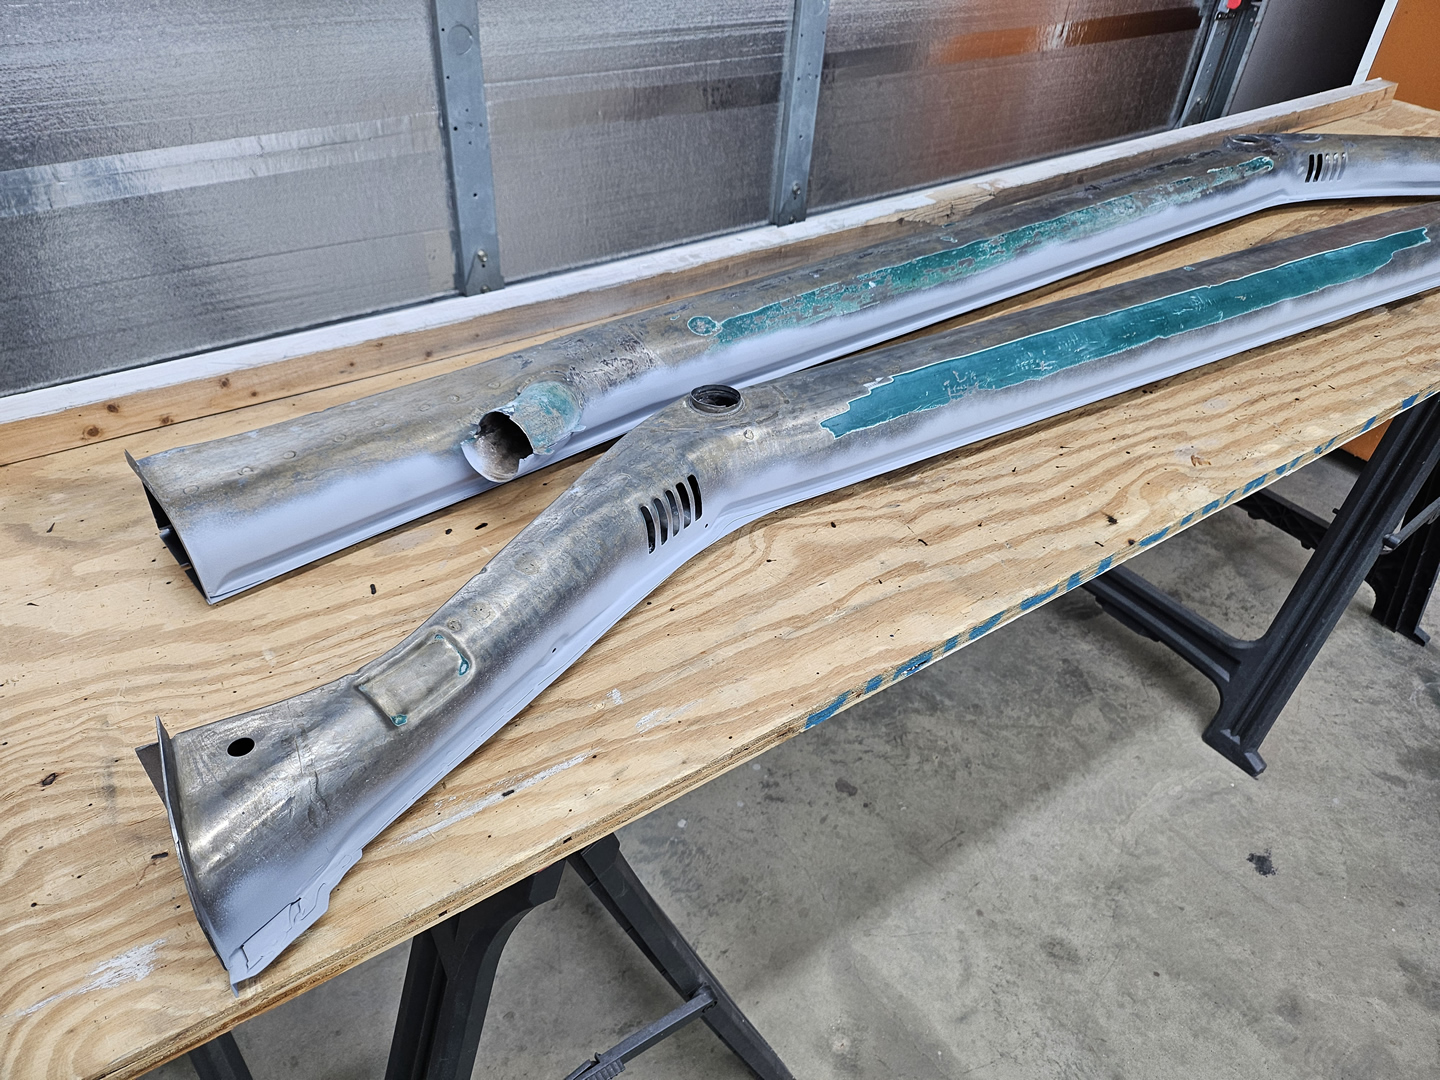
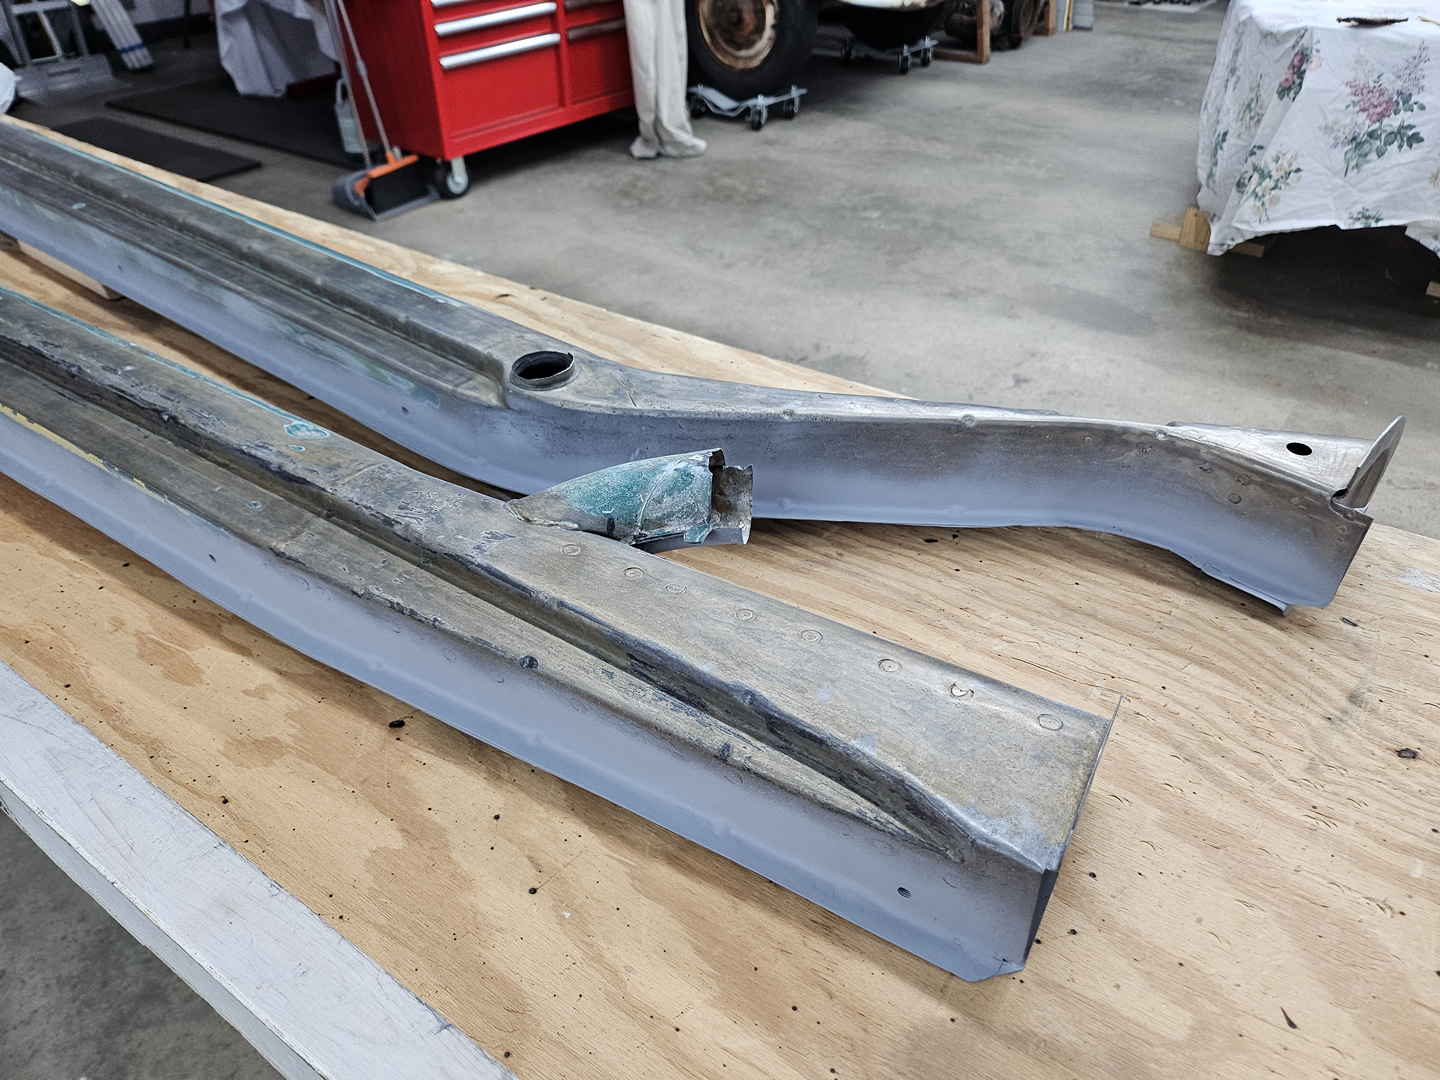
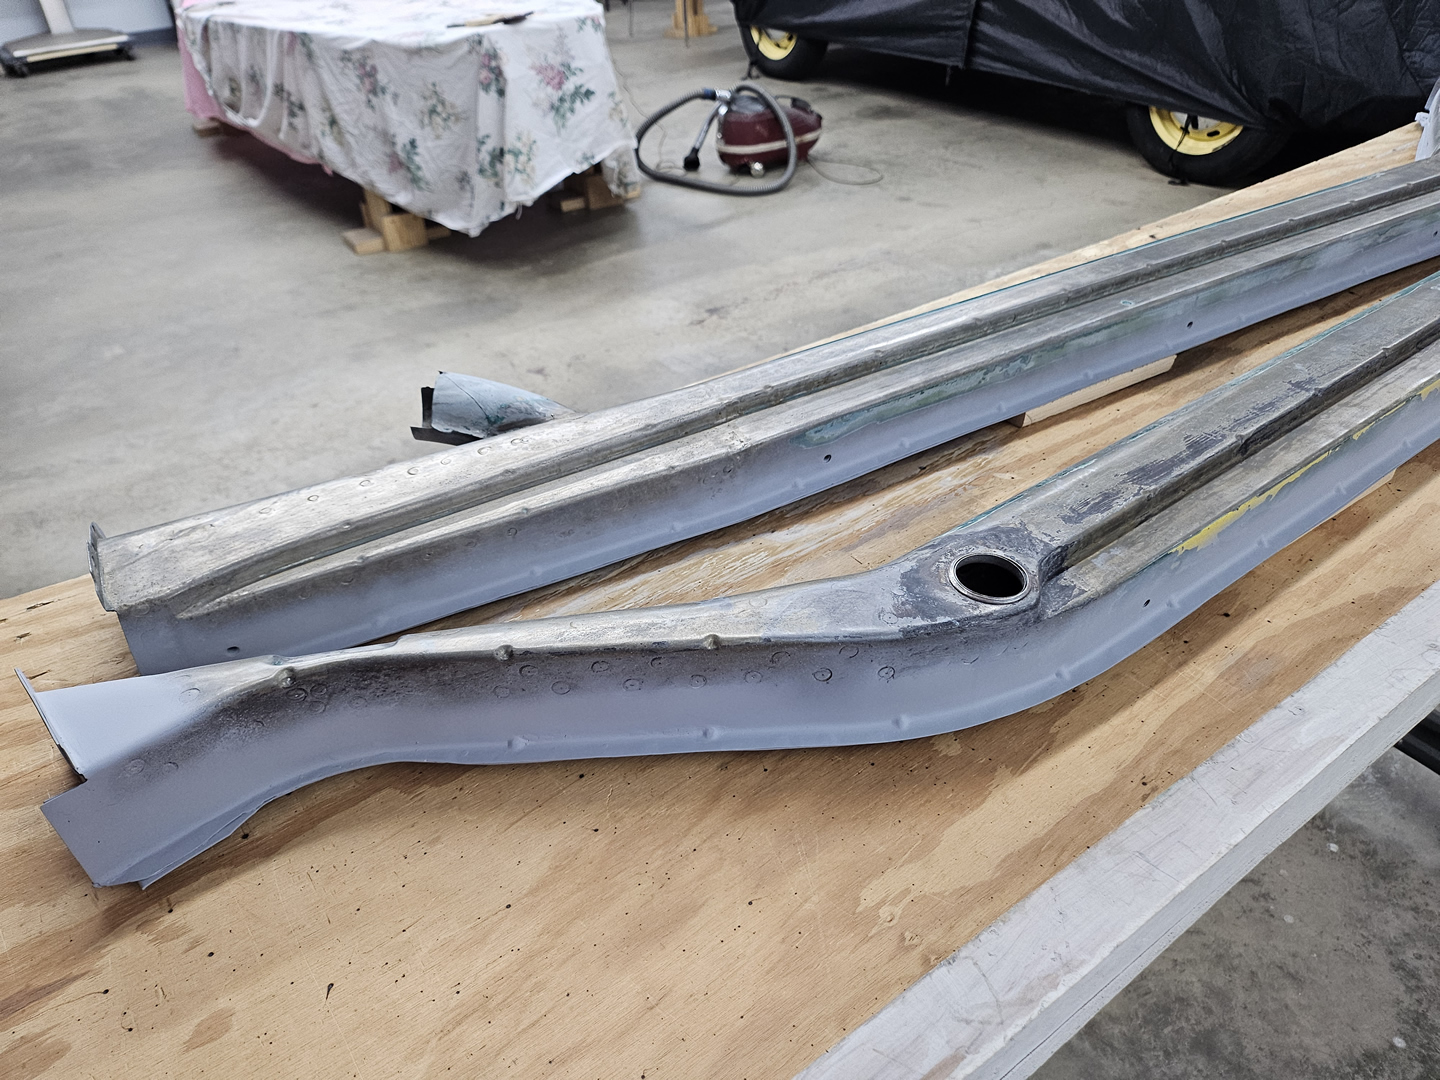
Ten years ago, I purchased two donor heater channels that included the quarter panels. I paid $100 each for them, which is way less than the only acceptable new channels from KlassicFab that are now $500 each with shipping. These will have the bottom plates replaced, which will add another $150 for the Autocraft panels that are almost exactly like the originals. It's a big job to do this, but I want to make sure that they are solid internally and to rust treat and protect them inside and out. Rather than trying to preserve the bottom plates and re-use them, I am going to sacrifice them to make sure that the other parts of the channels are intact. There are many spot welds on the channels, and it would be almost impossible to remove the bottom plates without damaging the plates and/or the channels. There are also quite a few repair that need to be done on both of the channels as well.
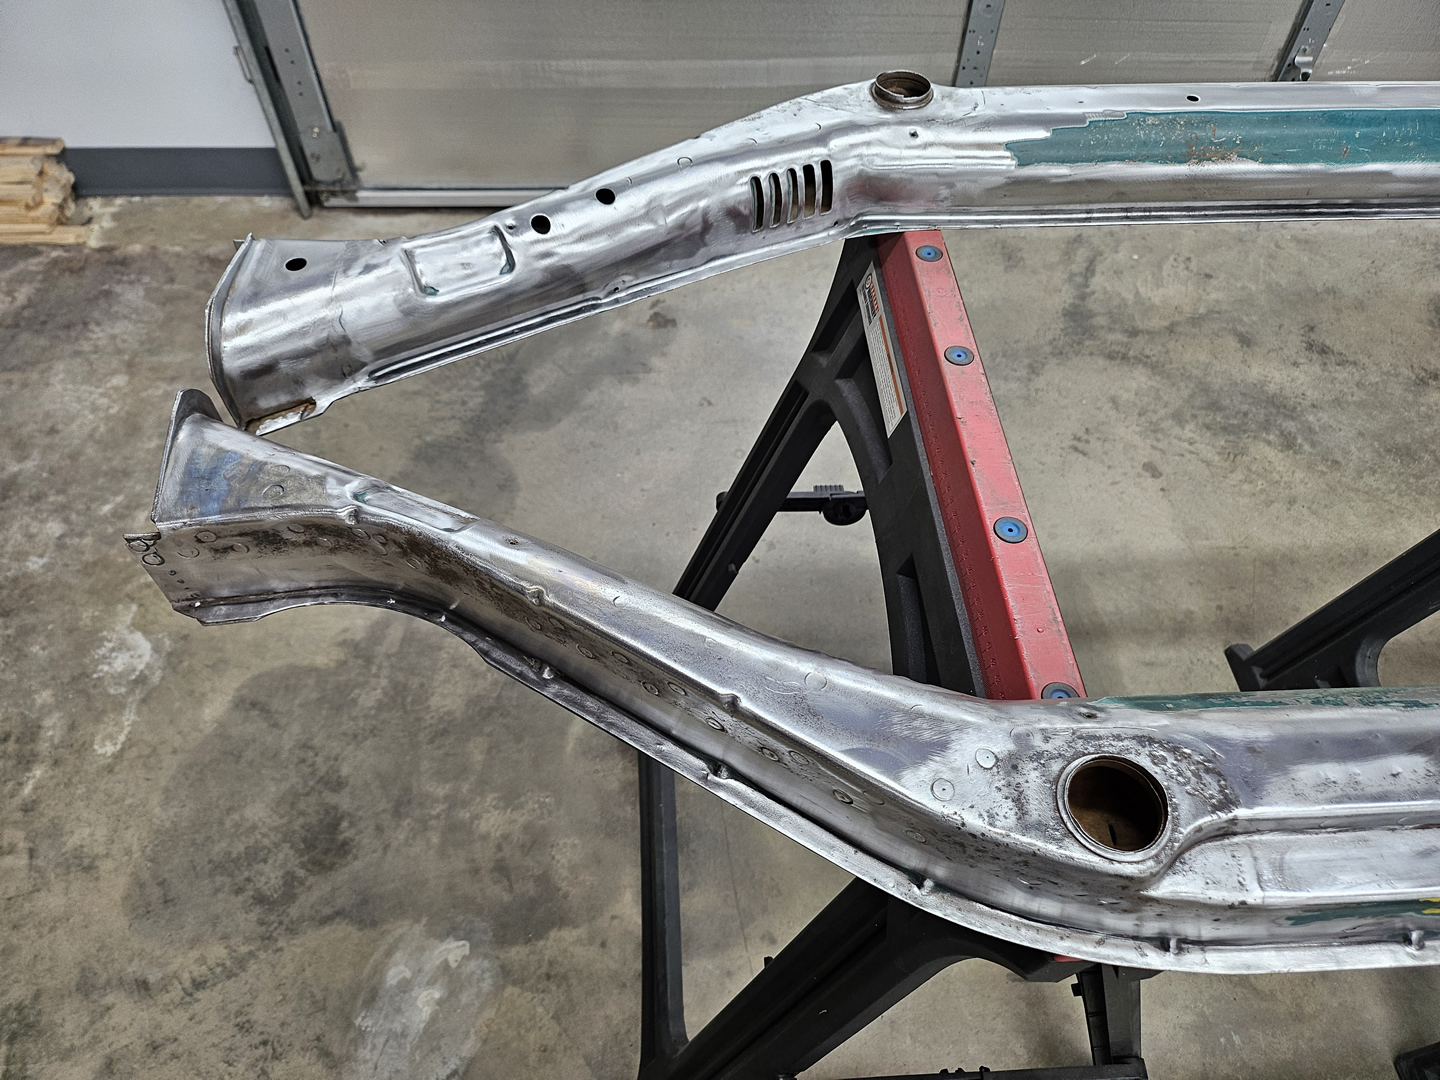
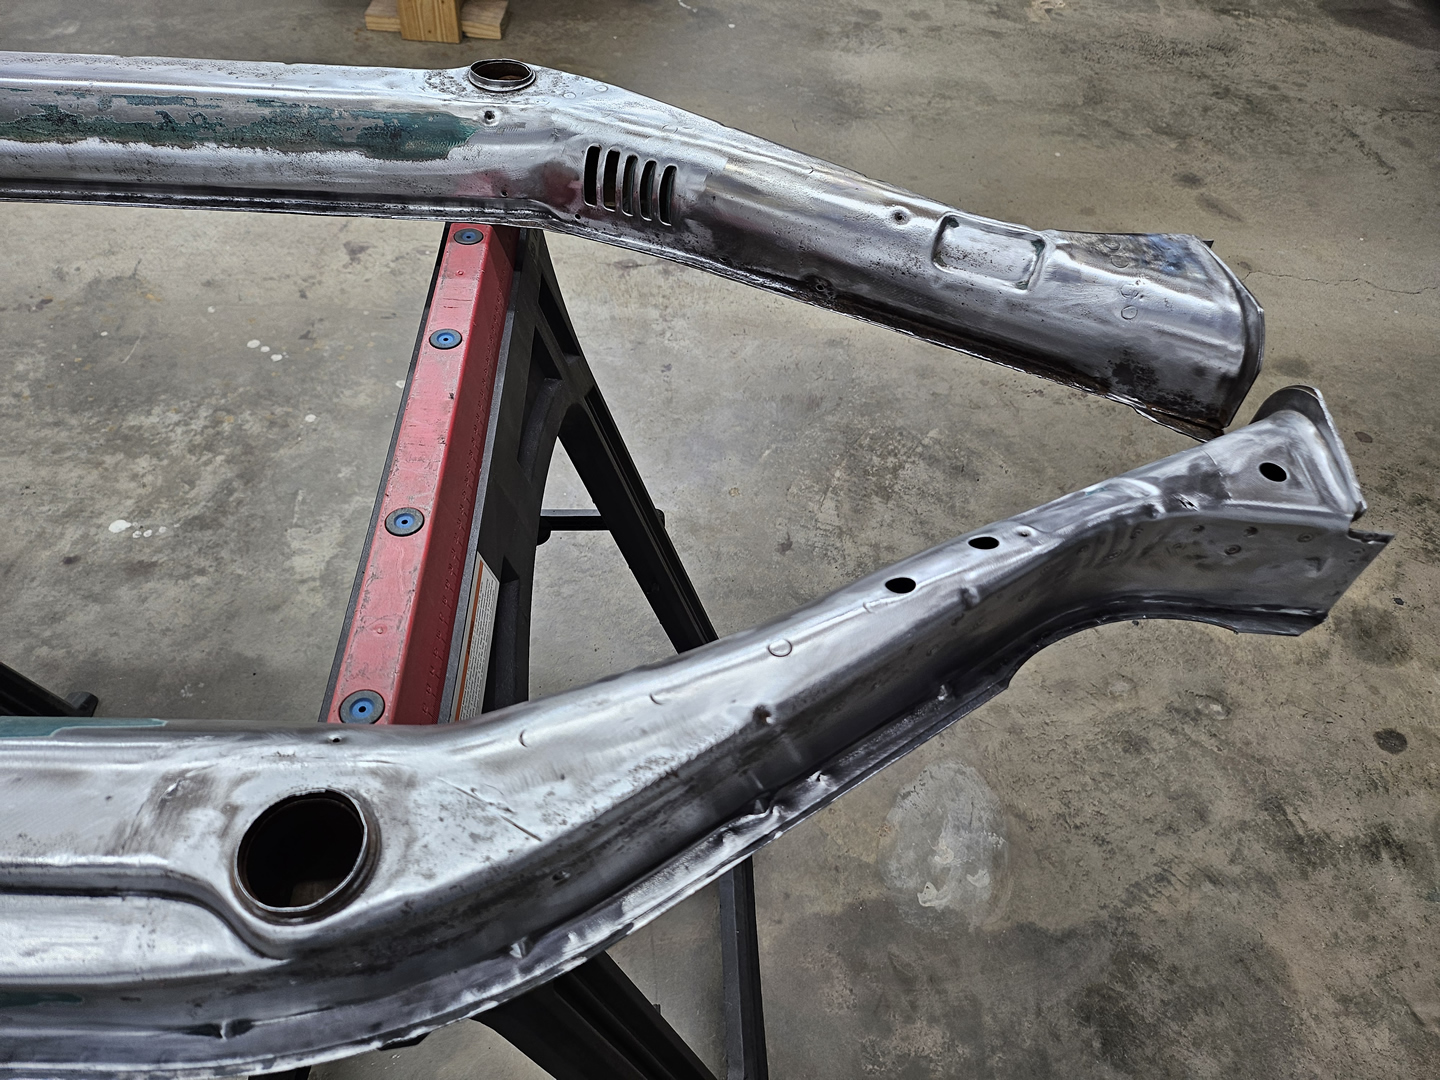
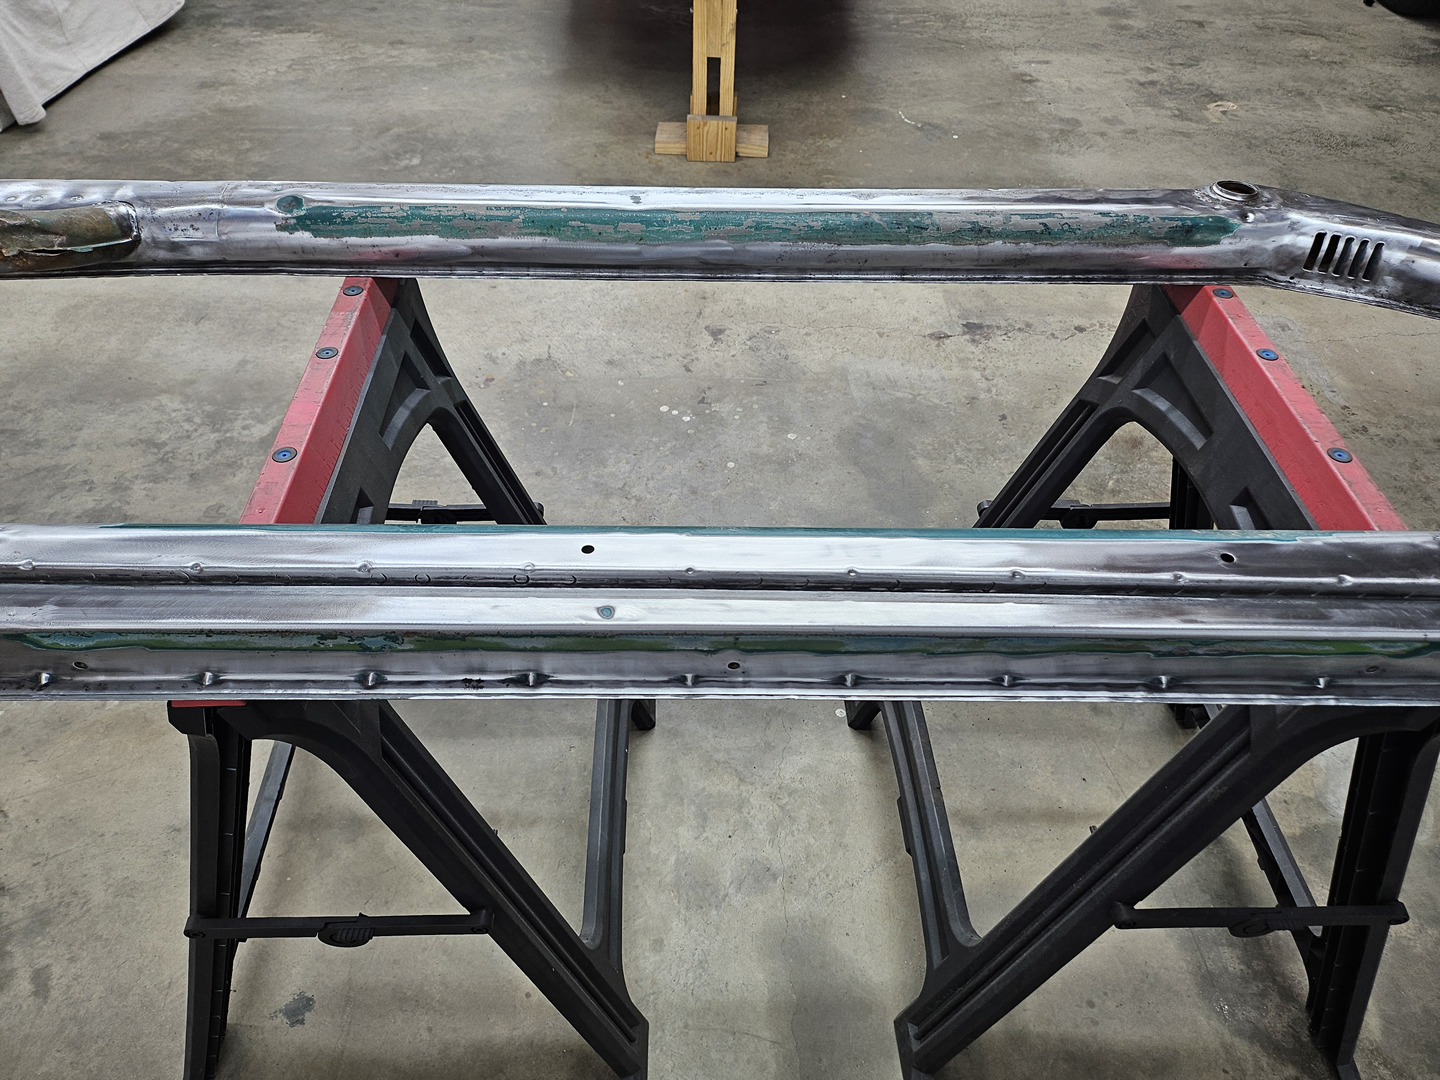
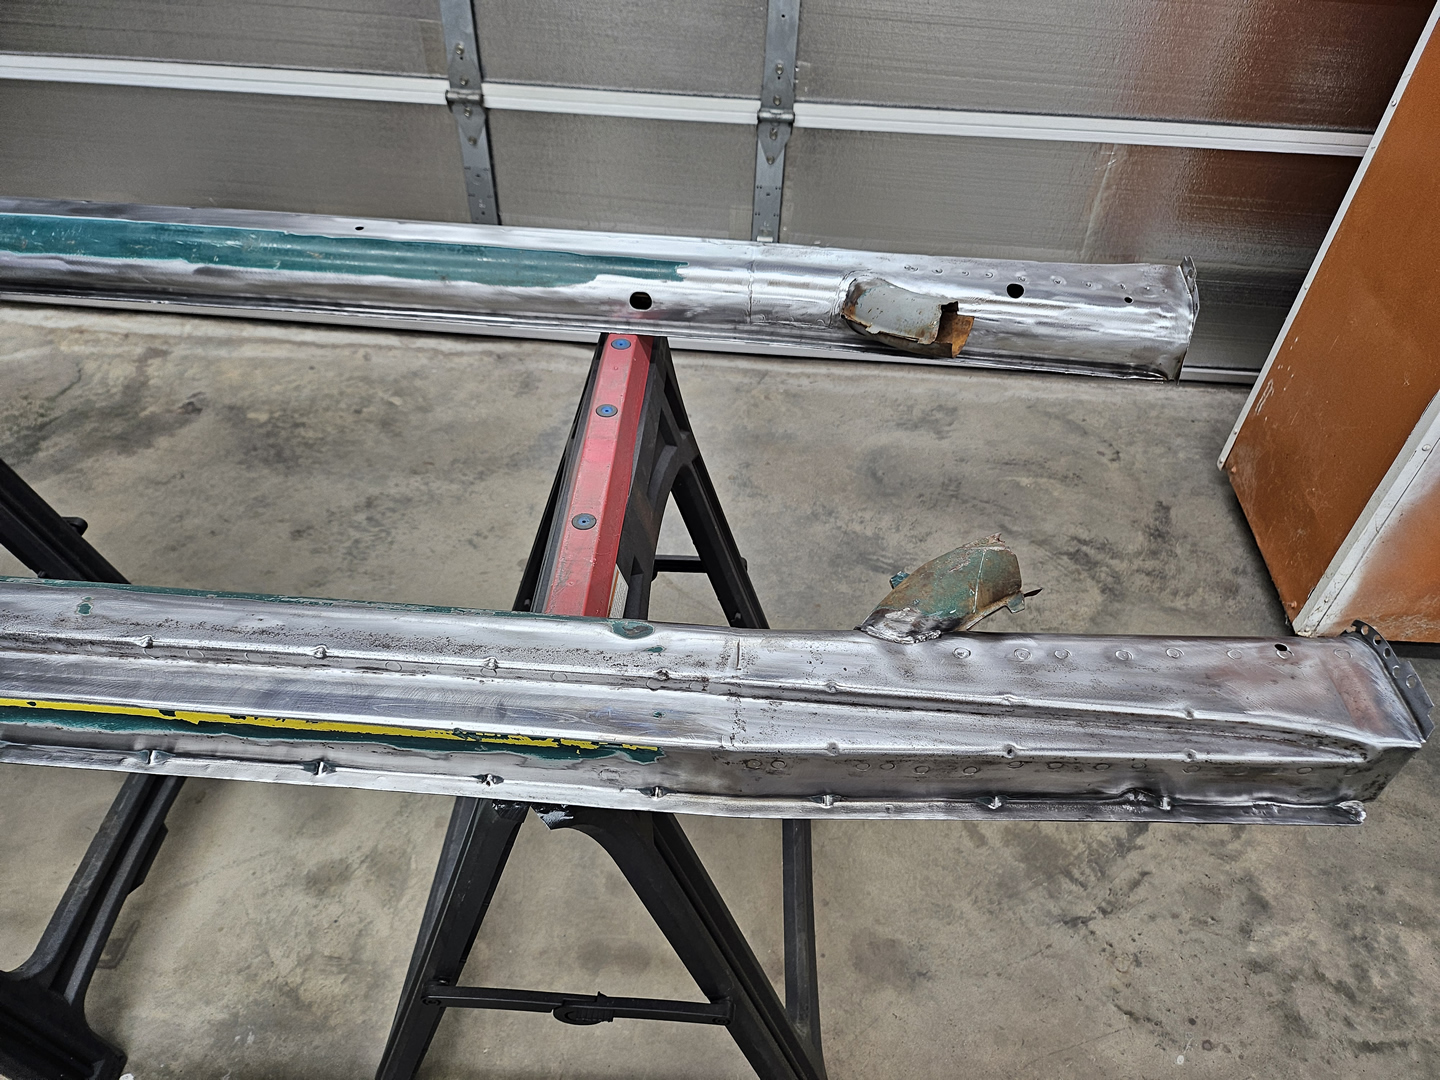
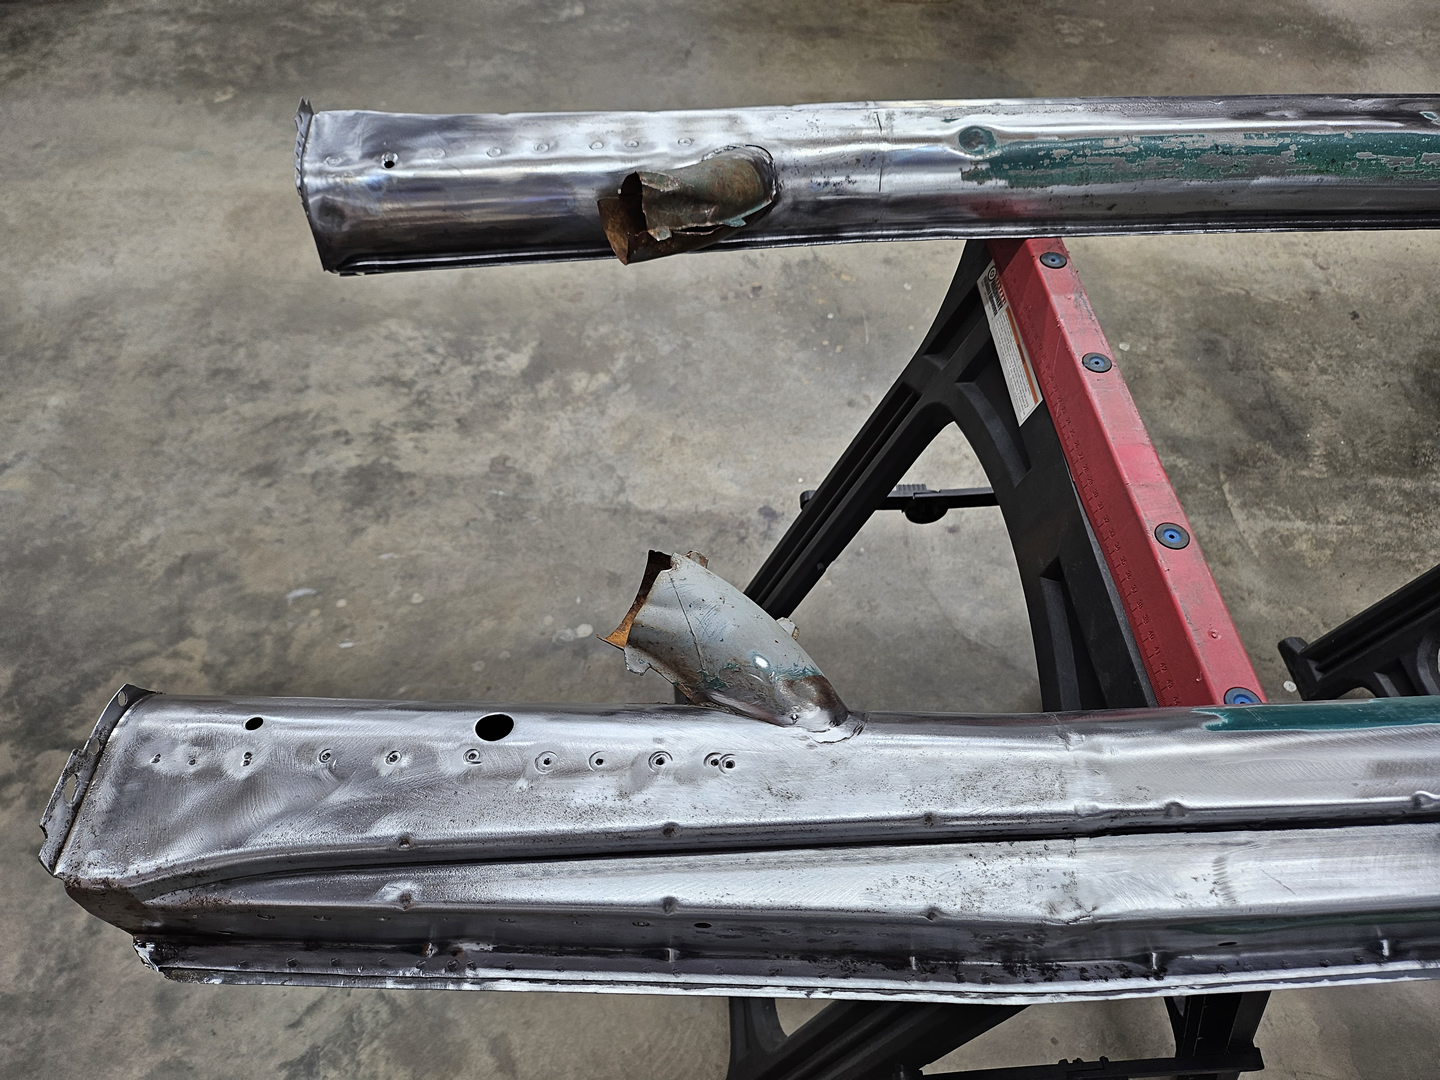
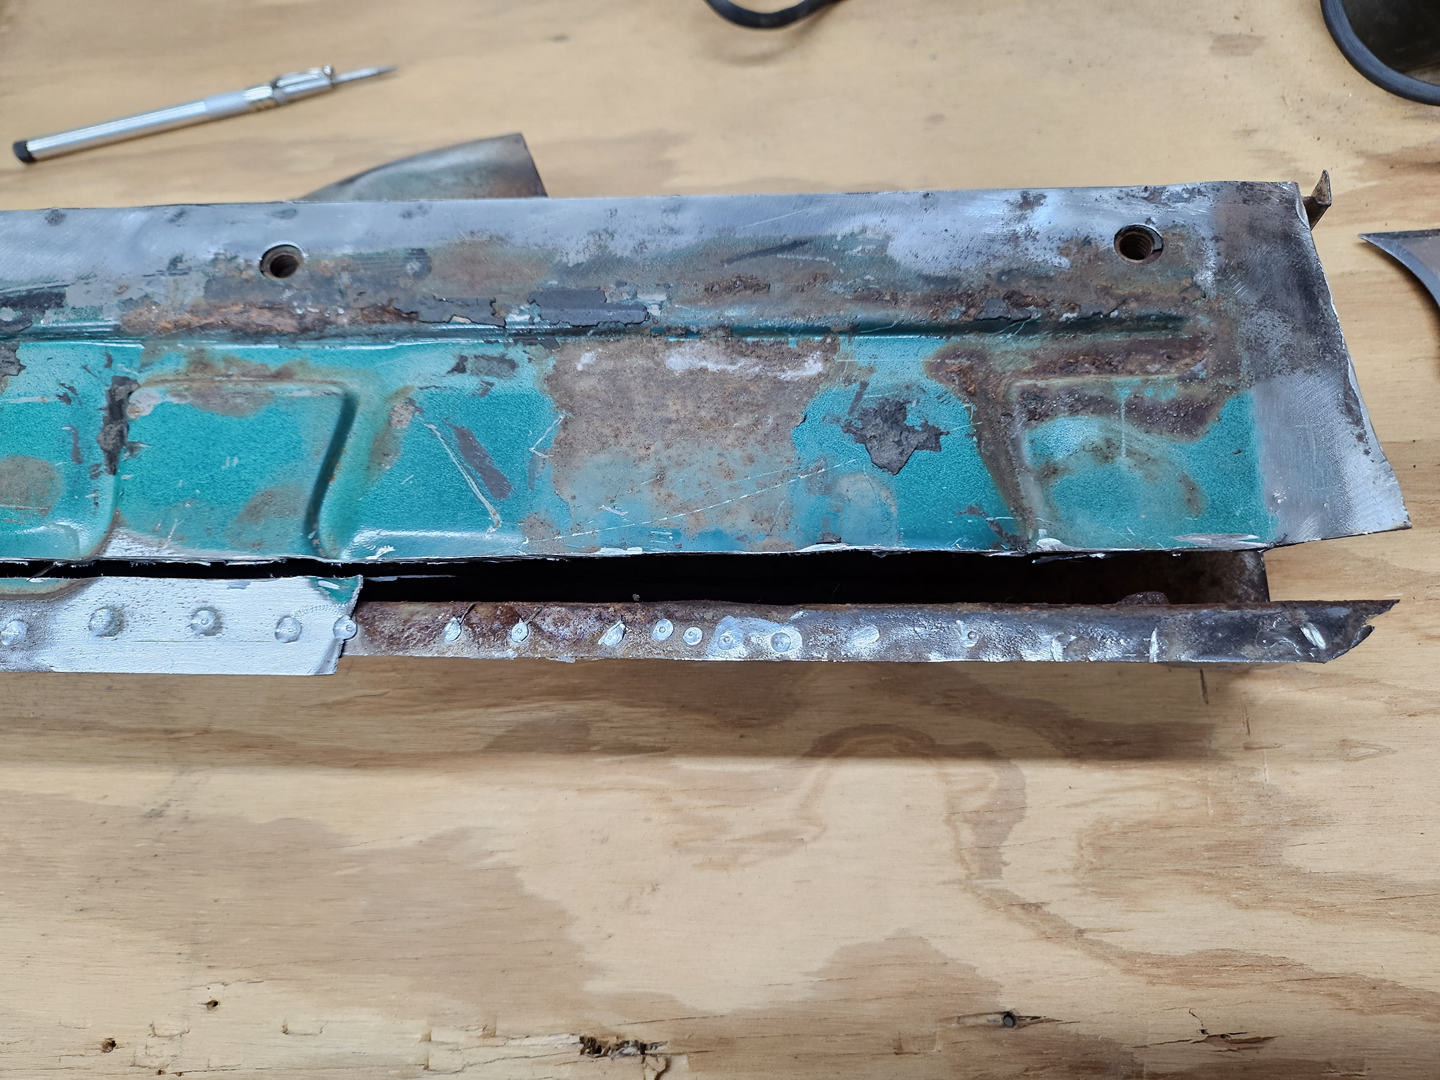
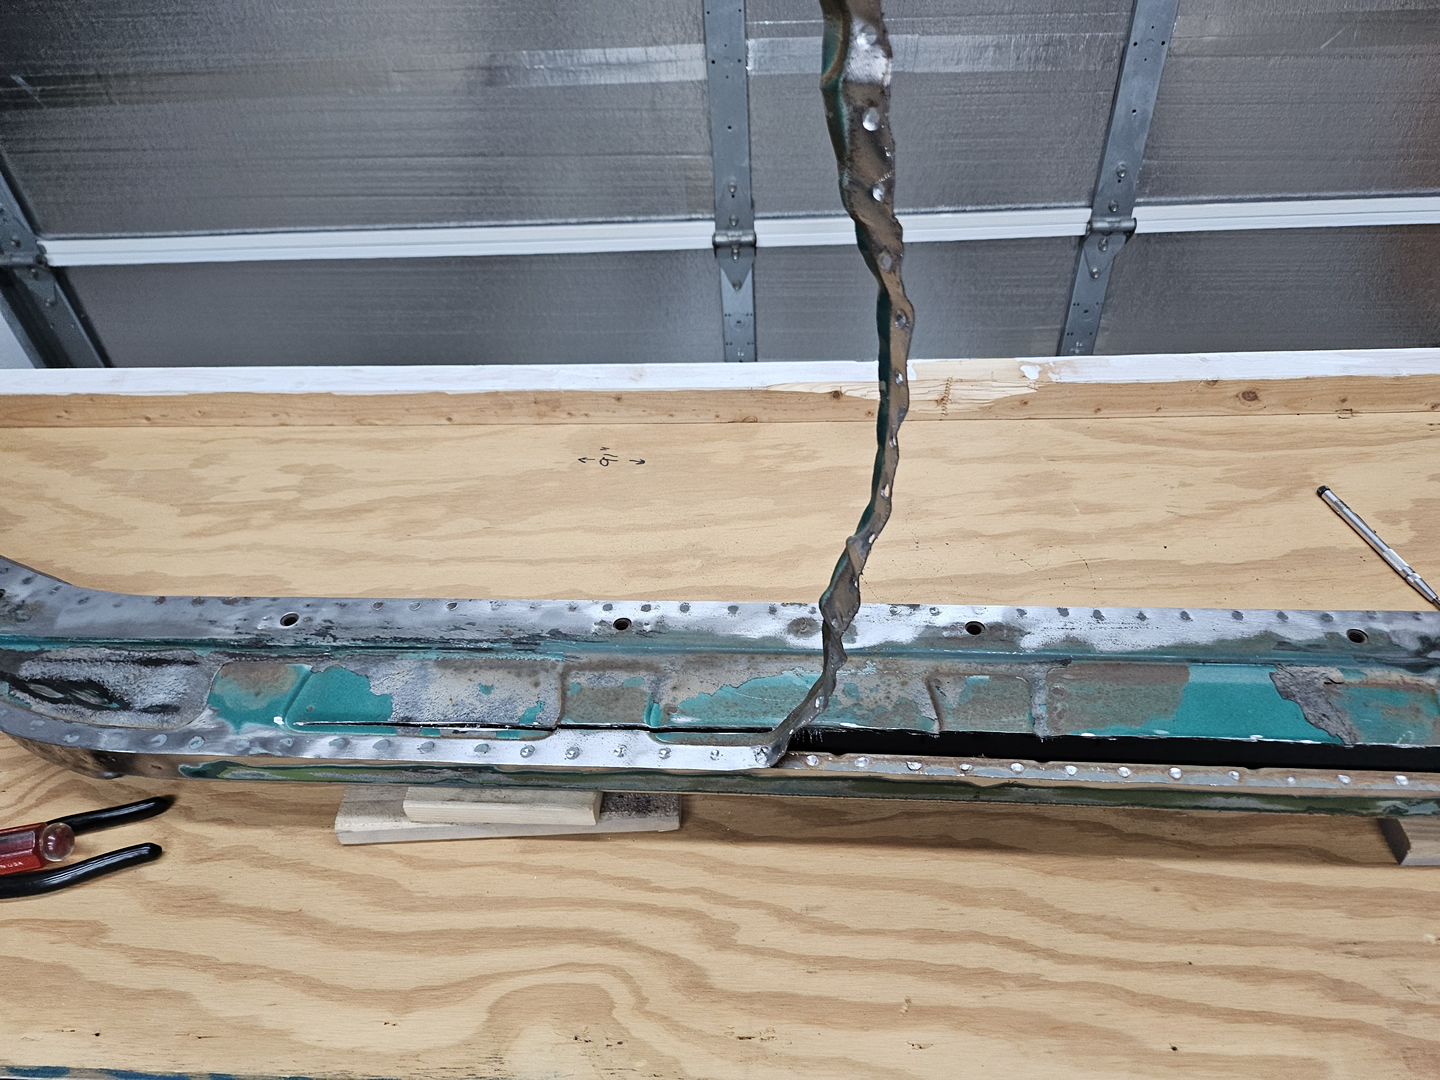
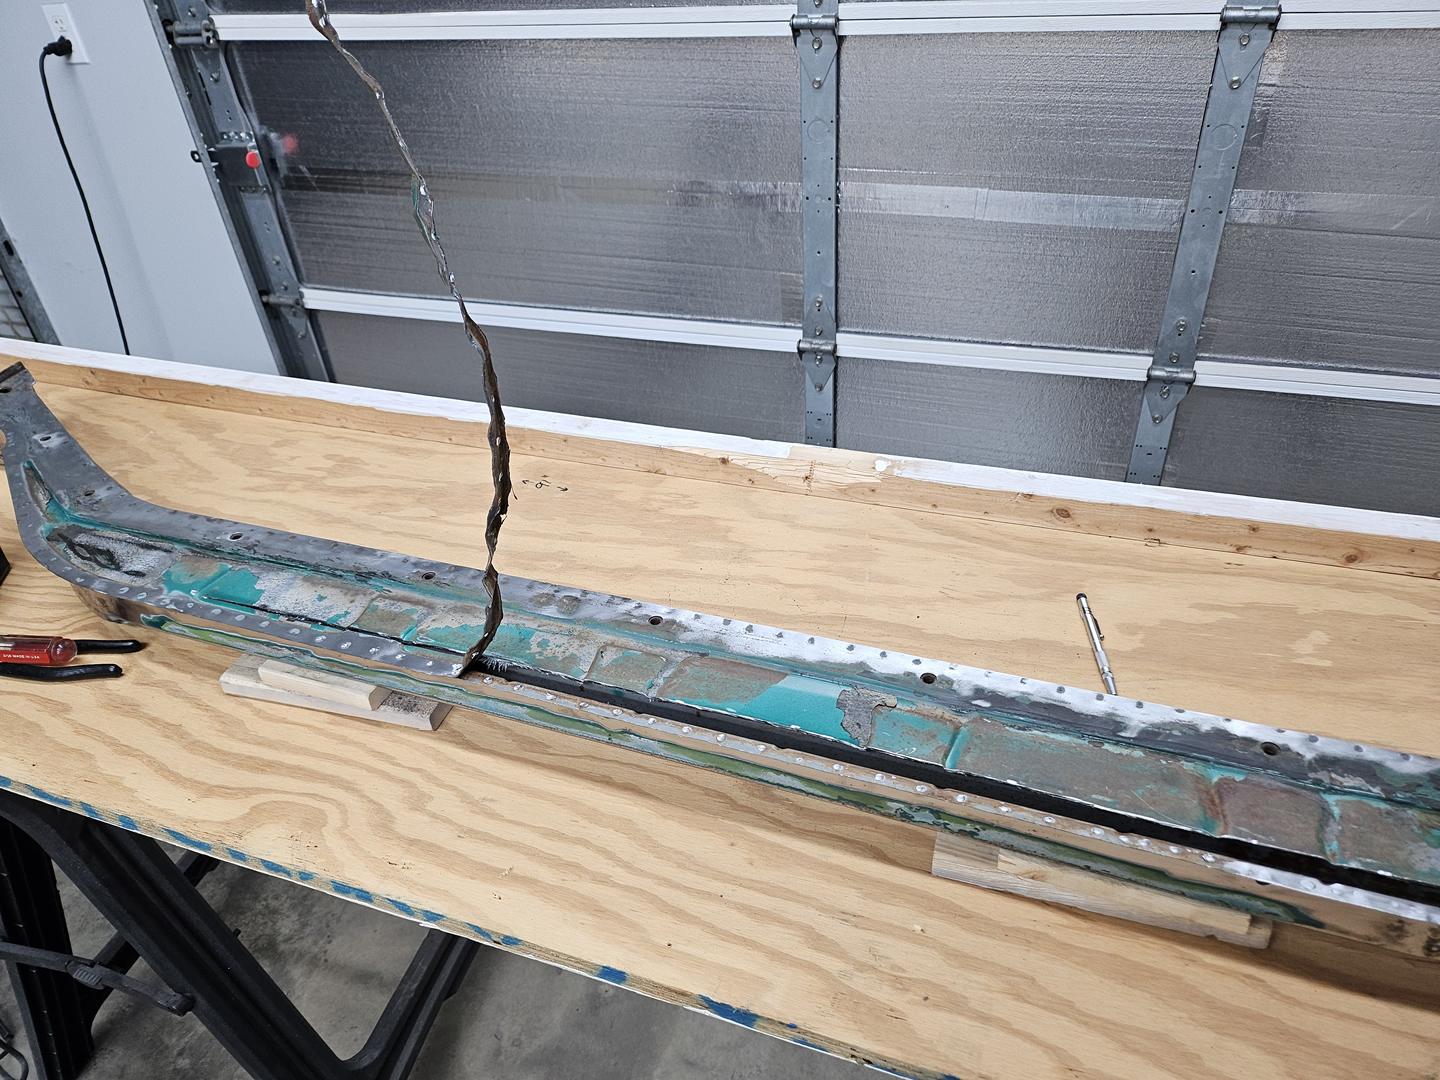
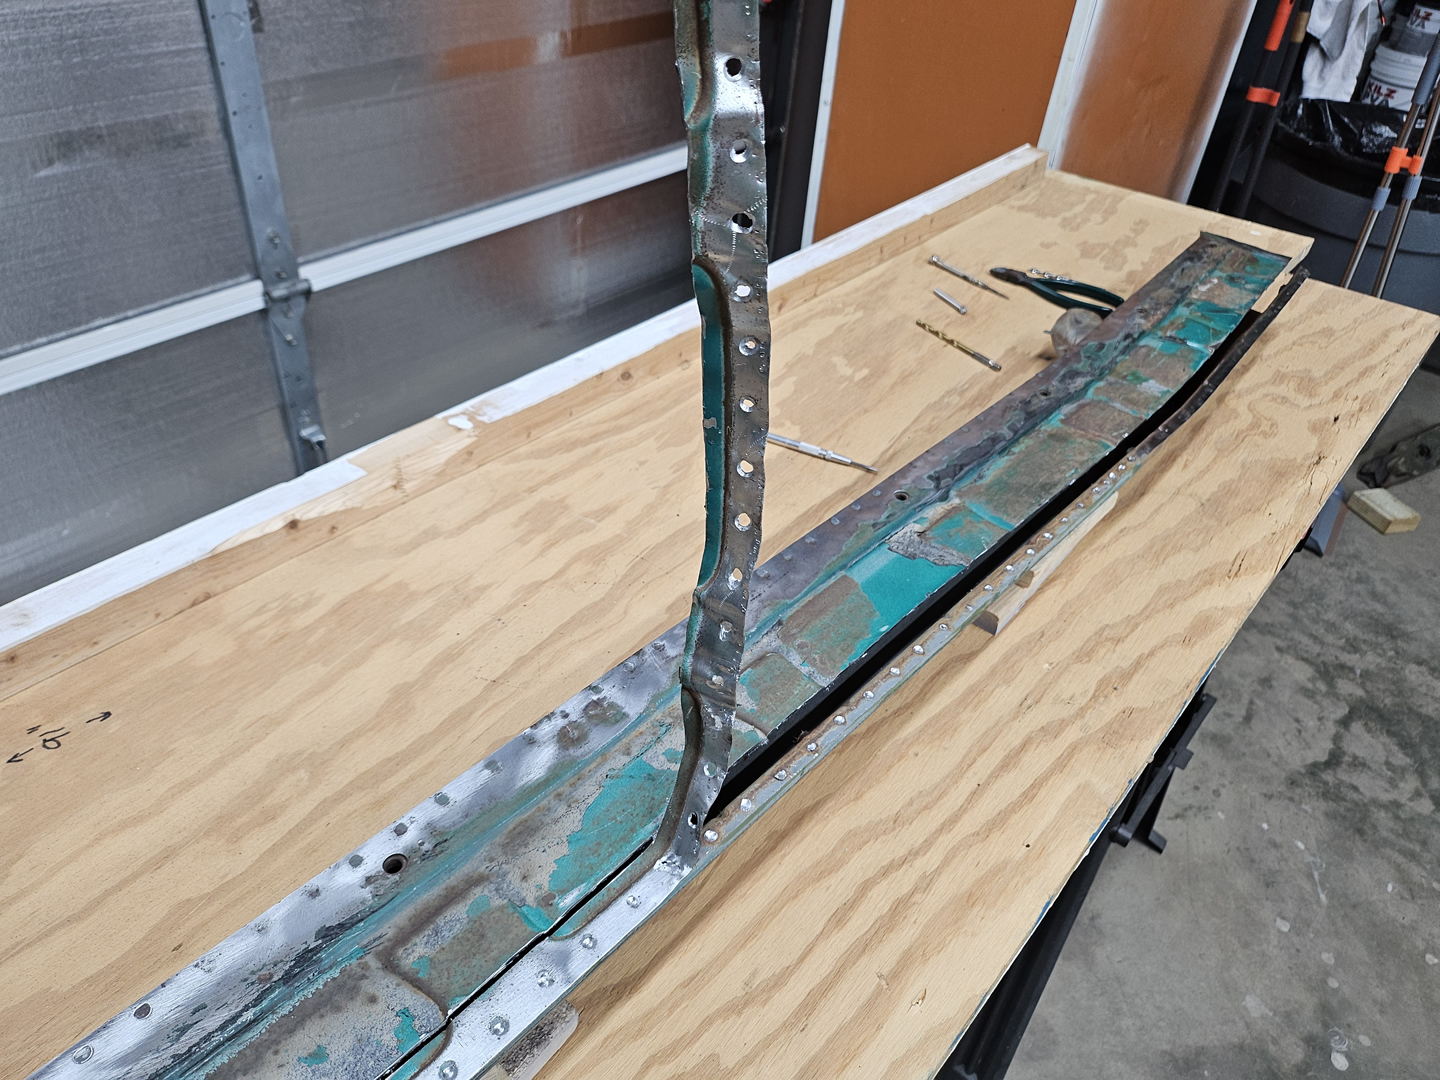
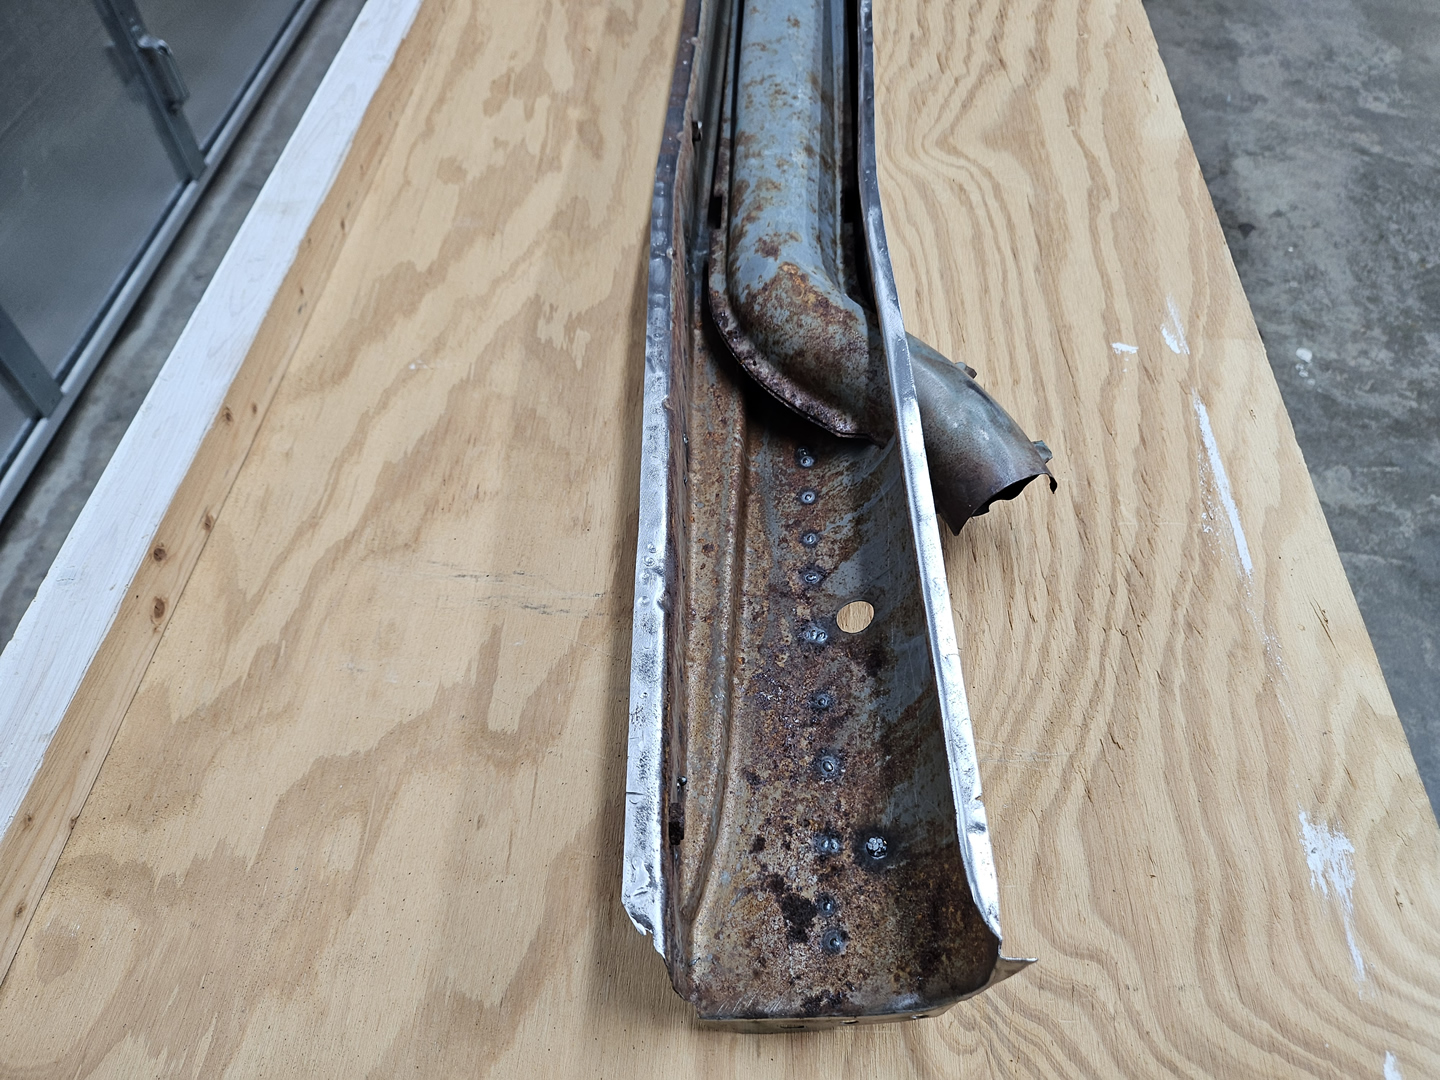
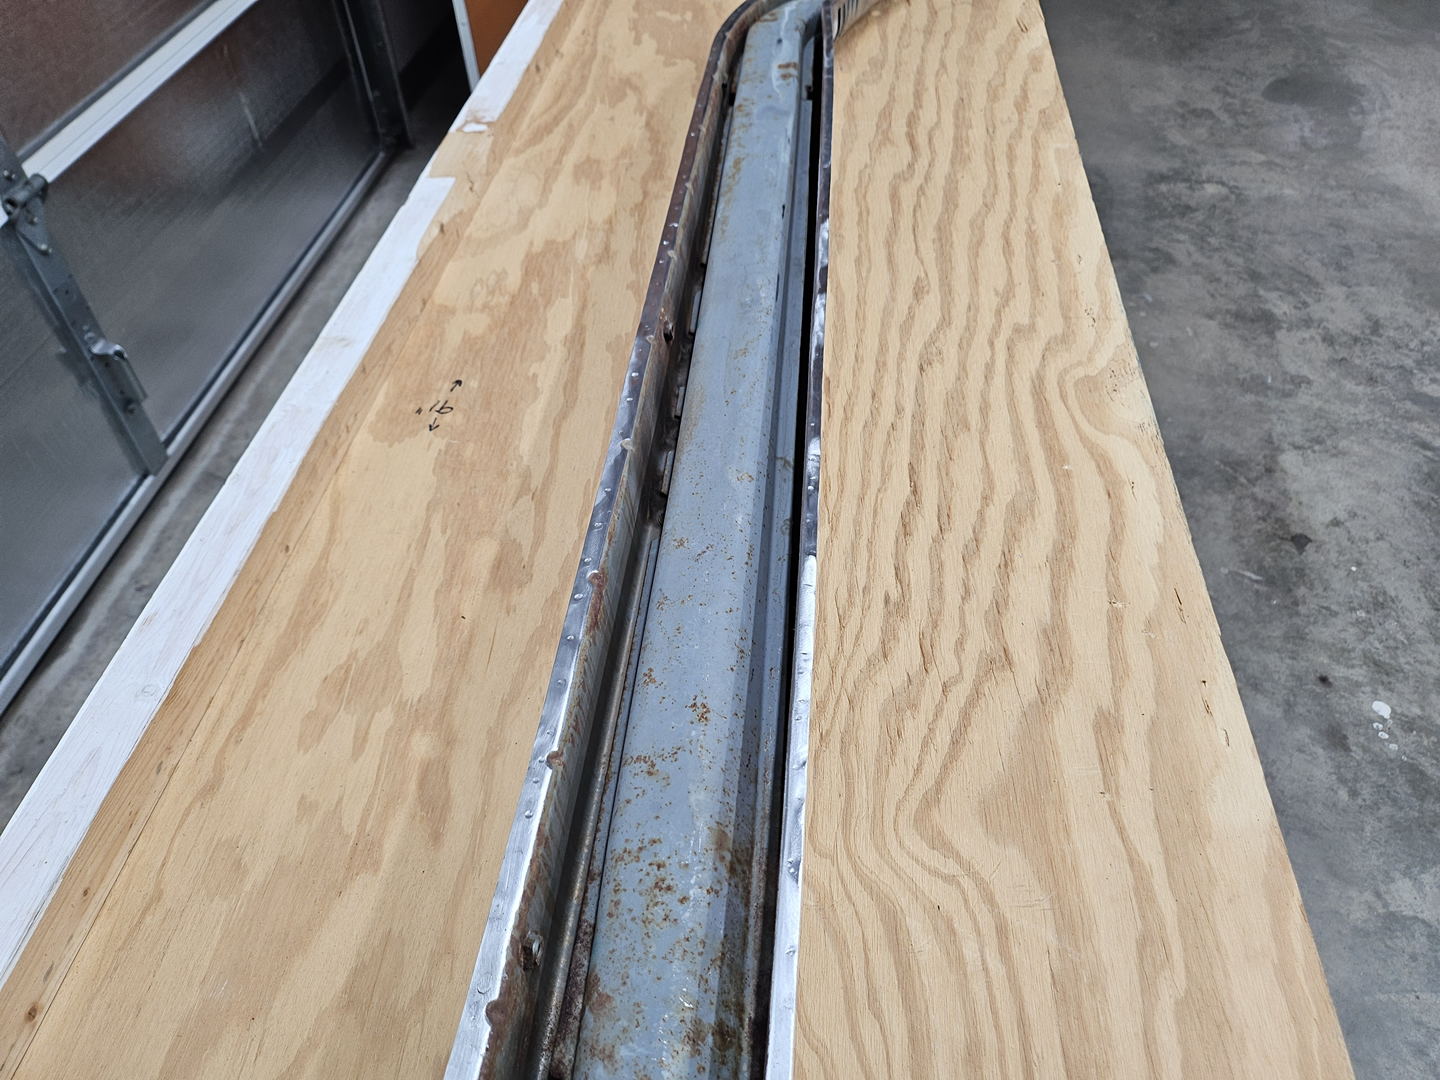
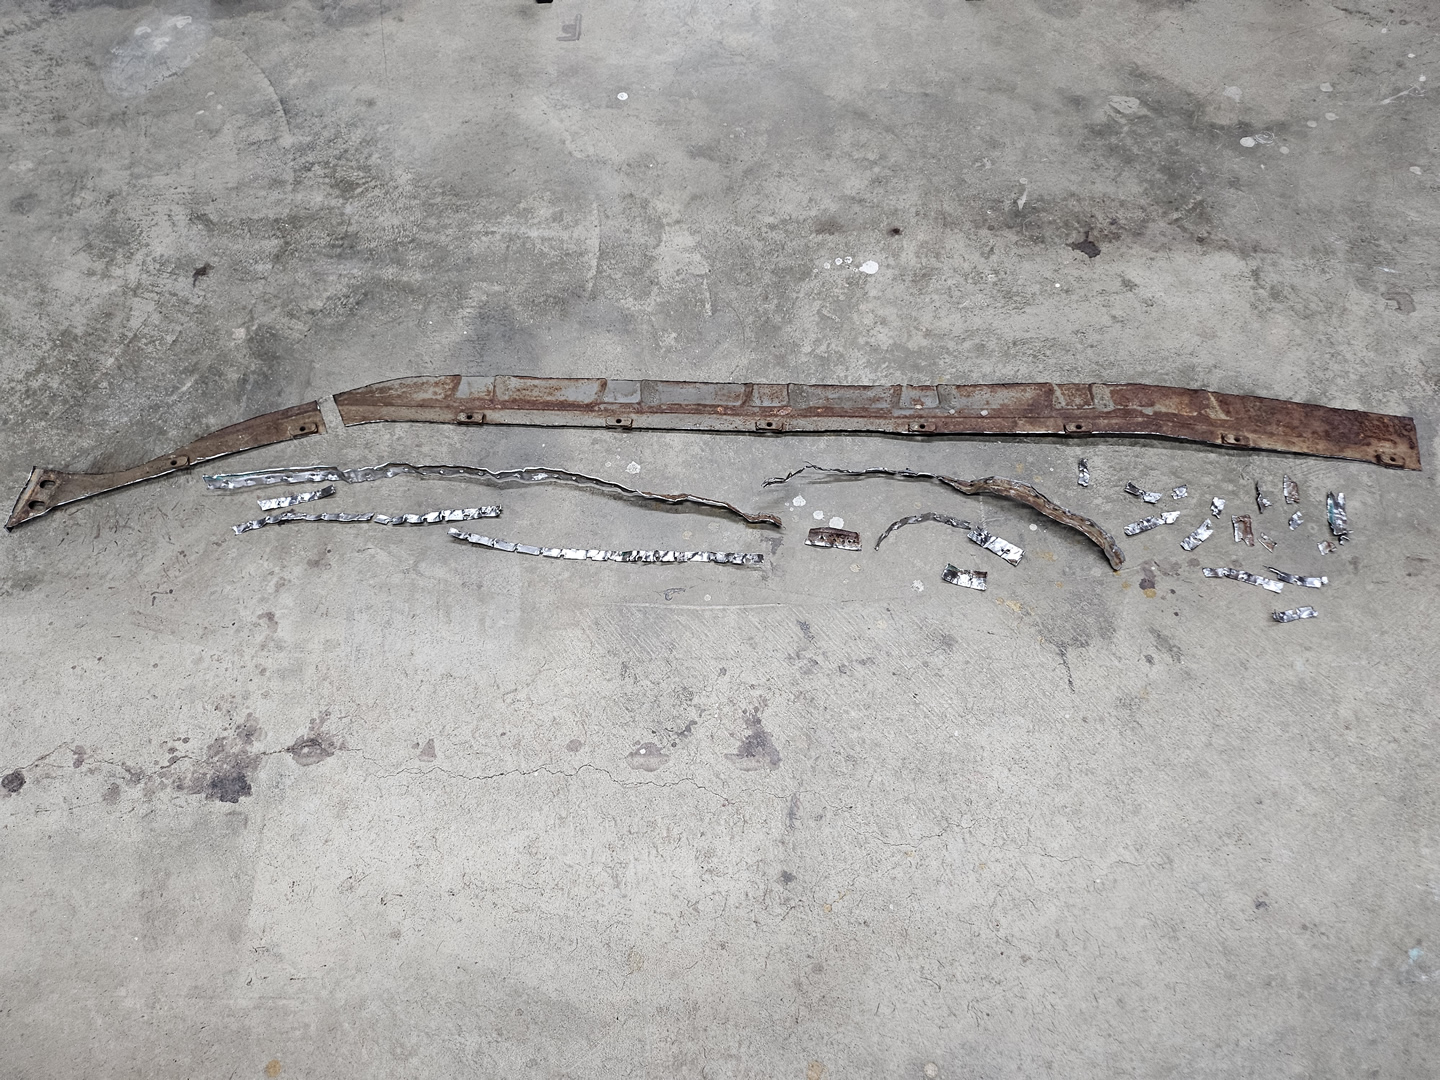
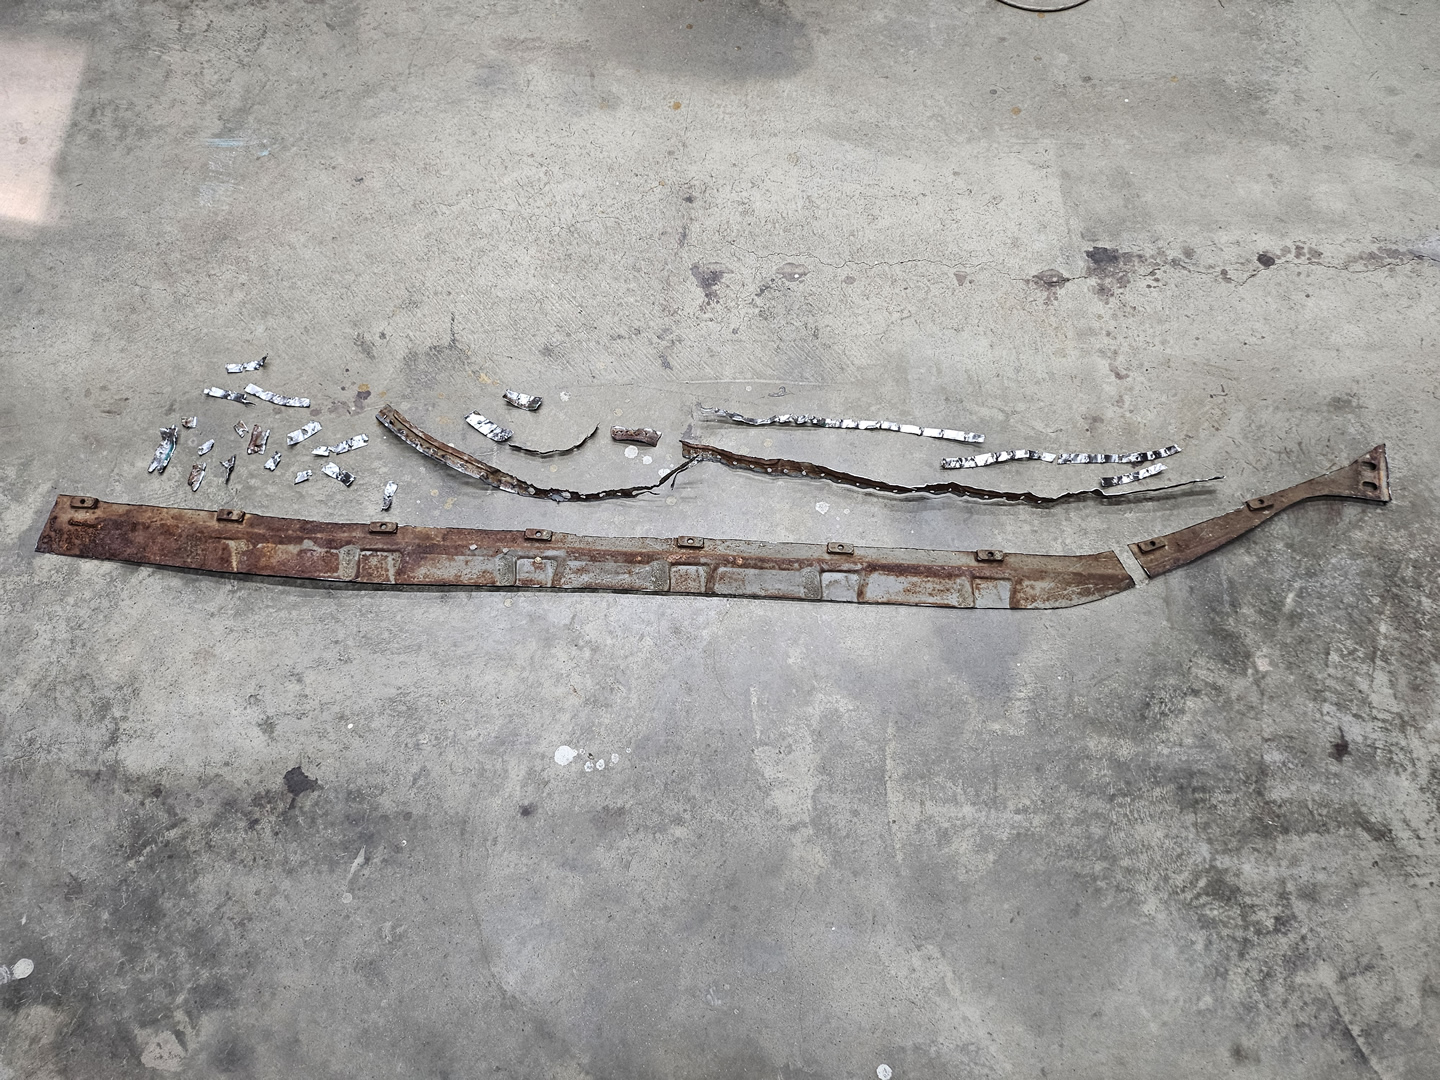
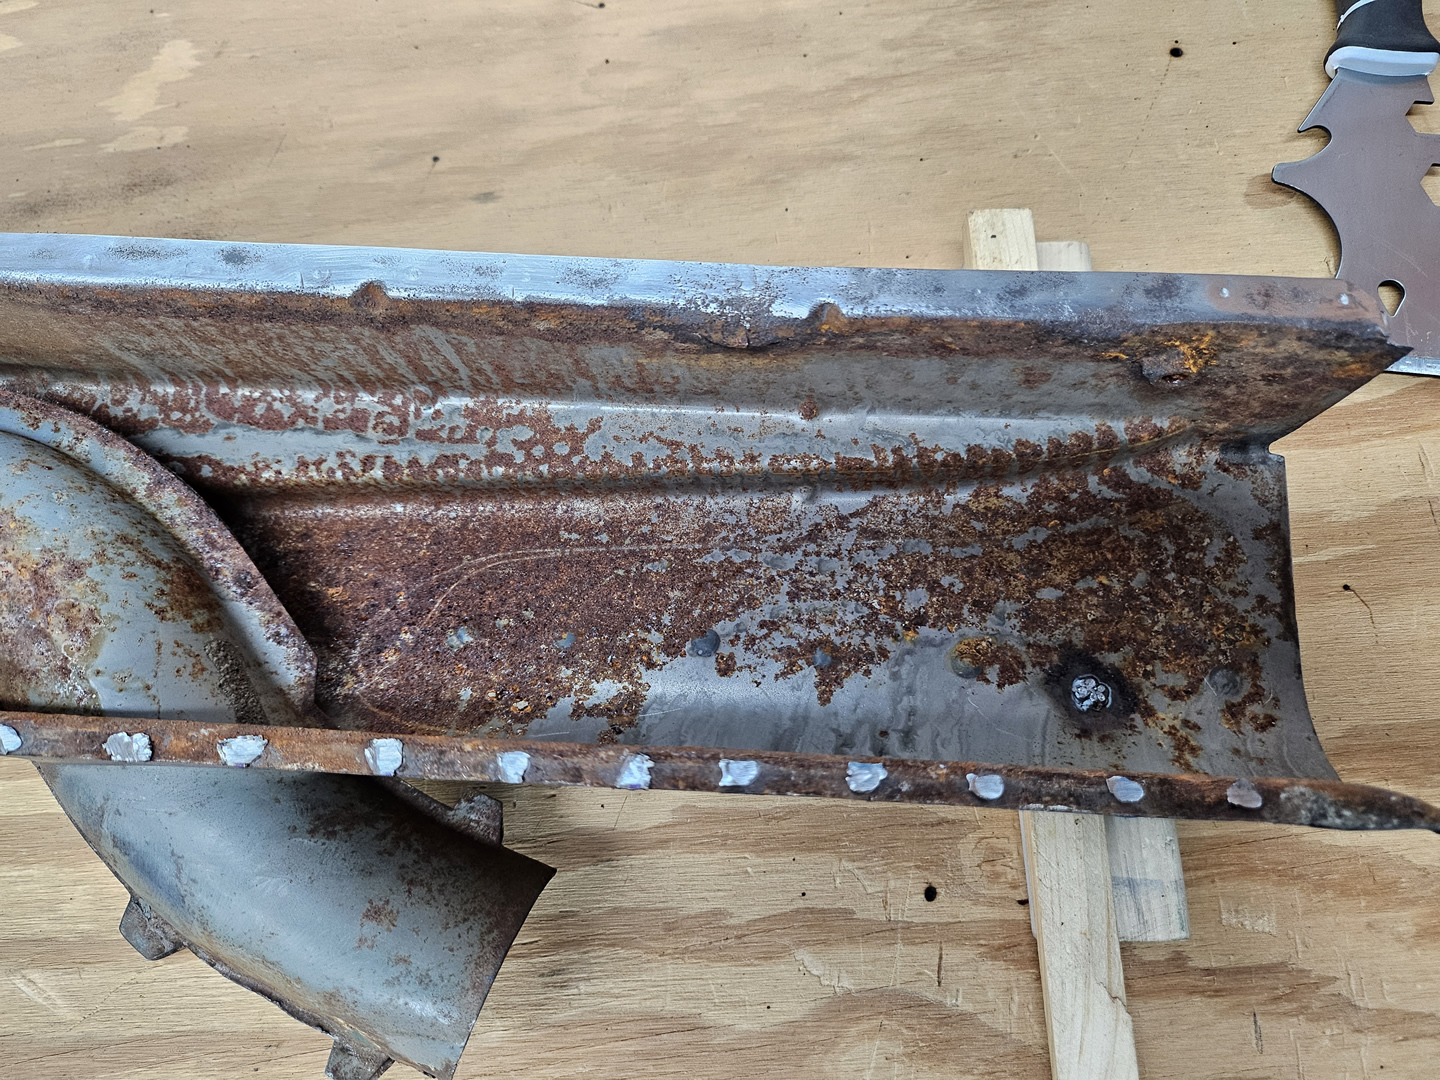
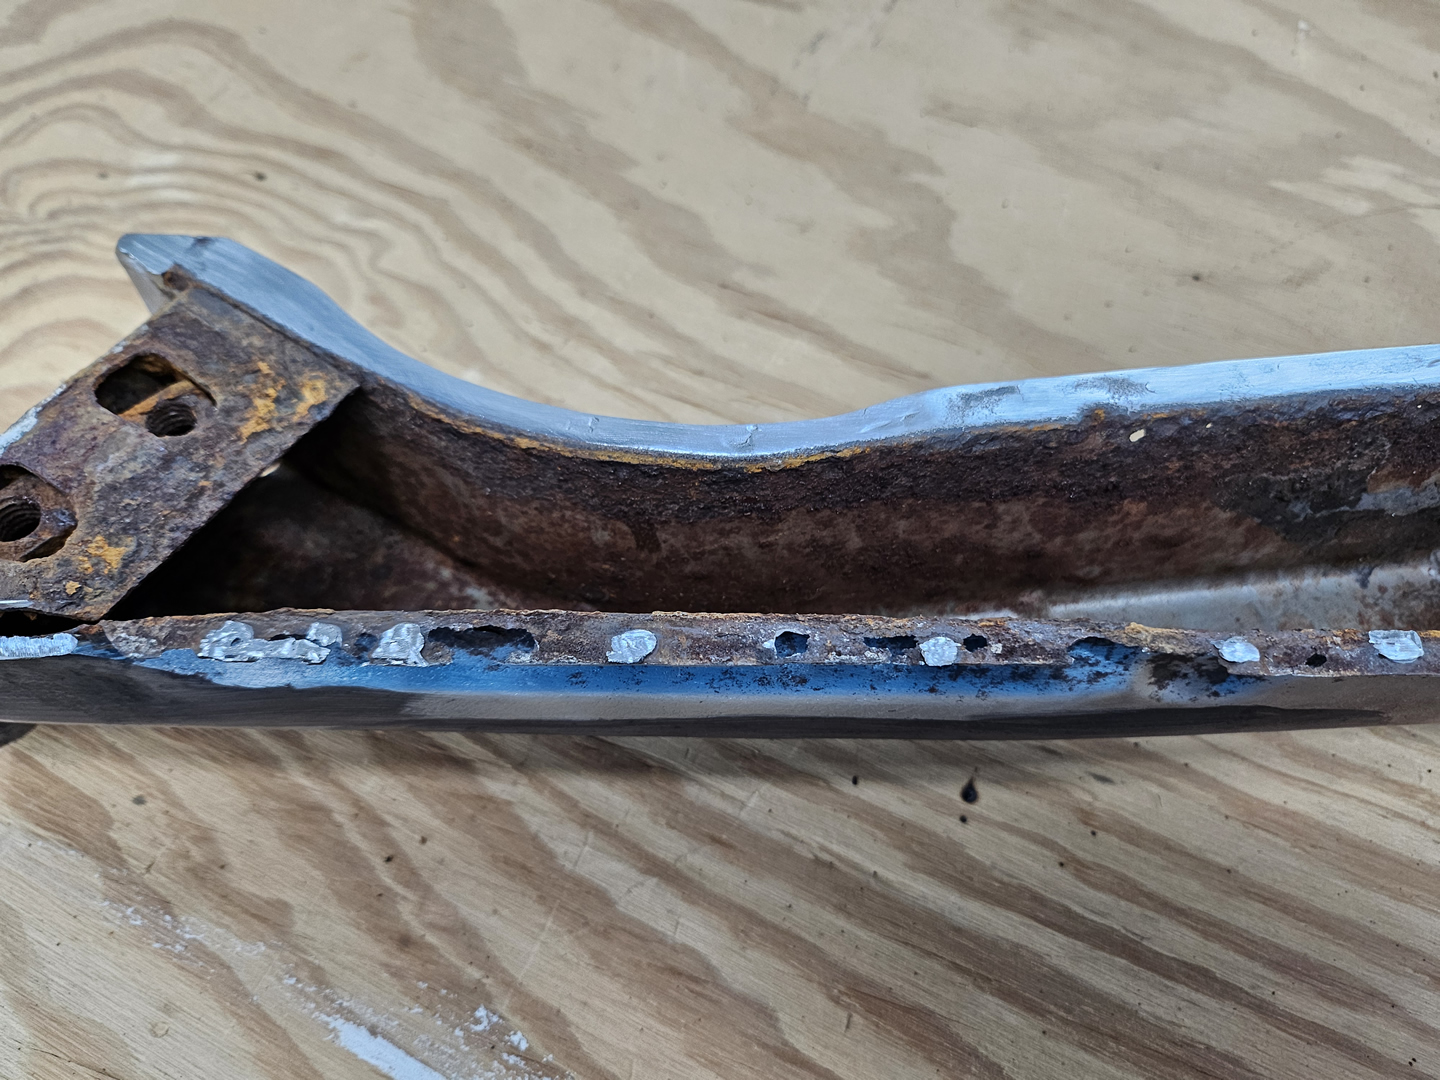
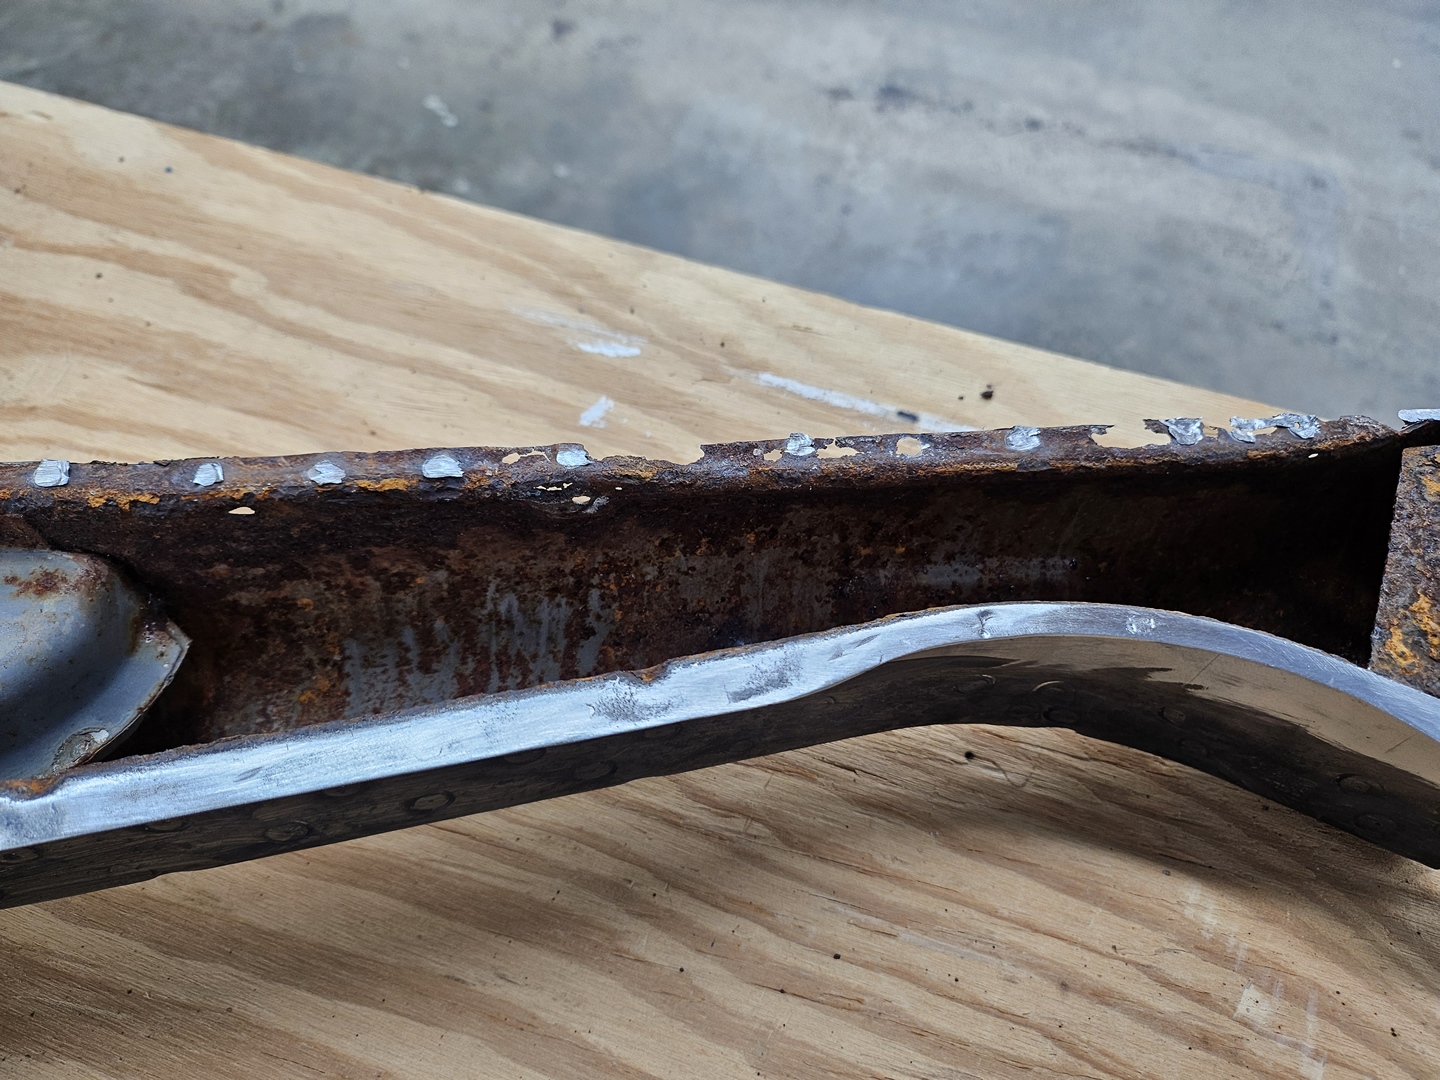
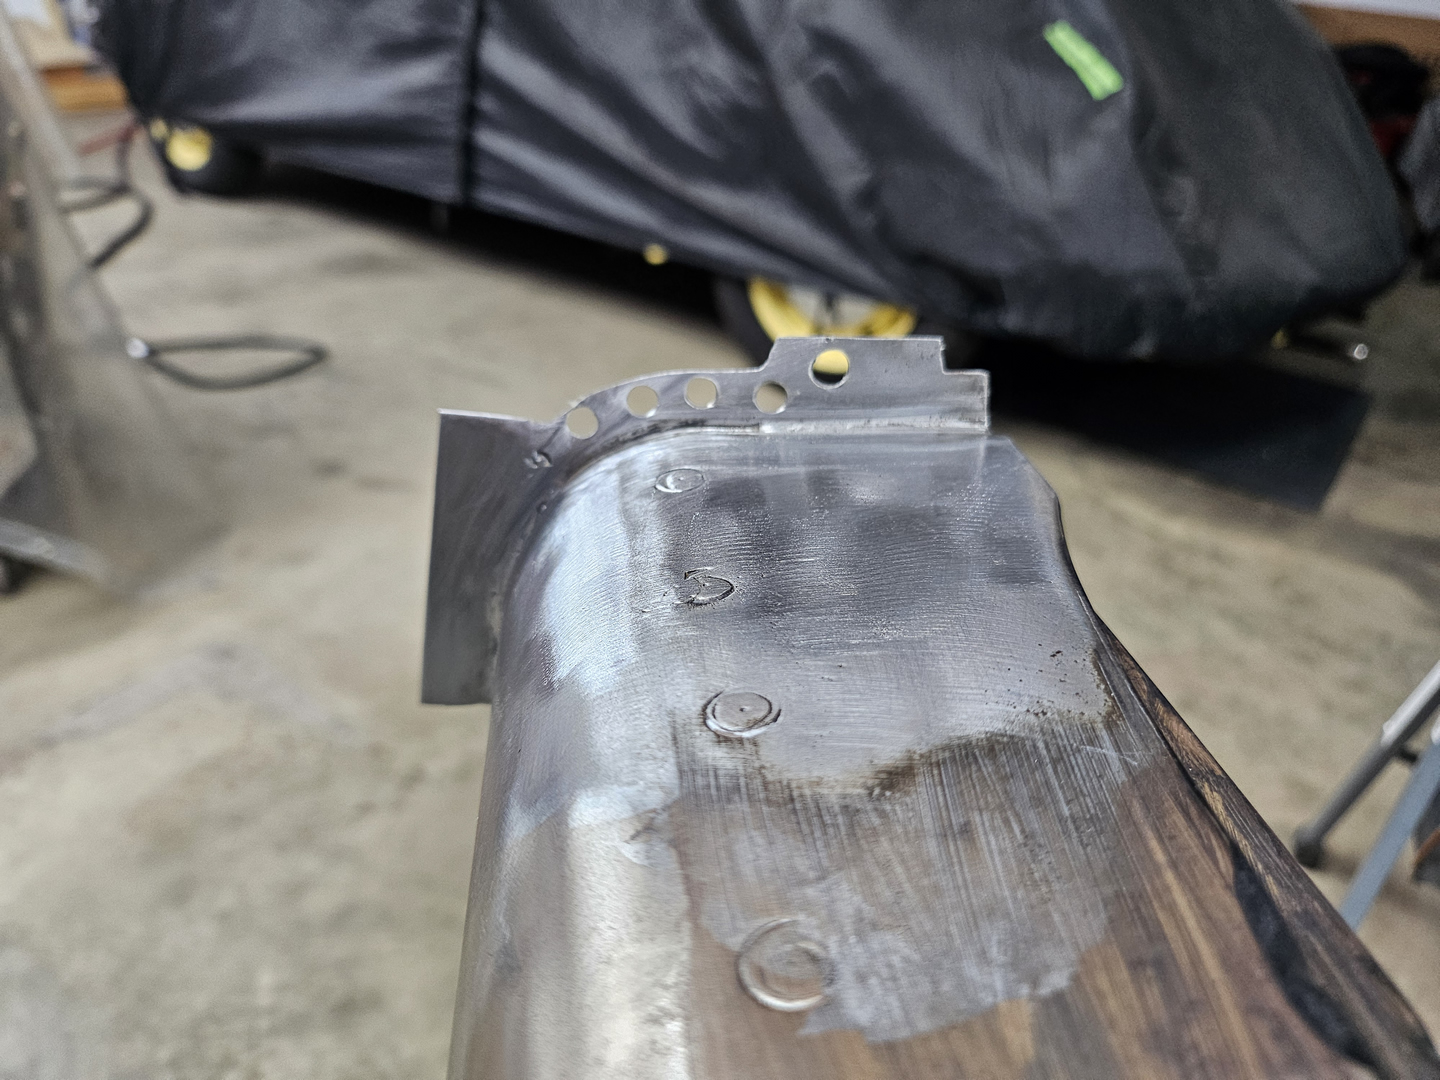
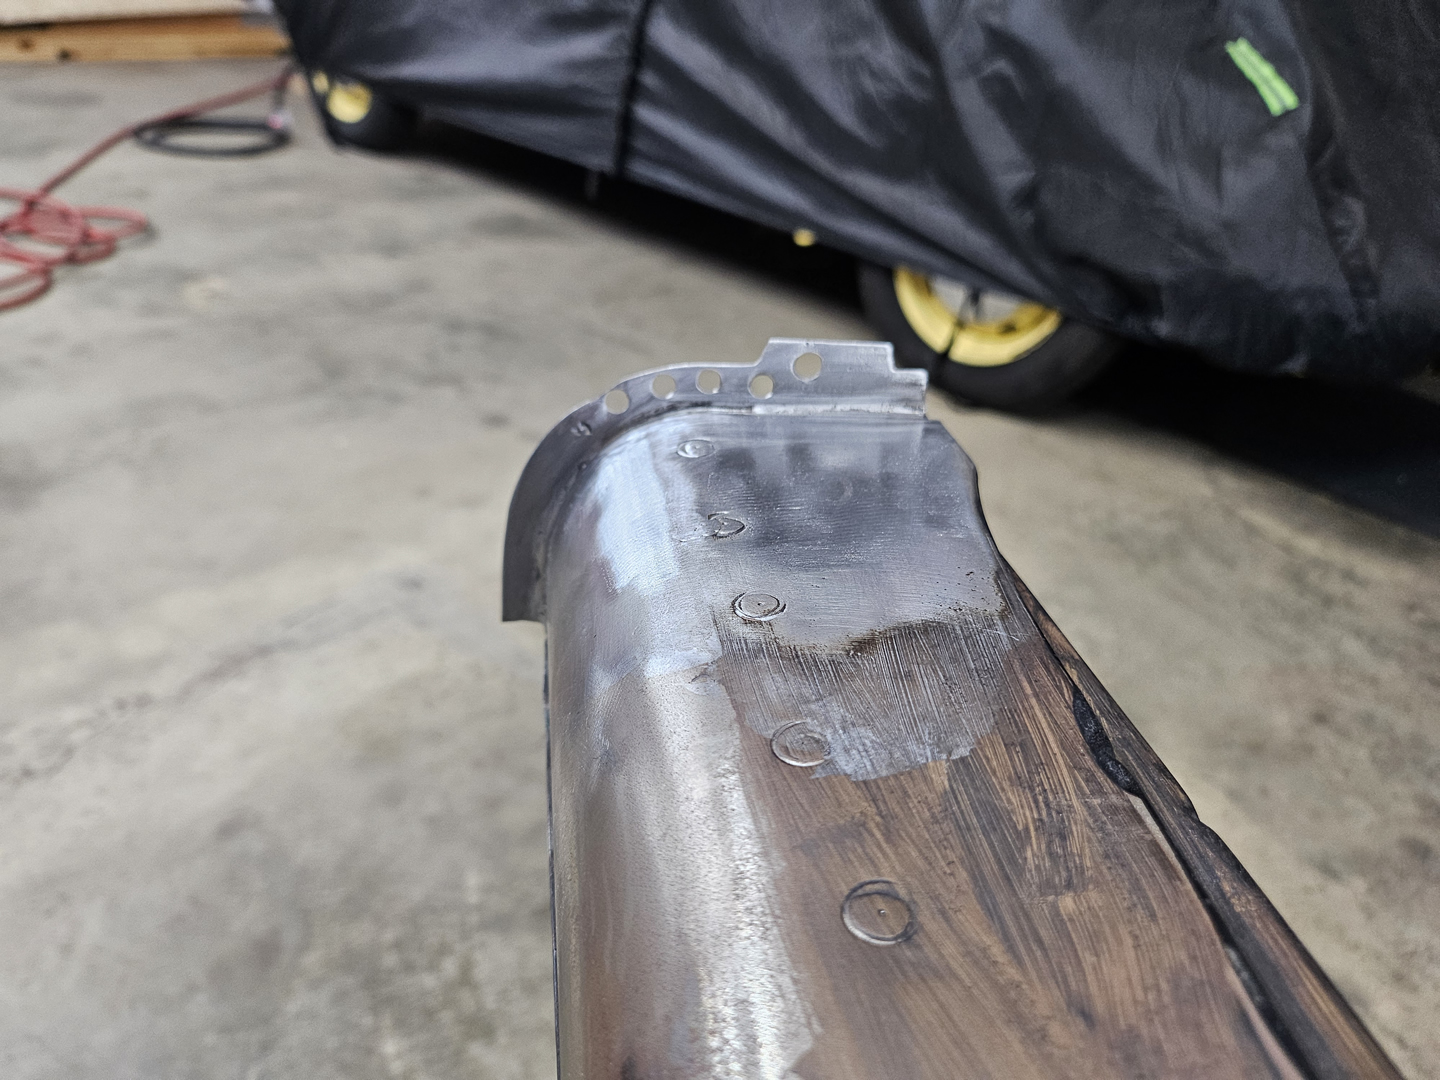
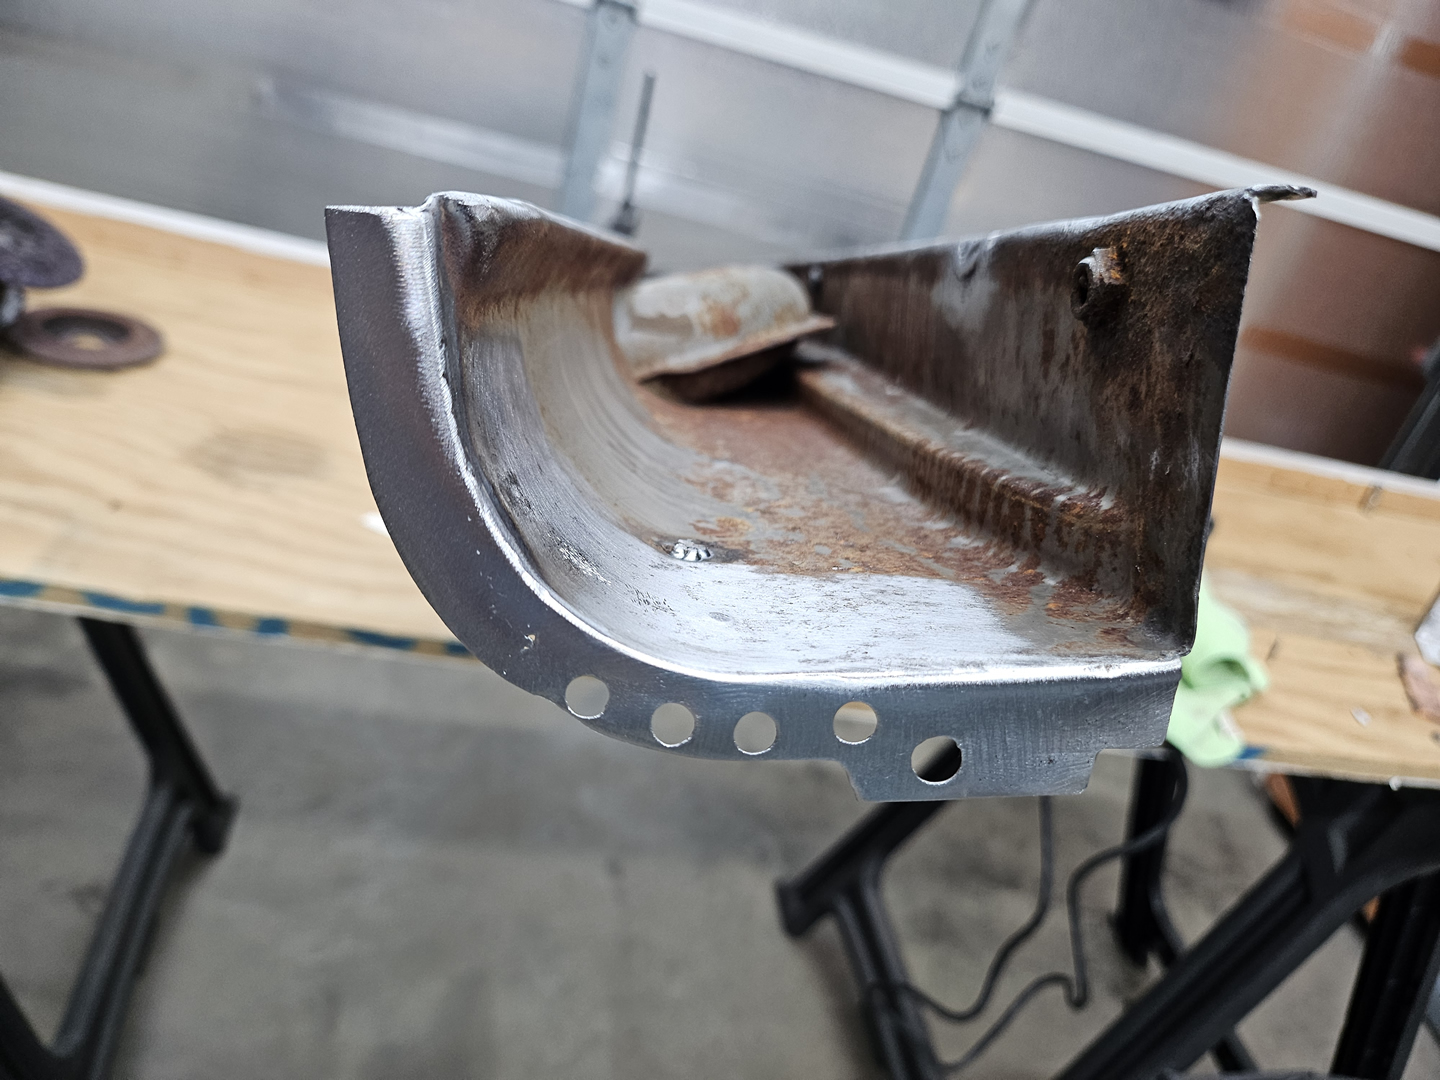
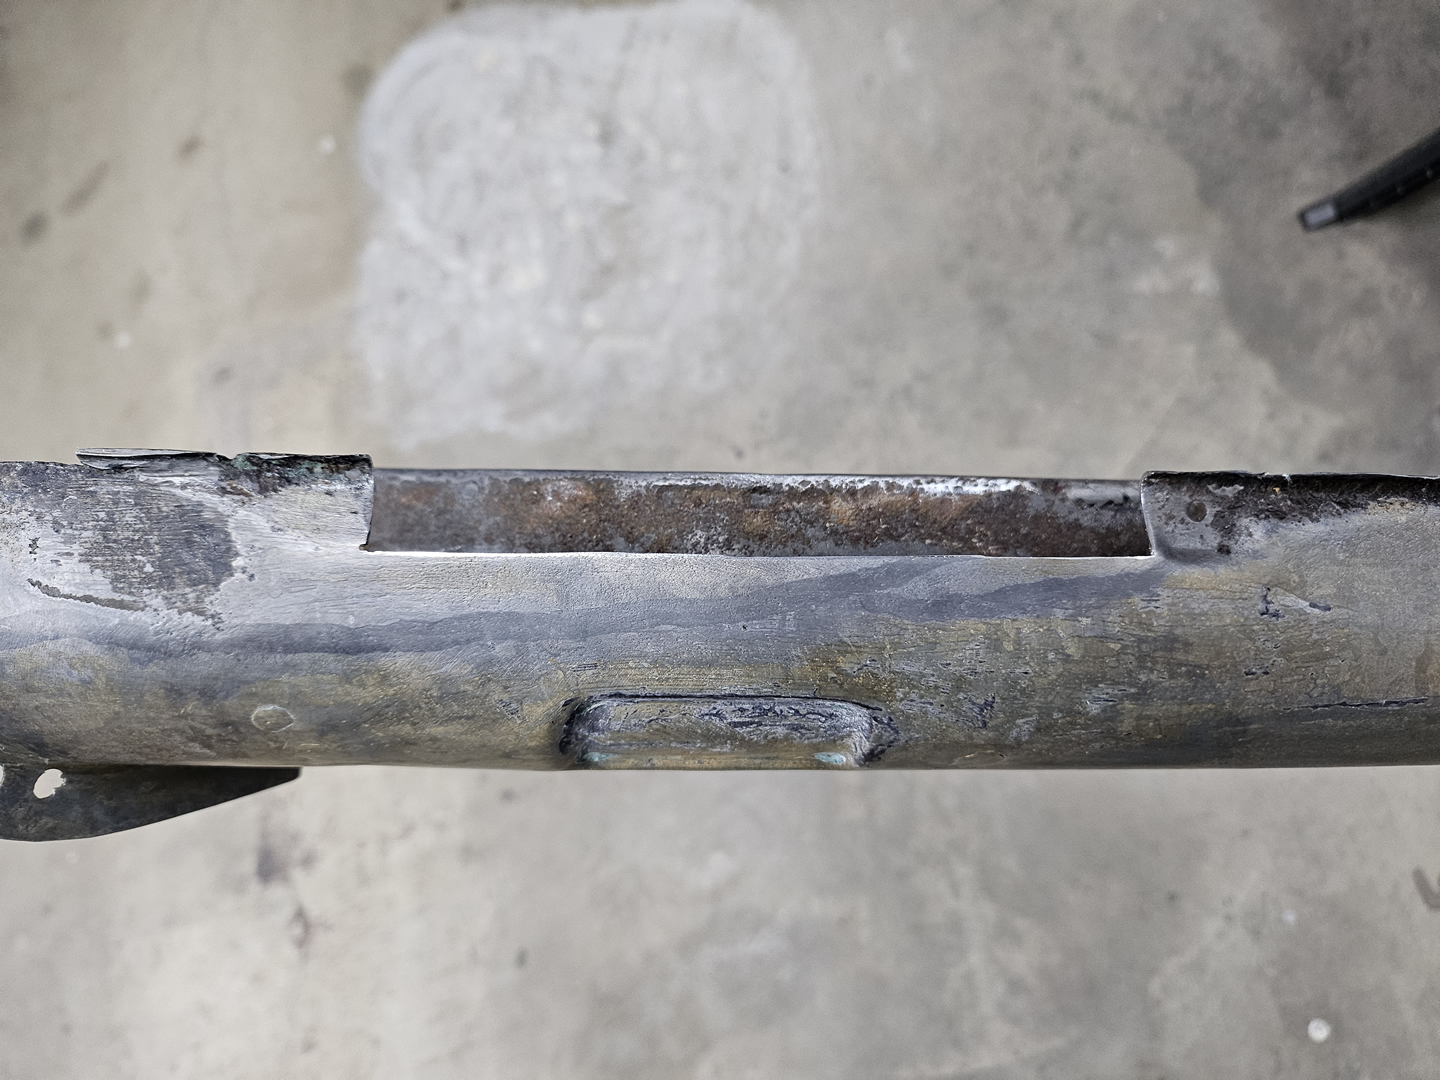
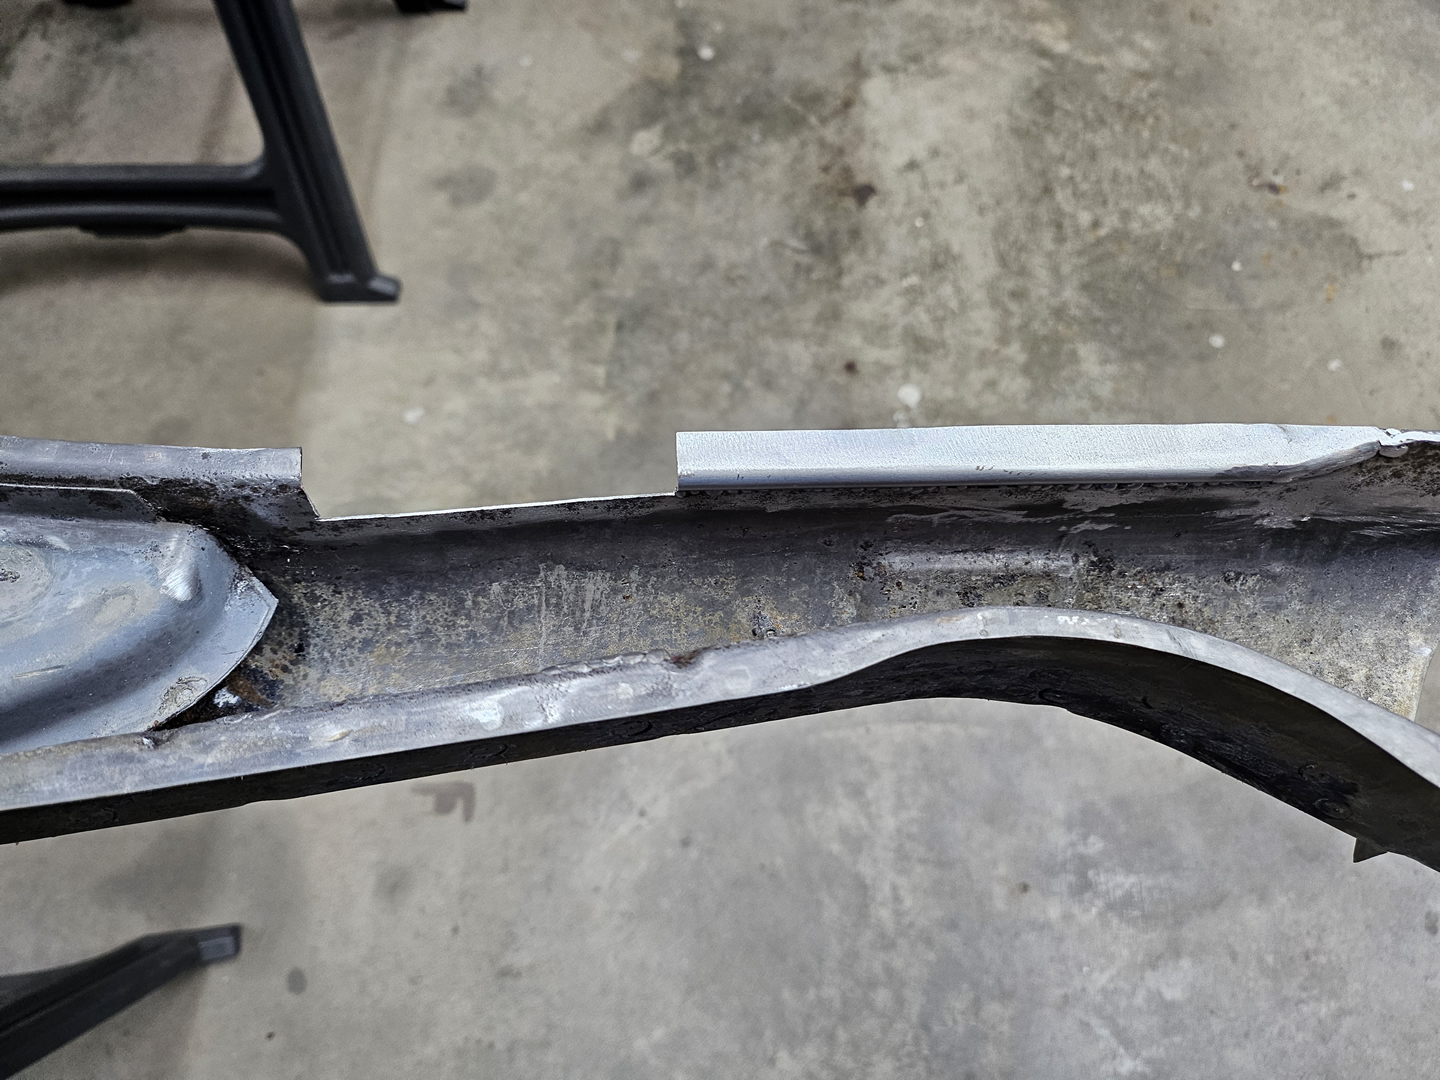
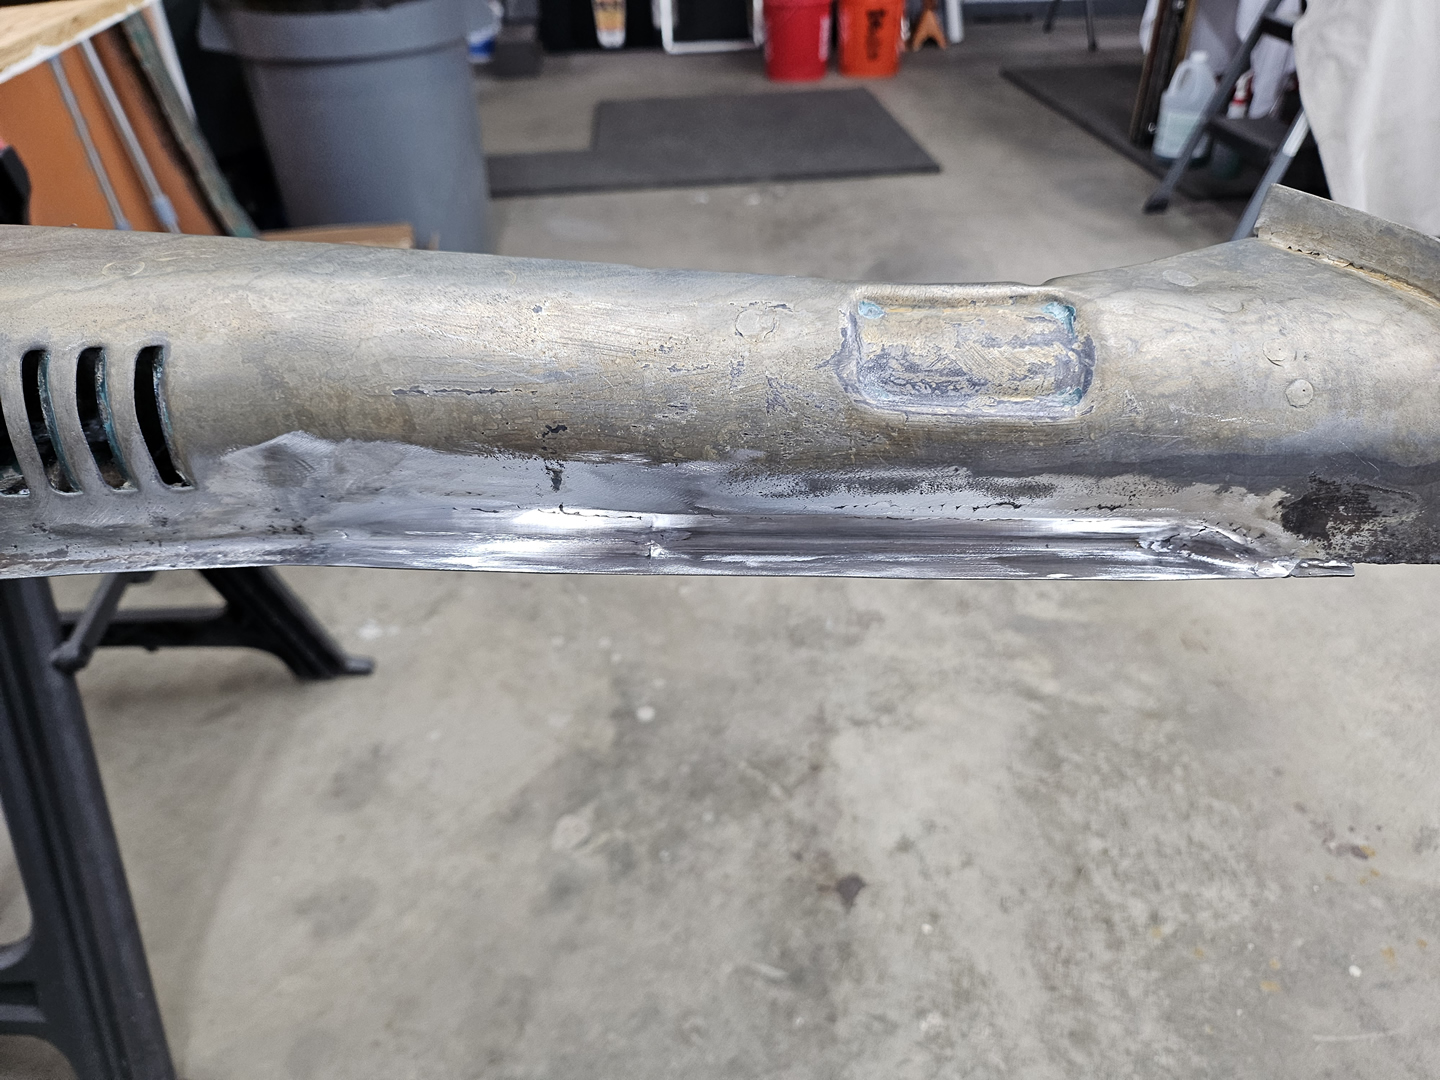
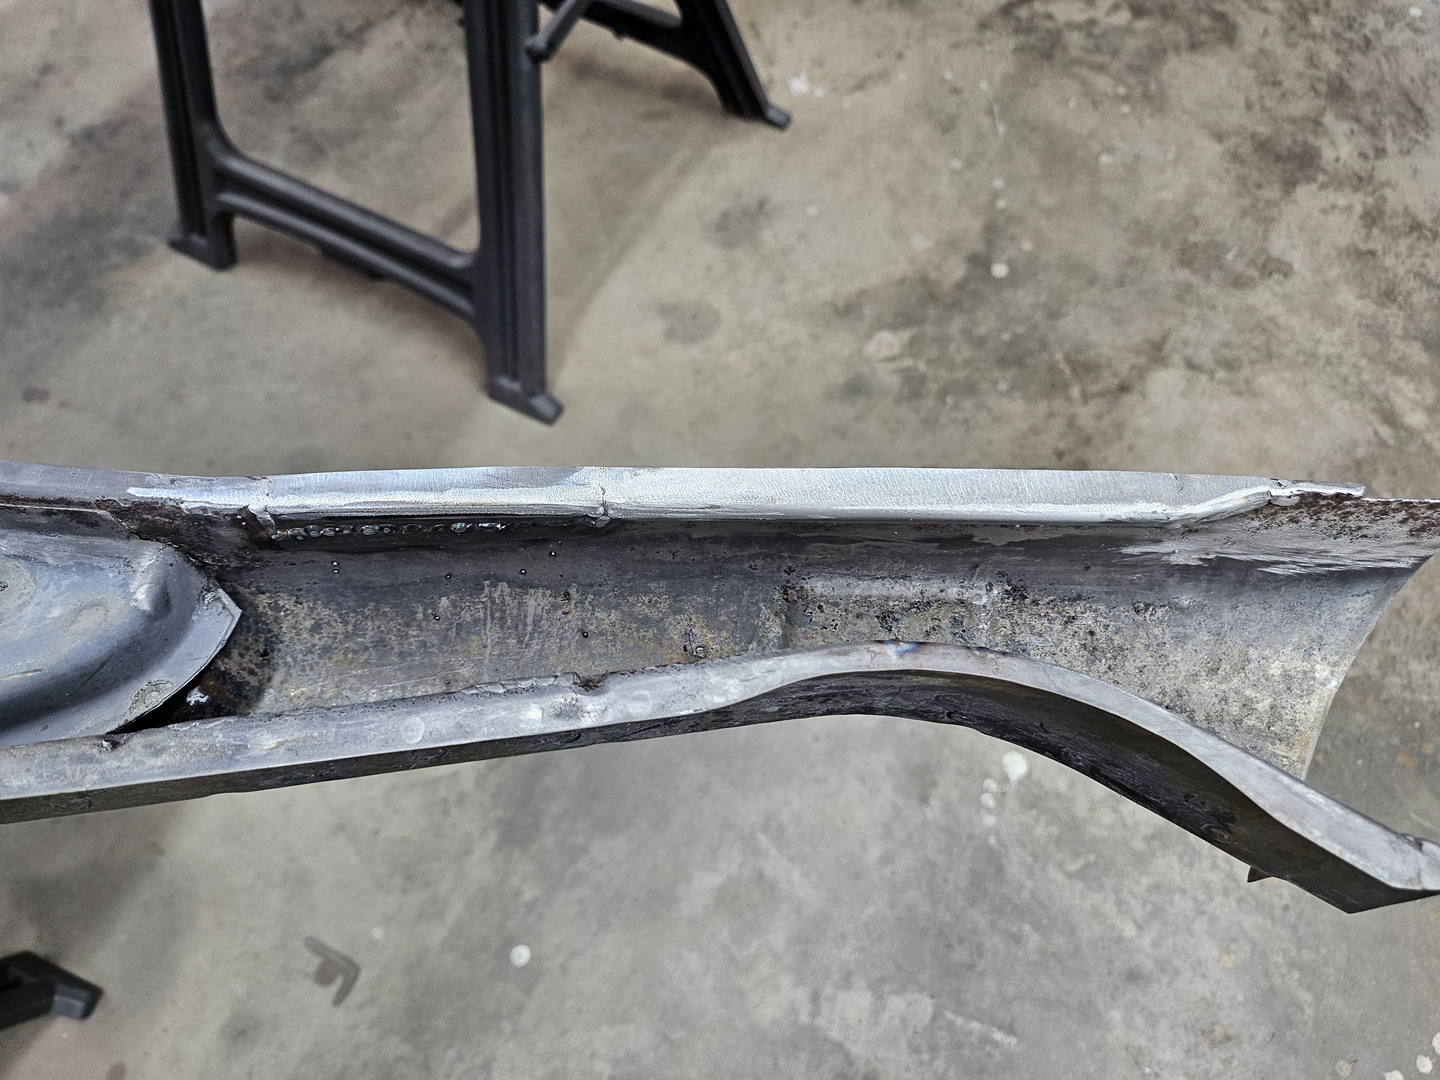
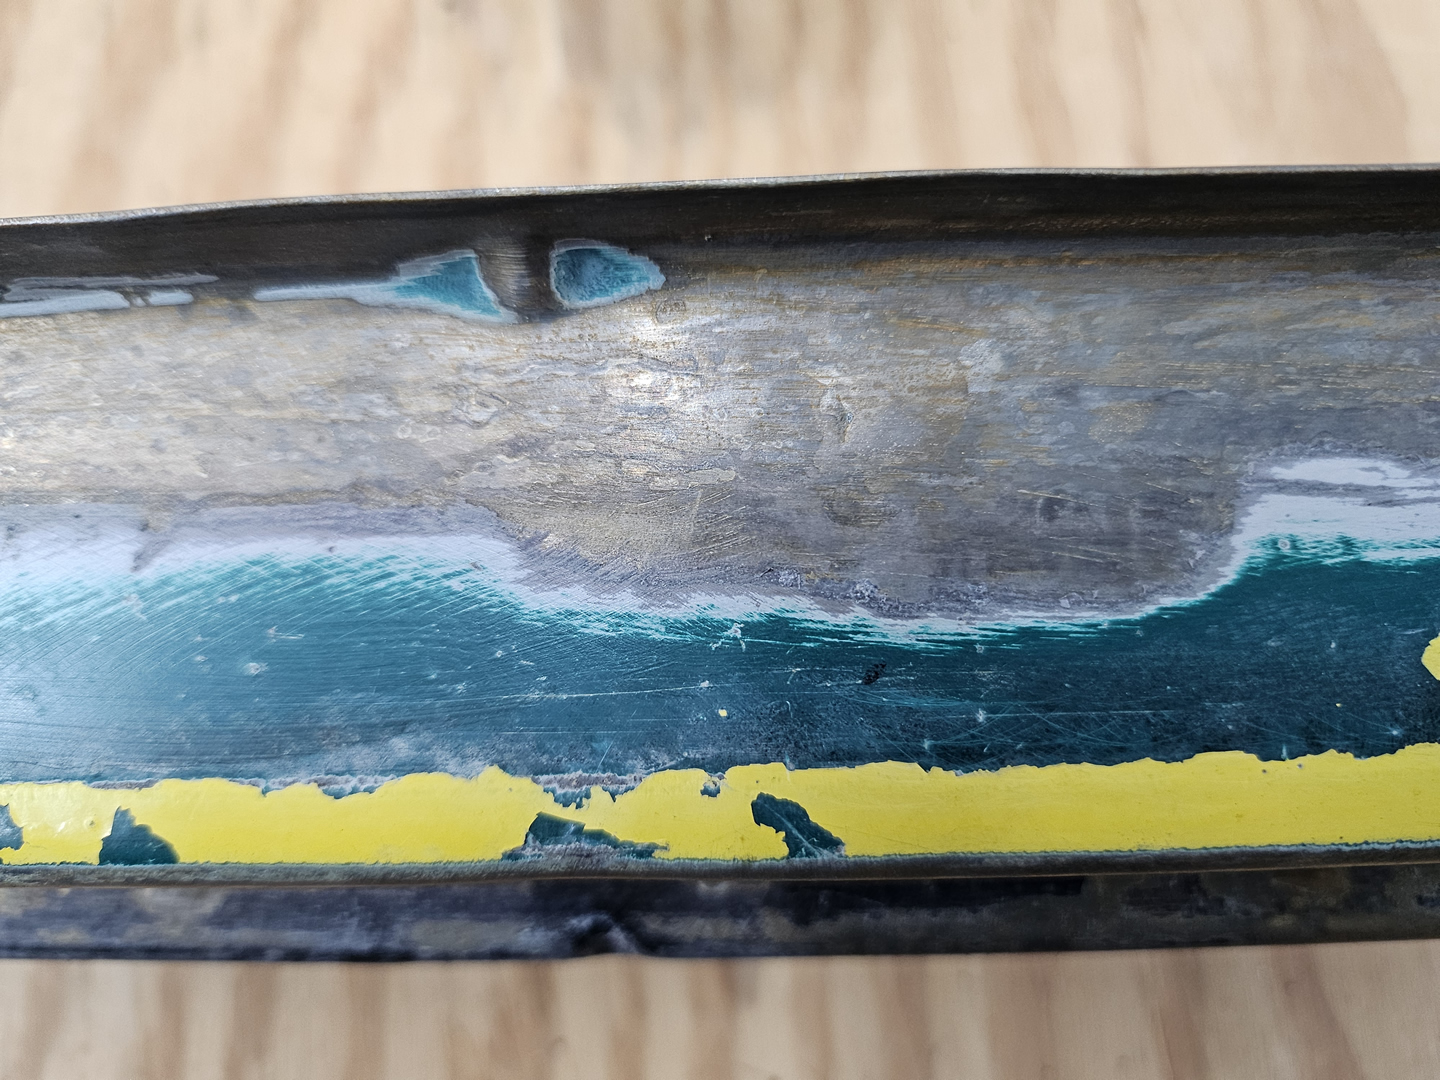
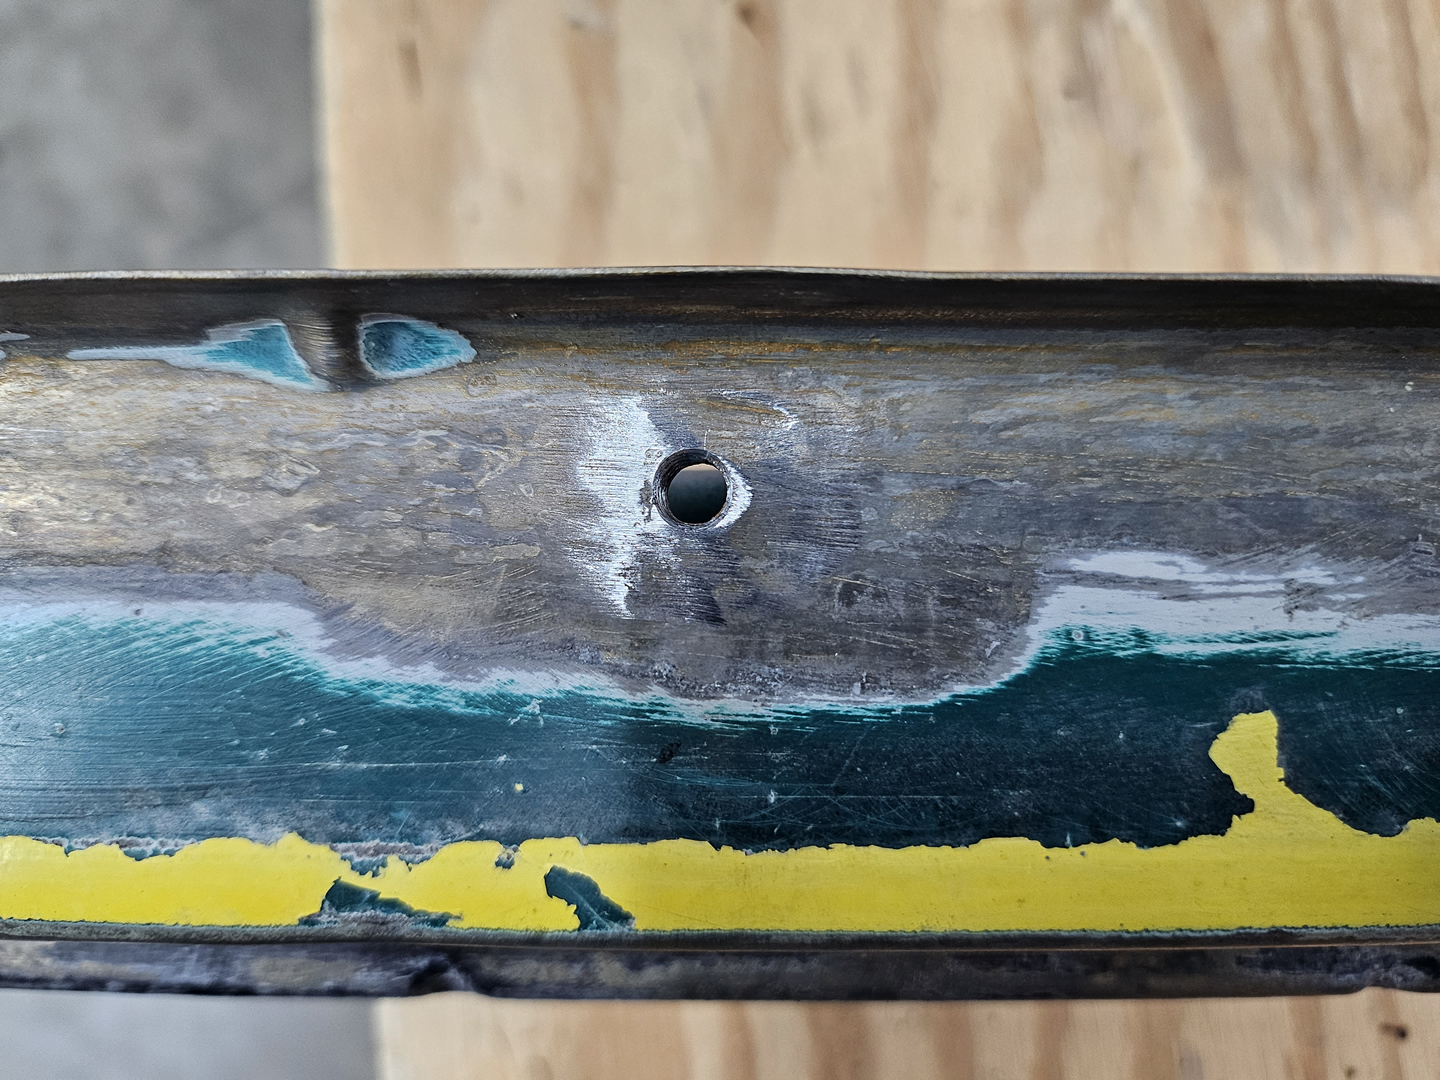
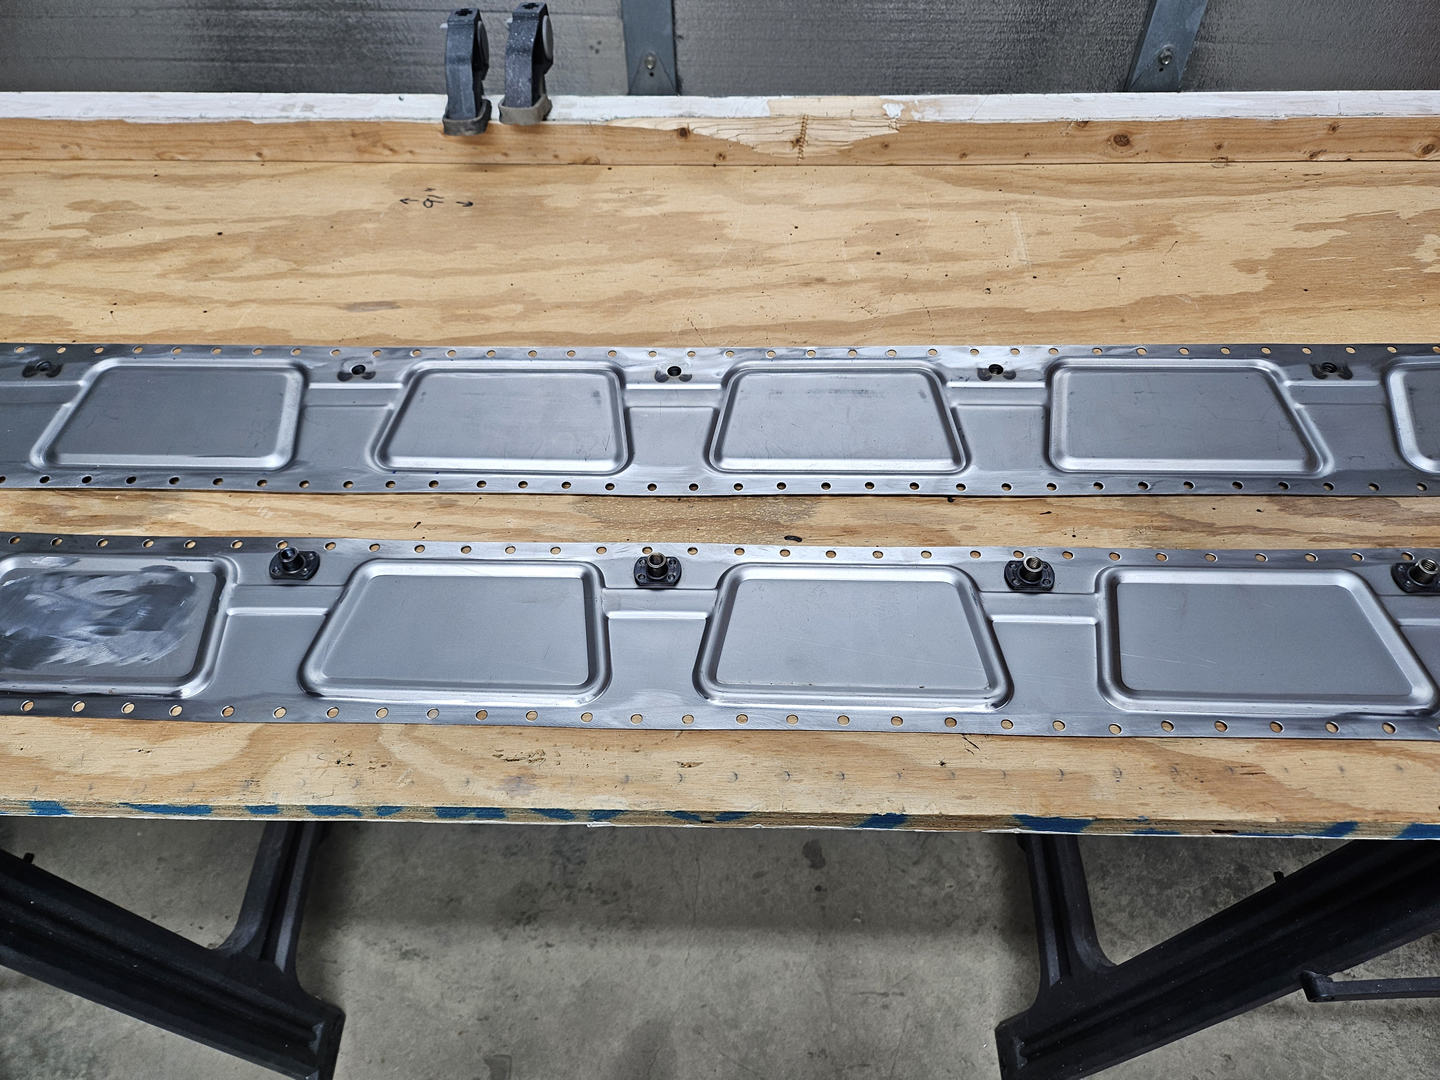
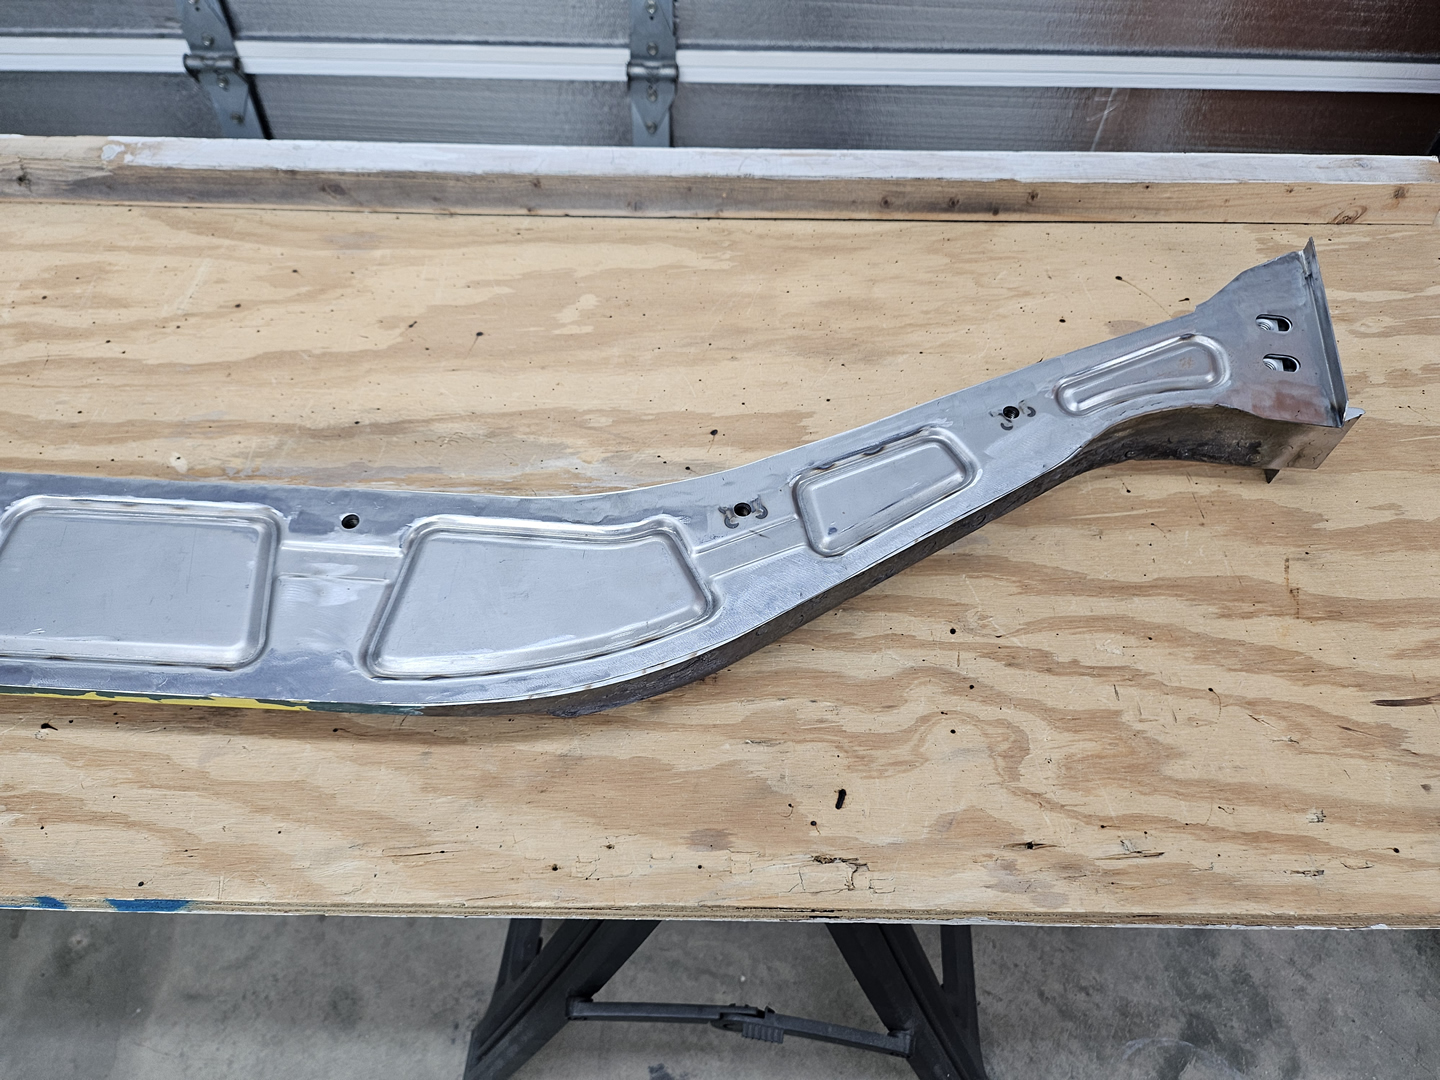
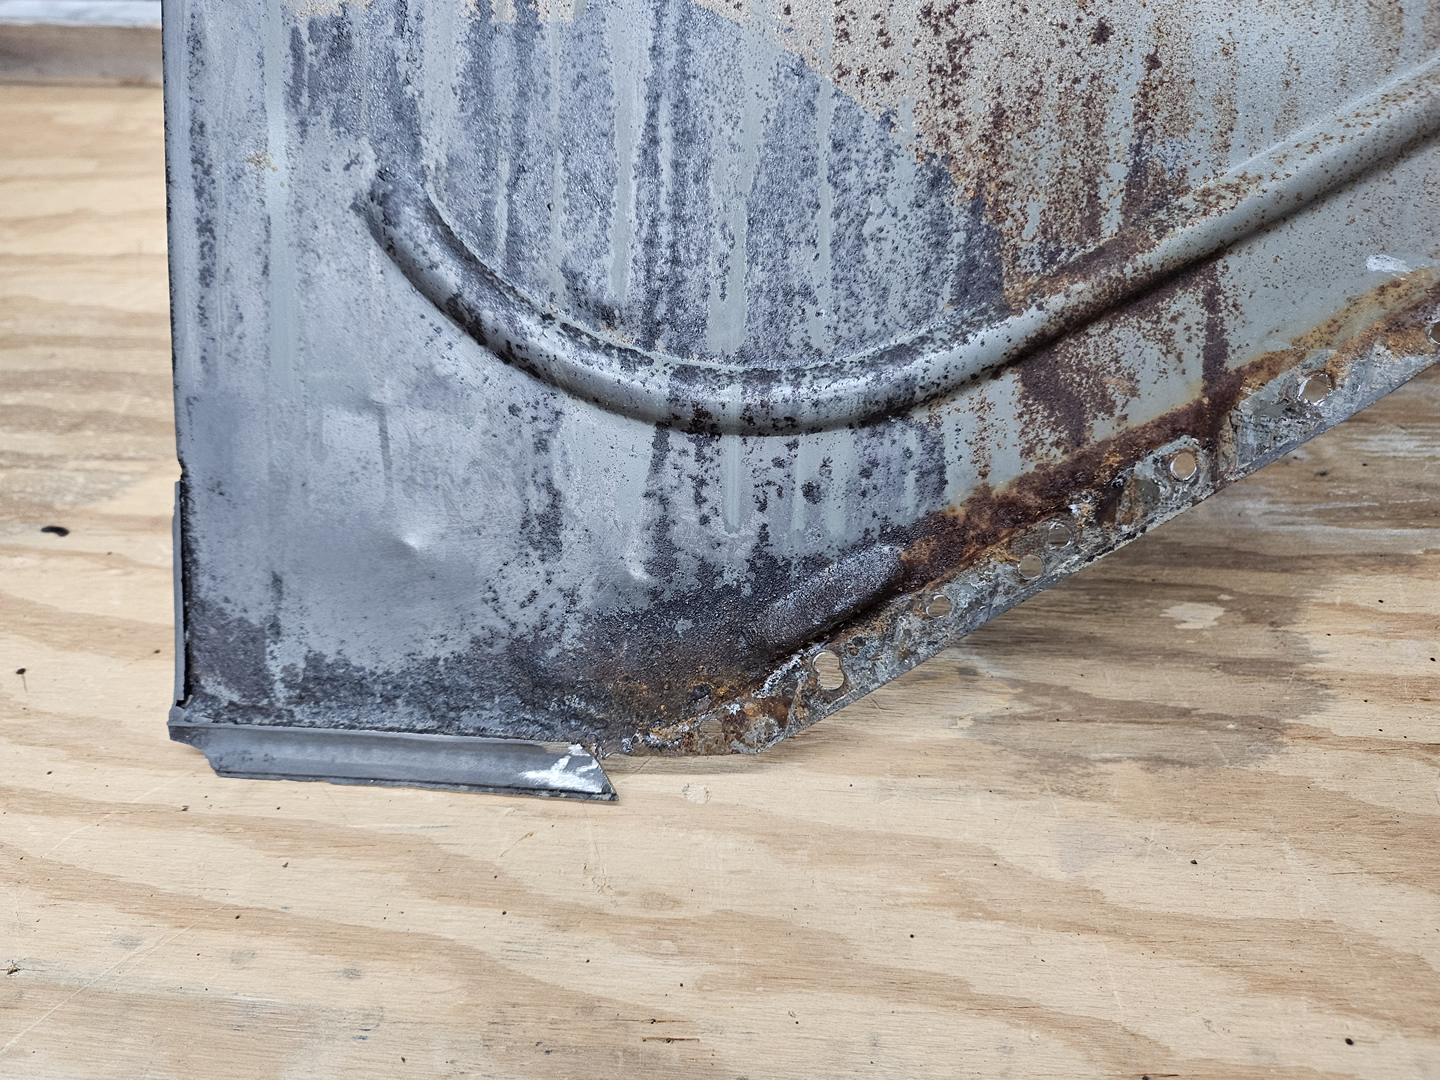
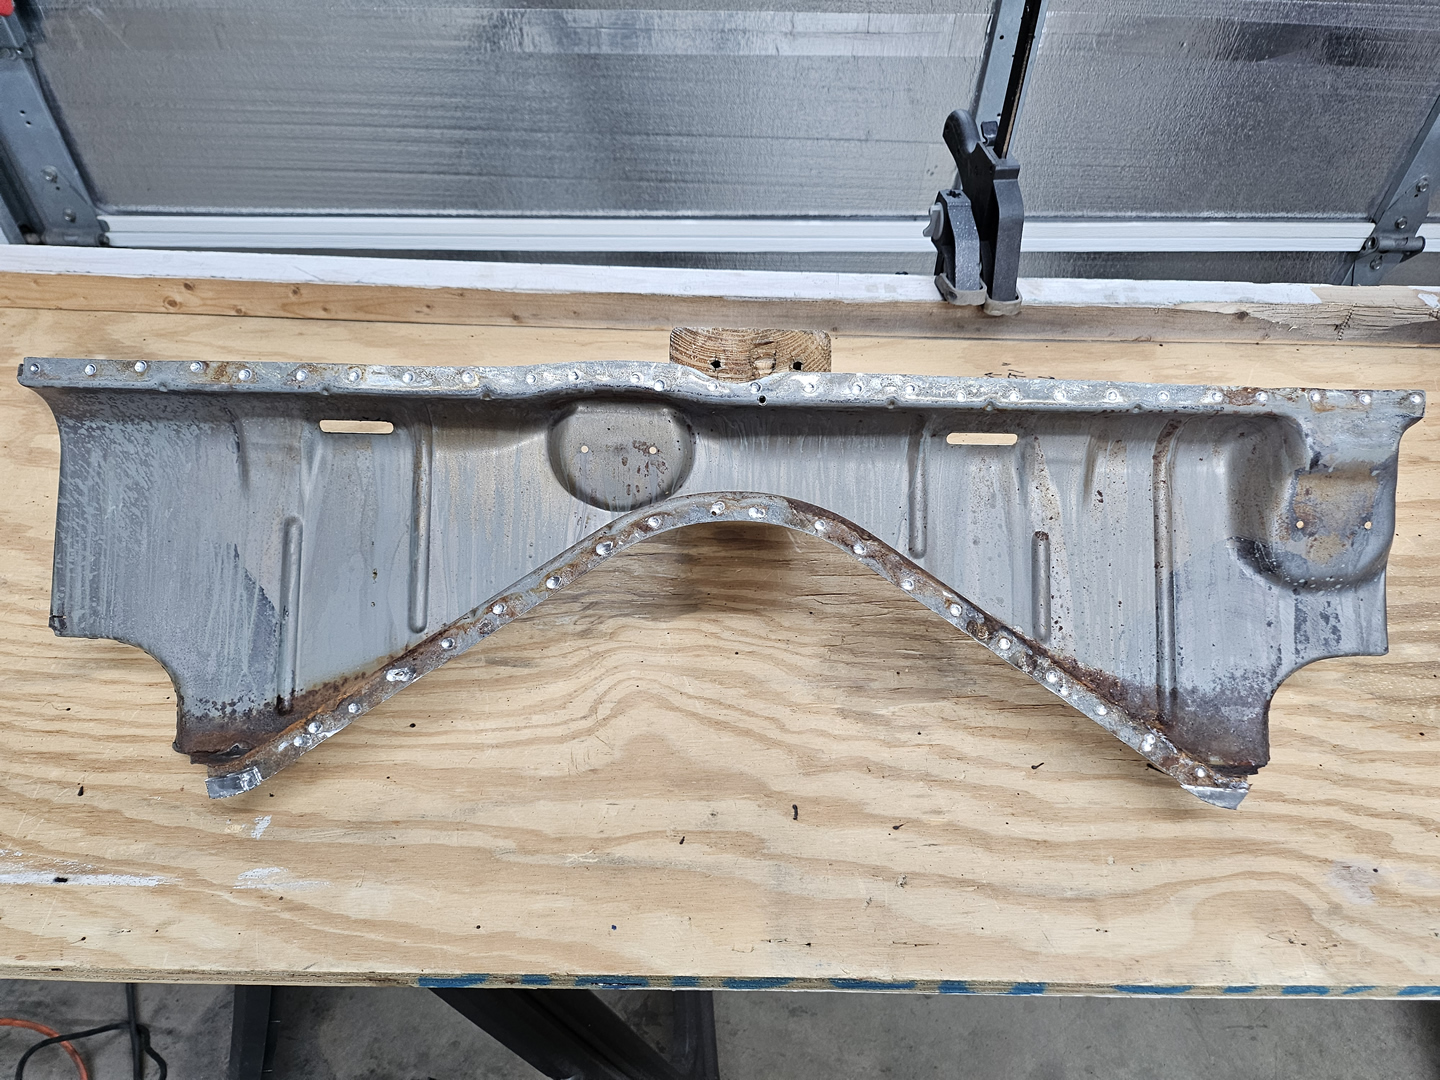
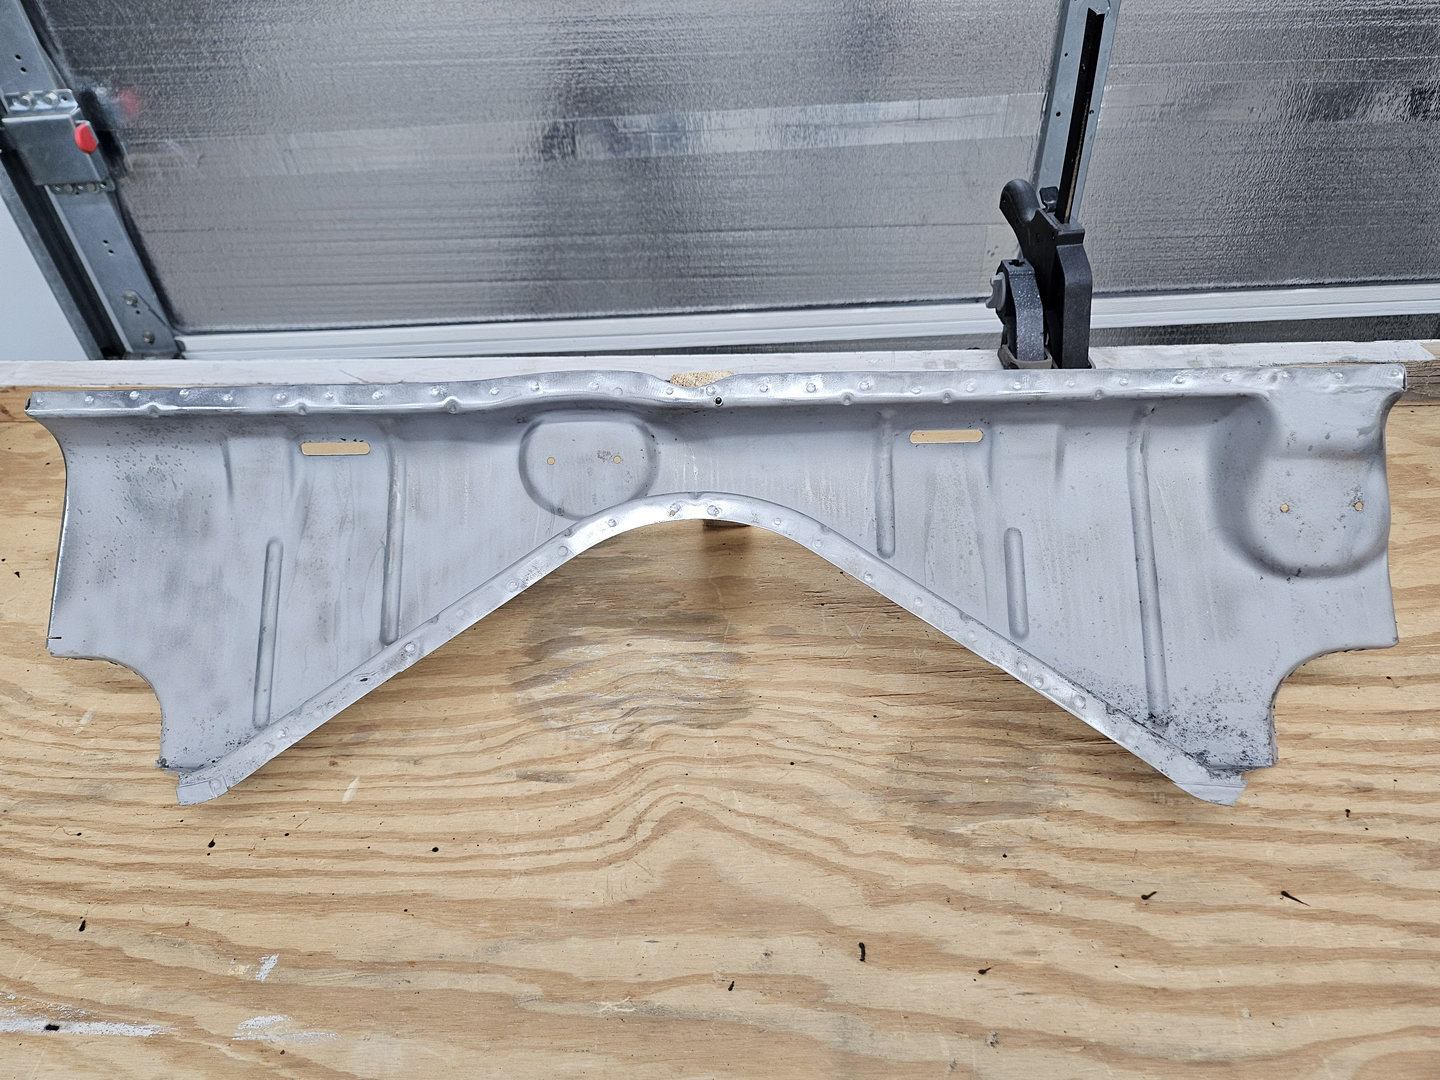
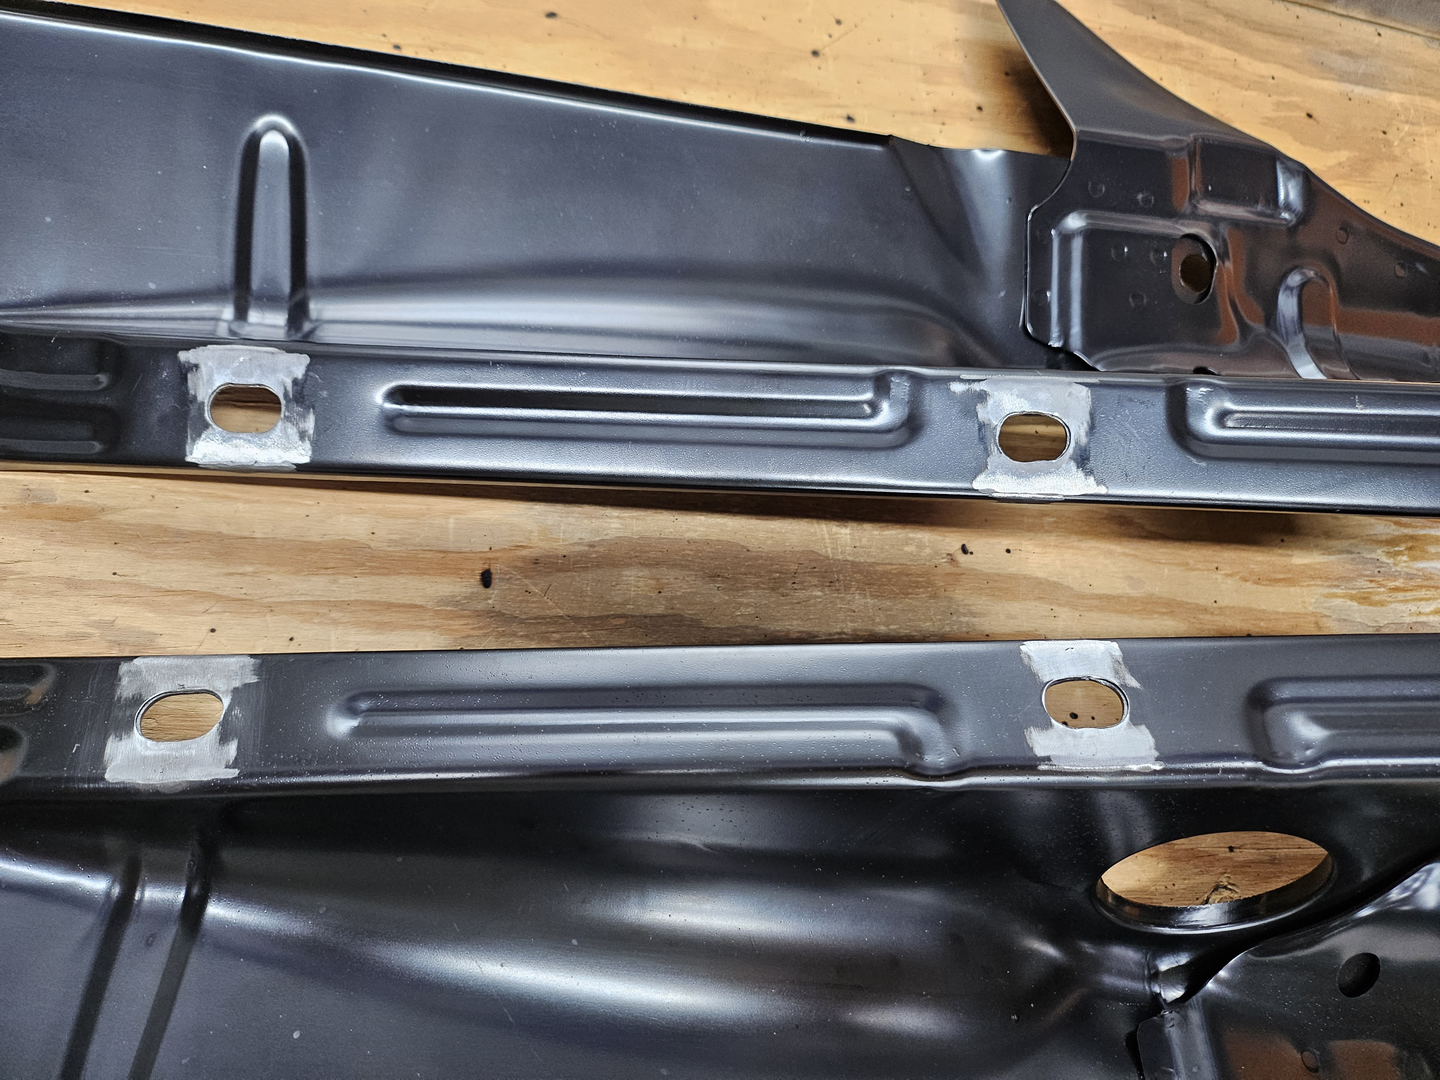
I started on the passenger side heater channel first. It is in the best condition of the two. I first went through and welded up any holes or deep cuts from the spot weld cutters I used when I was removing the remnants of other panels. I then started removing the bottom plate. This is not an easy job. There are around 100 spot welds on each side of the bottom plate. I found that the best way to remove the plate was to grind down into the spot welds, cut the bottom plate on each side about 3/4" from the edge, and then peel off the strip that was left of the plate. This took many hours to do both sides. I took my time and tried to be very careful not to damage the metal underneath the strips. Once all of the plate had been removed, I then ground off the pieces remaining of the spot welds and cleaned up the flanges on both sides. I was pleased to discover that there wasn't a lot of rust on the inside of the channel.
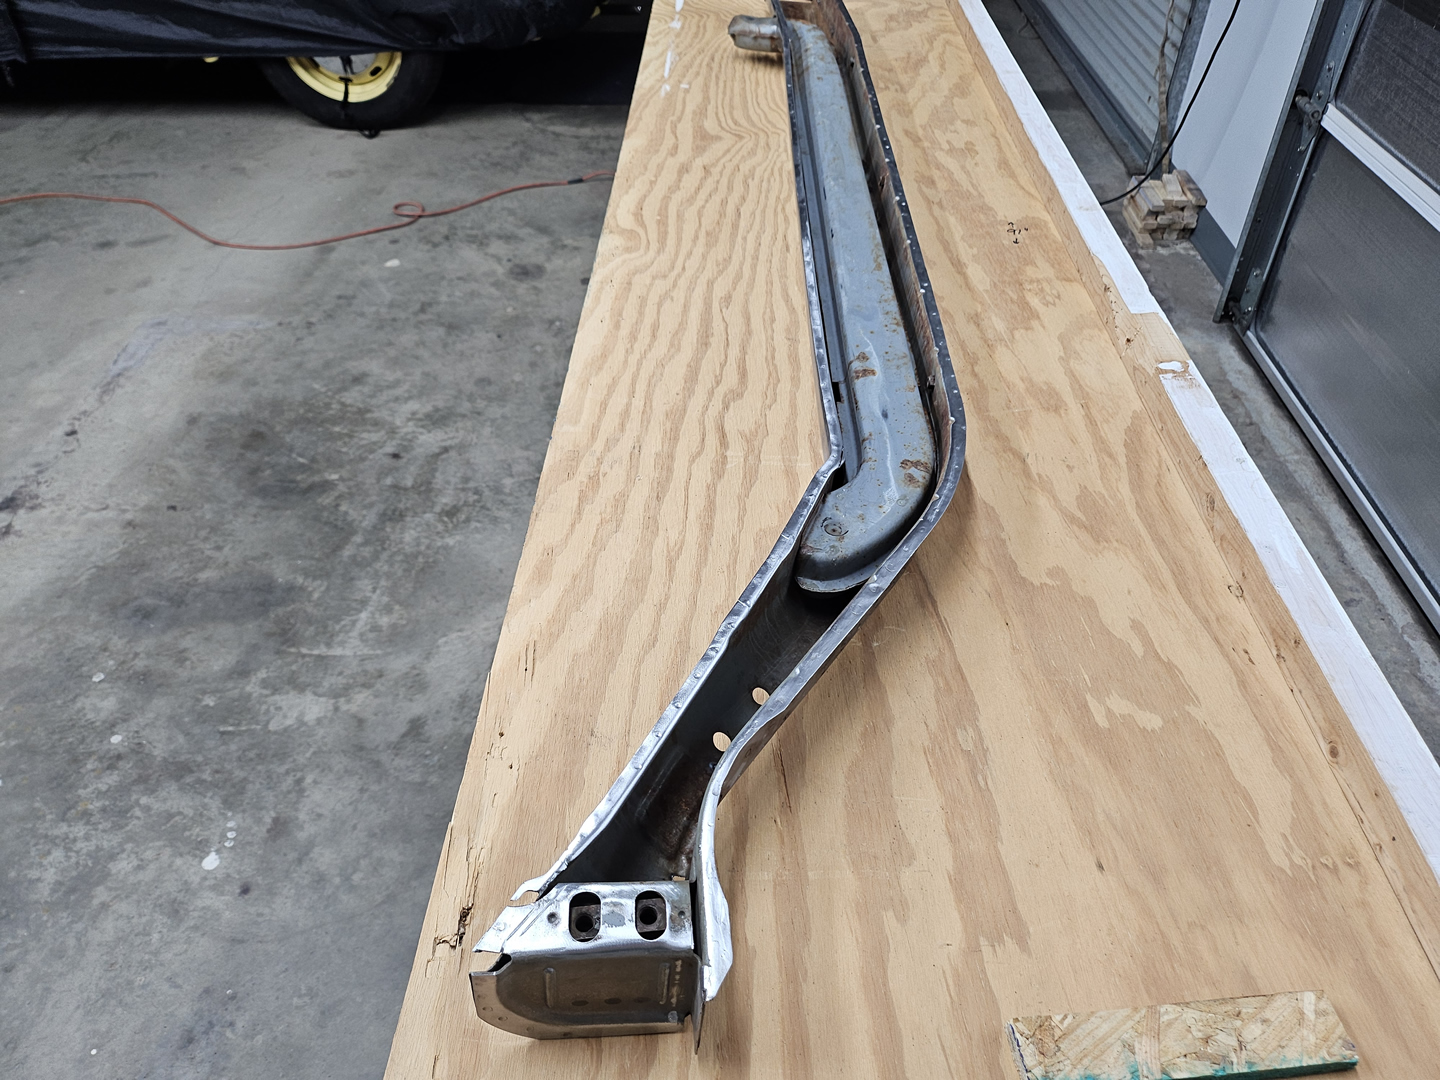
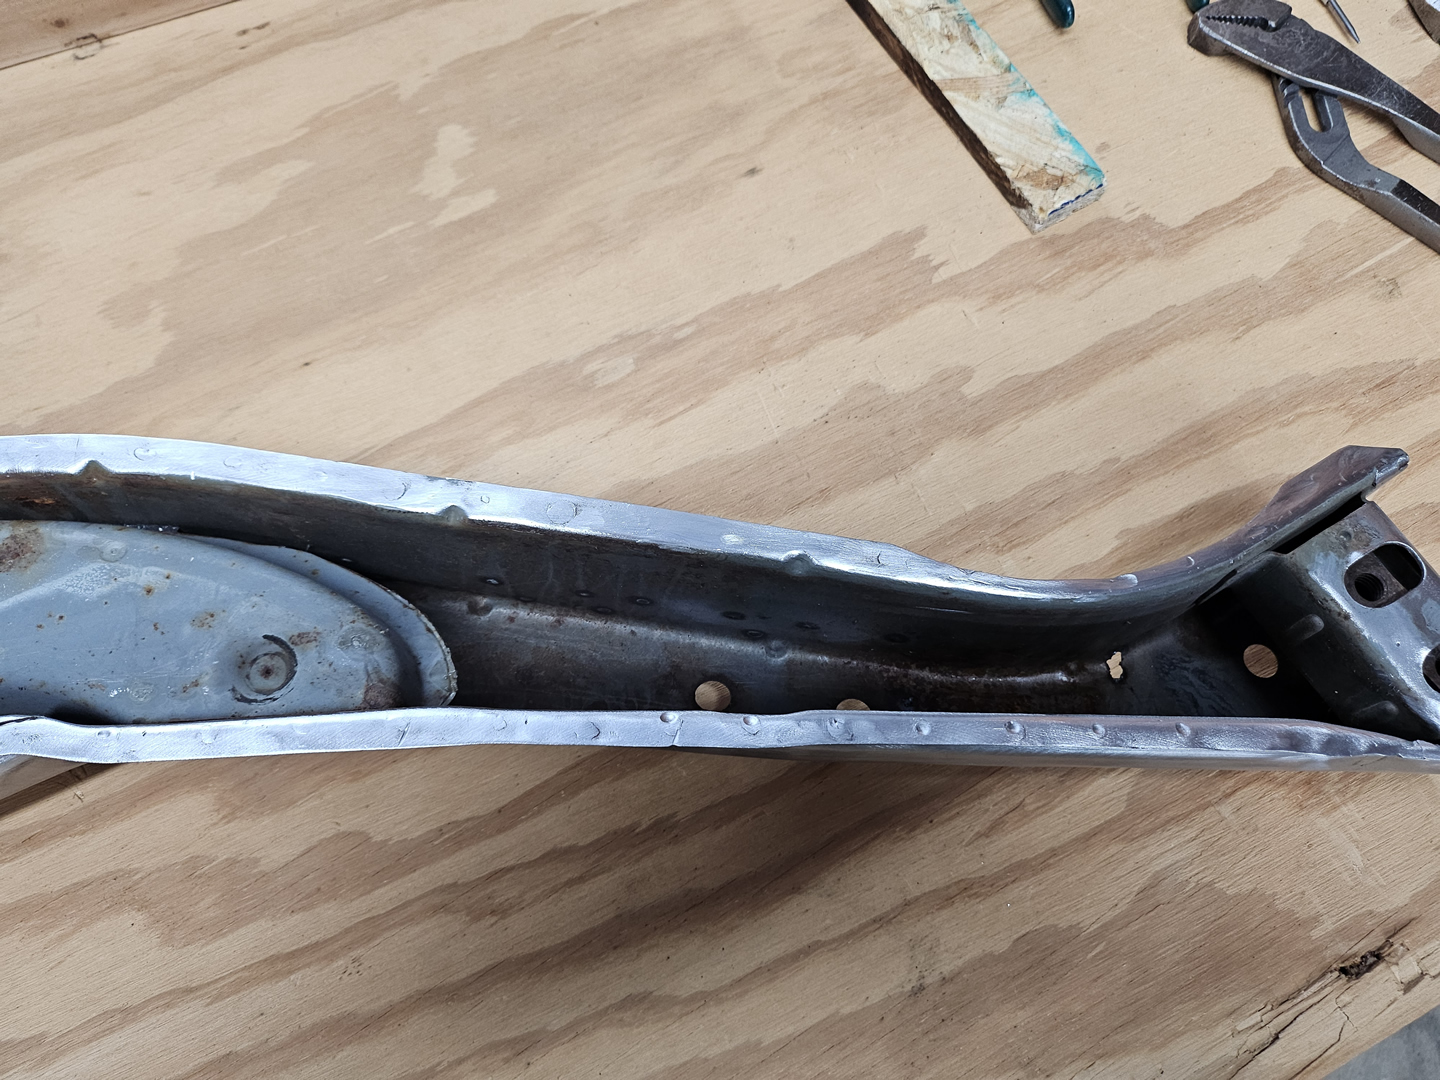
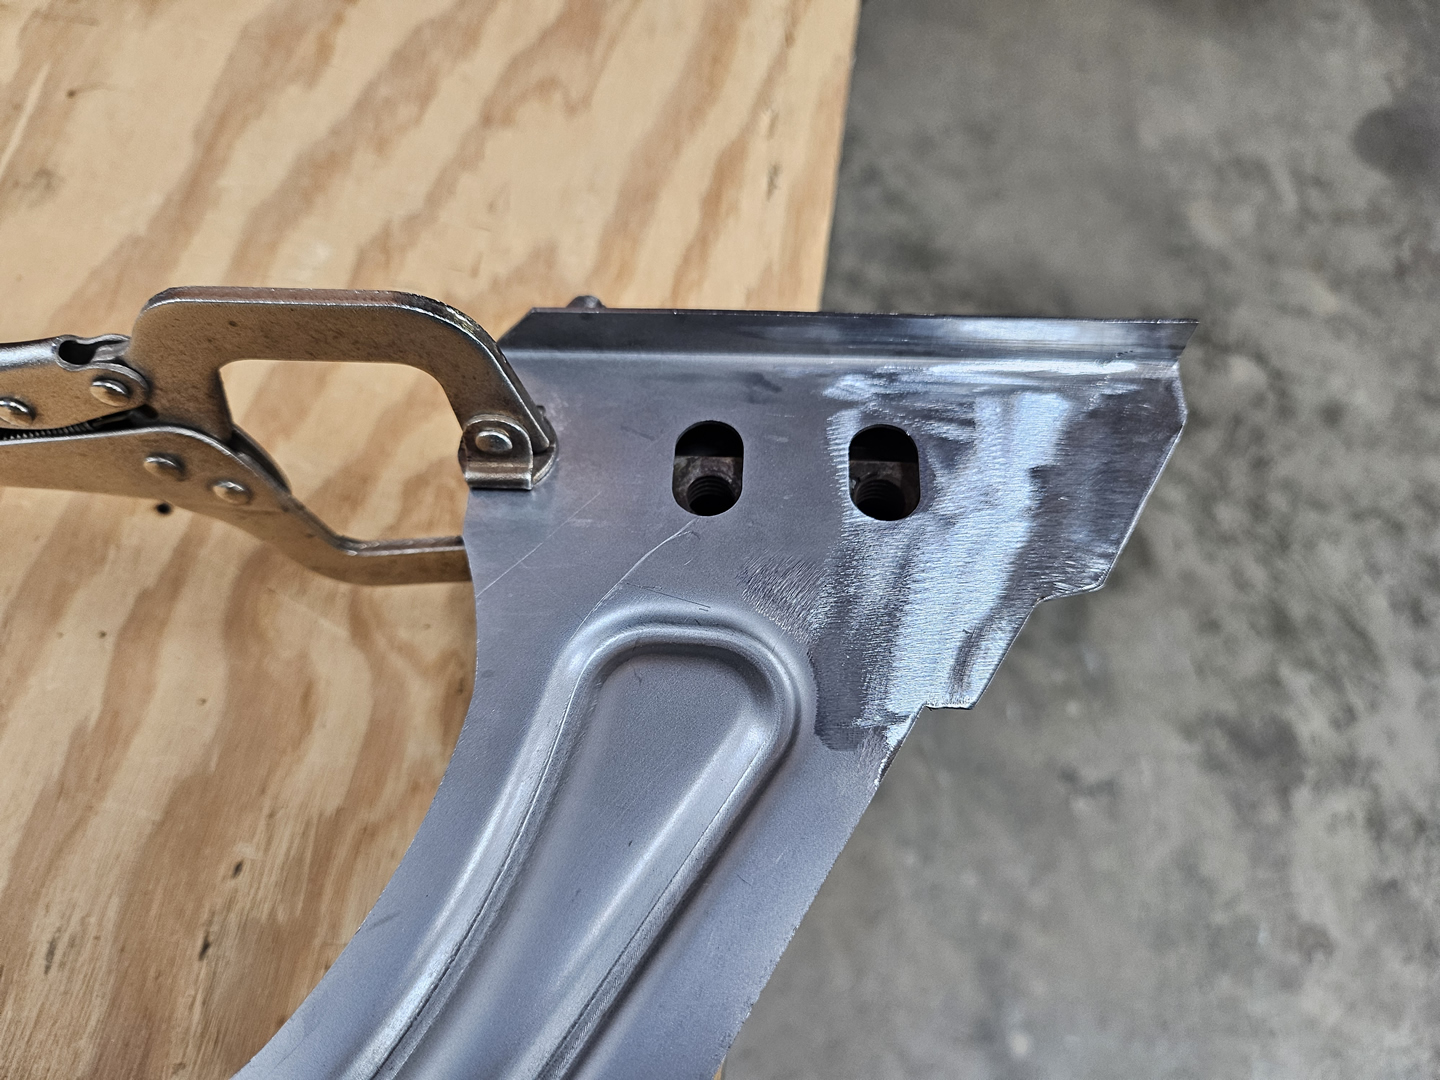
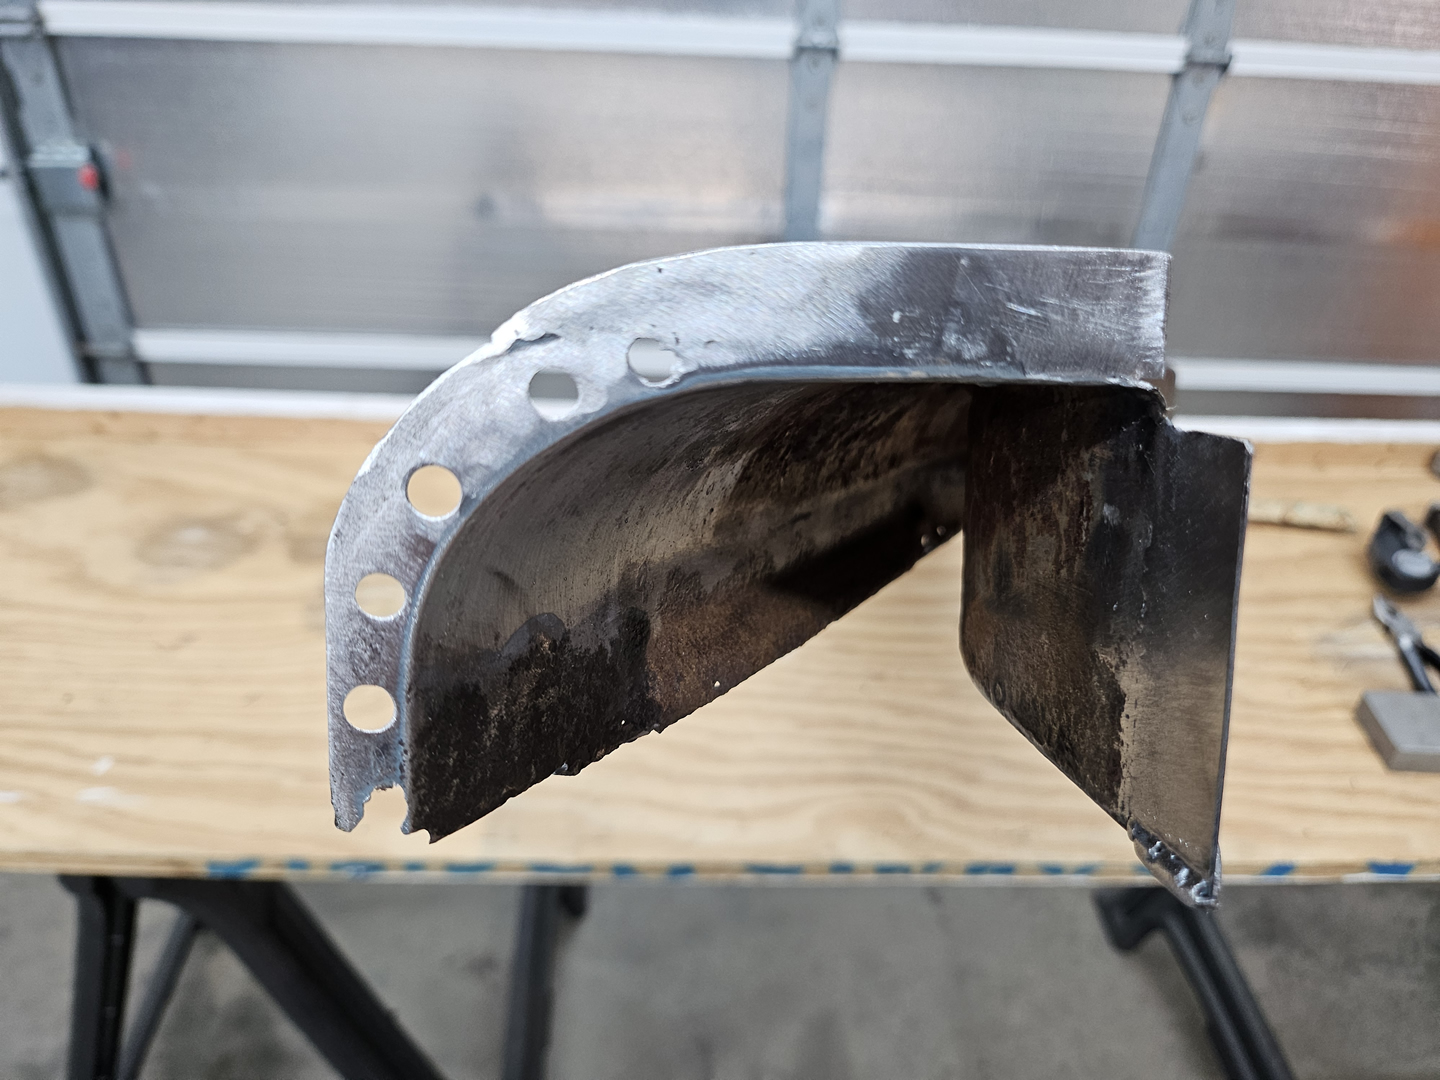
I discovered one weird thing that inner side part of the front end cap where the threaded plate is mounted - this side is not attached to the body of the channel. It is on the outer side, but not on this side. The bottom plate, however, is welded to this part of the end cap. I'm not sure why it is designed this way. Perhaps it is to give it some flexibility to this area when attaching to the bottom of the front firewall.
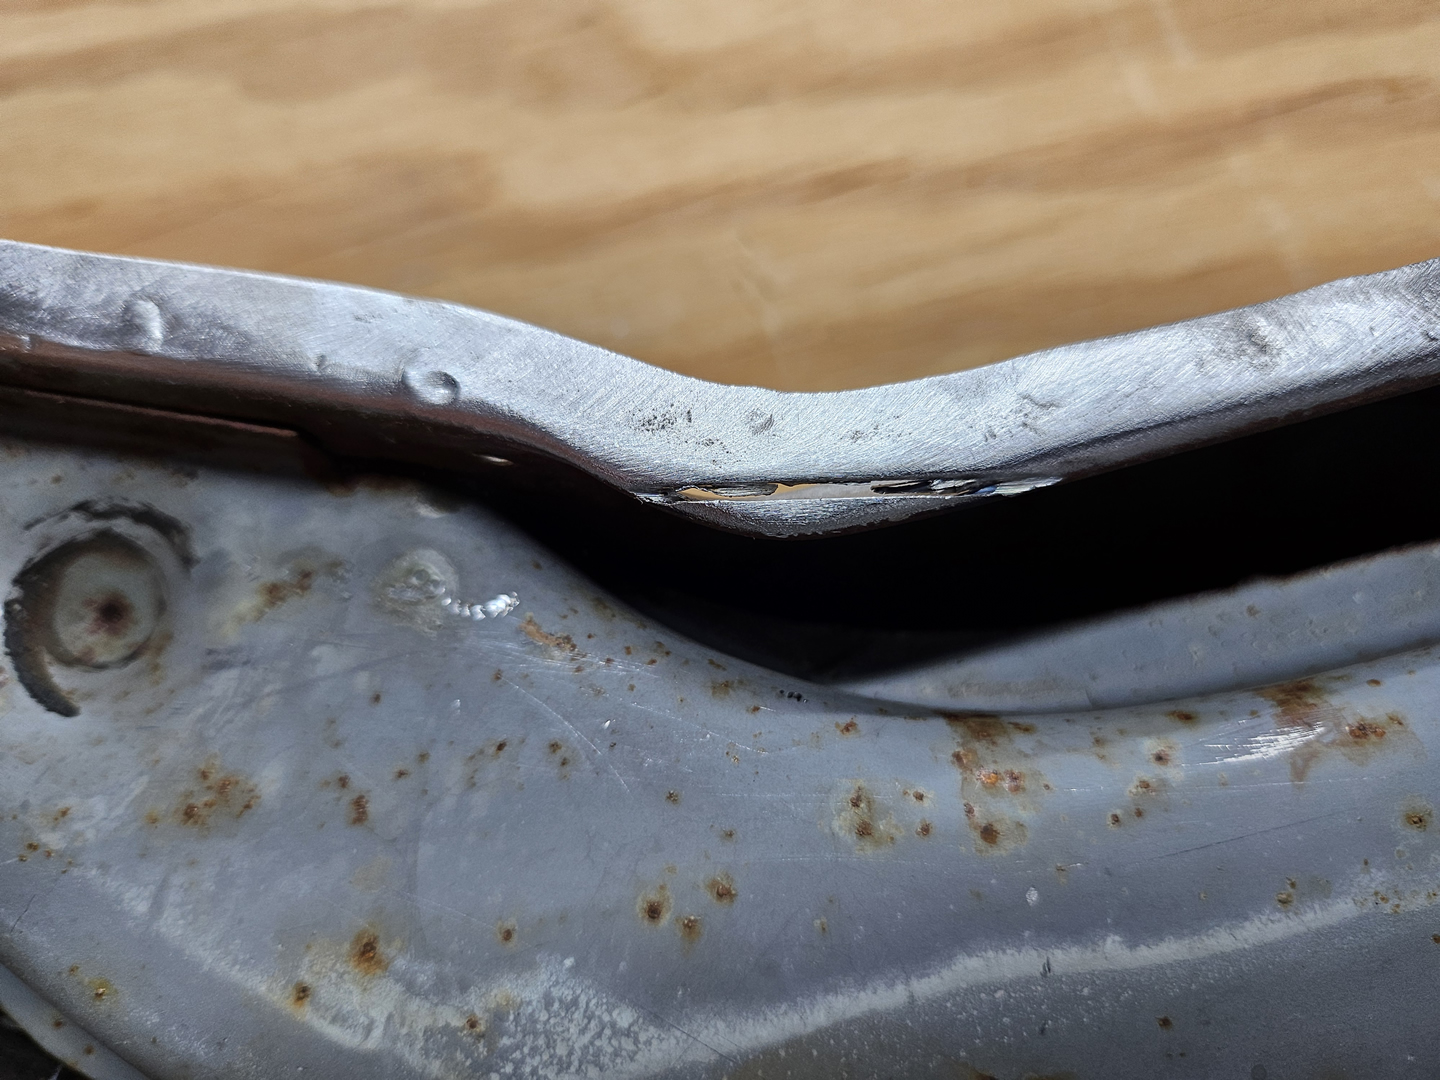
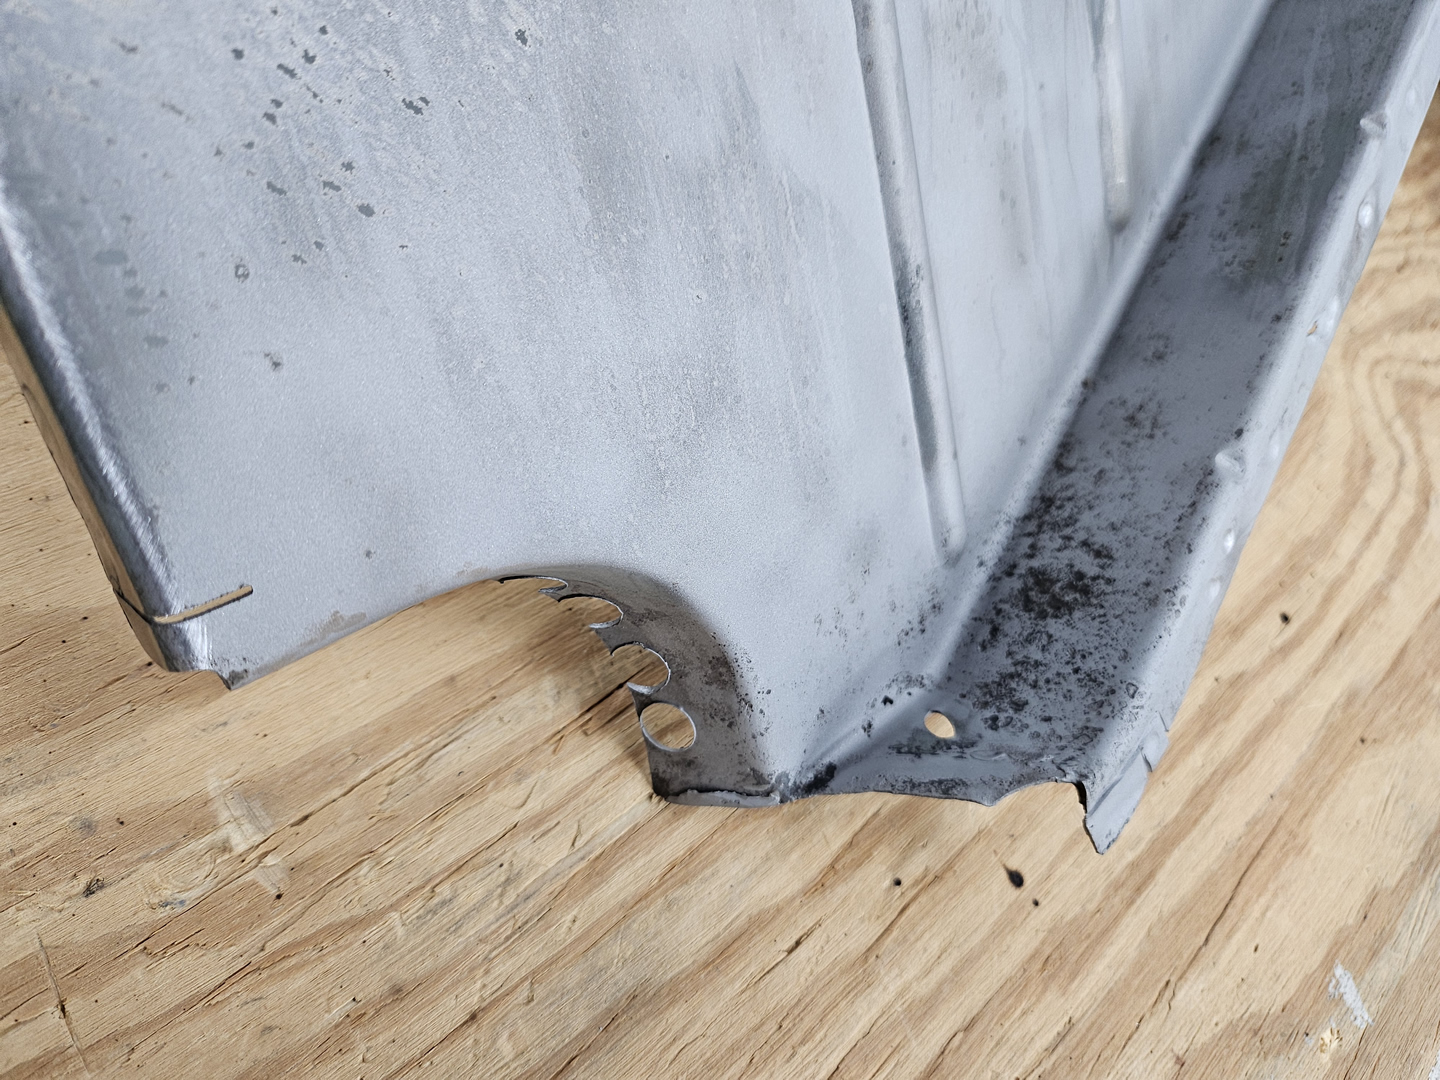
Also, I was a bit careless and cut into a sharp bend of the channel when removing the bottom plate. More welding practice.
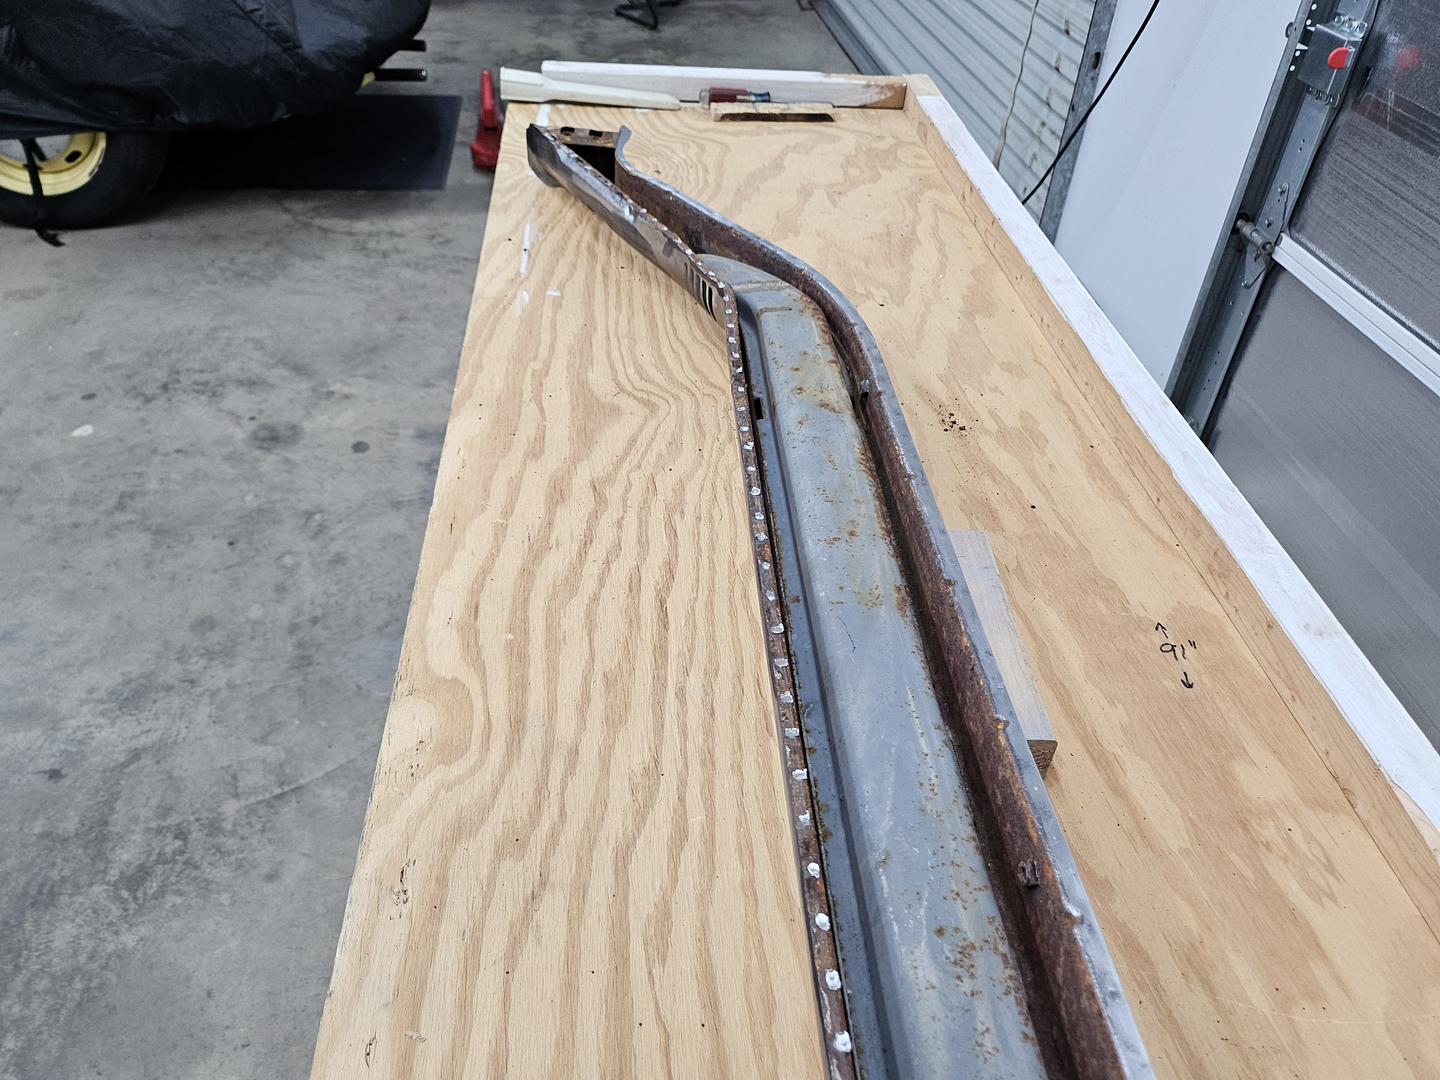
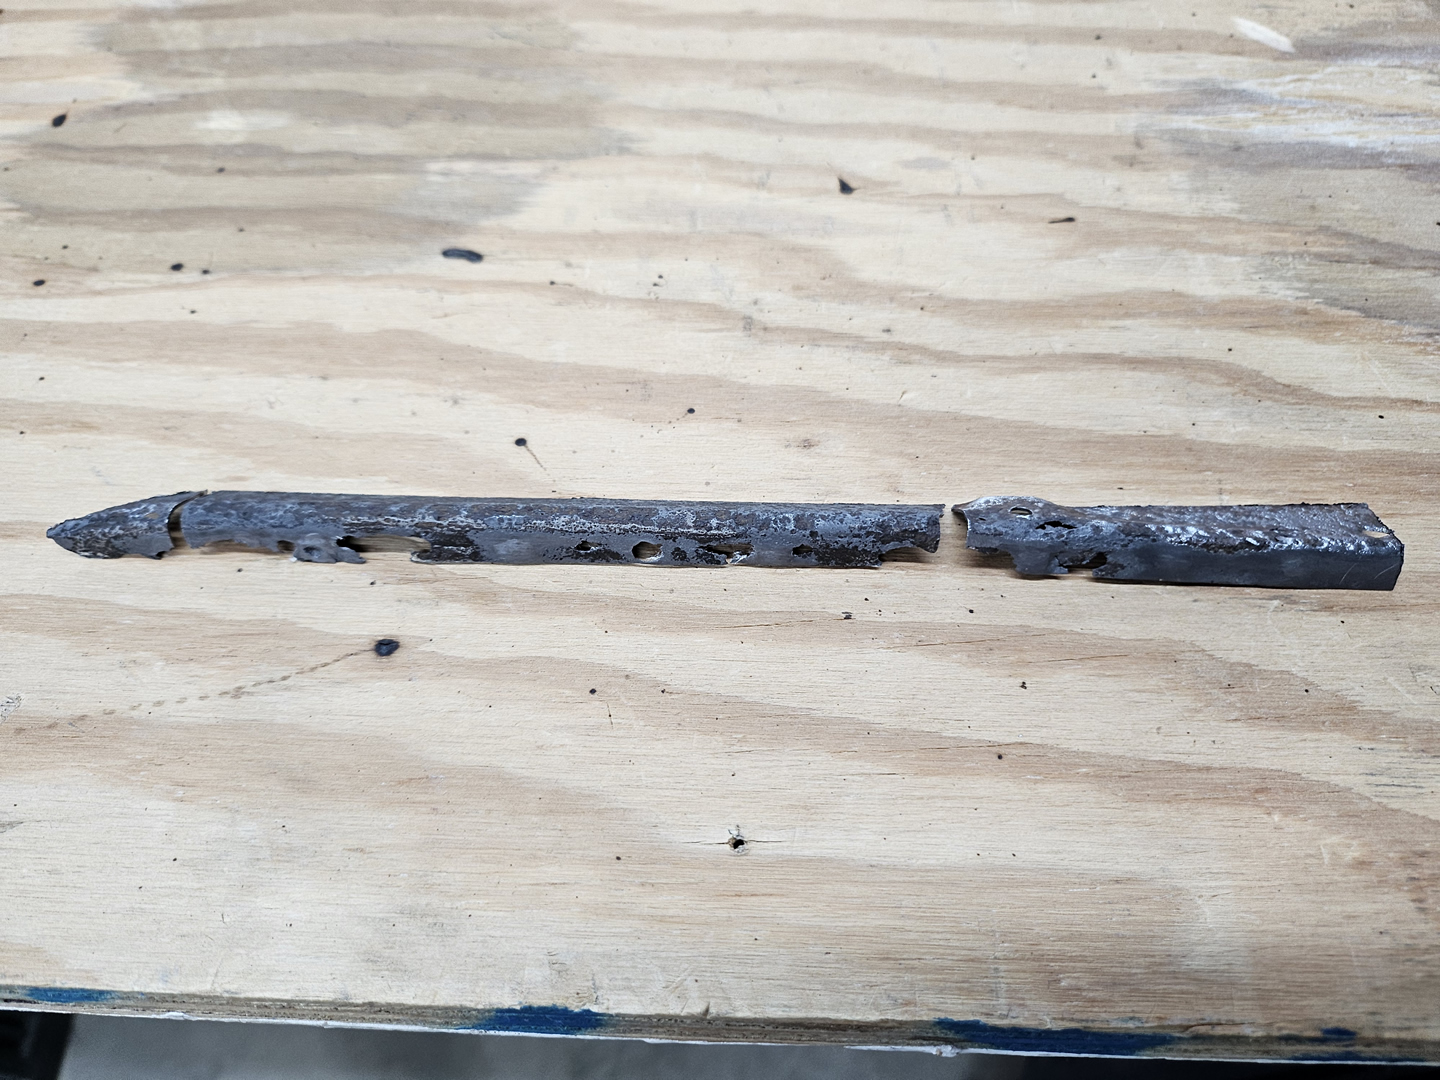
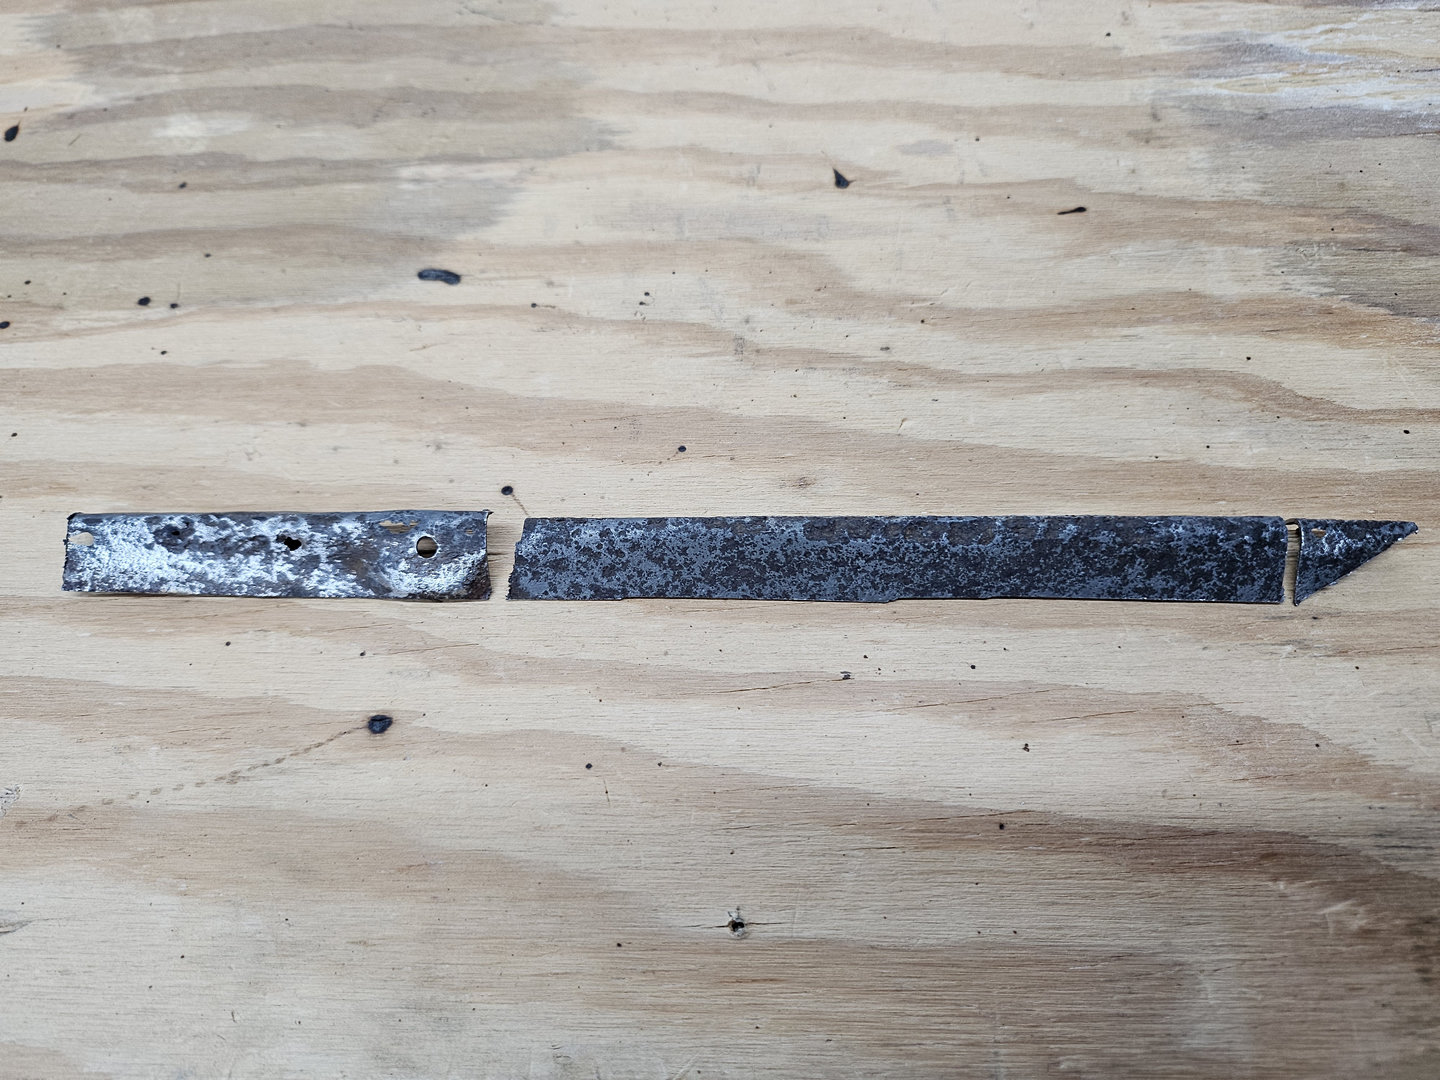
After the plate was completely removed, I was left with a pile of rusty and twisted metal. Overall, it was worth the effort to remove the bottom plate on this channel as it was very rusted and dented.
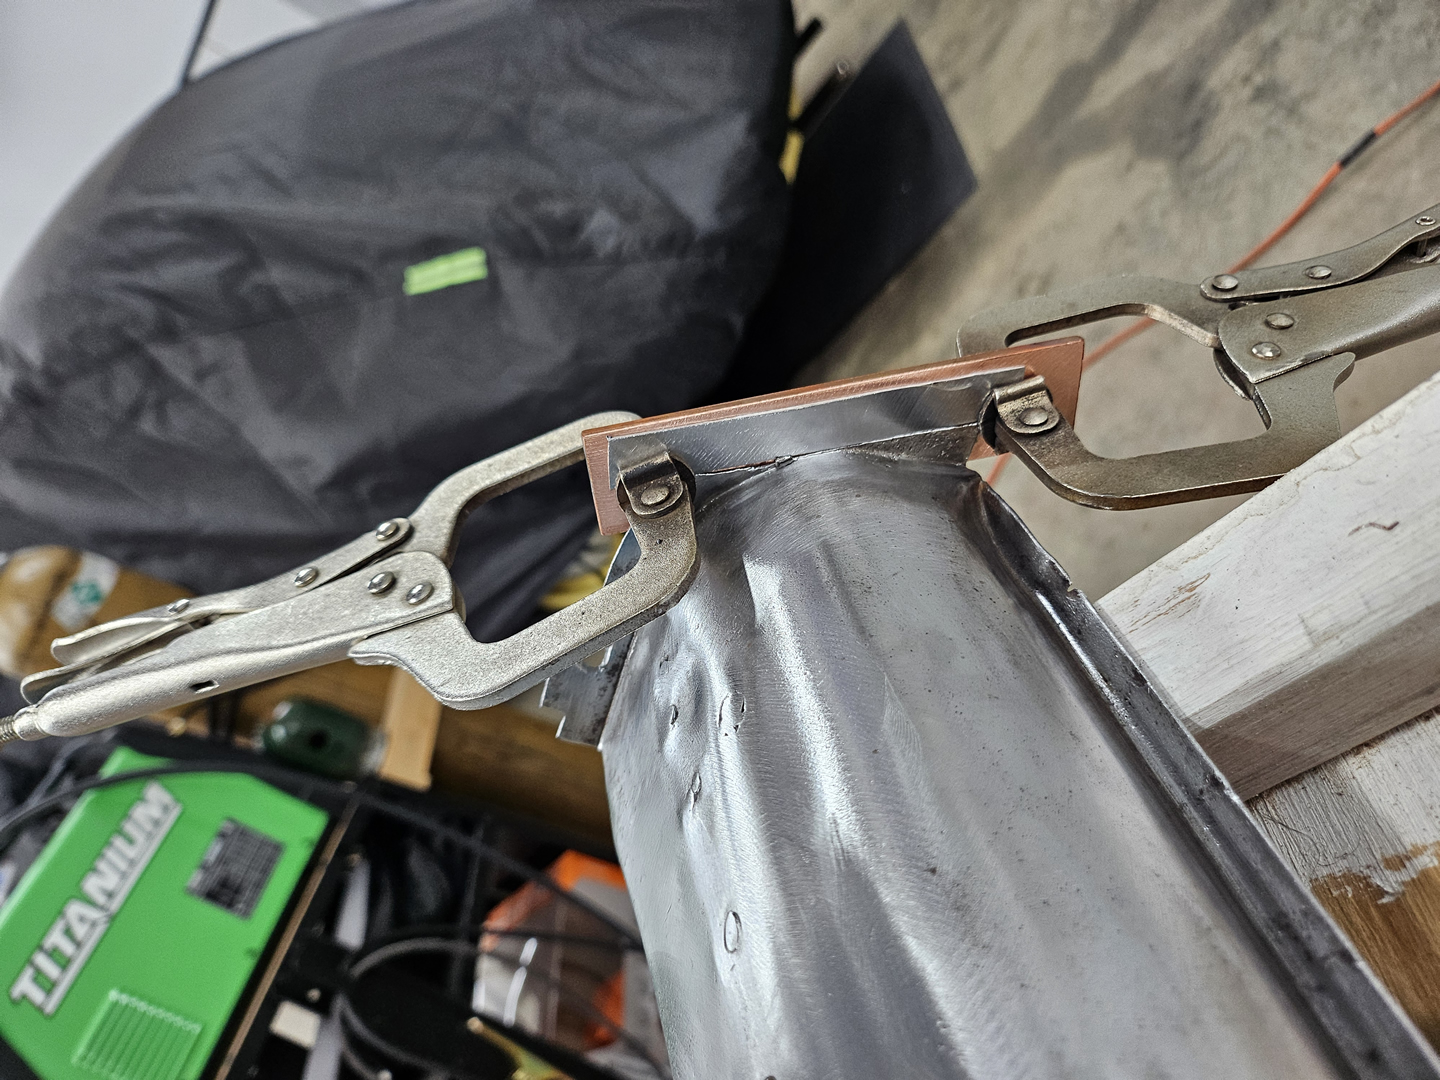
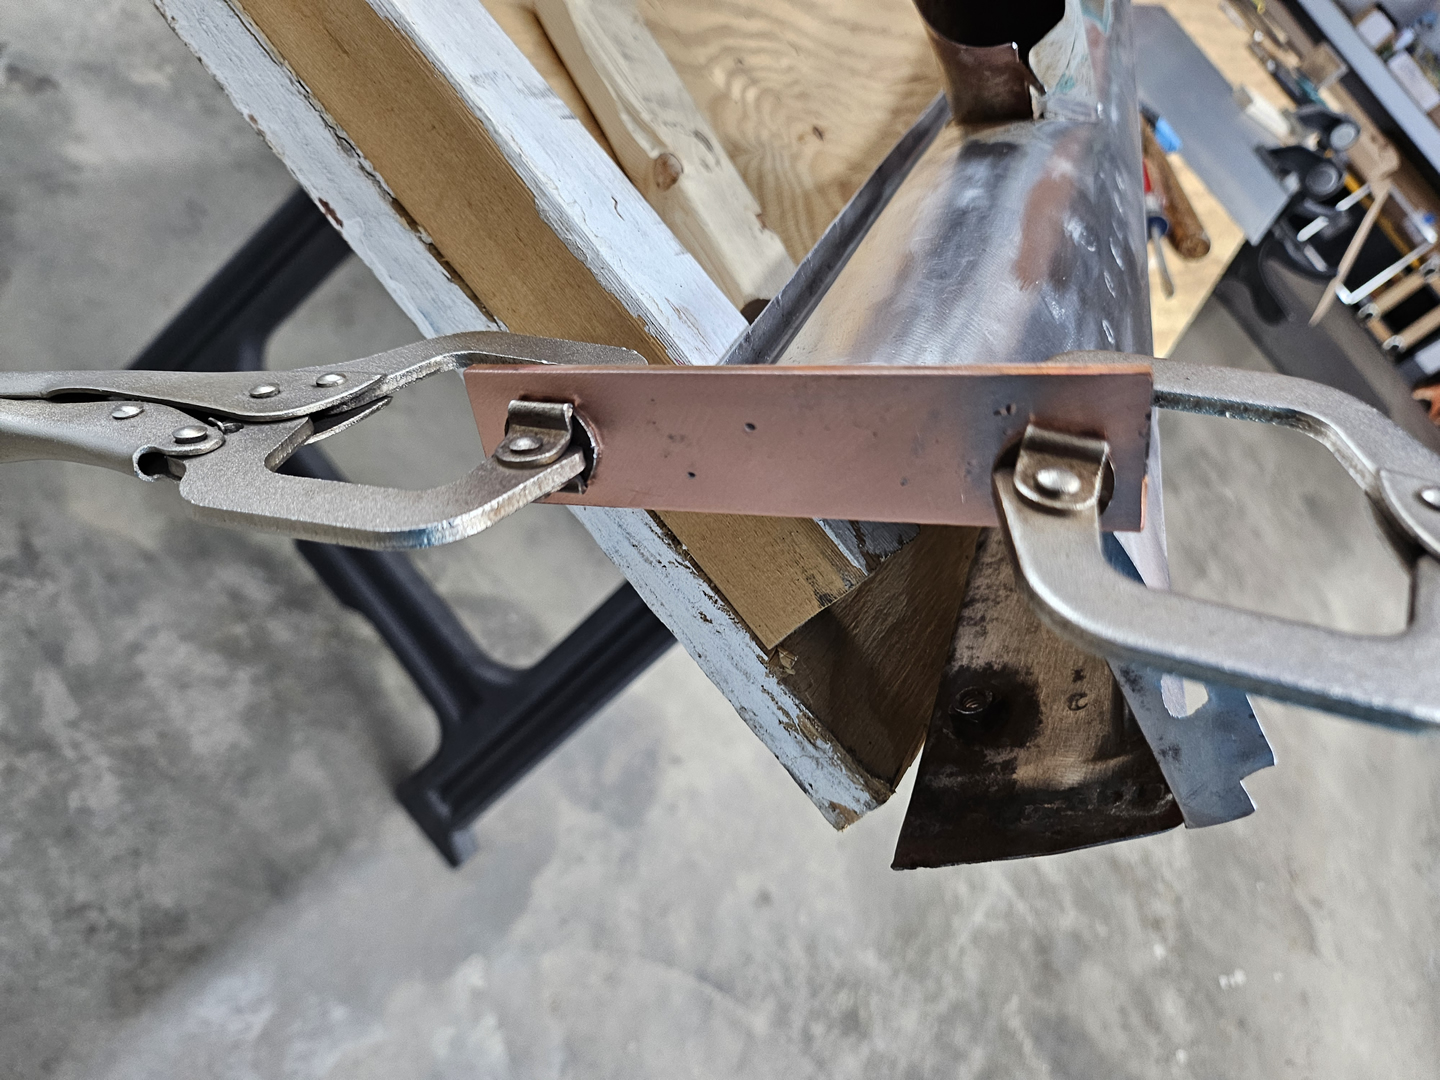
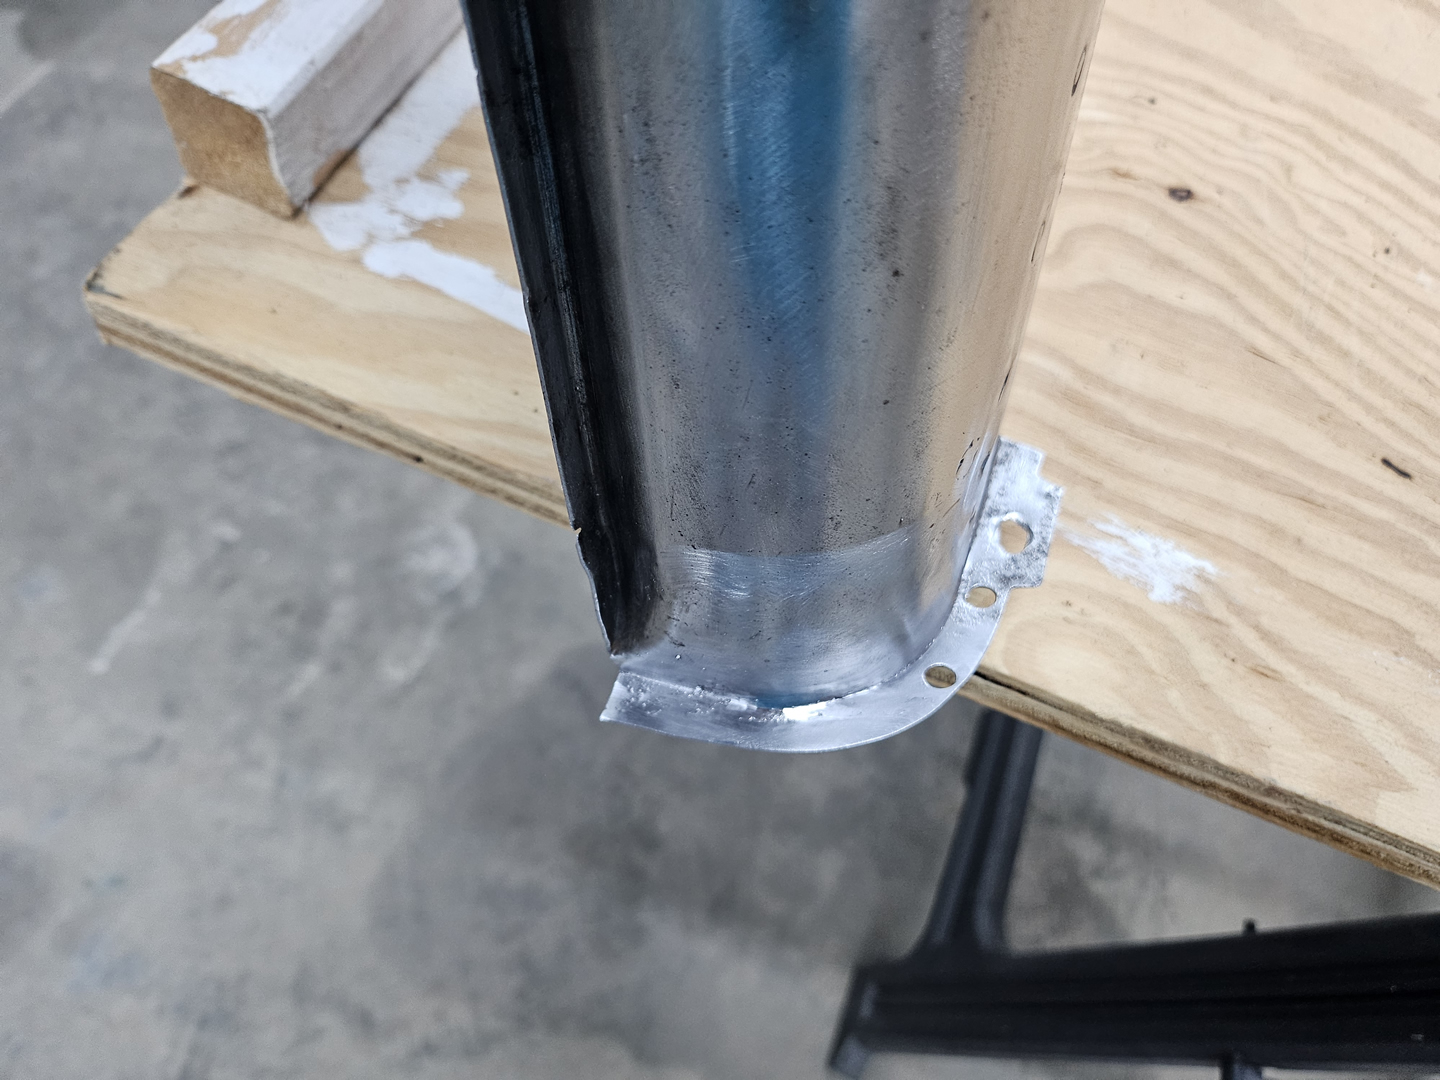
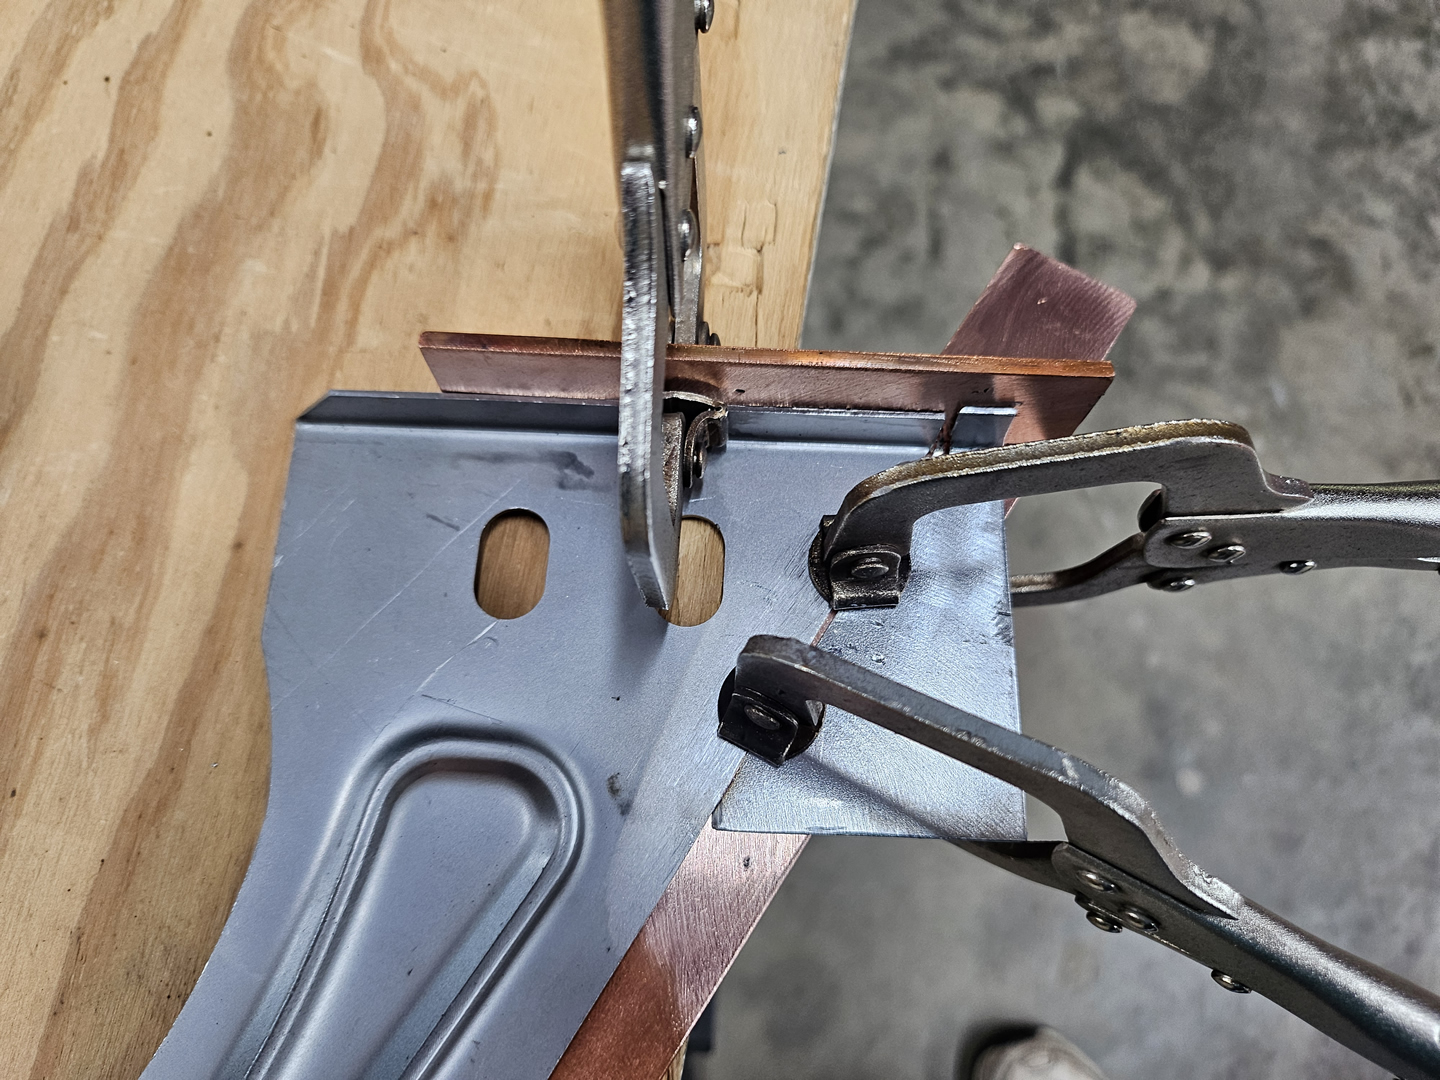
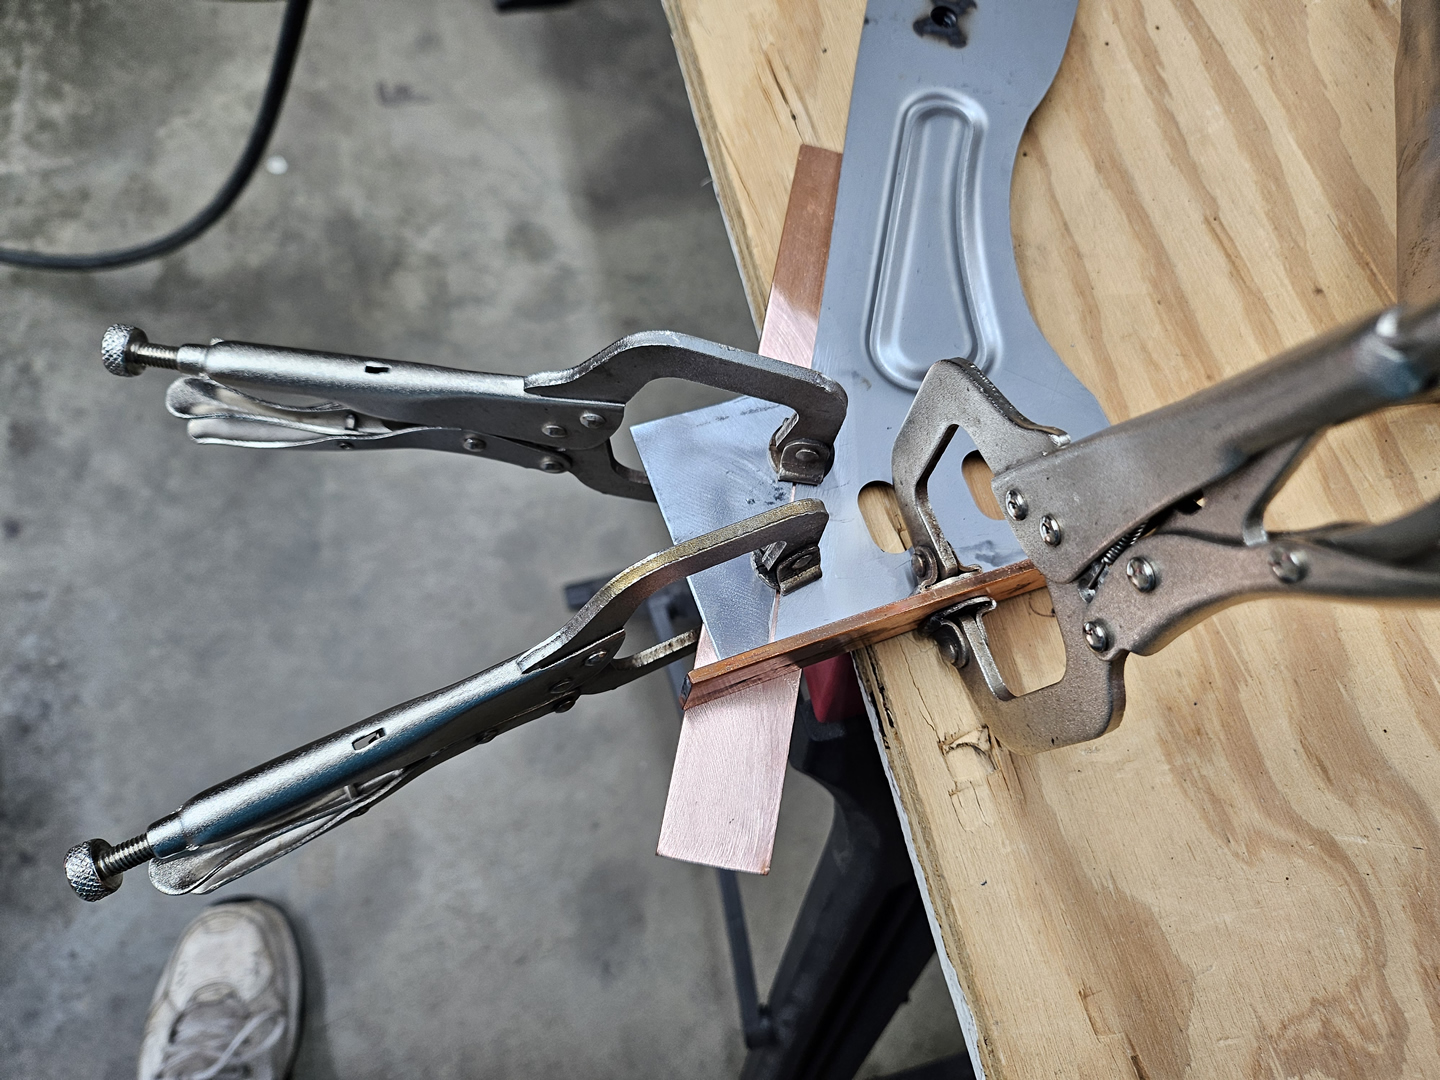
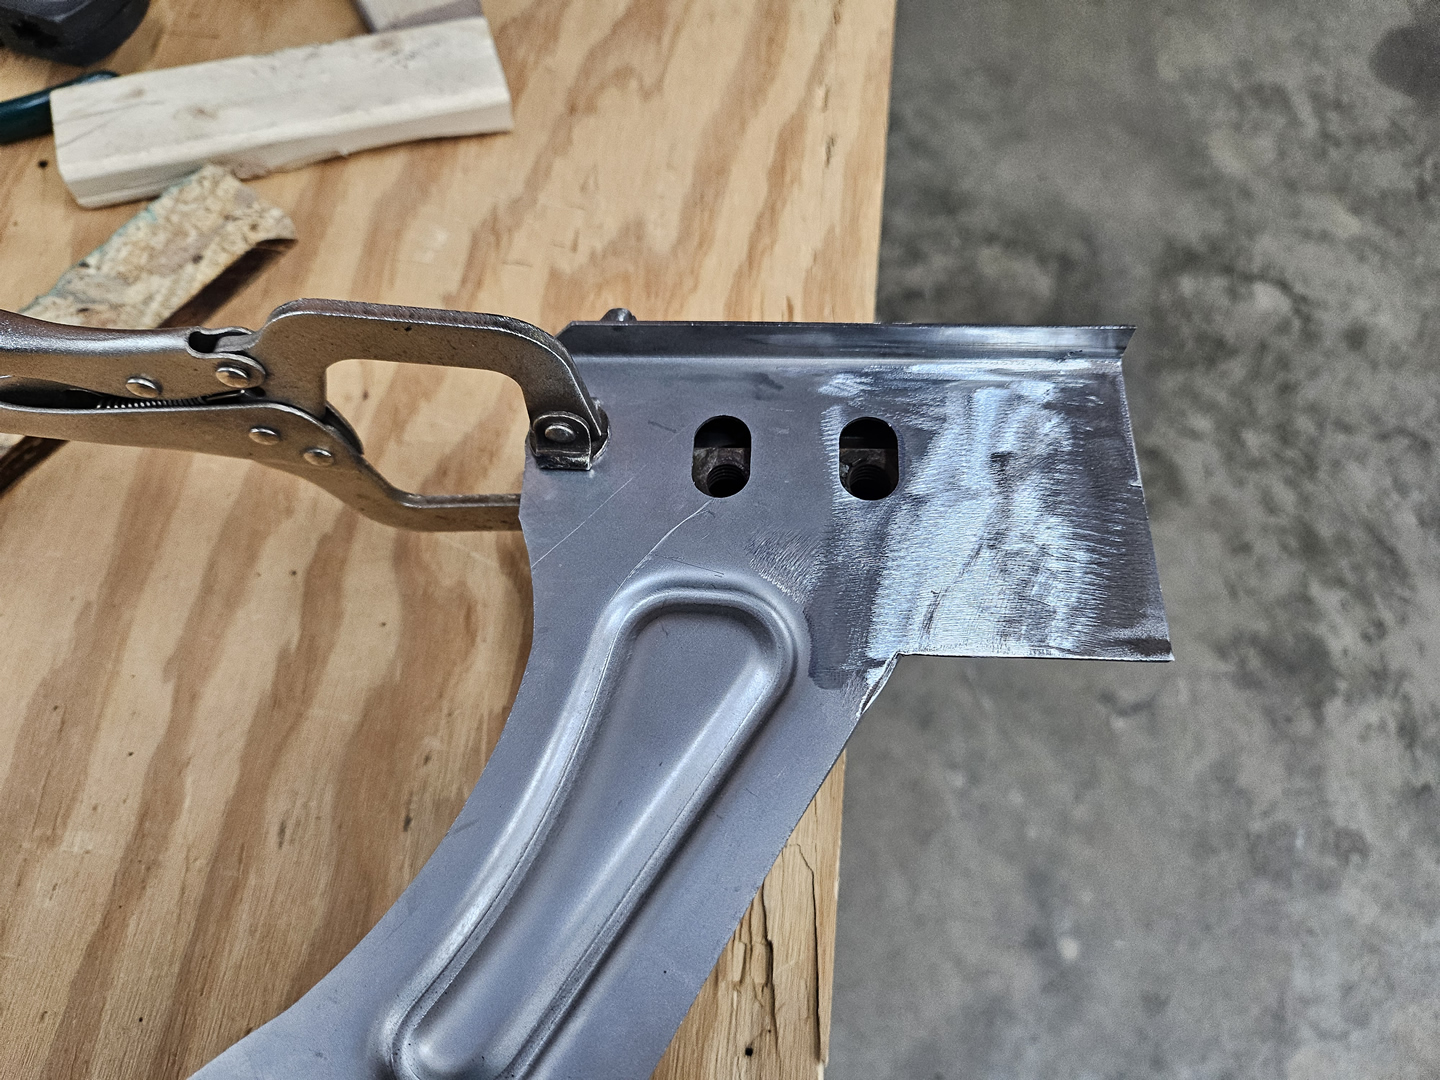
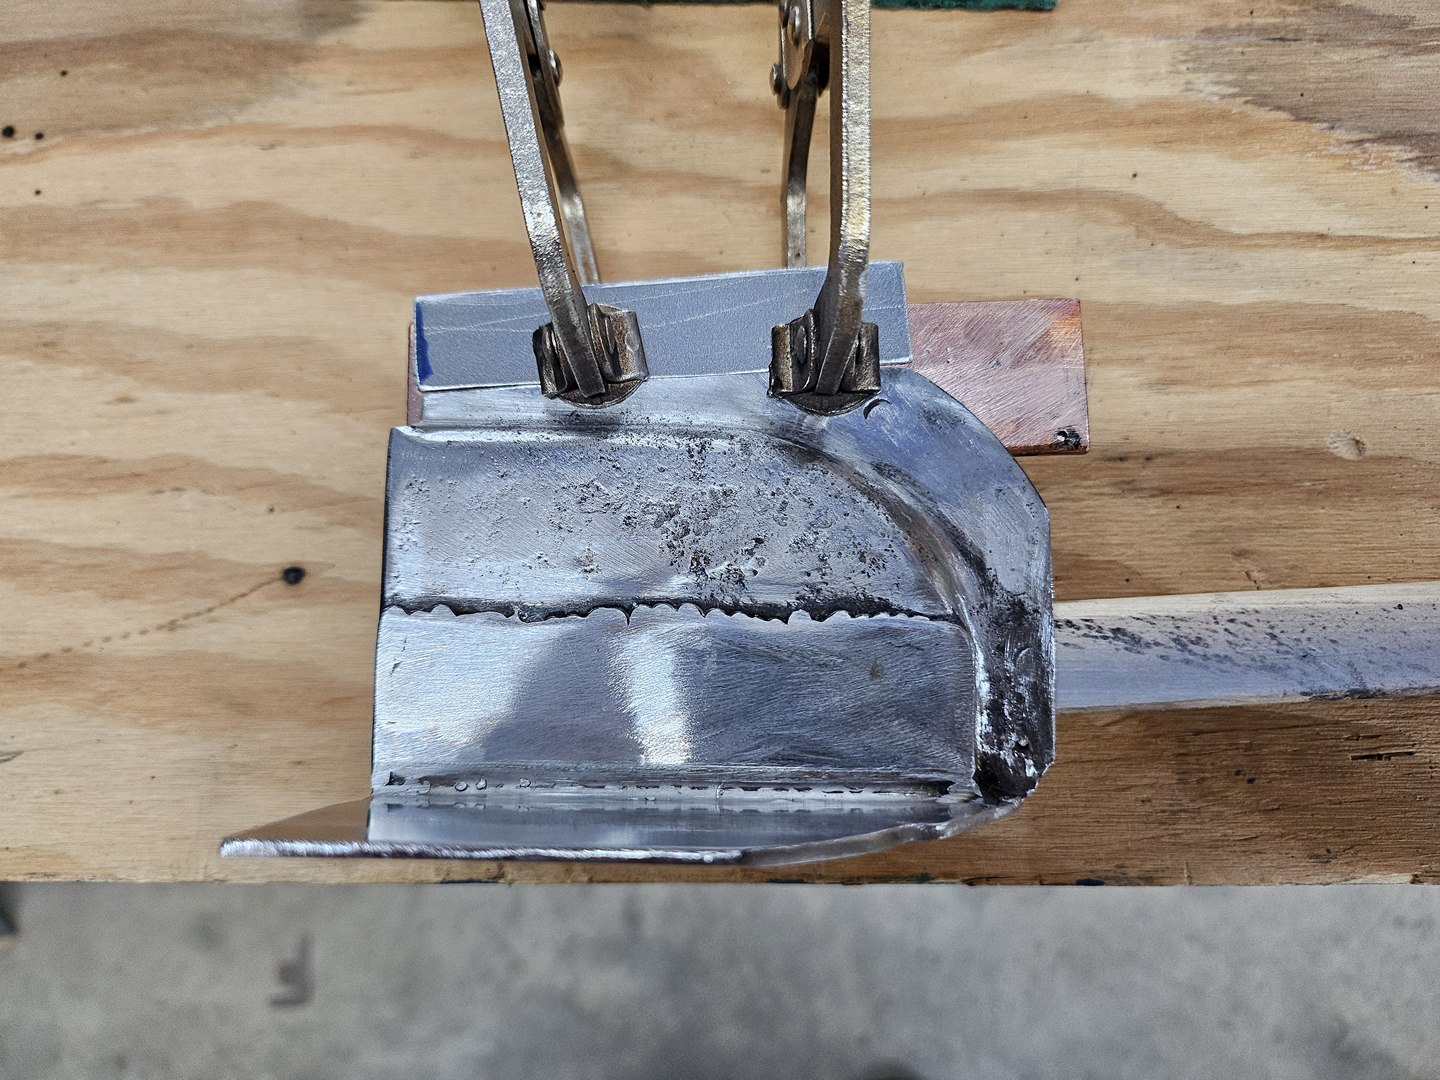
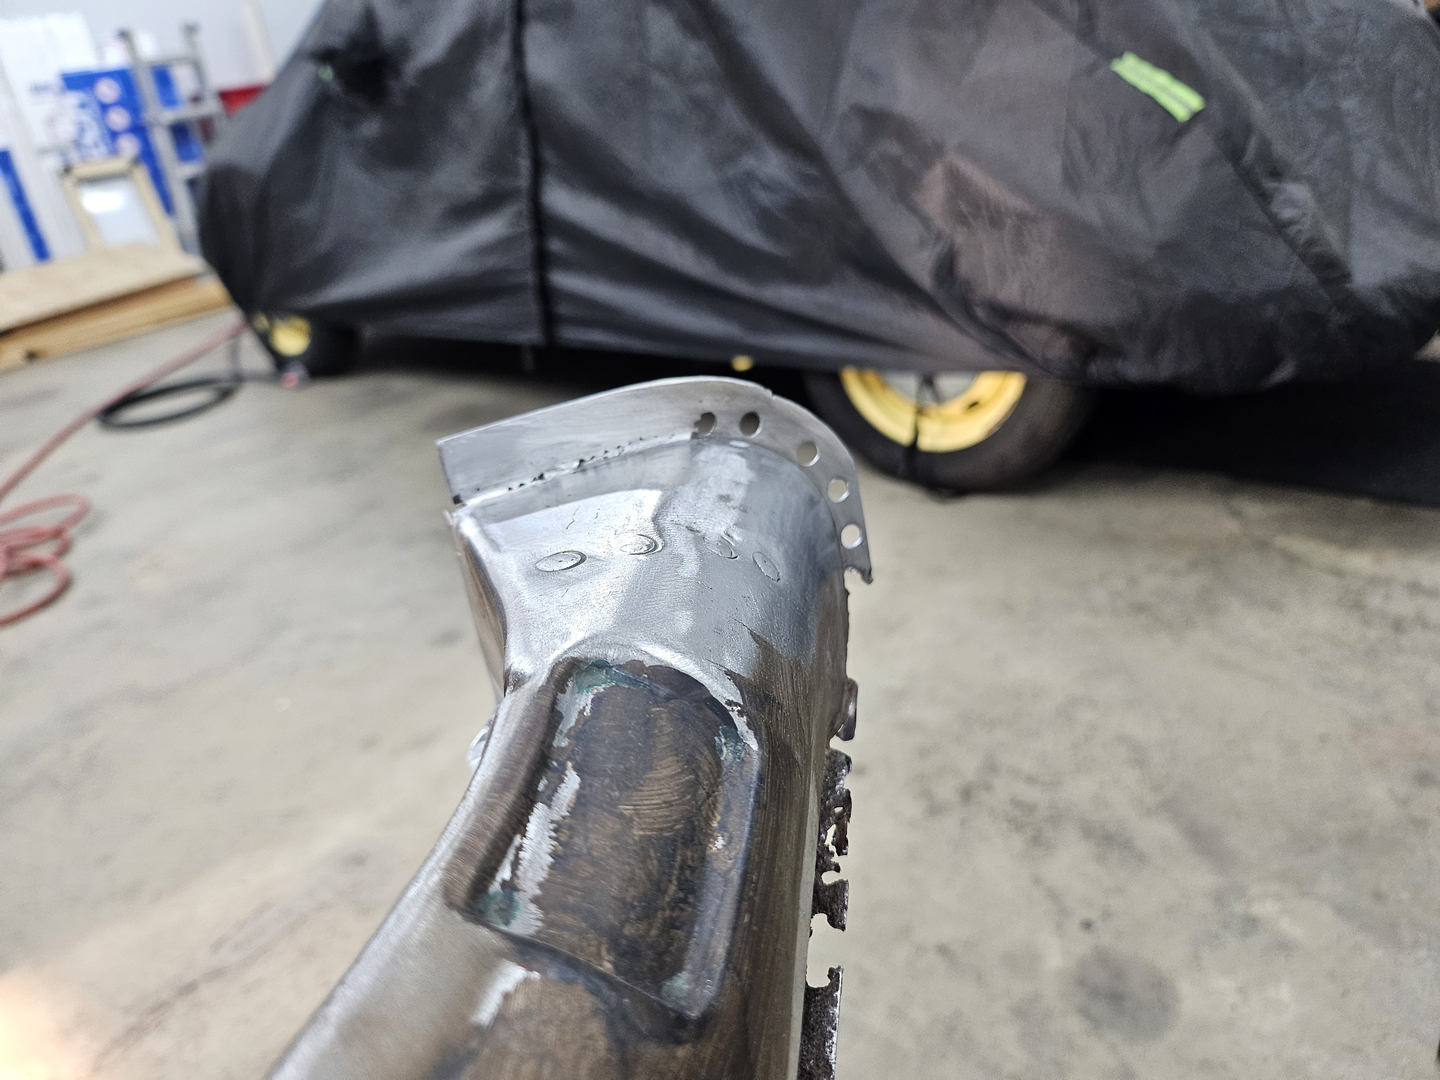
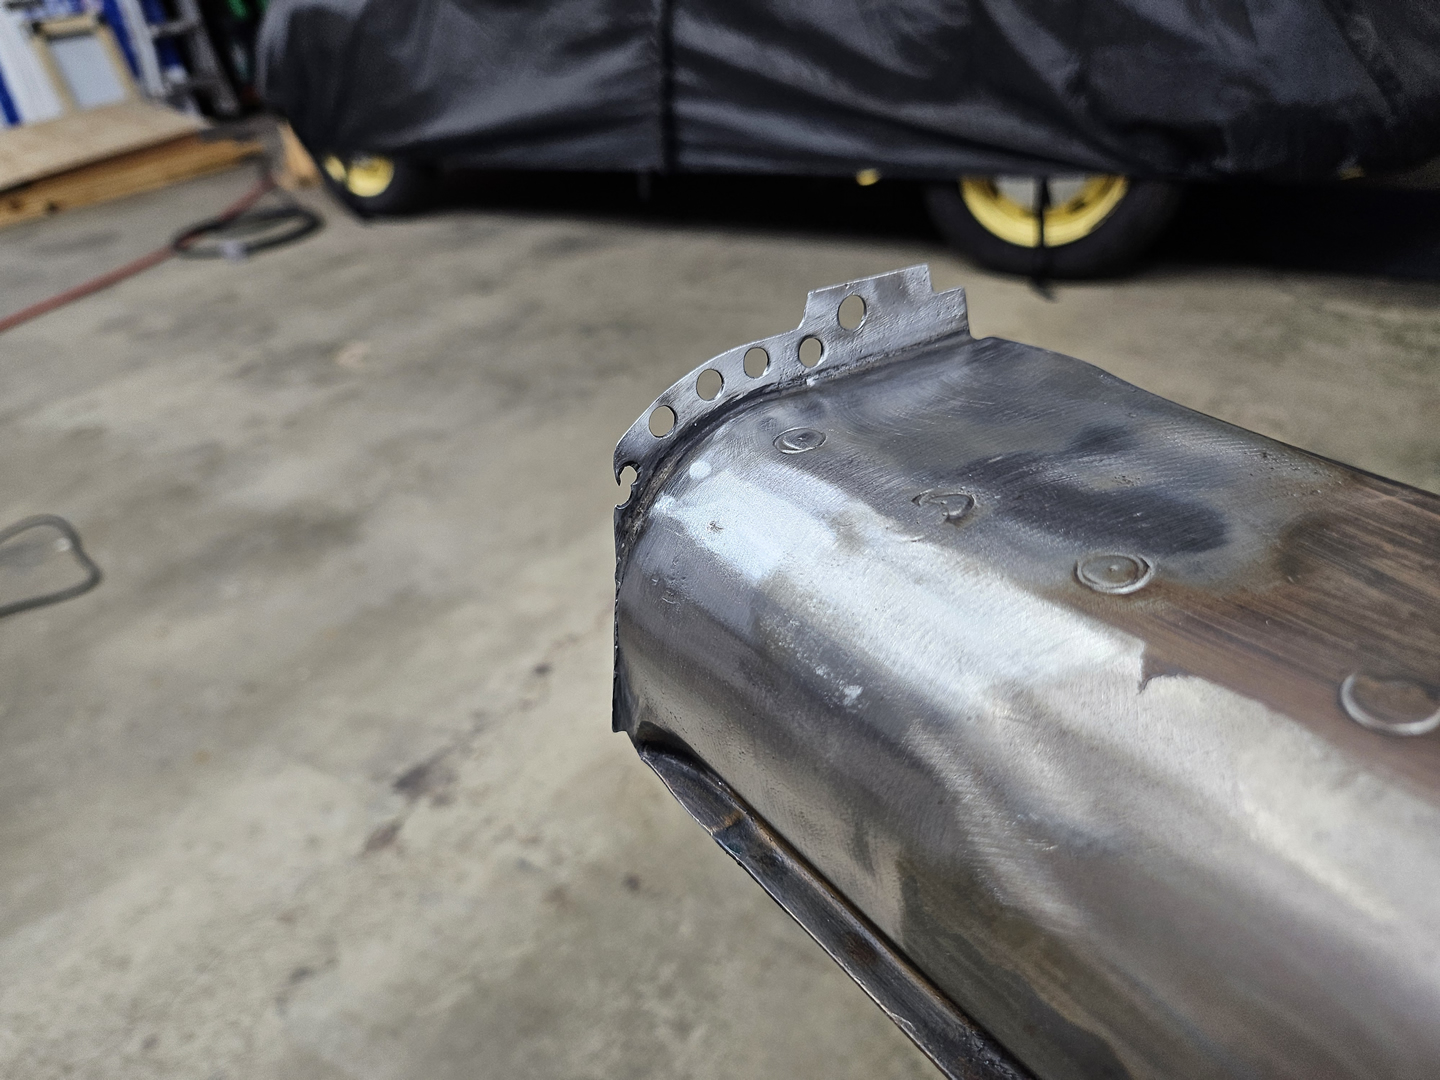
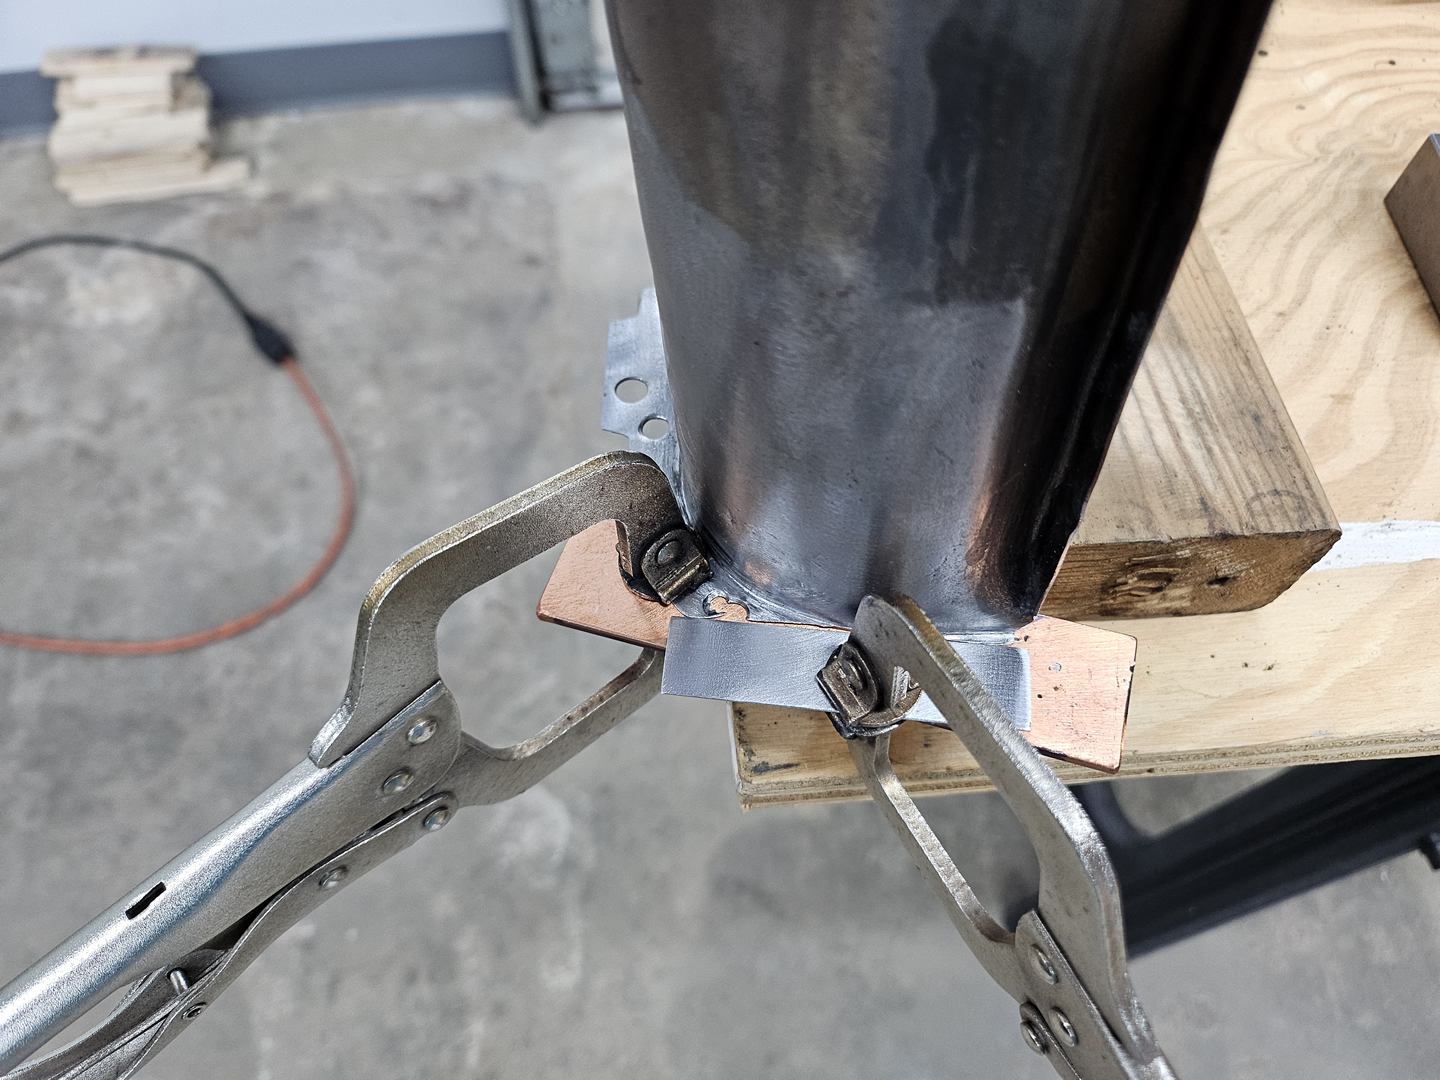
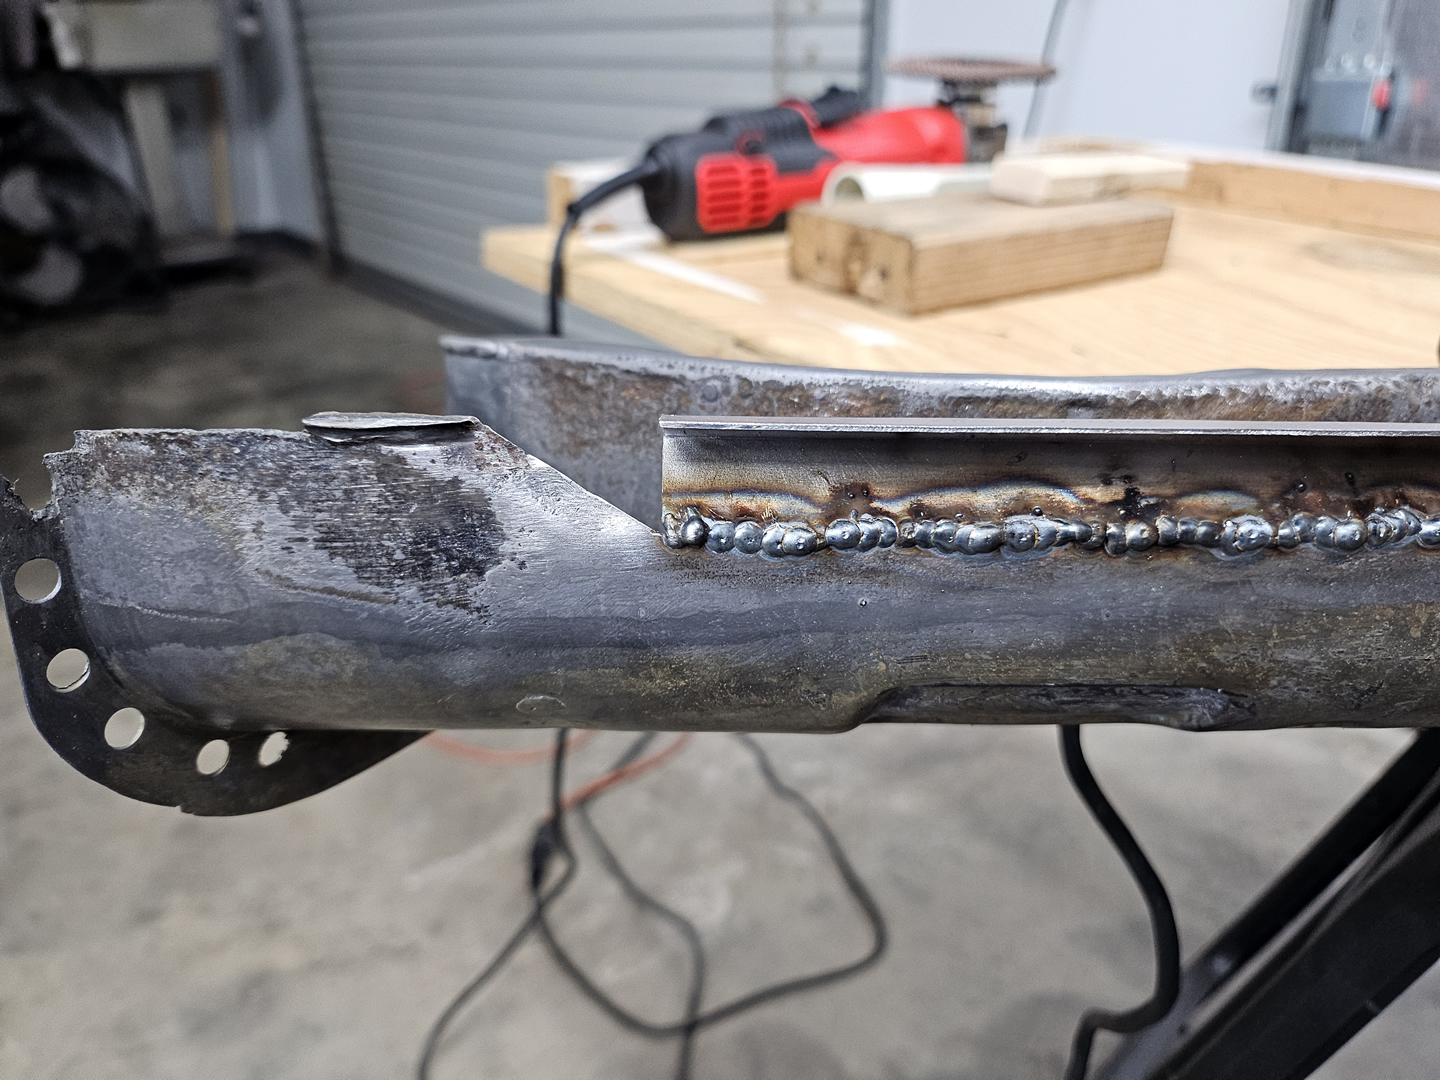
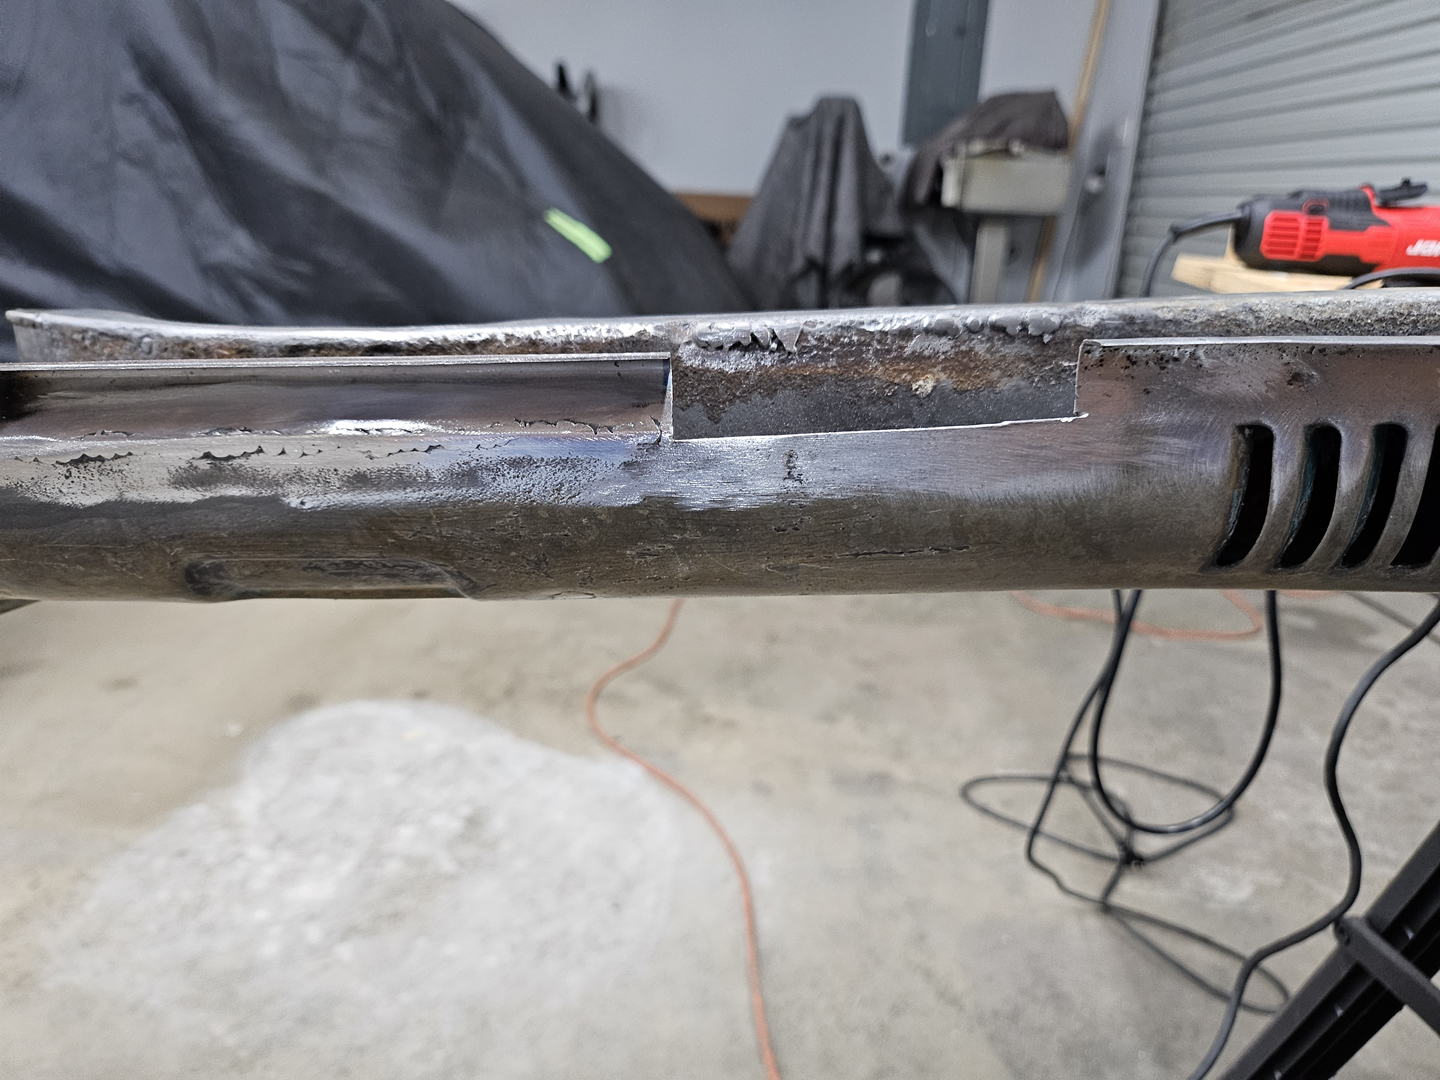
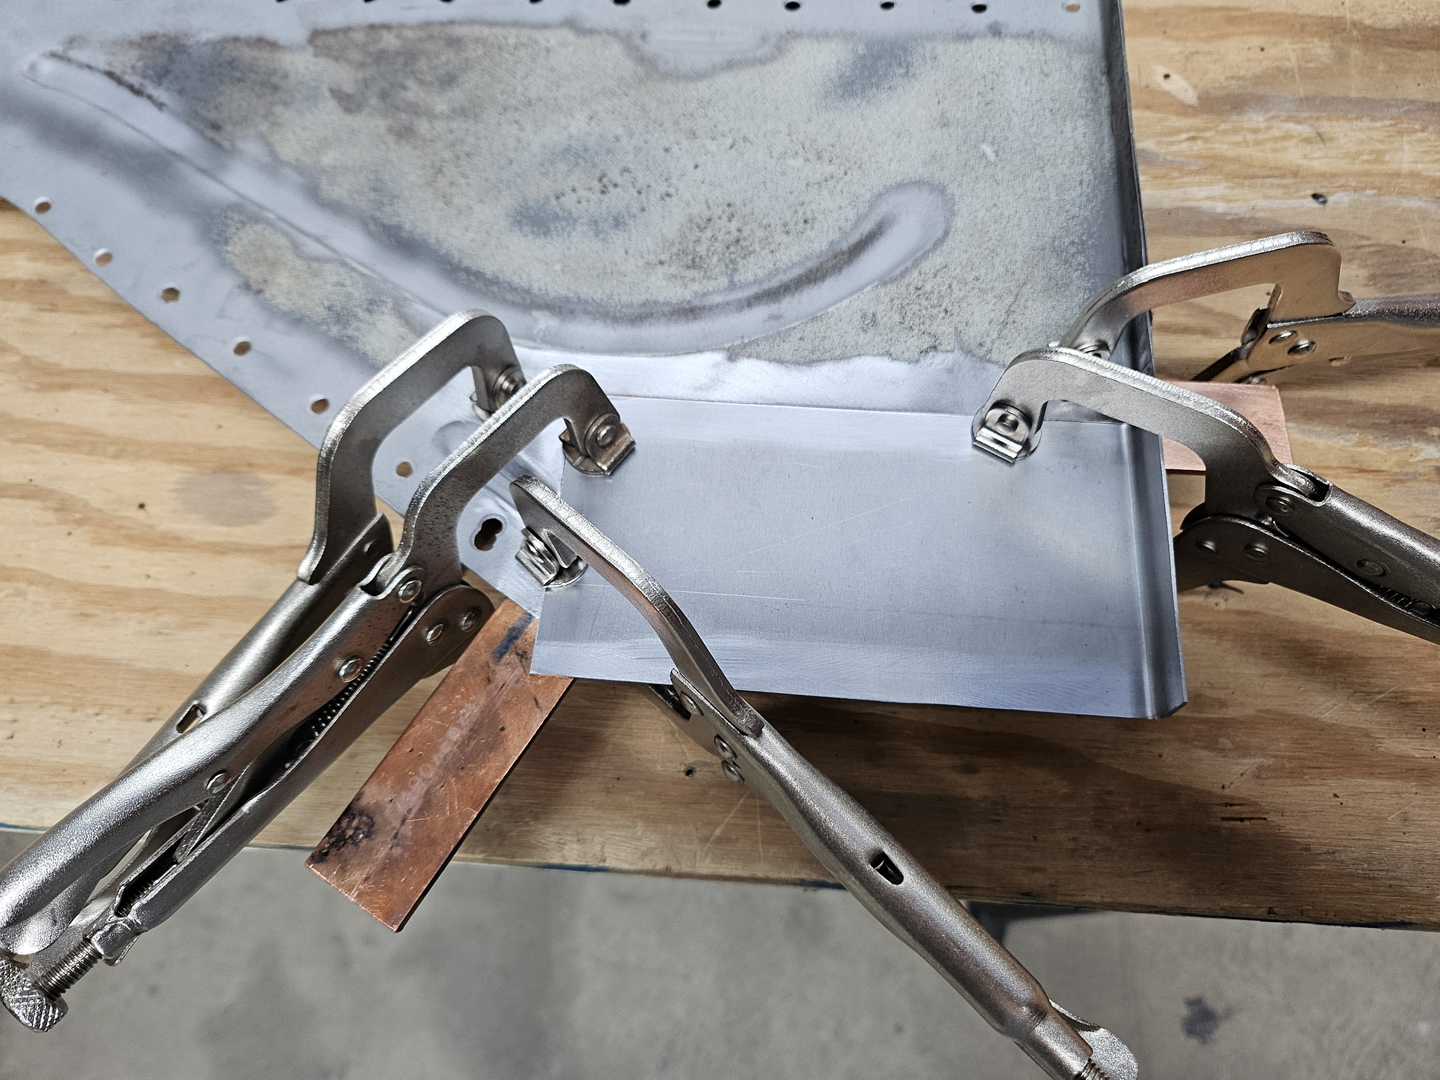
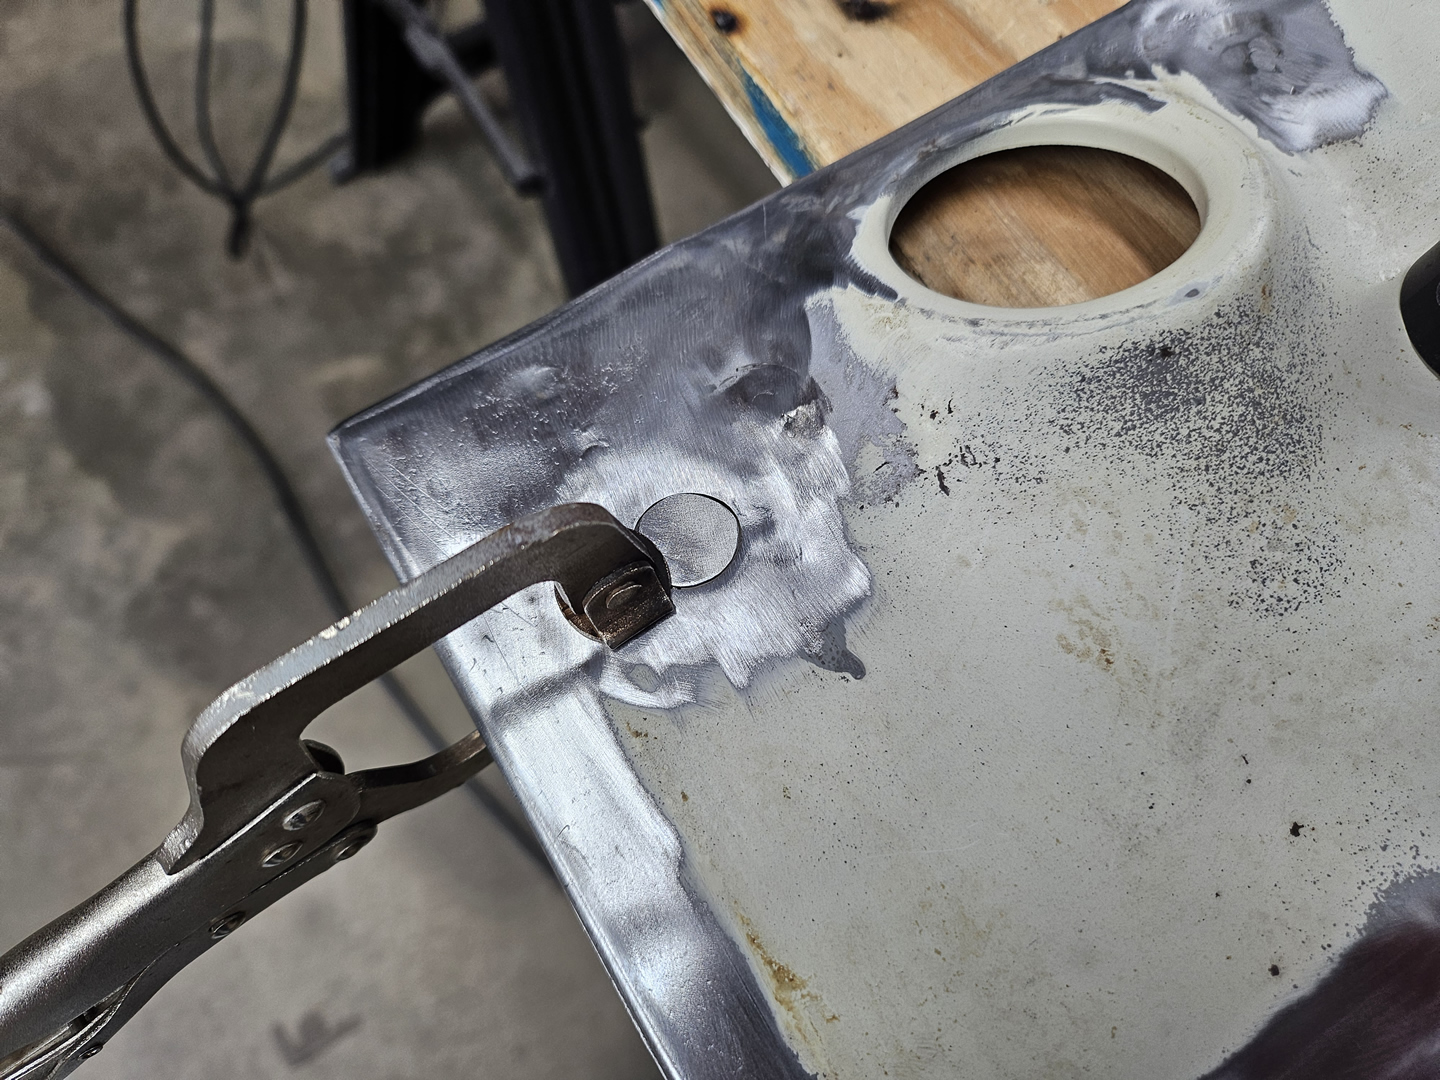
Continuing on with the passenger side heater channel, I decided to repair the flanges on the front and rear ends where they had been cut by the person who cut them off of the donor car. I did the rear flange first. This is where the heater channel is attached to the rear cross members. I used 20-gauge stock which matches the original metal. I used a piece of a flat copper bar which not only holds the repair piece flat and in place, but allows me to weld with a little more heat and get better penetration without blowing through the metal.
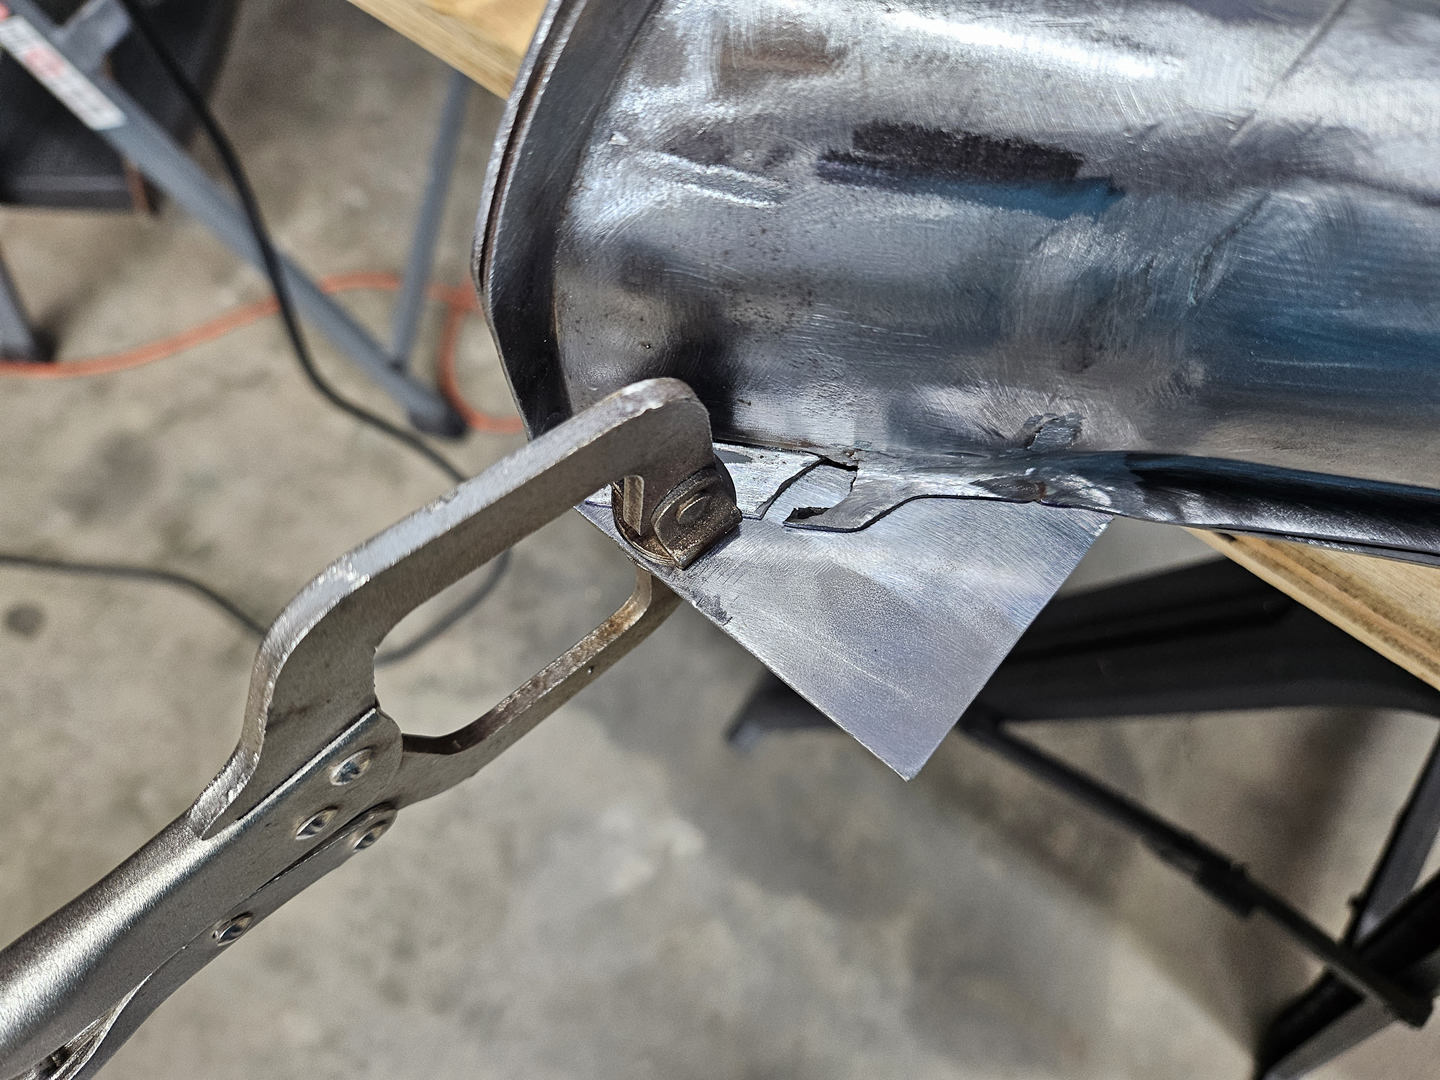
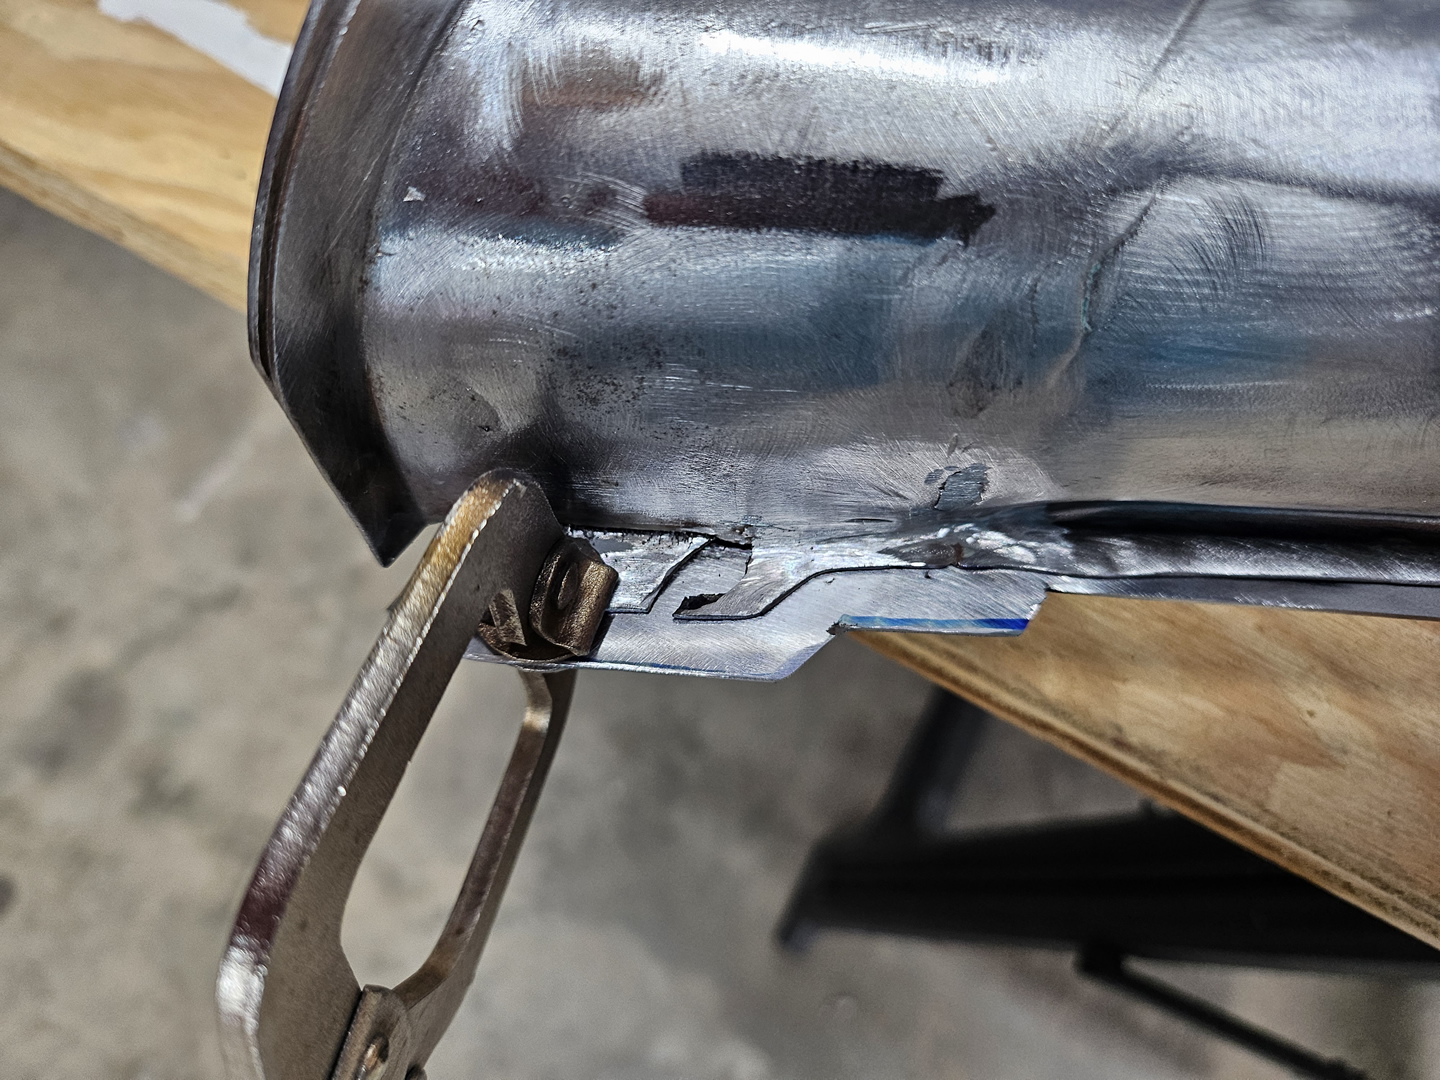
Next, I patched in a piece on the front flange of the end cap. Here, the flange is actually the end cap and the flange on the flare of the end of the body of the channel. But since I wasn't going to remove the end cap for any reason, I just welded in a single thickness of metal that was equivalent to the two pieces combined.
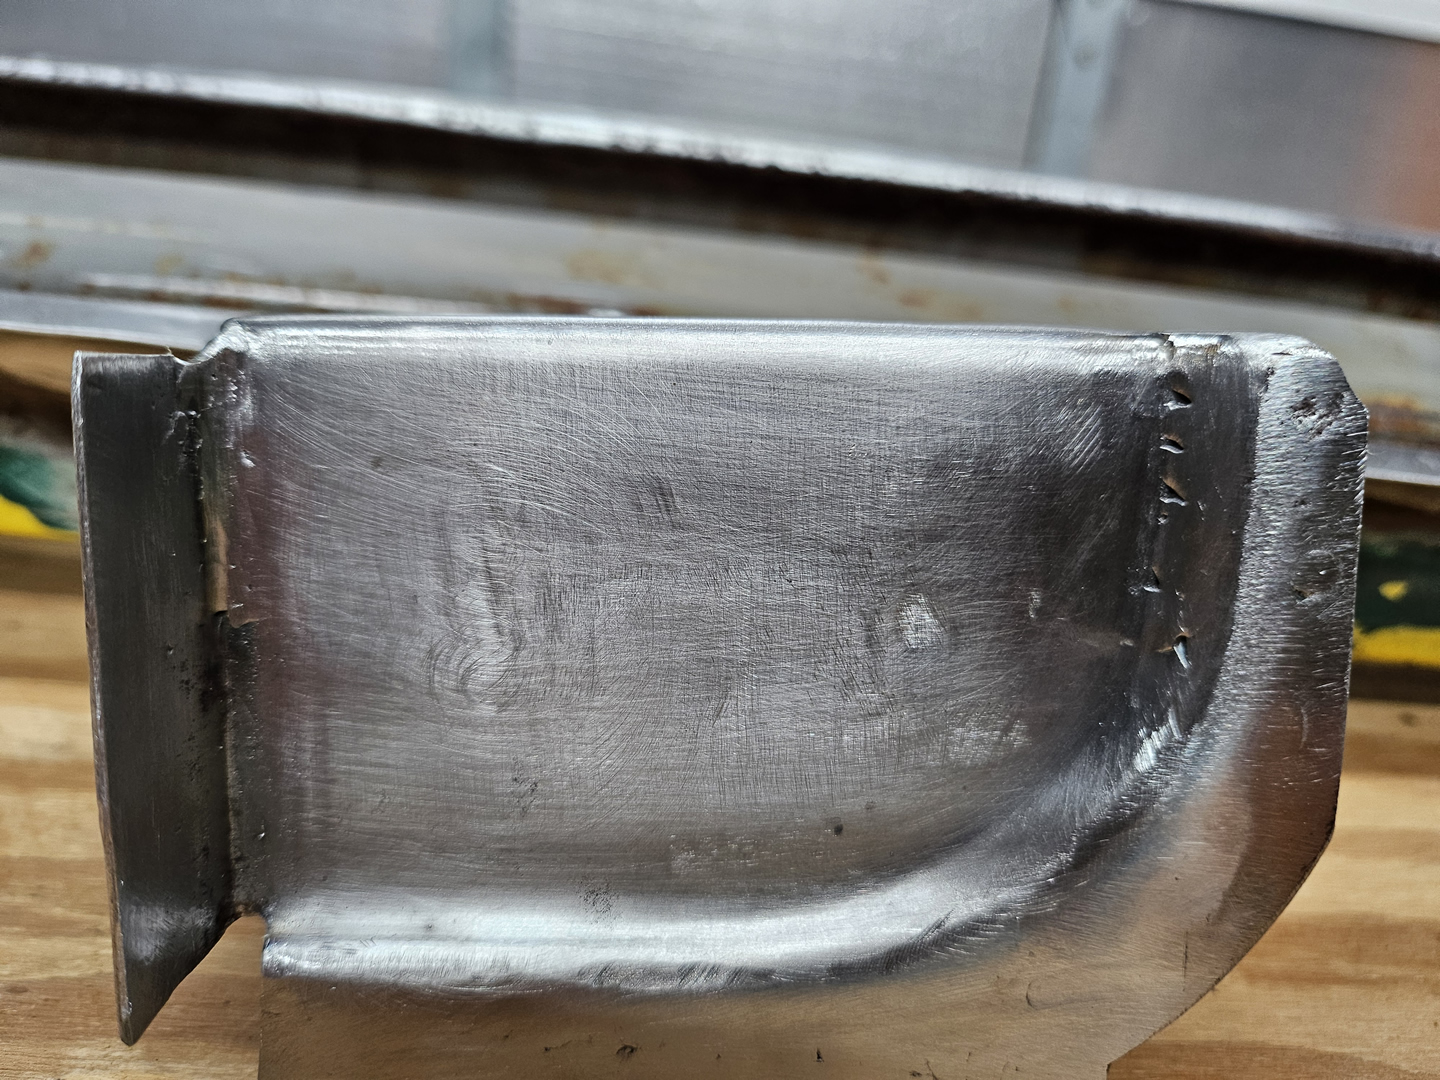
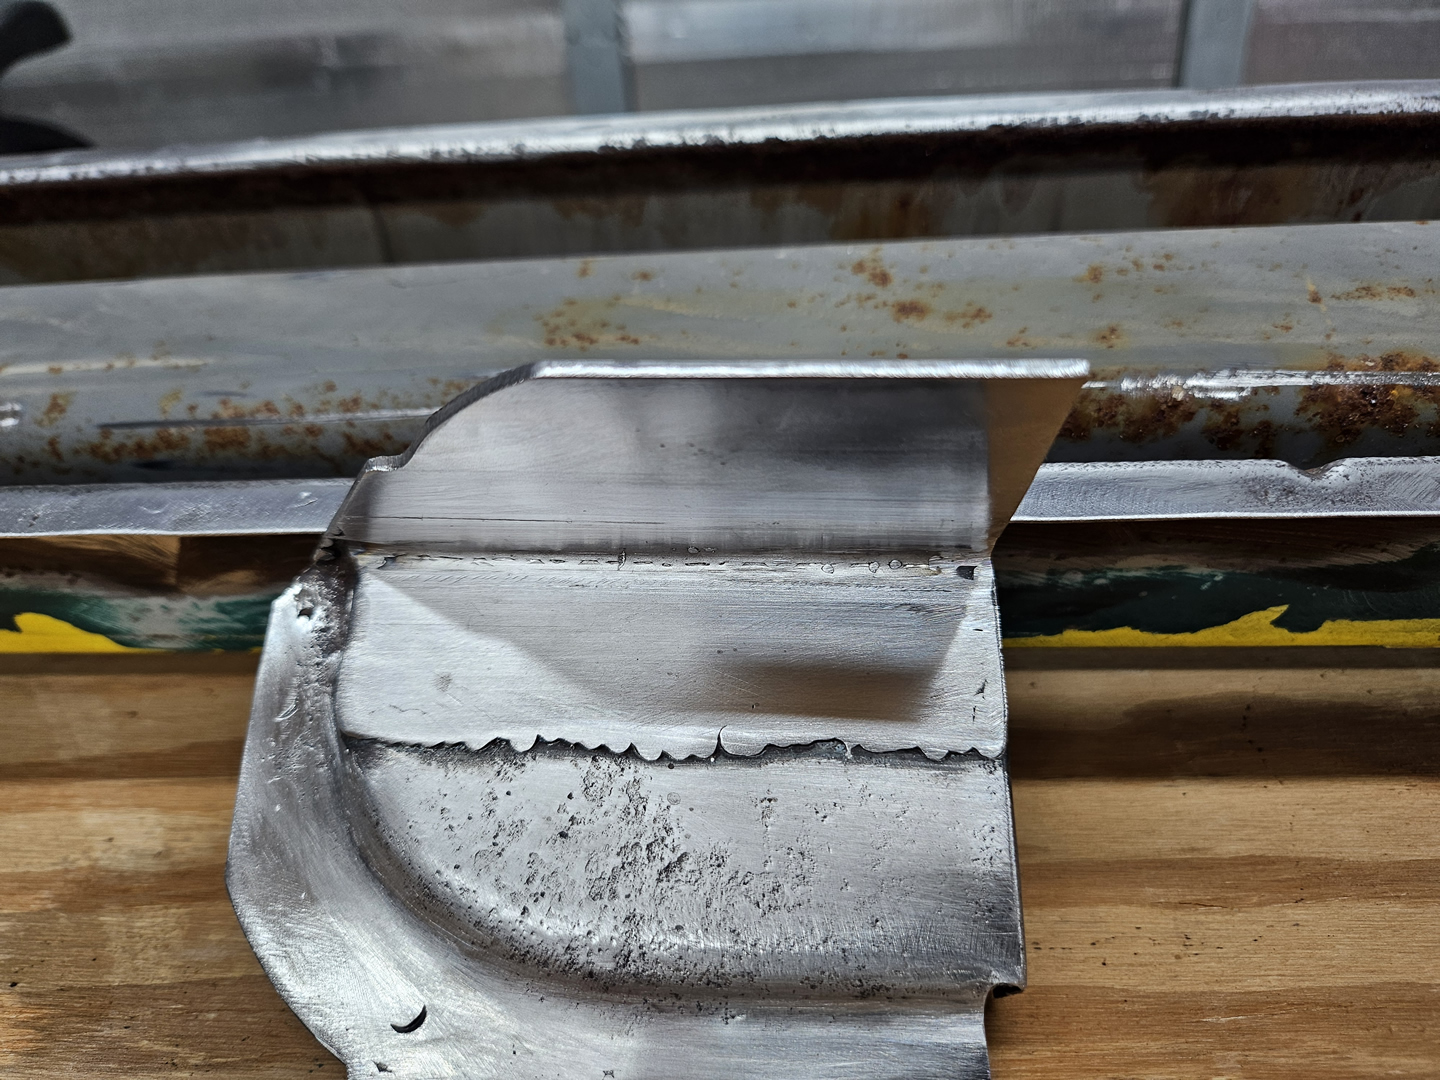
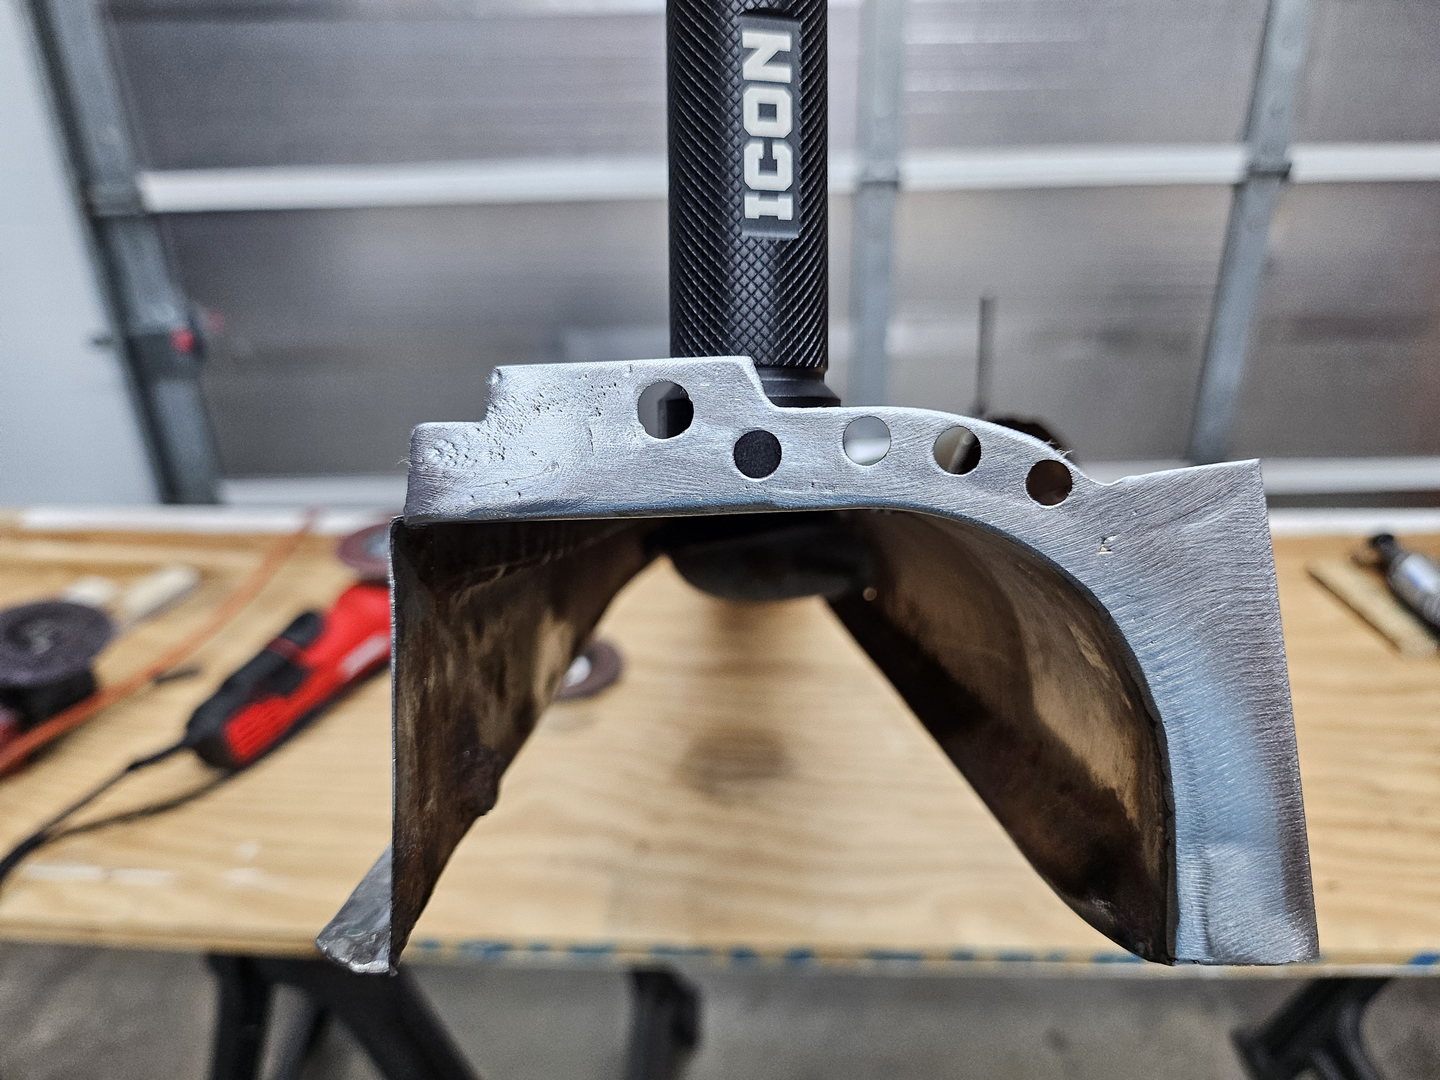
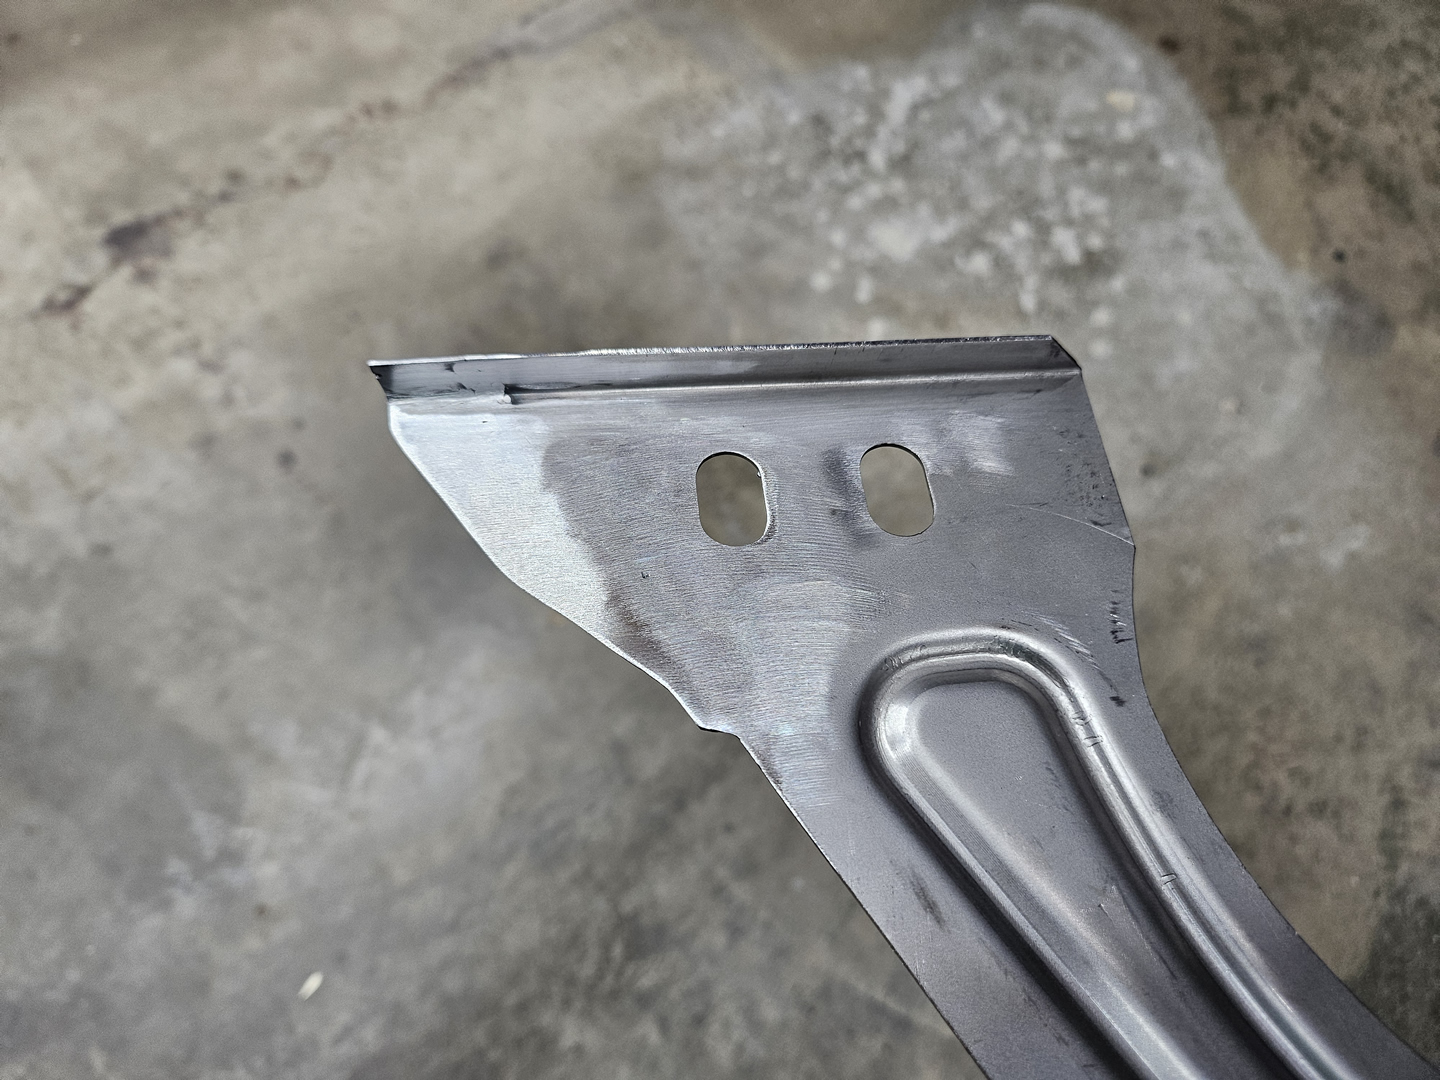
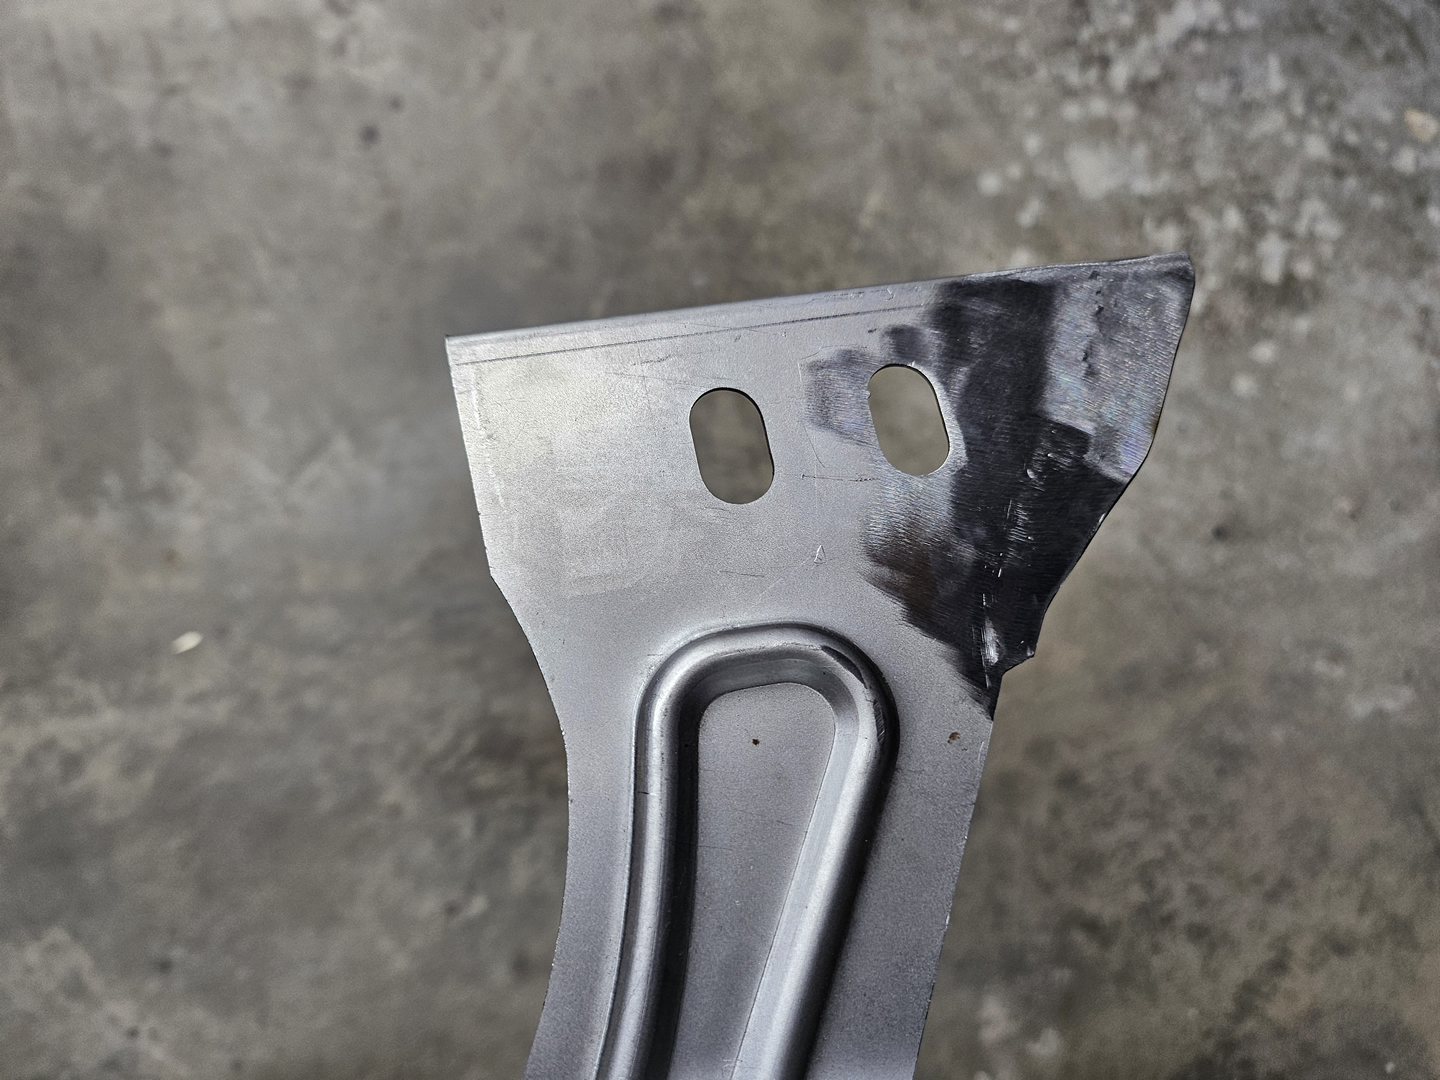
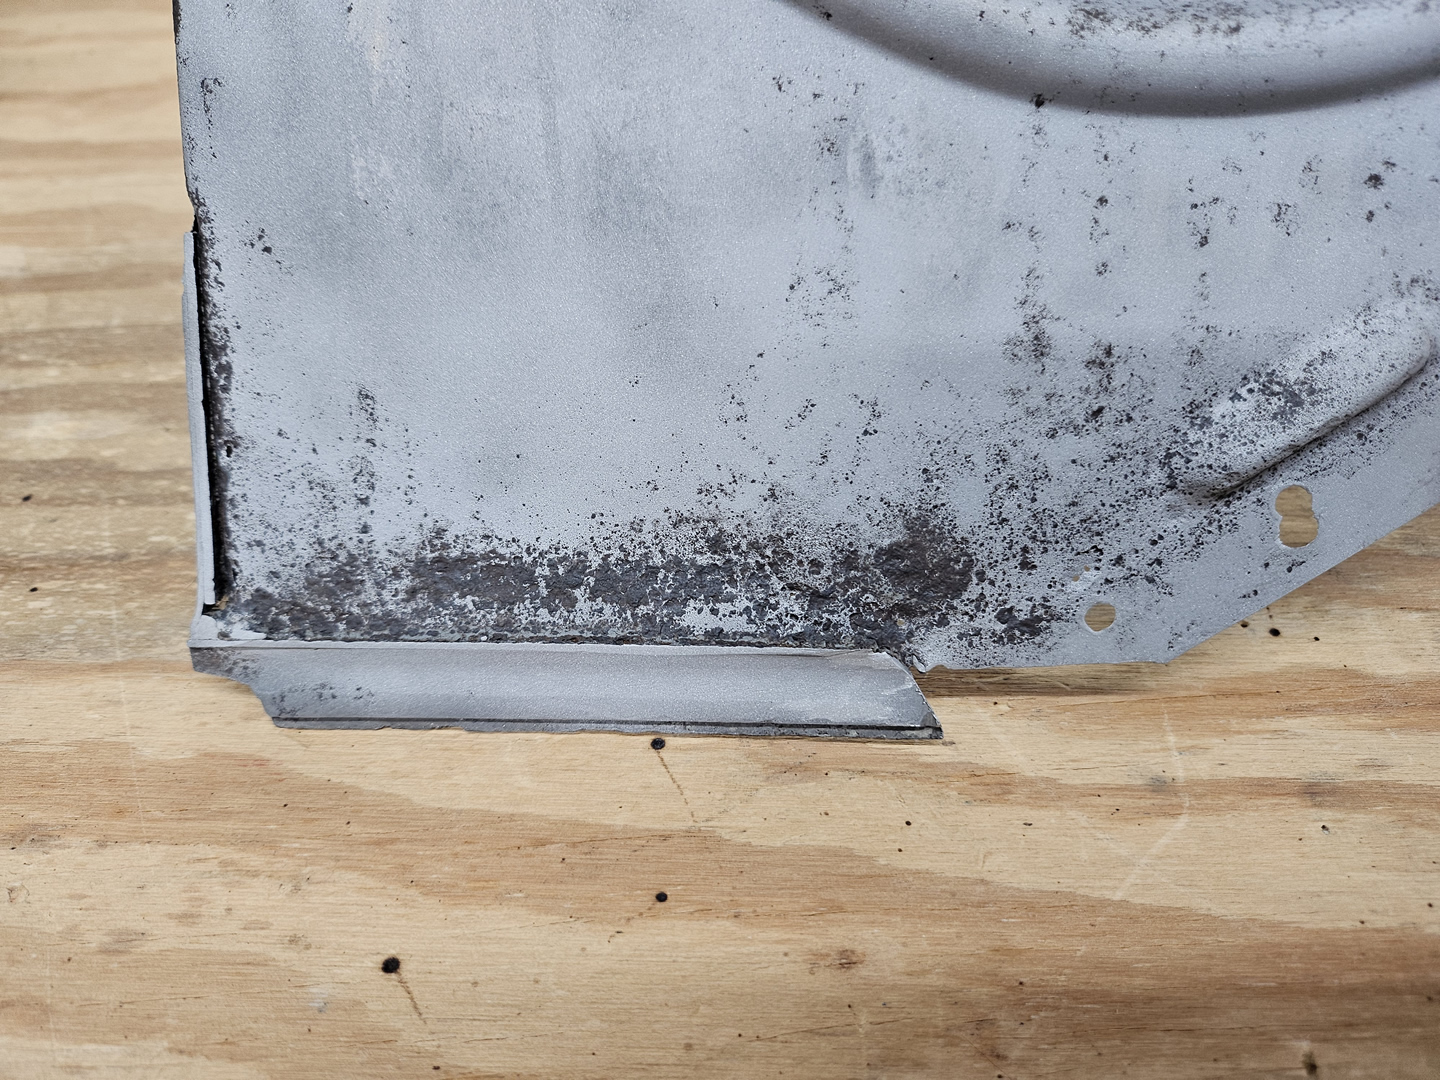
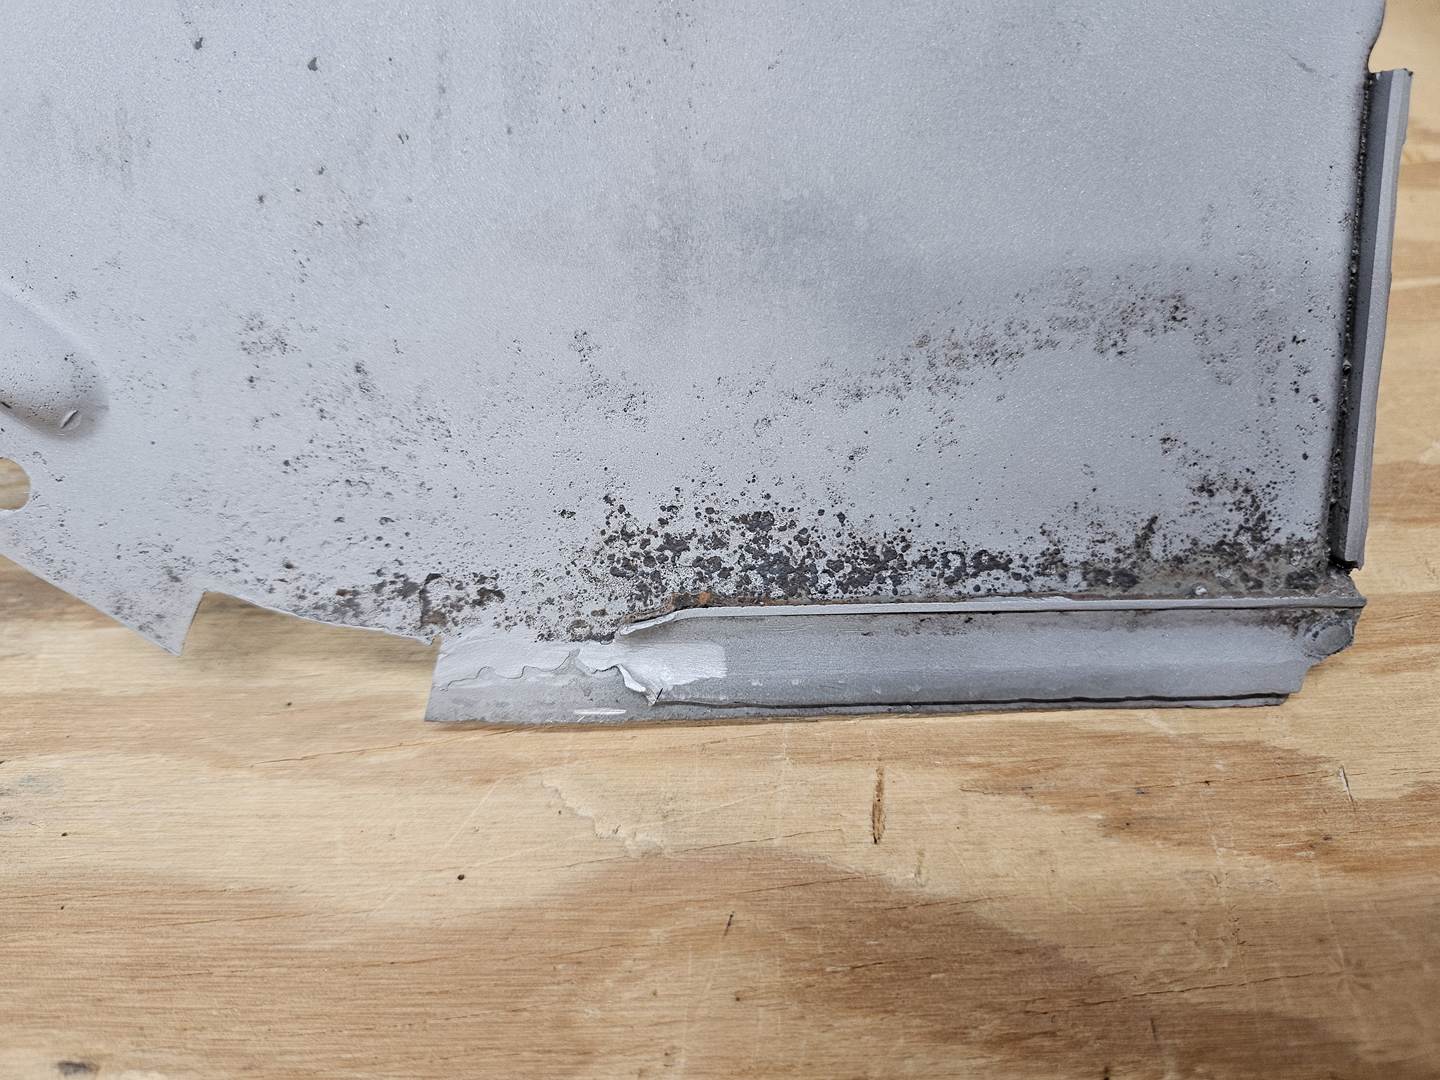
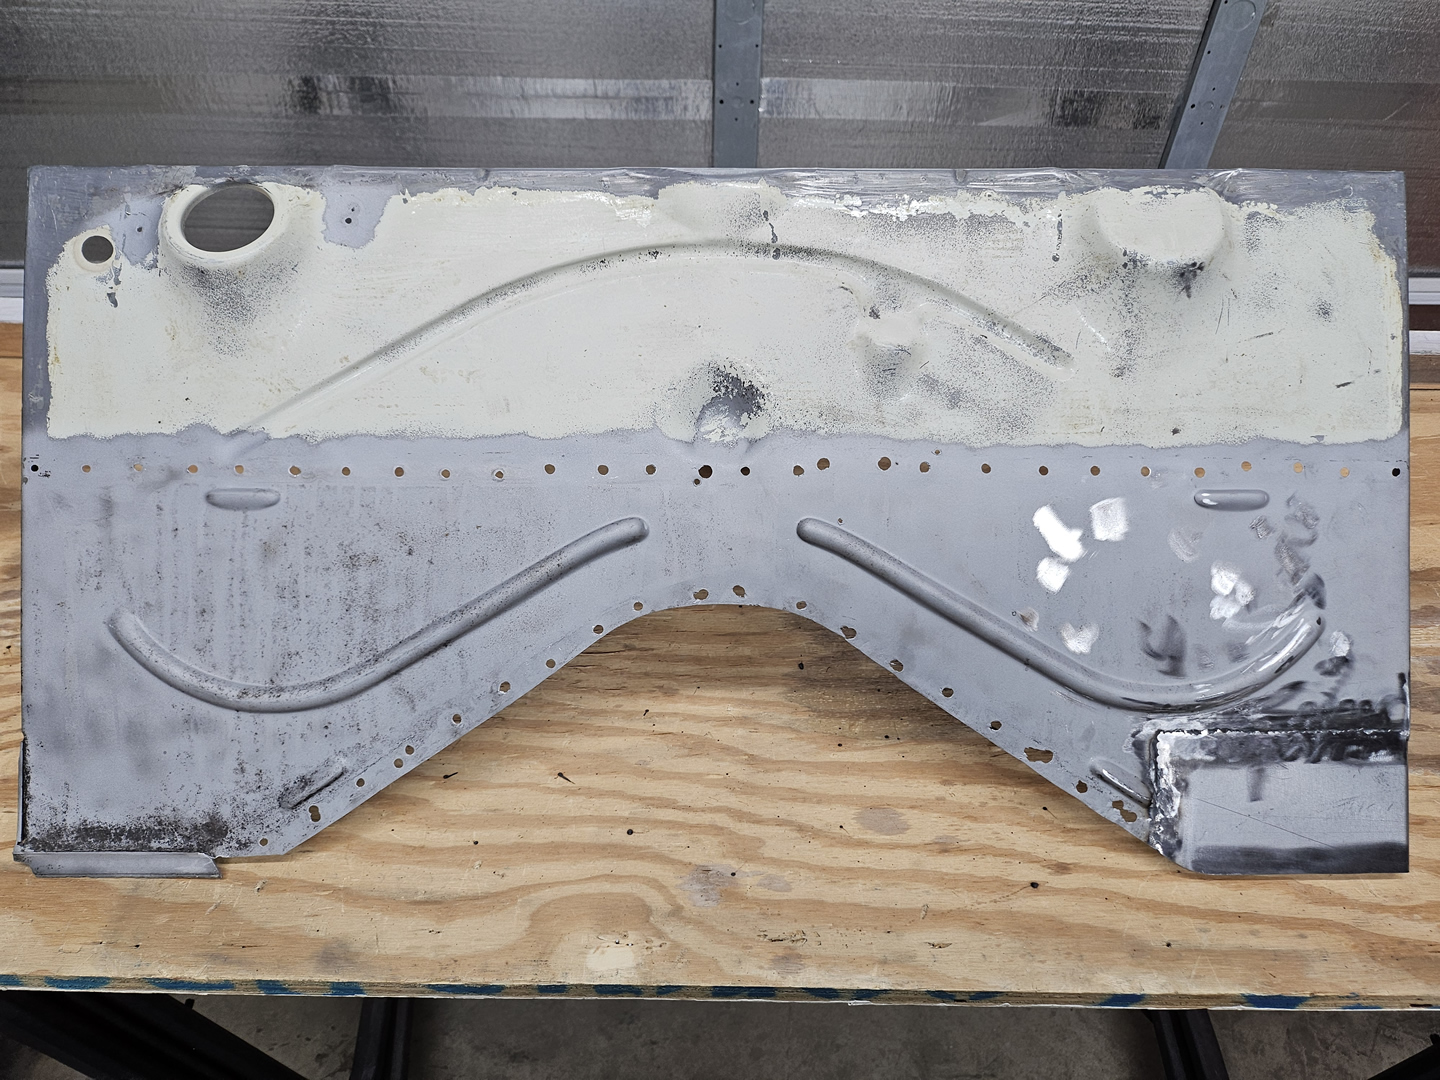
On the bottom plate for the passenger side channel, I added a piece of metal to flare out the inner side of the front edge. Both heater channels had this flare on the inner sides and I am matching what they had originally. This area is seam-welded to front firewall. I'm not sure if this is necessary, but test fitting the channels to the front firewall indicated that this would help to have more metal to seam weld this weld joint. I made the piece oversized and I will trim it later after the bottom plates are welded on and then when fitting the panels.
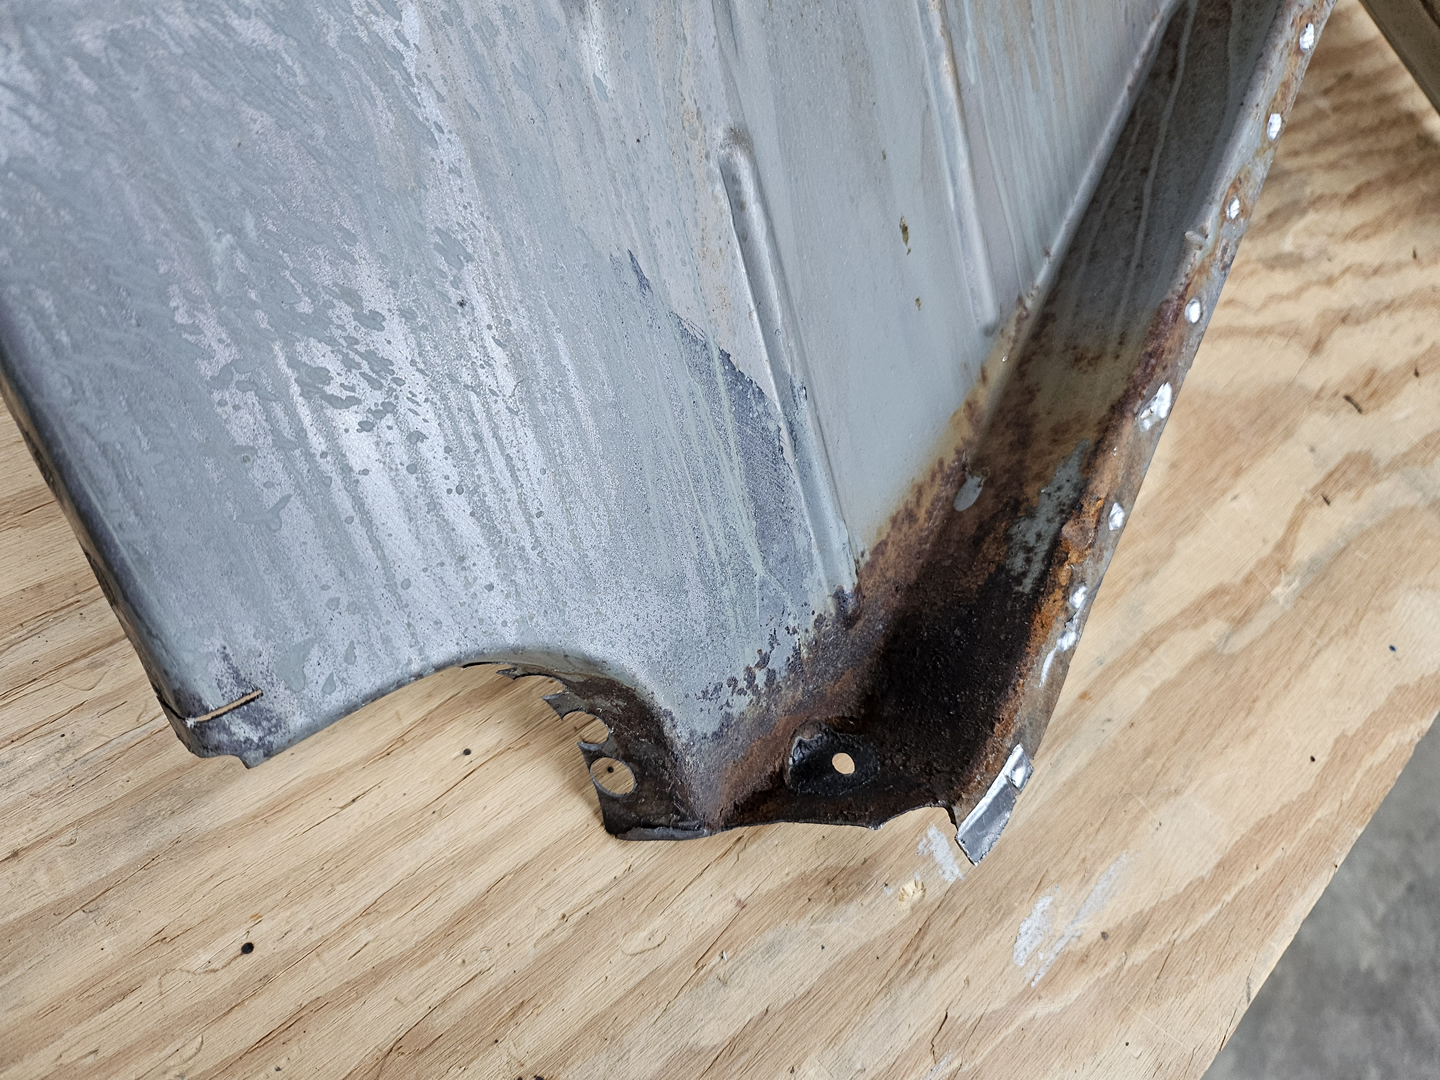
Now on to the driver side heater channel. I removed the bottom plate and again, it took several hours to grind out the spot welds and peel off the plate. This side has way more rust and quite a bit of rust damage on the front end. I will have to make and replace a few areas and will need to remove the front end cap and rebuild it. I welded up any scars from the spot weld cutter when I removed the remnants of the panels when I first got the channels, and also welded up any carpet nail holes. This channel also had many unneeded holes in it, and I filled them as well.
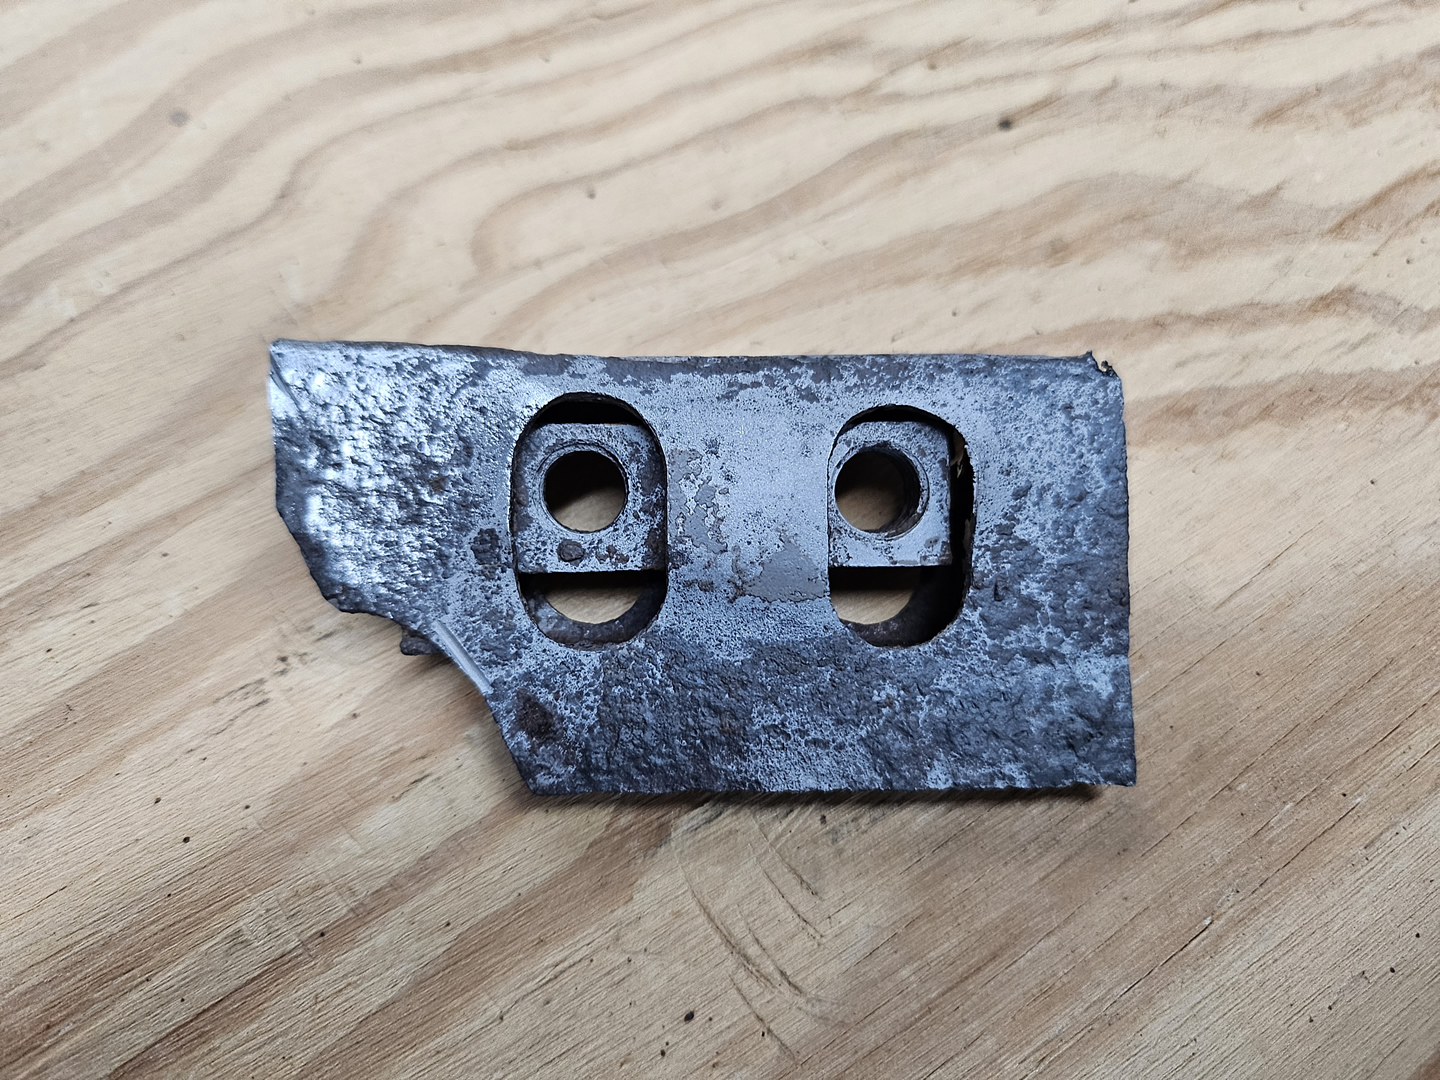
I removed the end cap and it is in very bad condition. I sandblasted it just so I could tell just how bad the rust damage is. I will definitely need to cut out a section of it where the threaded plate and its cage are attached, as well as replacing the cage and the threaded plate.
So I cut out a section of the worst damage and fabricated a new section. The original section was 18-gauge, but I used a piece of 14-gauge material just to make it a bit stronger. I also filled in the holes I made with the drill bits when removing it from the body of the channel.
I also welded on a piece where the flange had been cut off when the channel was removed from the donor car. I will trim it once I weld it back on to the channel body.
I did the same and repaired the front flange on the channel body.
And I repaired the flange on the rear end of the body as well.
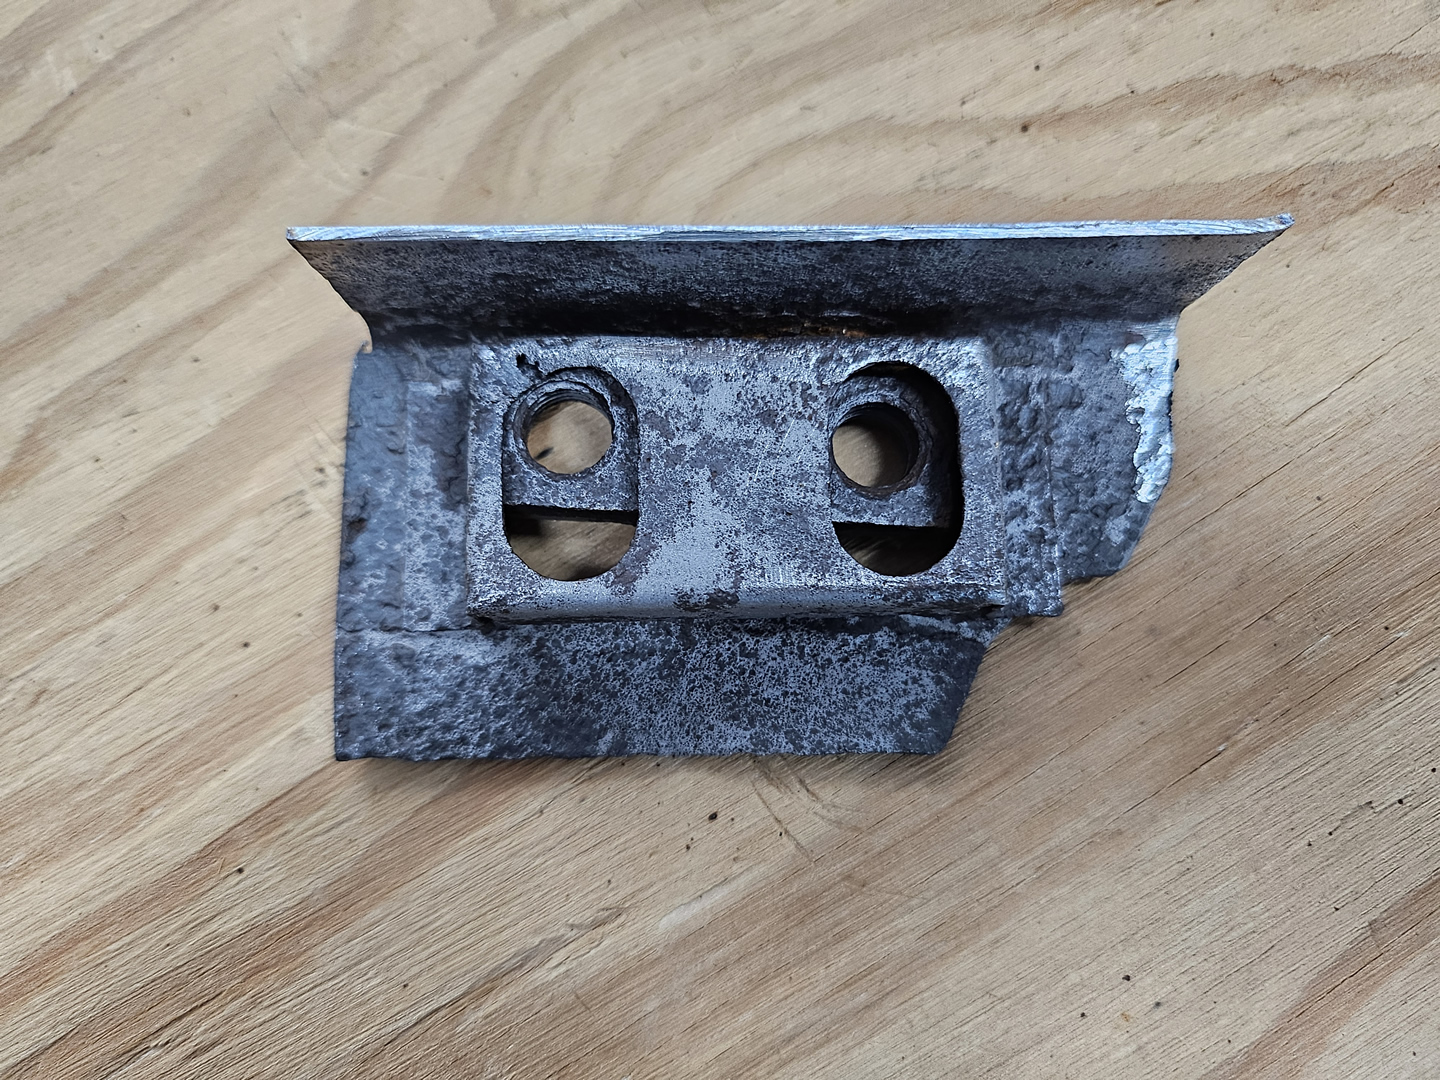
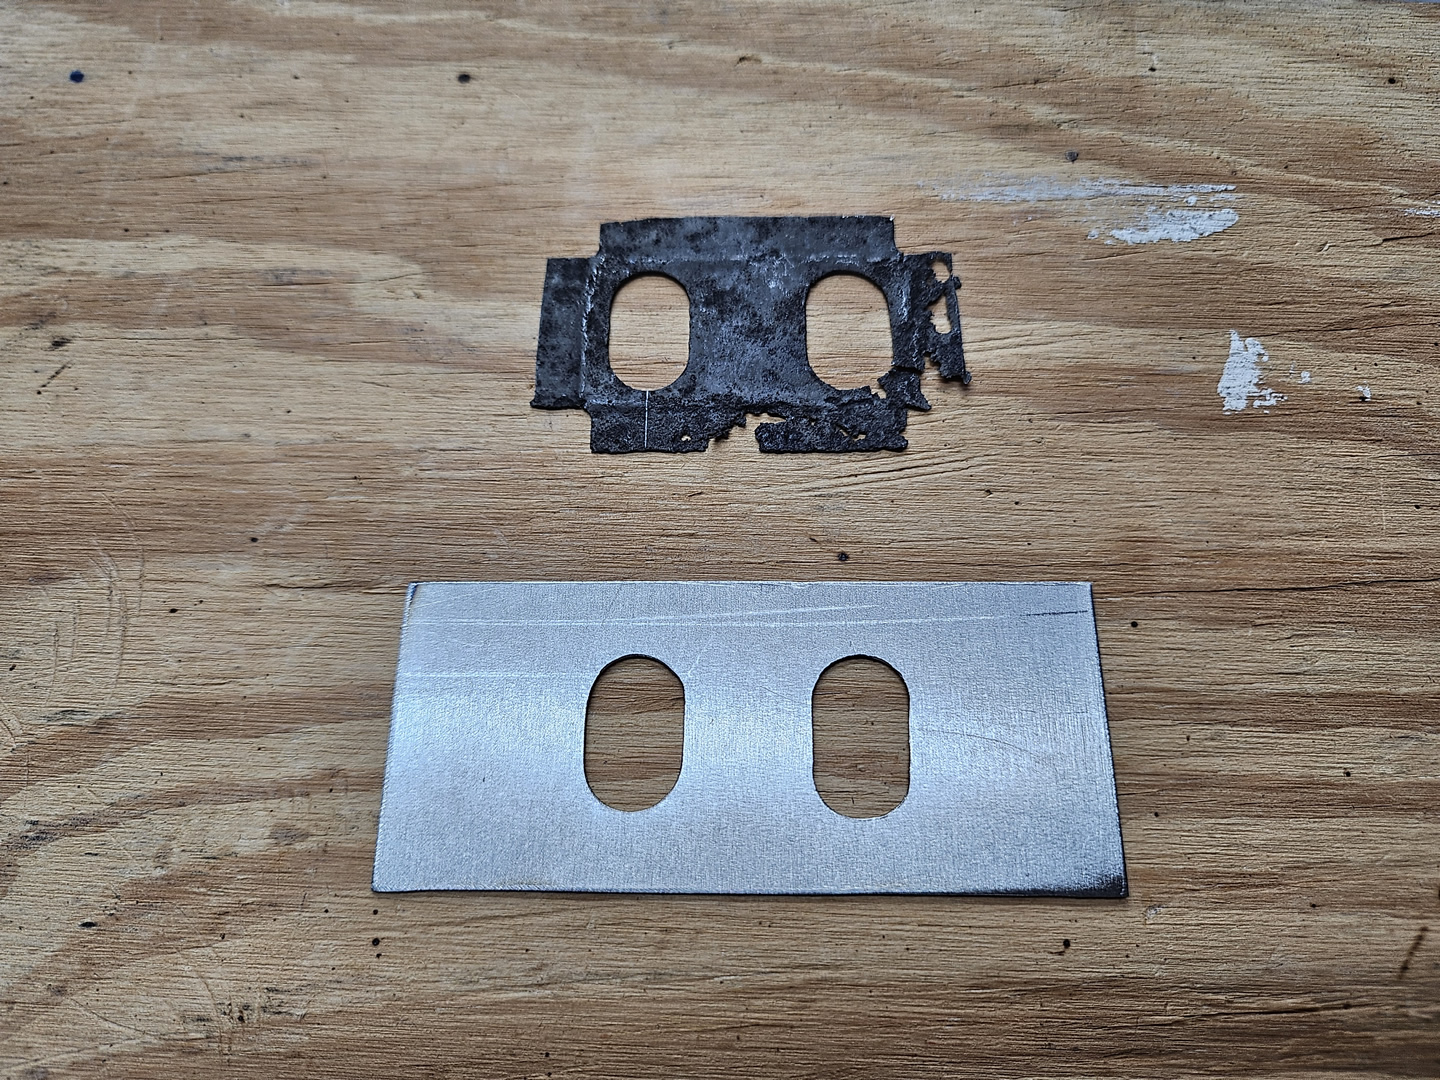
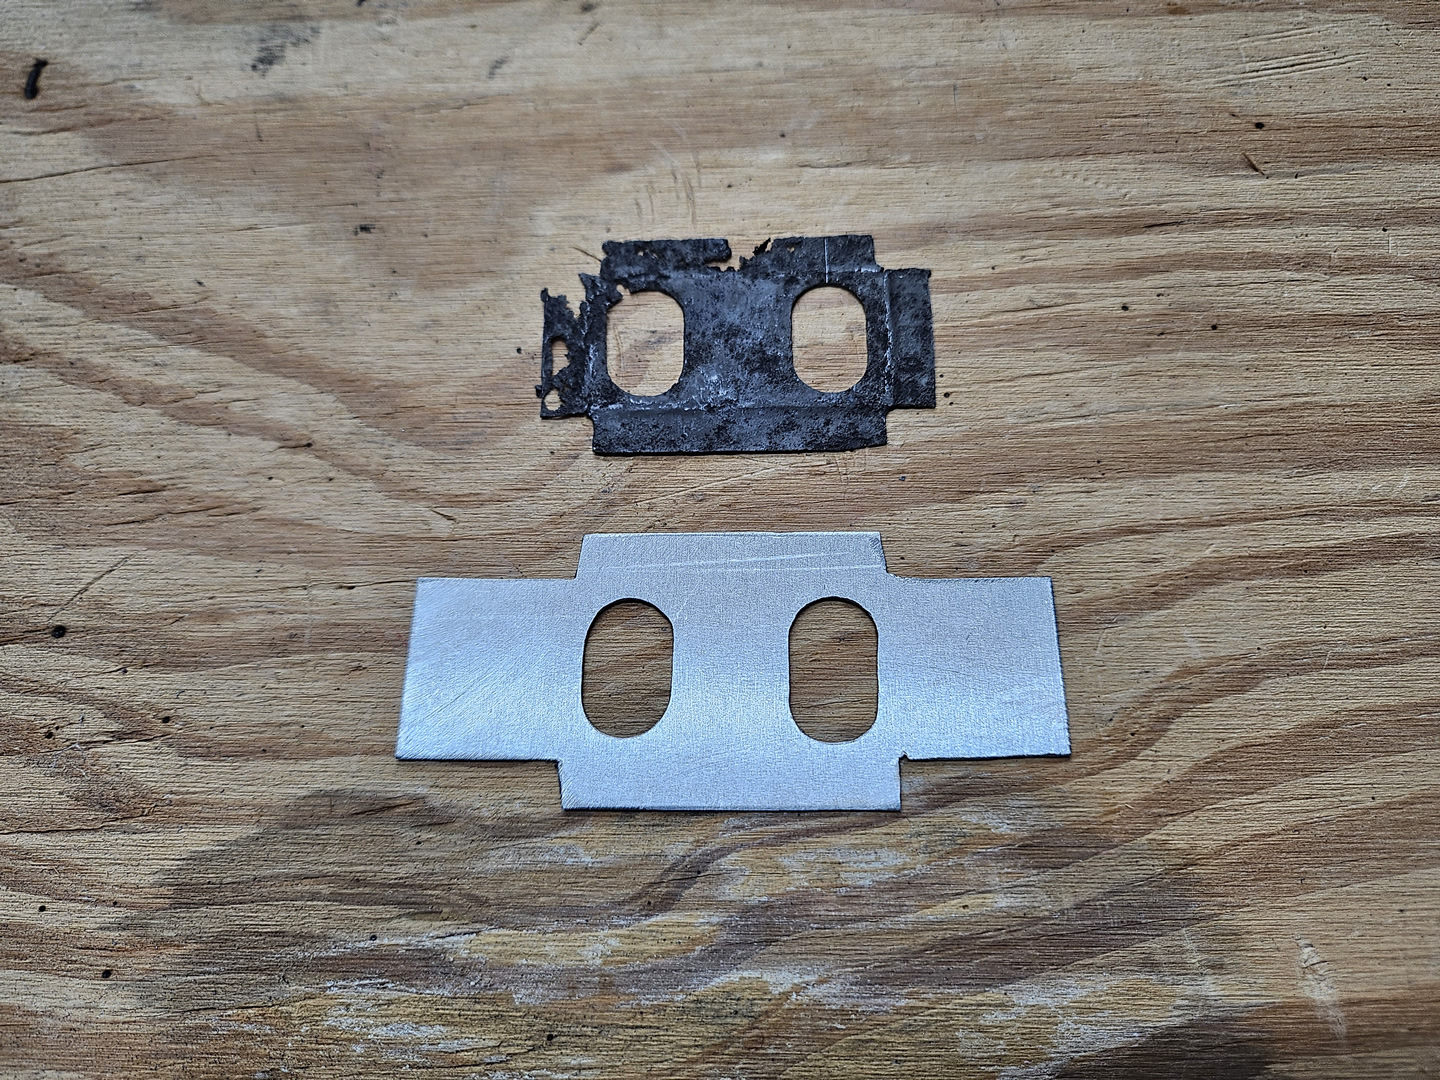
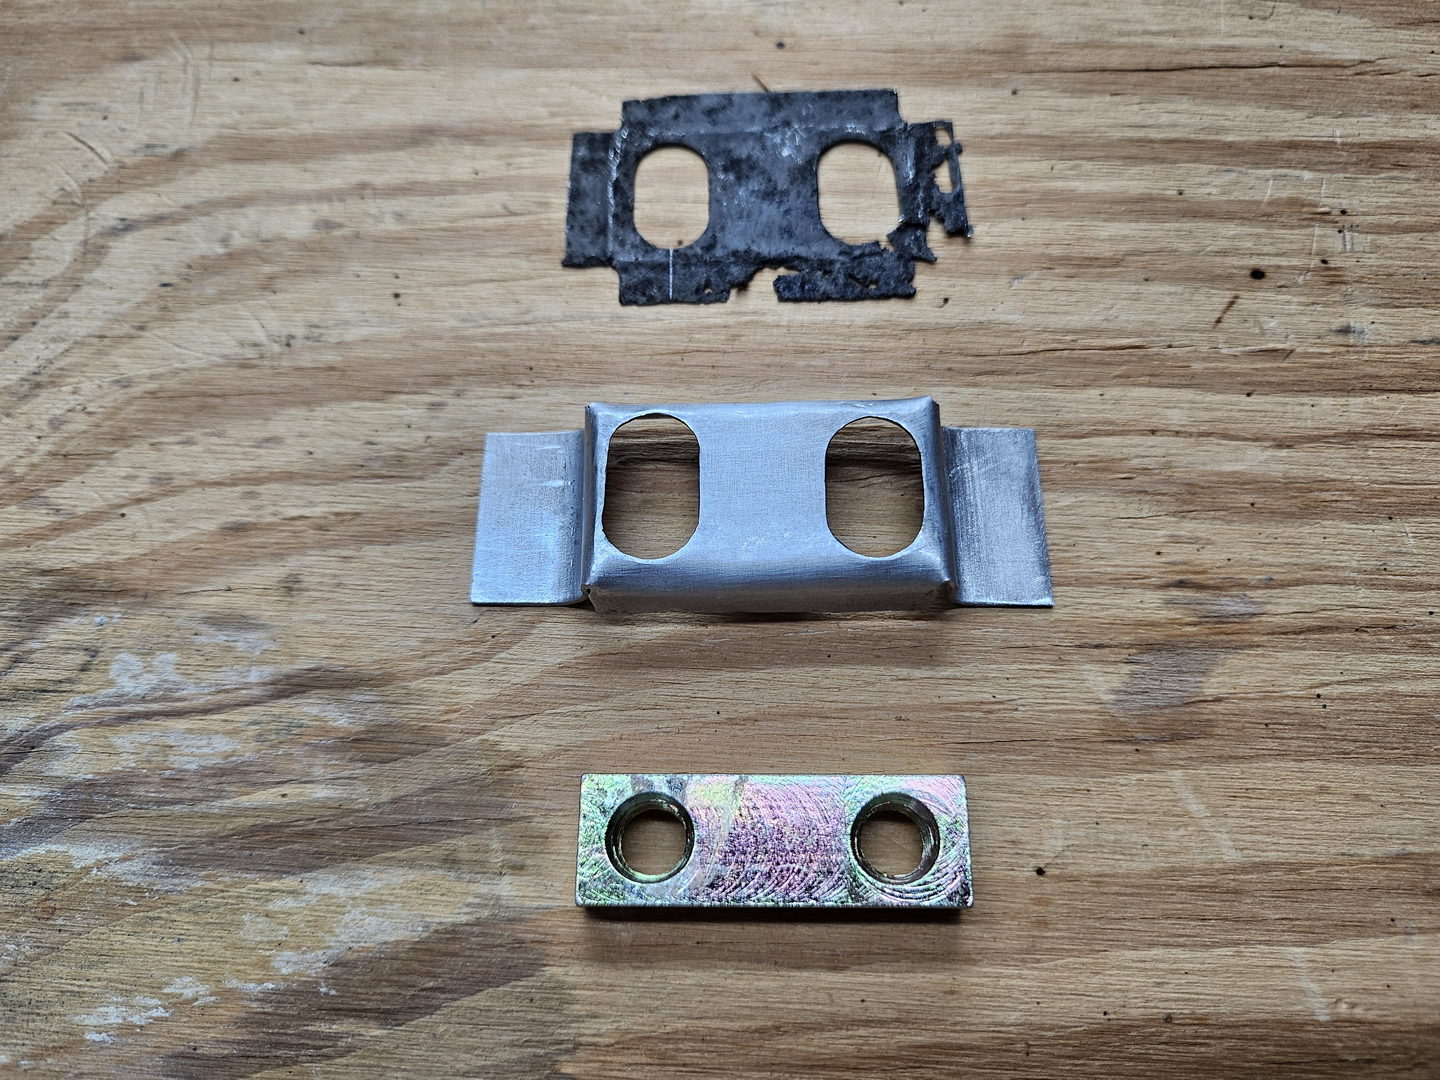
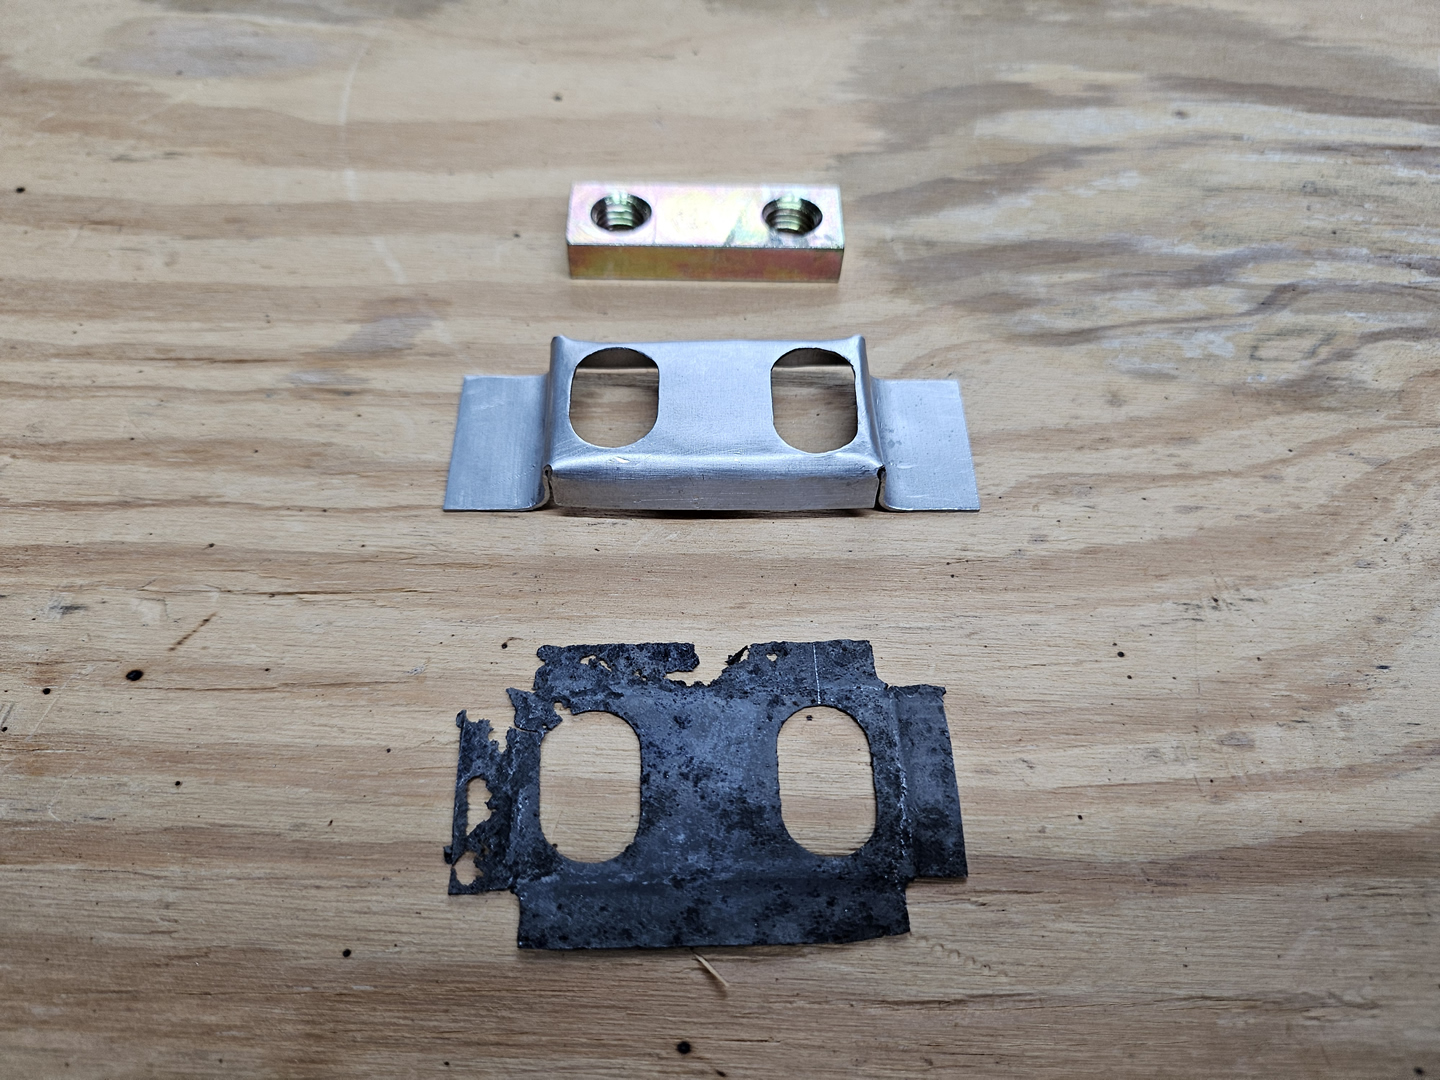
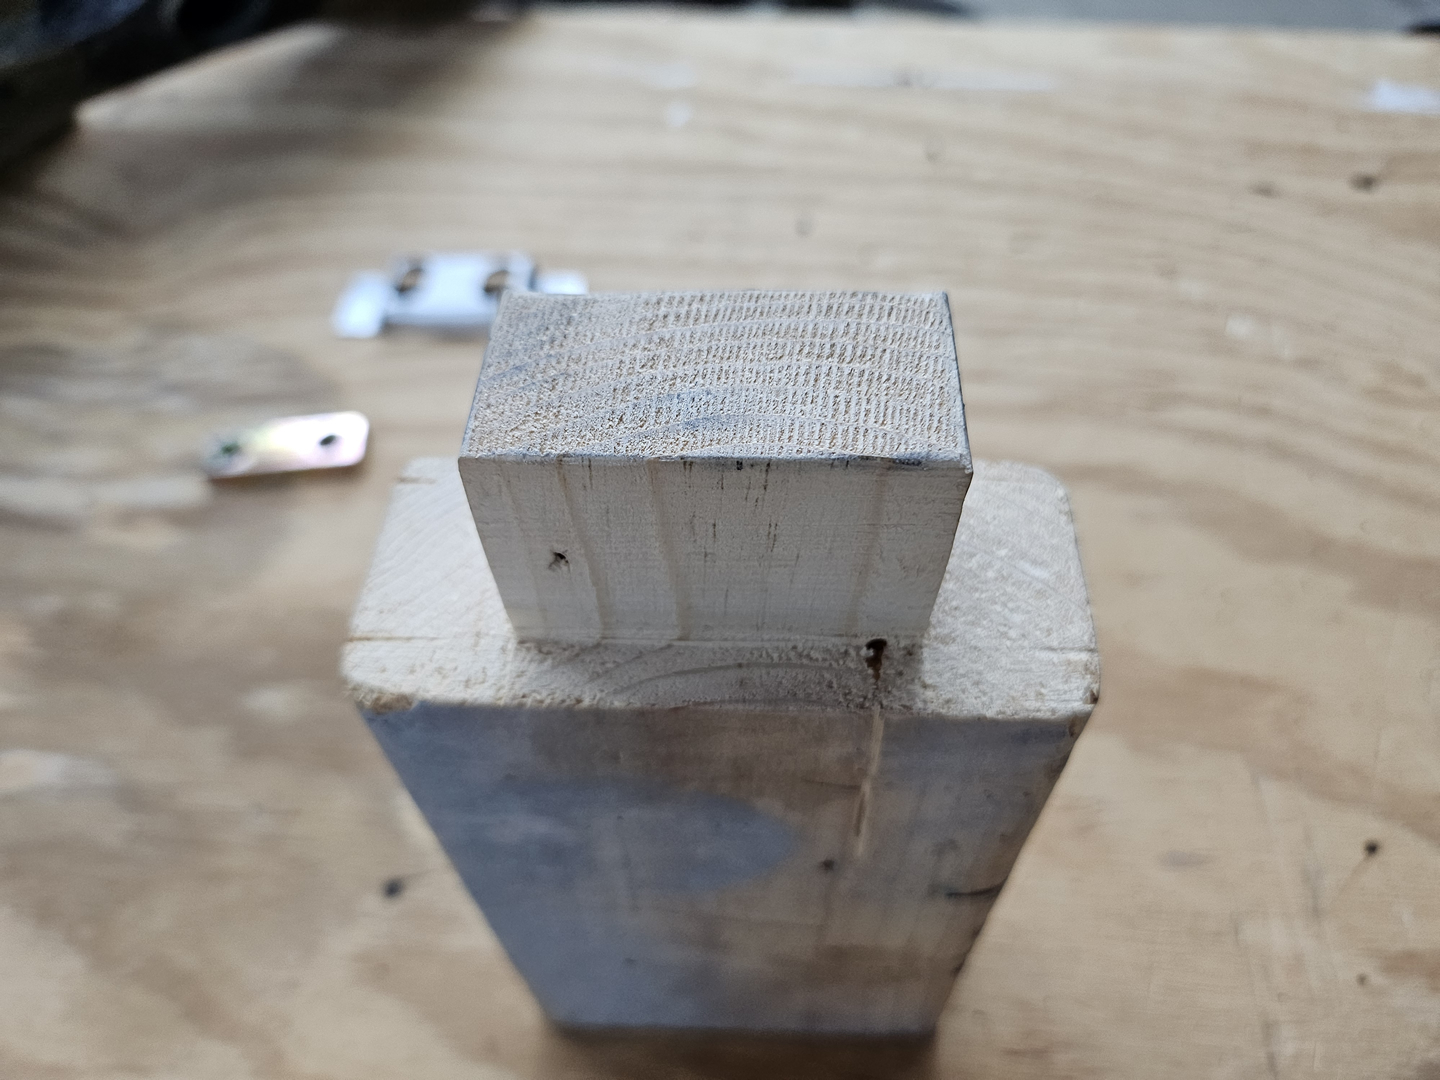
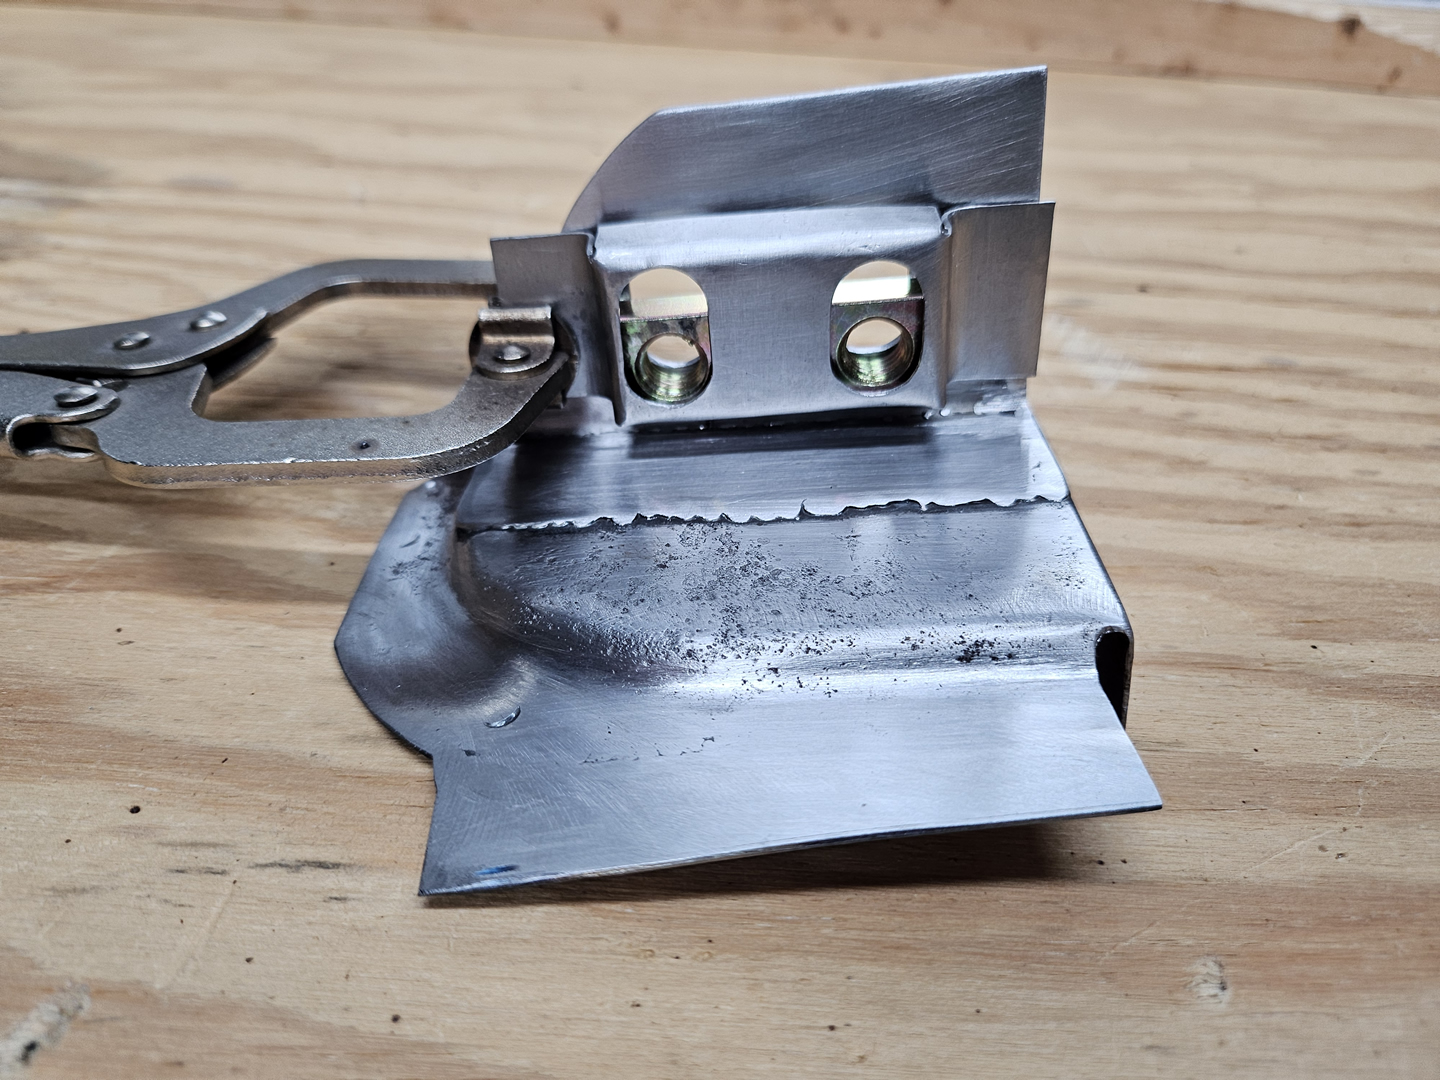
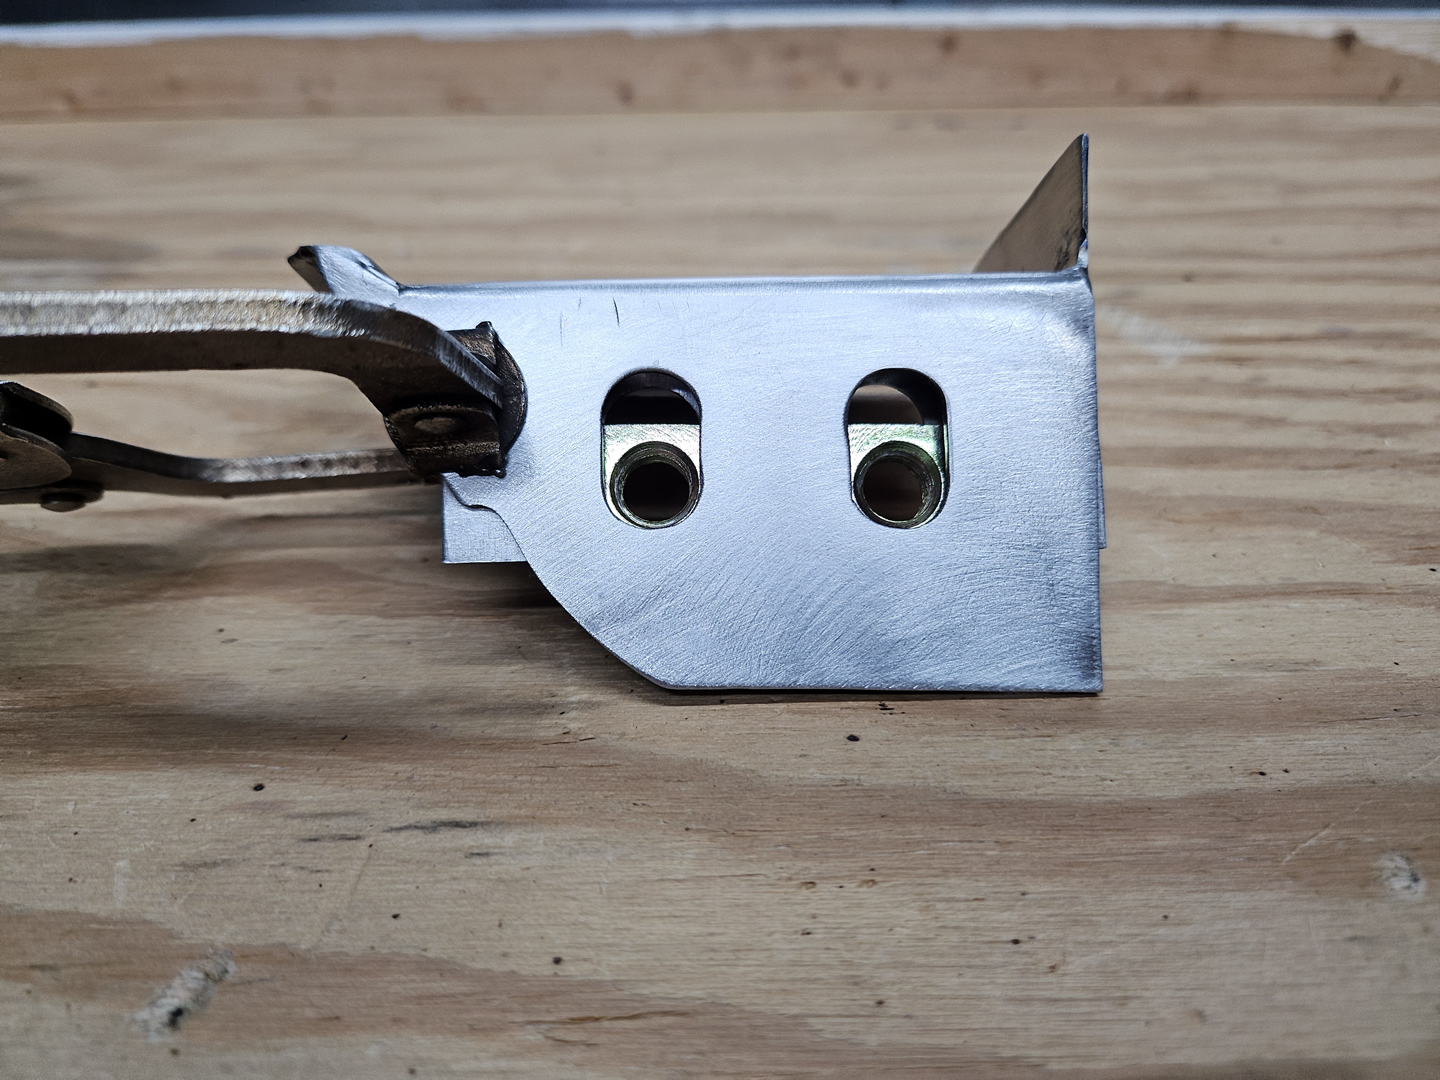
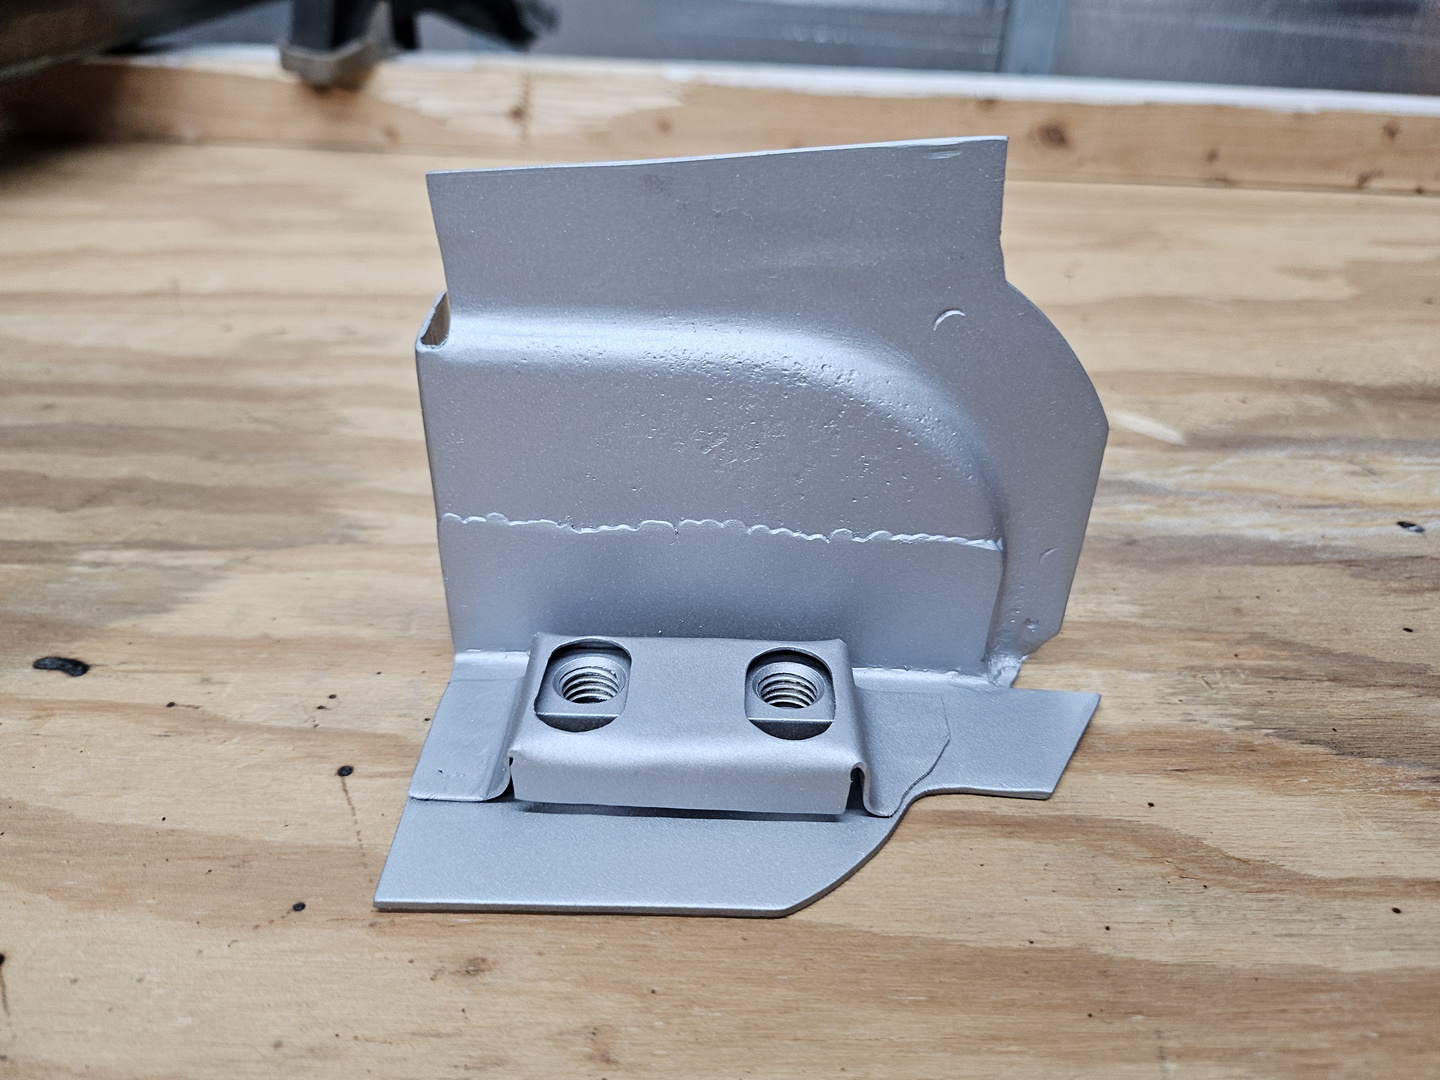
Since I couldn't find anyone in the US that was selling a replacement threaded plate cage, I decided to make one myself. I cut off the original one and flattened it out to help determine what pattern I would need to replicate it. I made a wood form or buck to help shape it, and it did help a little. I made the cage out of 20-gauge metal and it was a little too thick to bend over the form. I basically used pliers and a small hammer and was able to get it fairly close to the original. I made it the same dimensions as the original, but the replacement threaded plate was a little wider than the original plate. I had to take a little metal off of the ends of the plate and then it fit. It doesn't have the same amount of side-to-side play in it that the original one did and hopefully that will not be a problem. I will have to remember that when fitting the channels to the body. I sprayed the mating pieces with weld-through primer and welded the cage onto the end cap.
Next, I decided to tackle the rust damage on the channel body. There were a few areas on the front where the bottom plate is attached that had small holes, but there was good metal around it and the flange where the bottom plate is attached was undamaged. In those areas, I welded up the holes and any pits around them. However, on the inner side of the front section, there was whole area of the bottom plate flange was eaten through with rust as was an area 1/2" above it. This area had many different contours and shapes, and I decided it make it in three sections to simplify the process. It took some time, but I did get it done.
Now I can put the end cap back on. I sprayed the mating surfaces with weld-through primer and welded it back on. It has been a lot of work repairing the rust damage on the driver side channel, but it was definitely better than spending $500 for a suitable replacement.
This leaves one last difficult repair task on the driver side channel. Whoever had the car that this channel was removed from at some point welded up the holes and captive nut for the running board bolts. I was able to locate the centers of the nuts and drill out and tap all four of them. If I could have accessed them from the inside of the channel, it would have made this an easier task. But the heater pipe is in front of three of the four nuts and I was not going to remove the pipe just for that. That would be much more work than drilling and taping the nuts from the outside, or even rewelding the holes and re-tapping them again if the first attempts were unsuccessful.
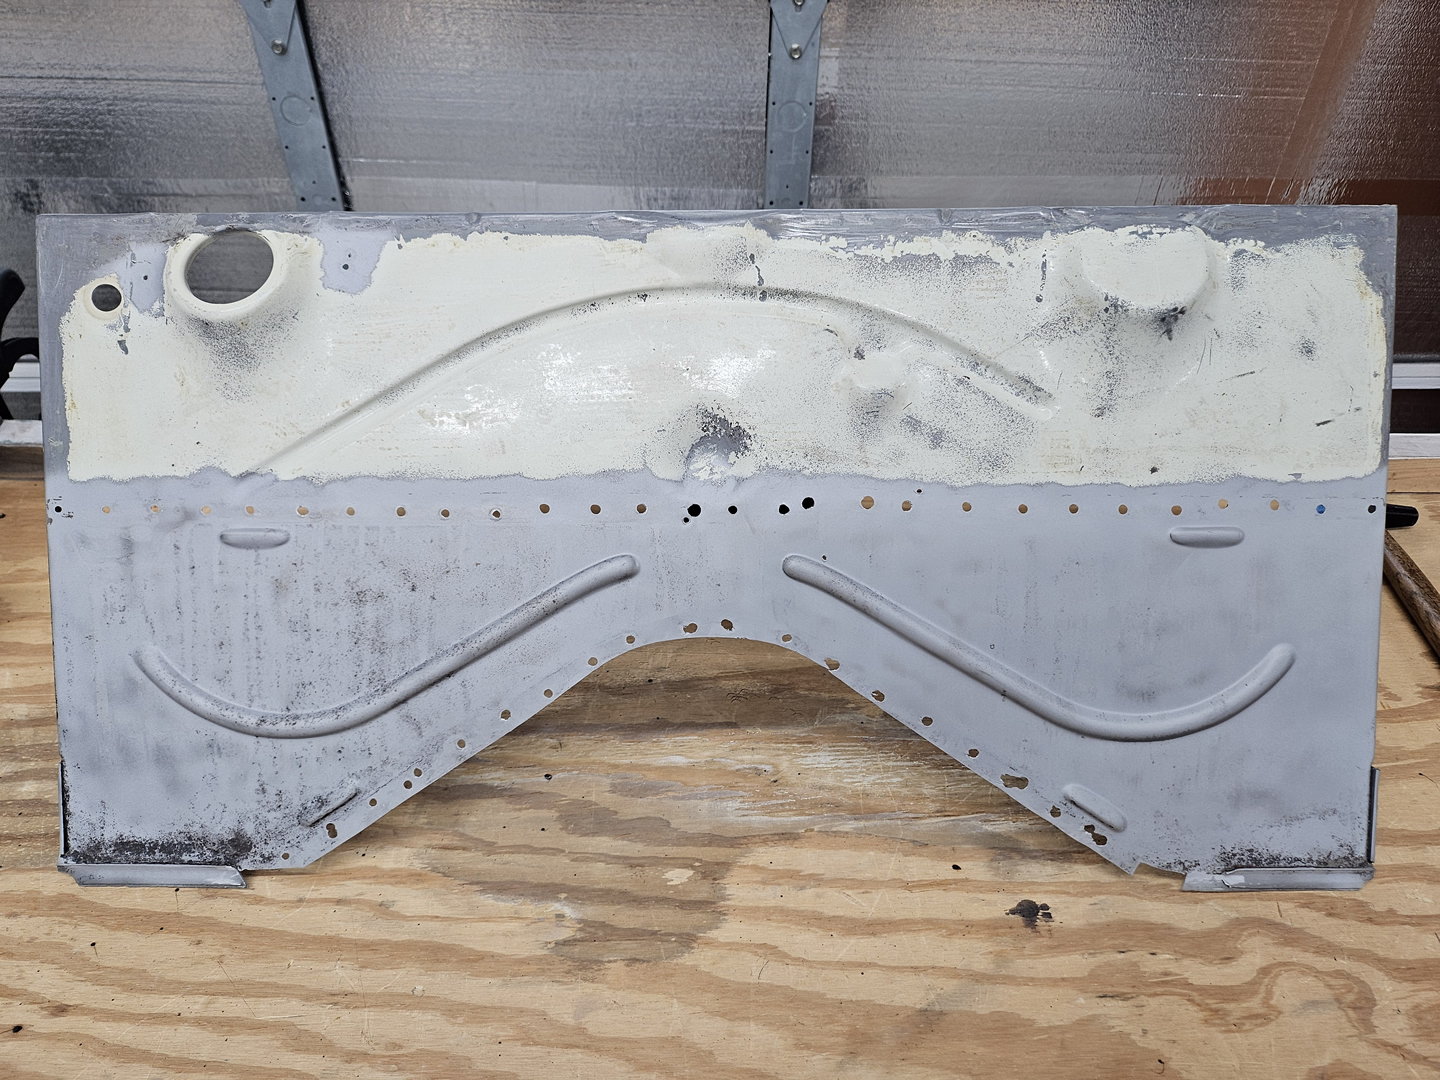
And before I can prepare the driver side bottom plate for welding, I need to add a piece on the inner side of the plate like I did on the passenger side plate to widen it to match where it will attach to the front firewall.
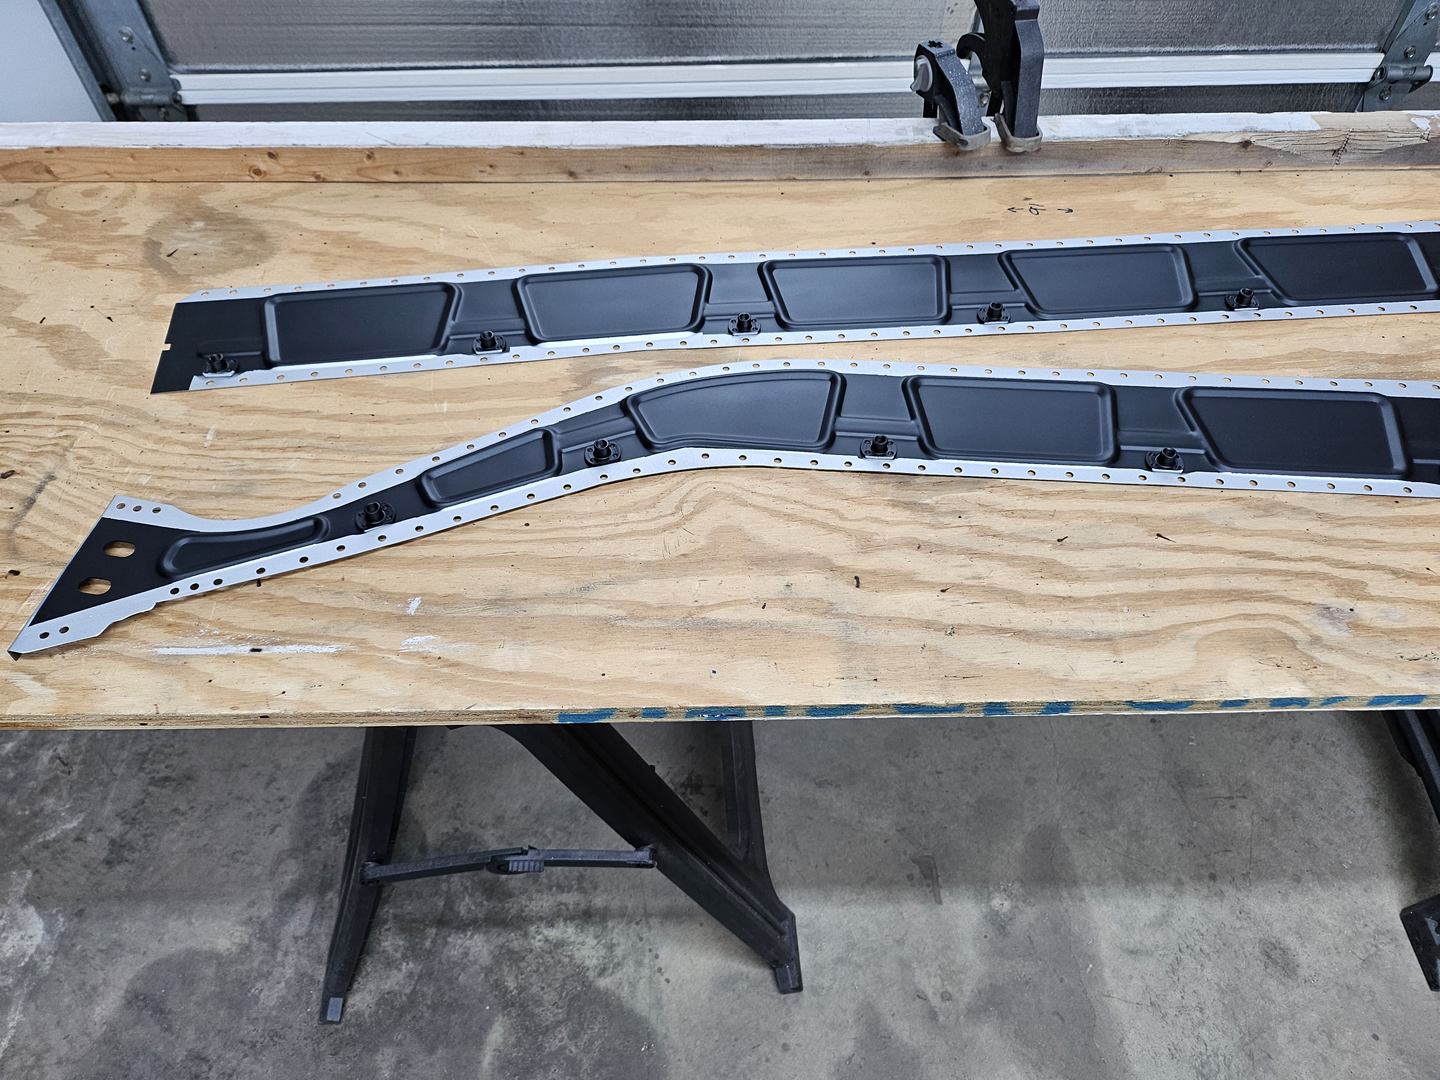
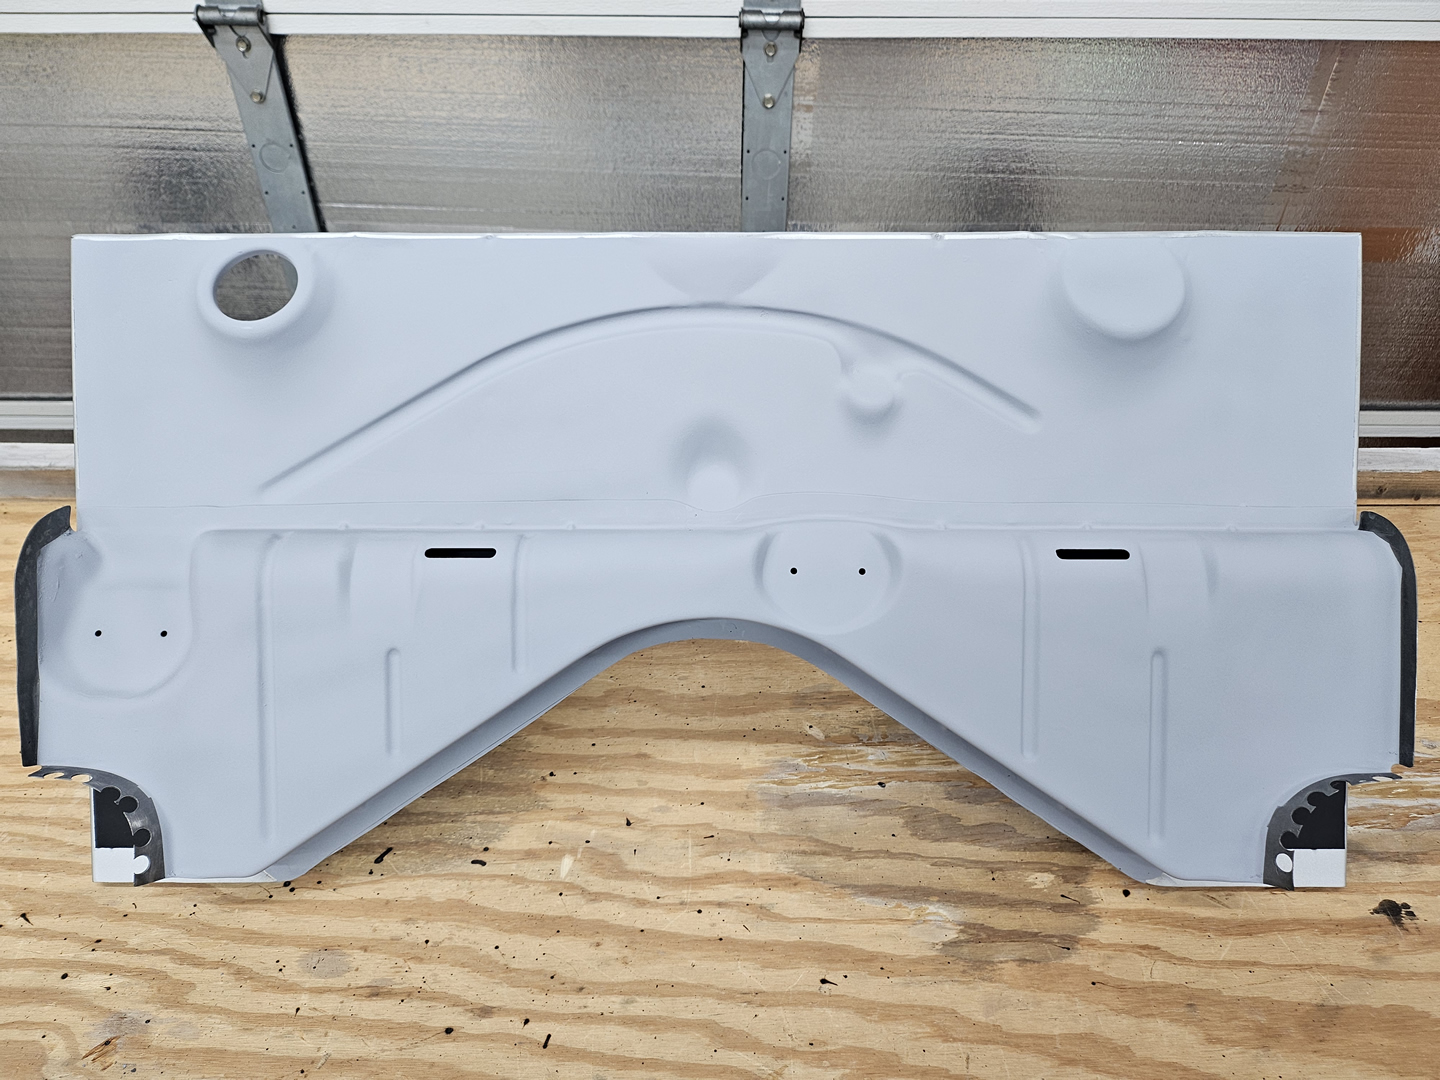
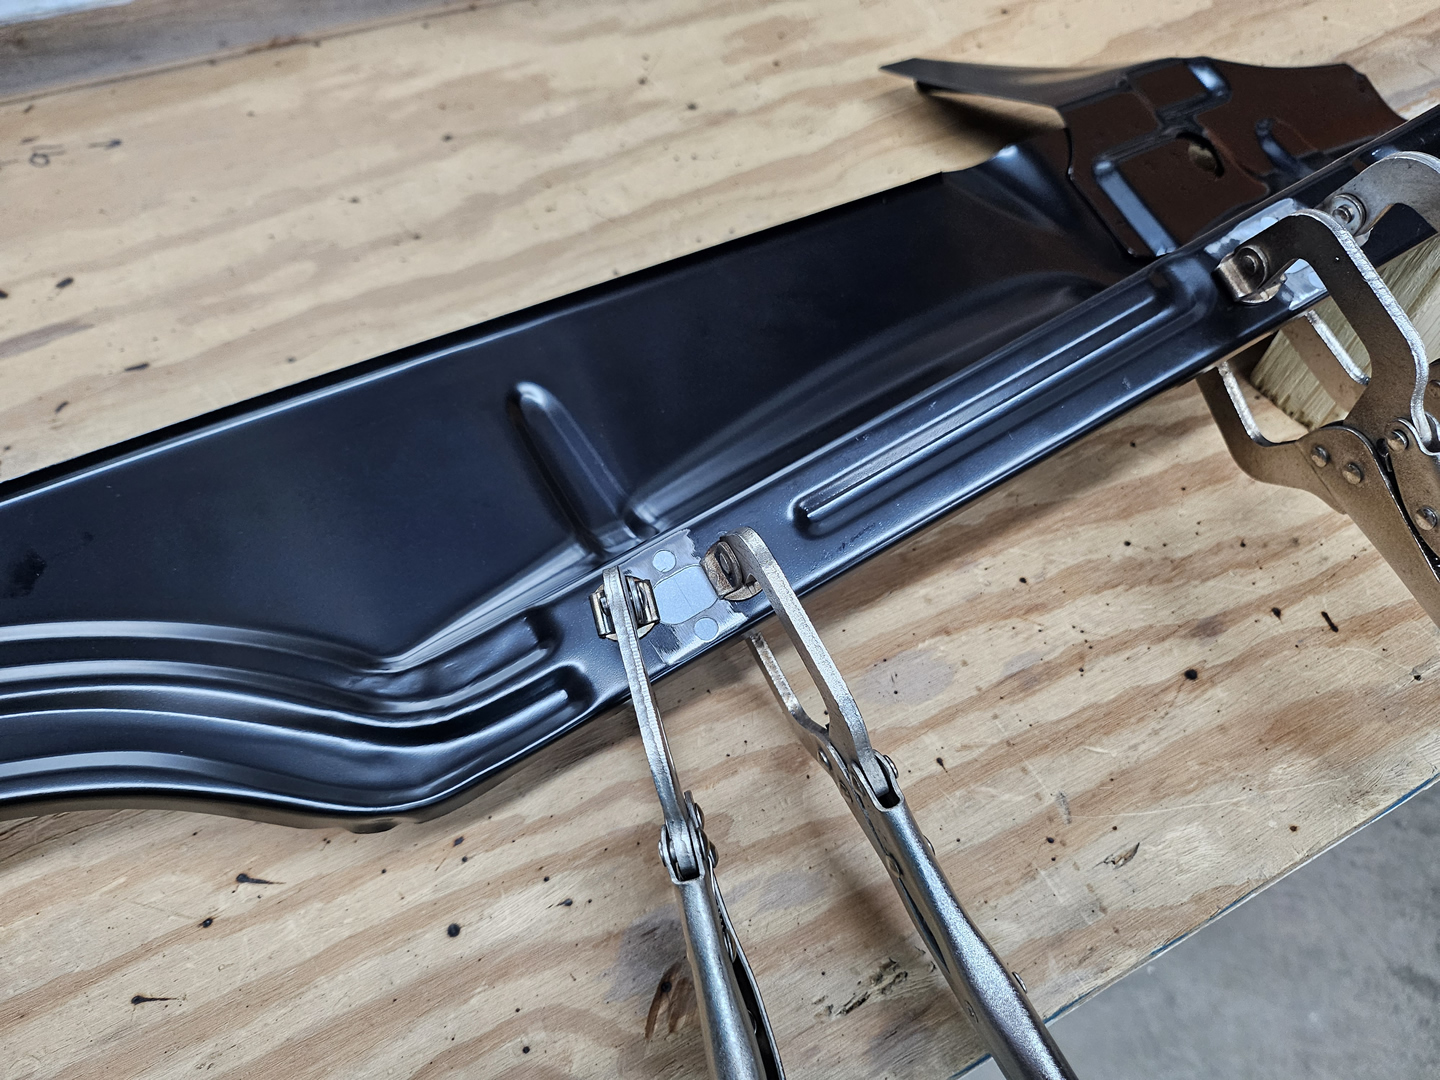
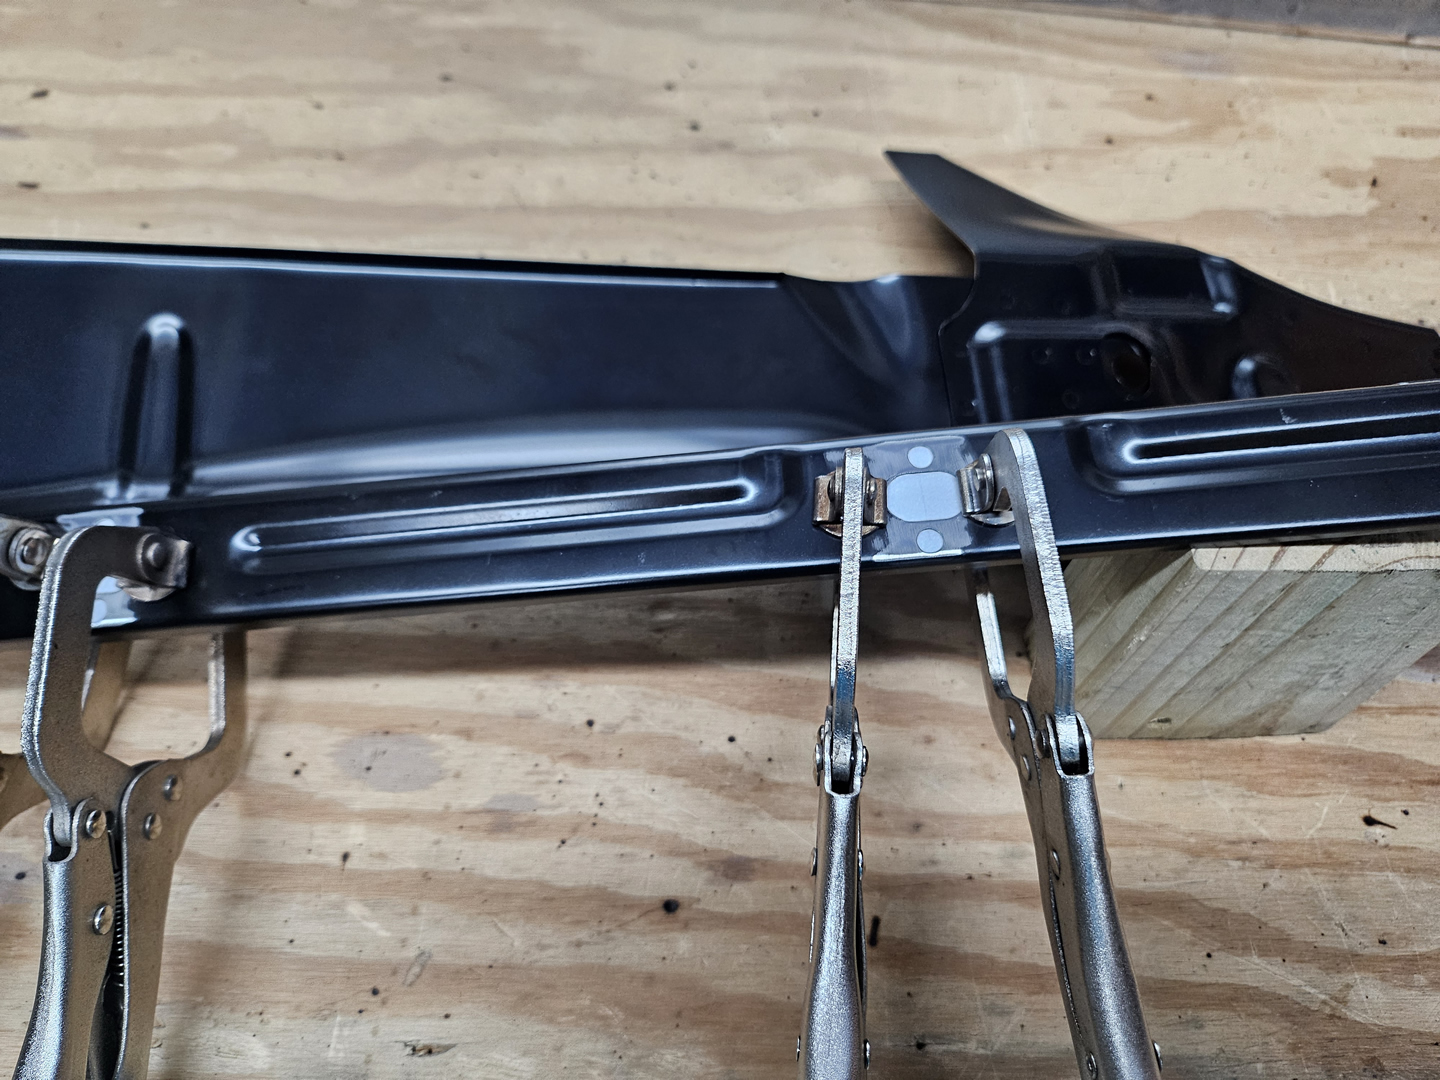
Finally I can prepare the bottom plates for welding. First, I punched and drilled holes for spot welds. Then I sprayed the areas to be welded with U-POL Weld #2 Zinc Weld Through Primer, and sprayed the areas on the inside of the bottom plates with Eastwood Matte Black Rust Encapsulator. I did the same thing with the heater channel bodies and sprayed U-POL Weld #2 Zinc Weld Through Primer on the areas to be welded, and sprayed the areas inside of the heater channel bodies with Eastwood Matte Black Rust Encapsulator.
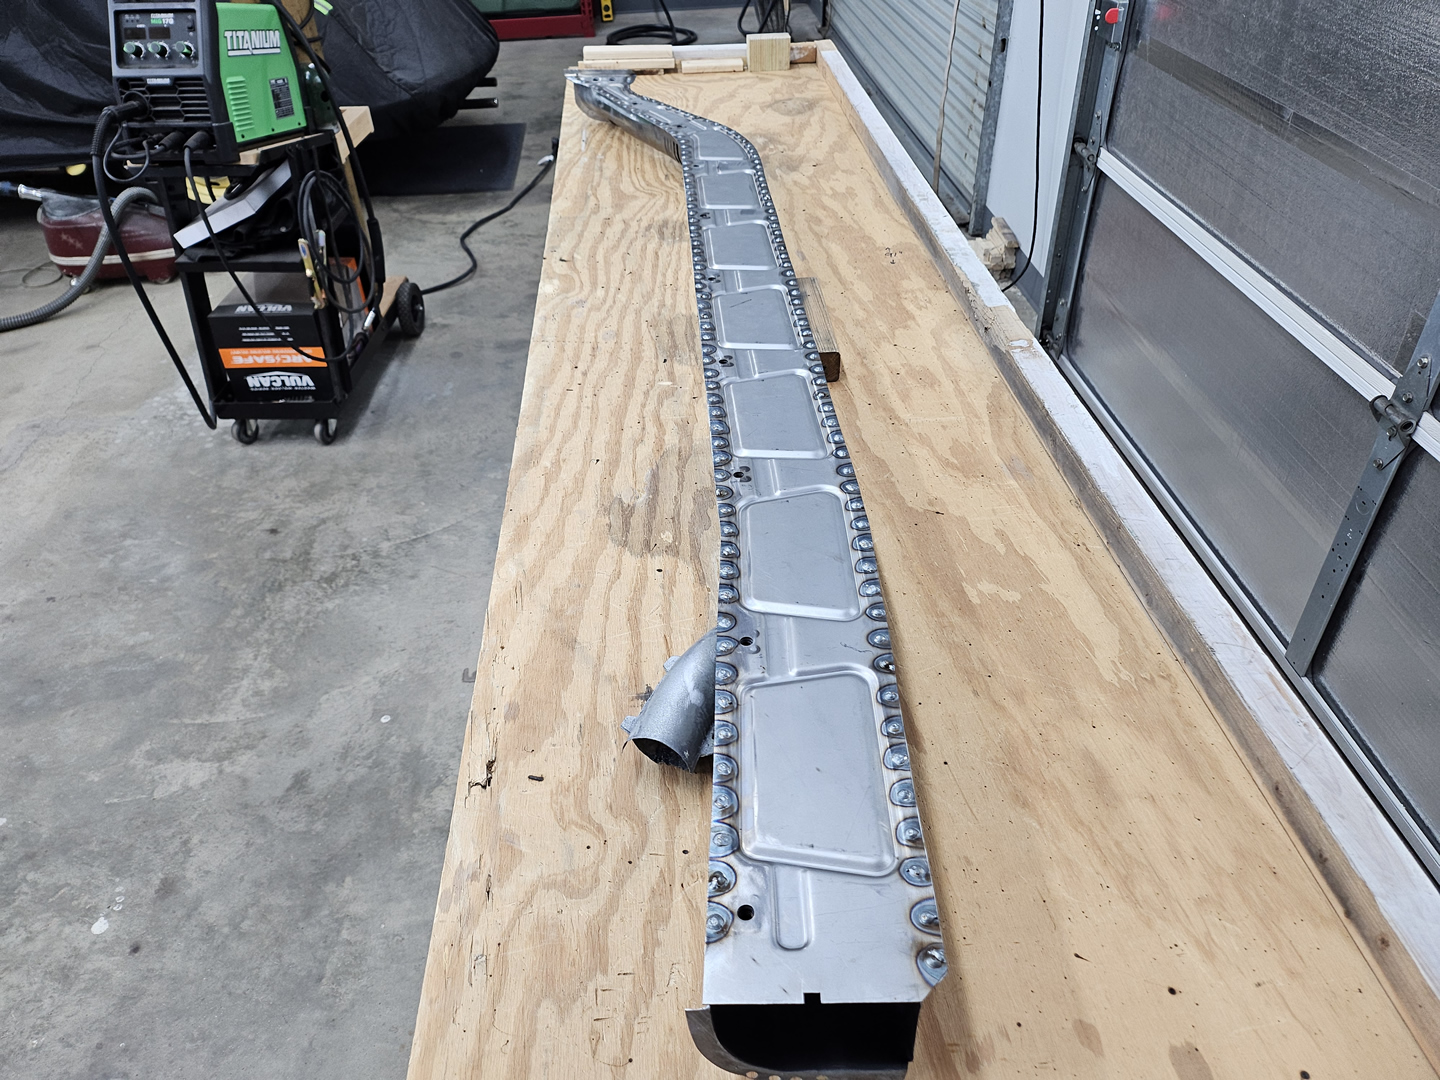
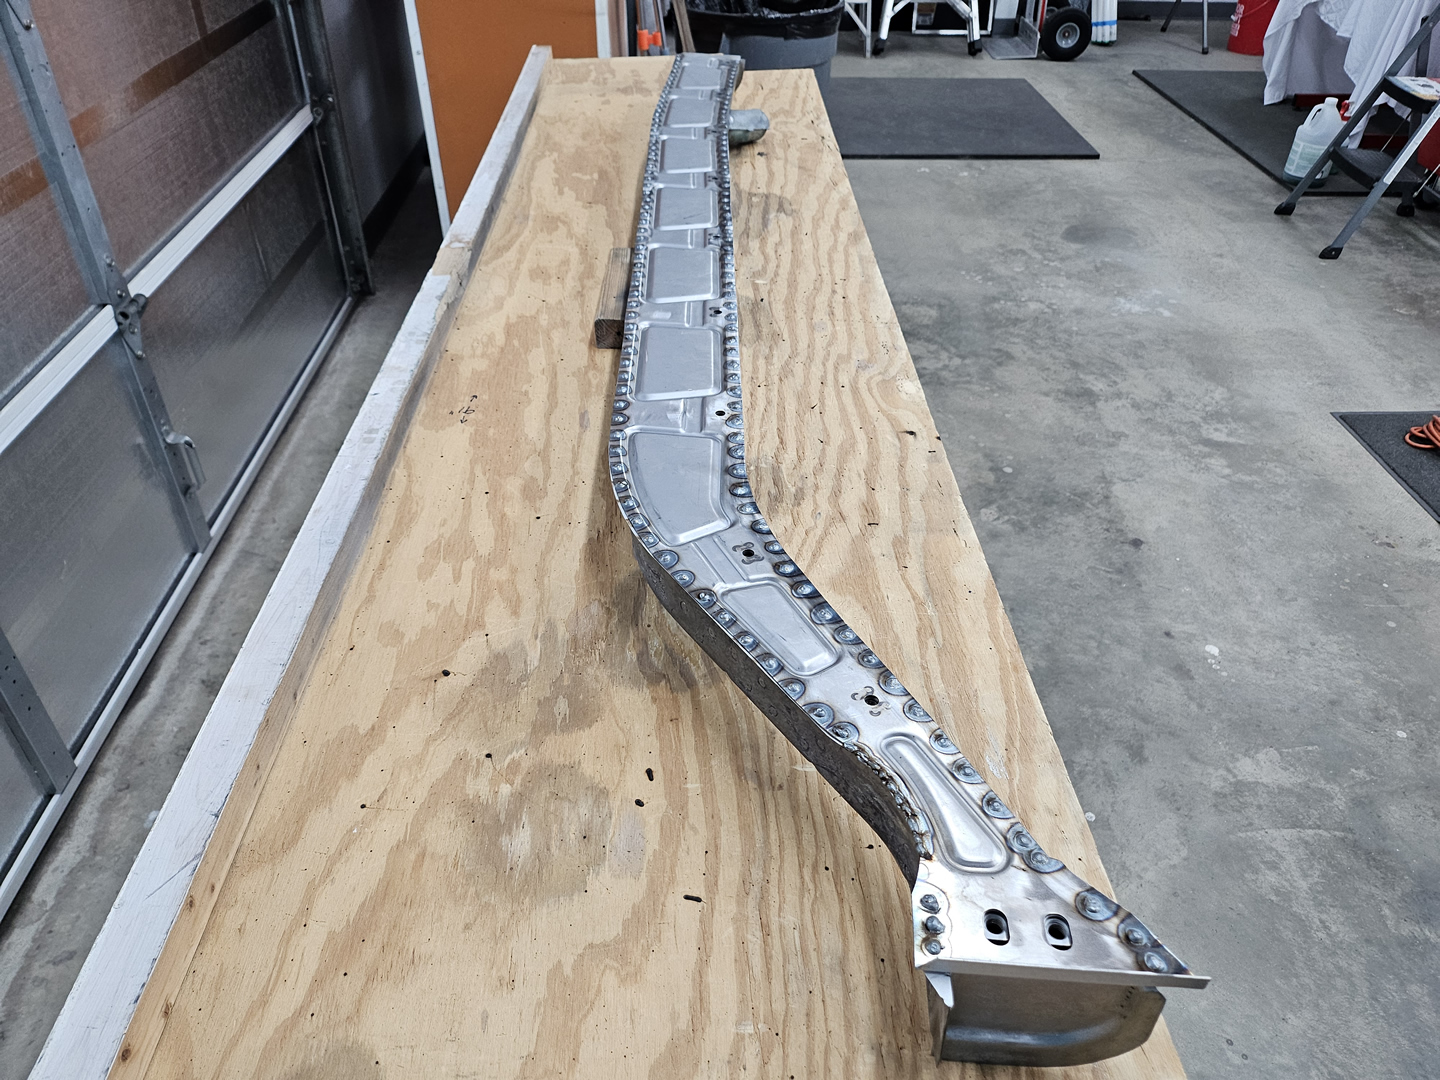
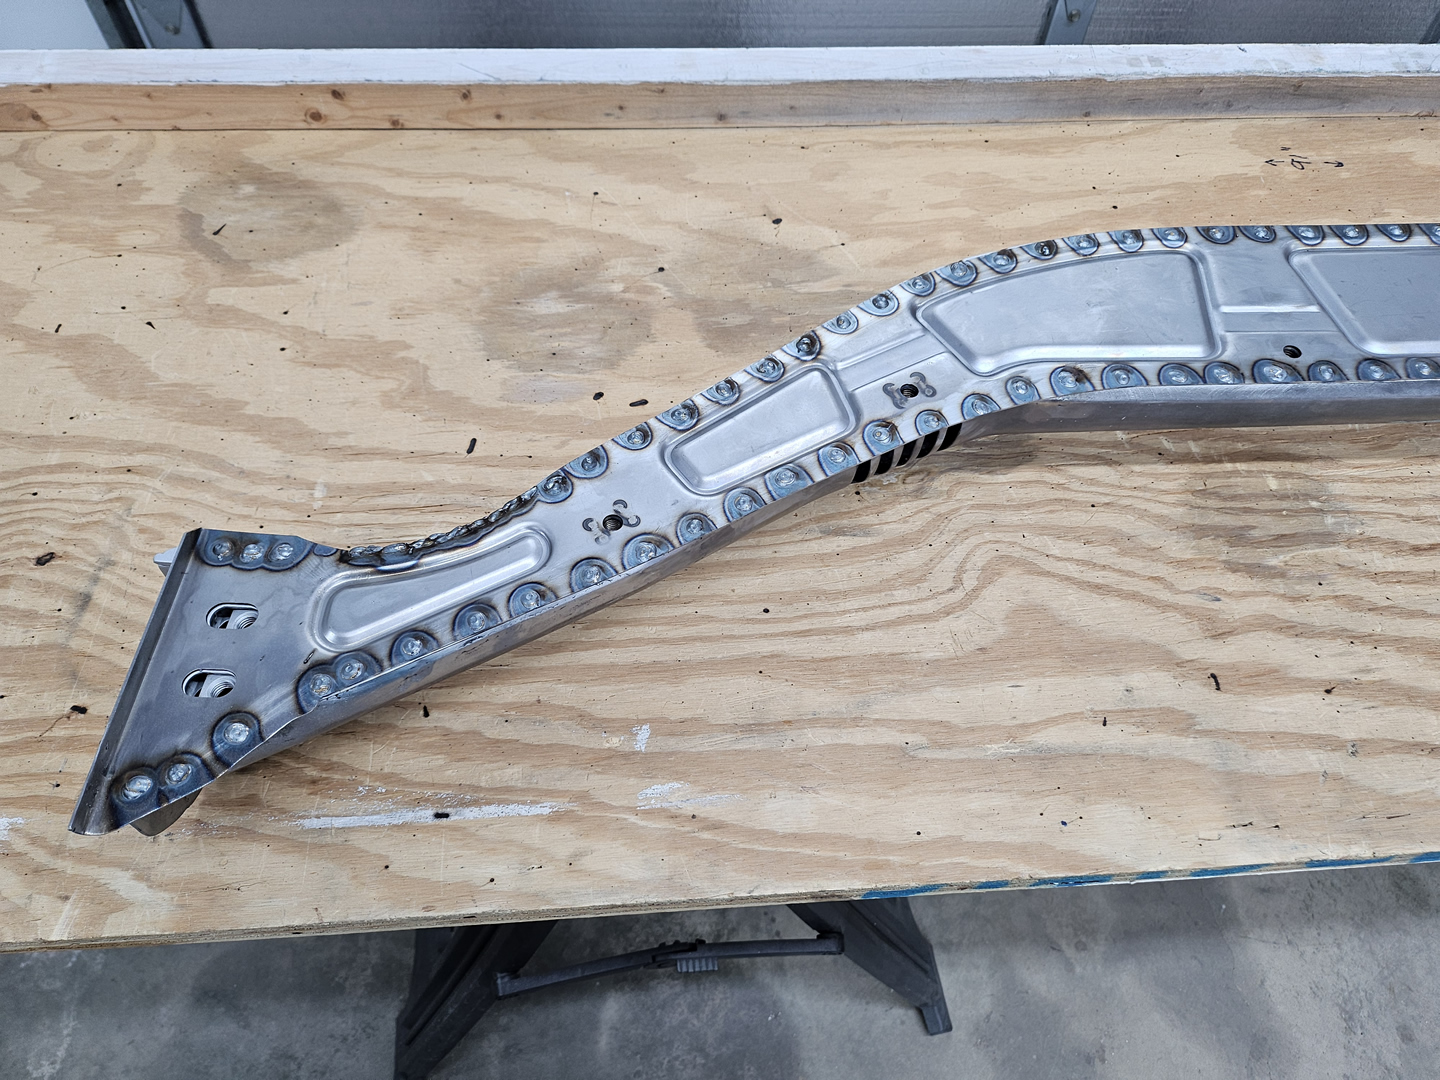
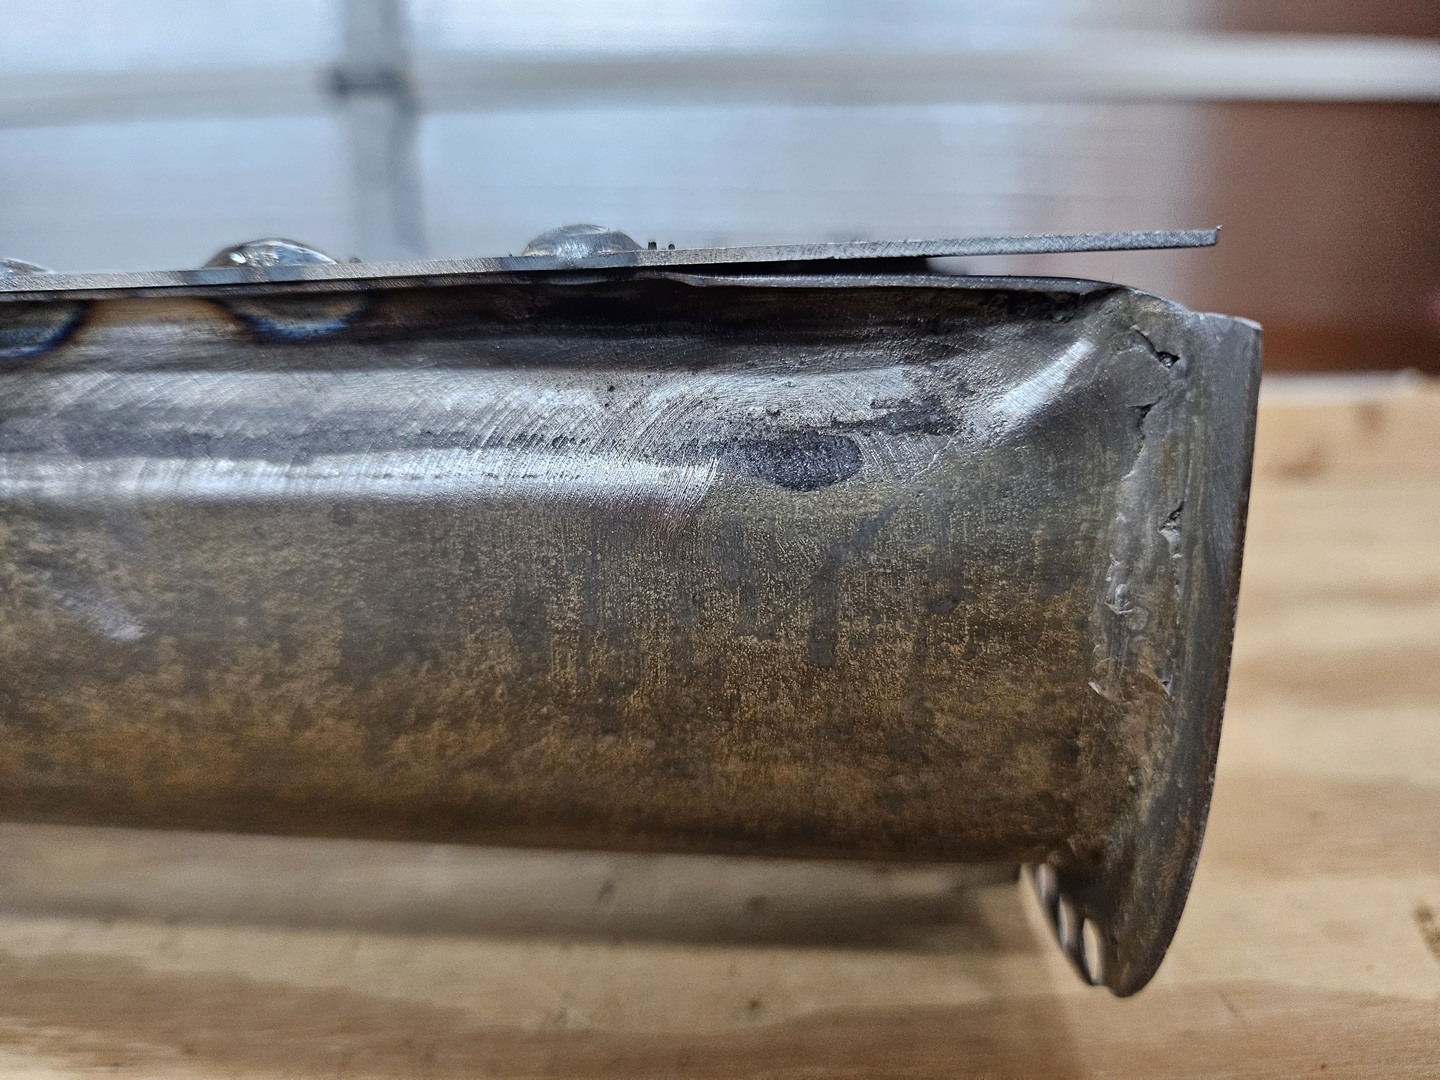
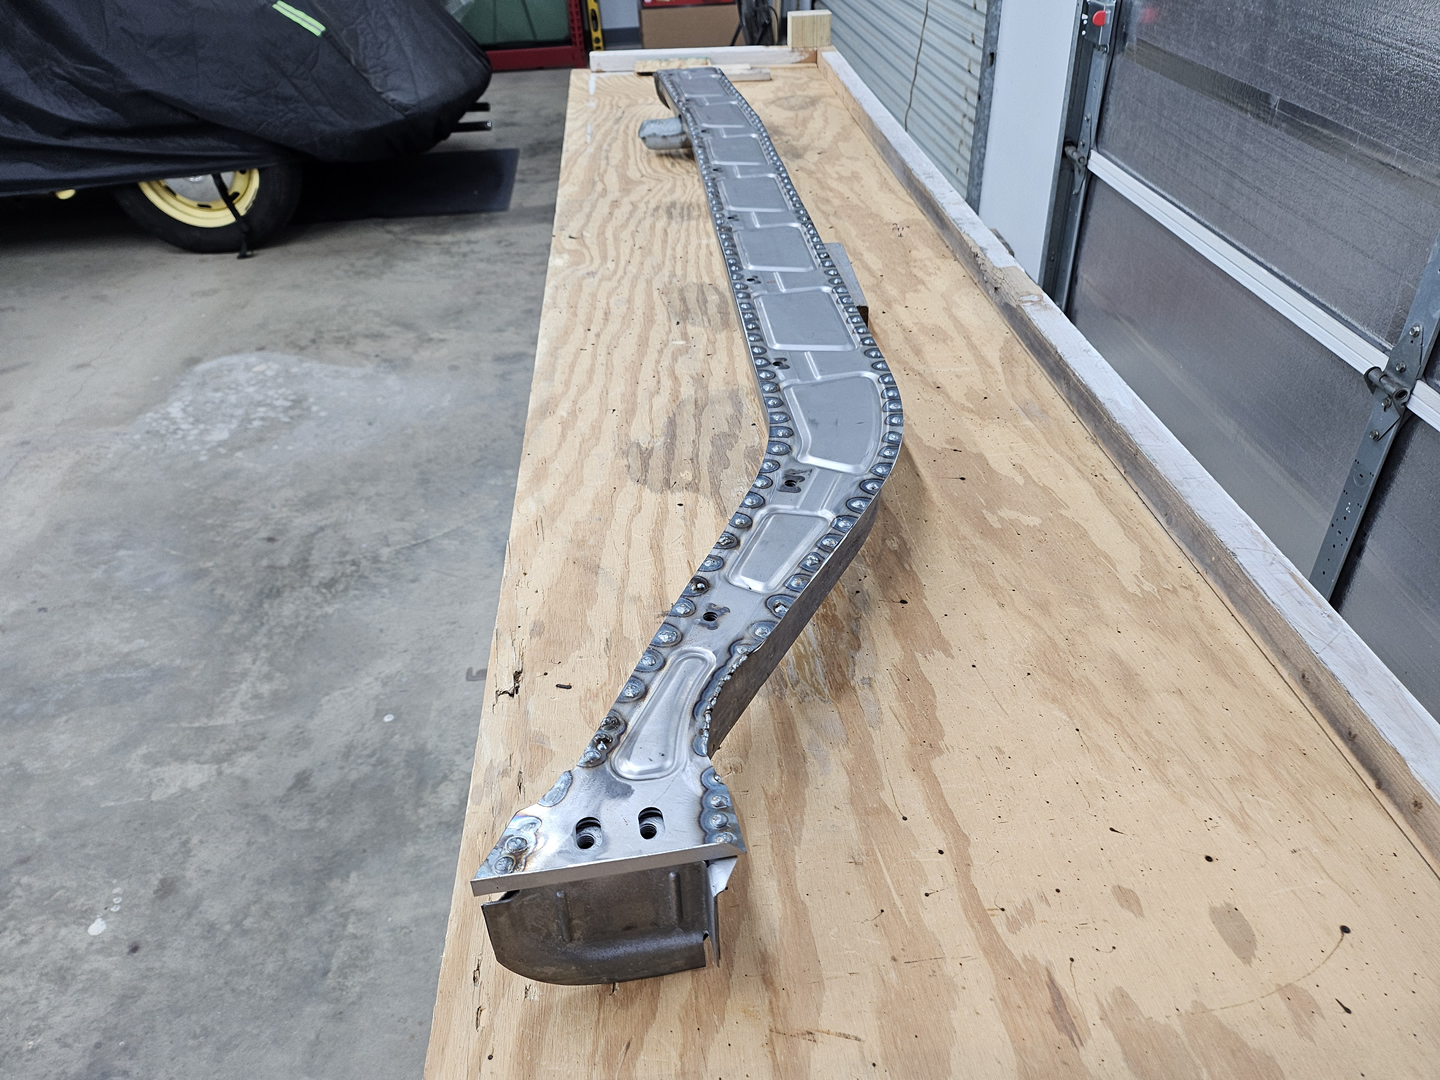
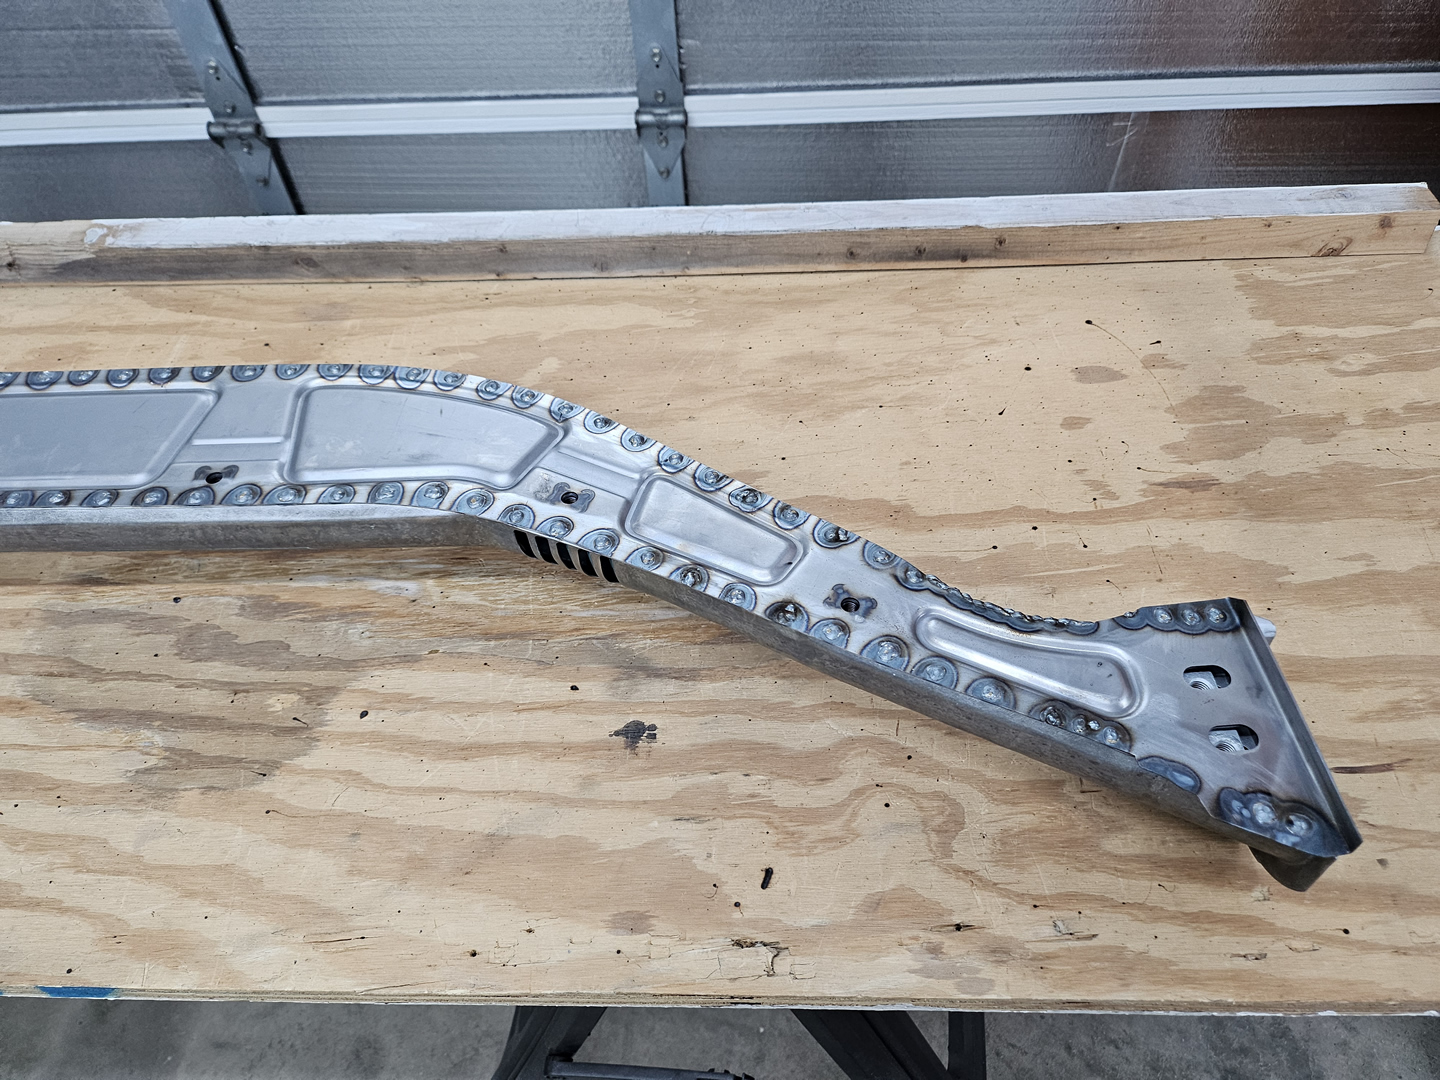
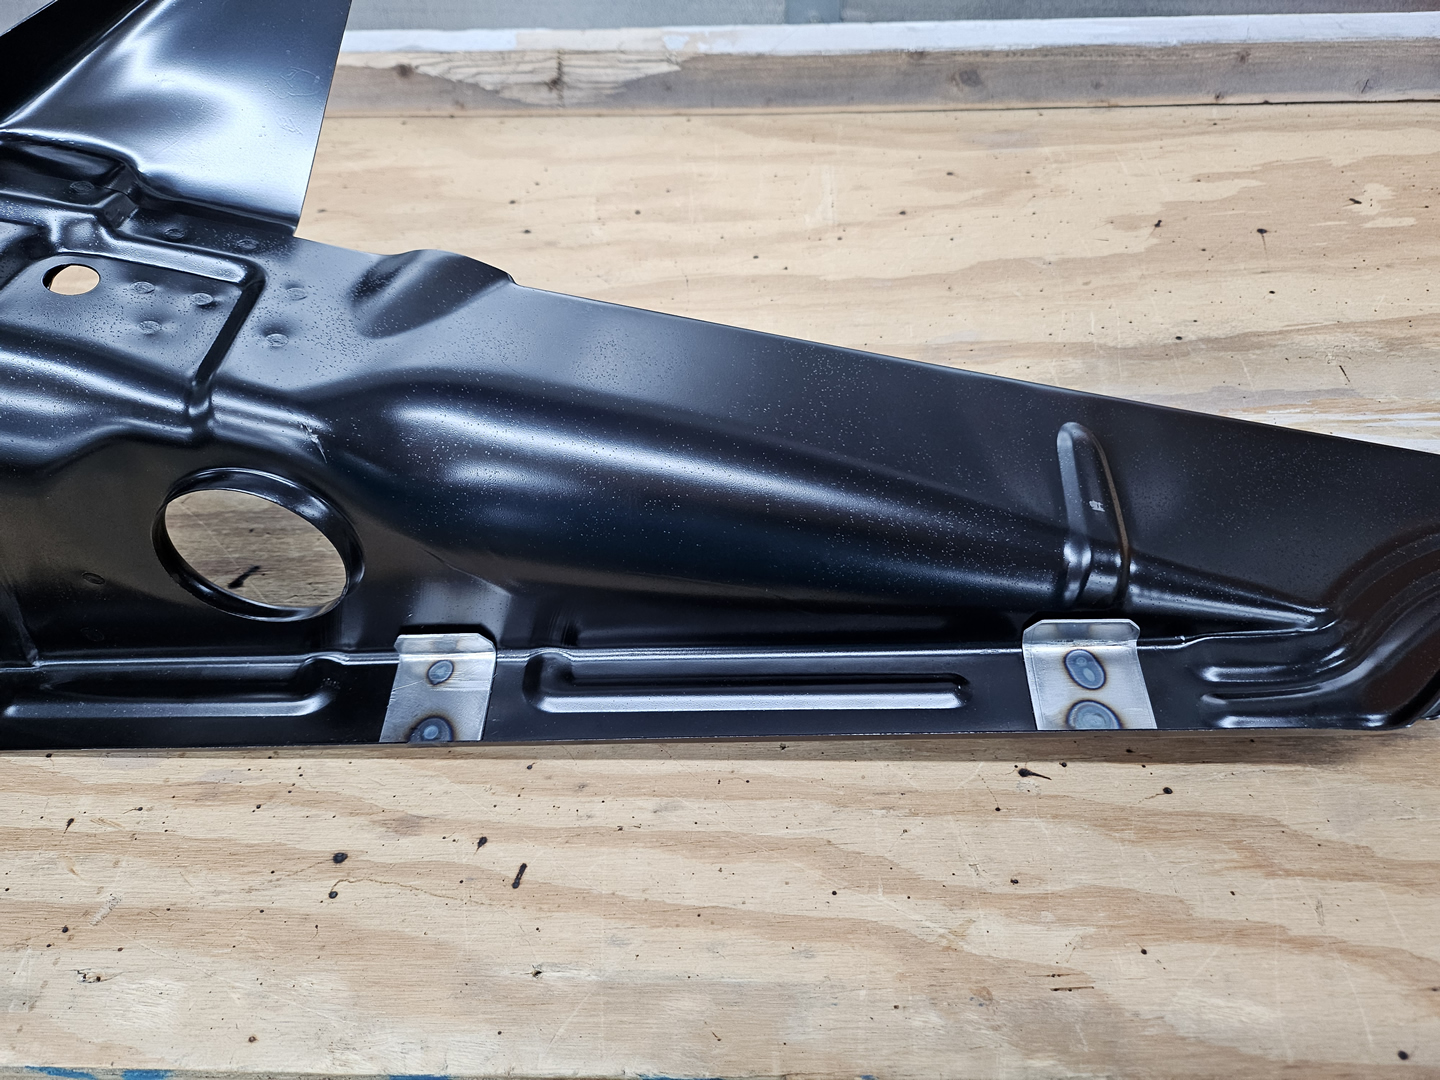
Time to weld the bottom plates on. I started with the driver side heater channel. There were 140 spot welds on this channel and one seam weld on the outside of the front section where it is too narrow do spot welds. Also, on the rear inside corner of the bottom plates, there is no spot weld and there is a gap between the bottom plate and the channel body where the rear crossmember fits into it.
|
|
|
|
|
|
|
|
|
|
|
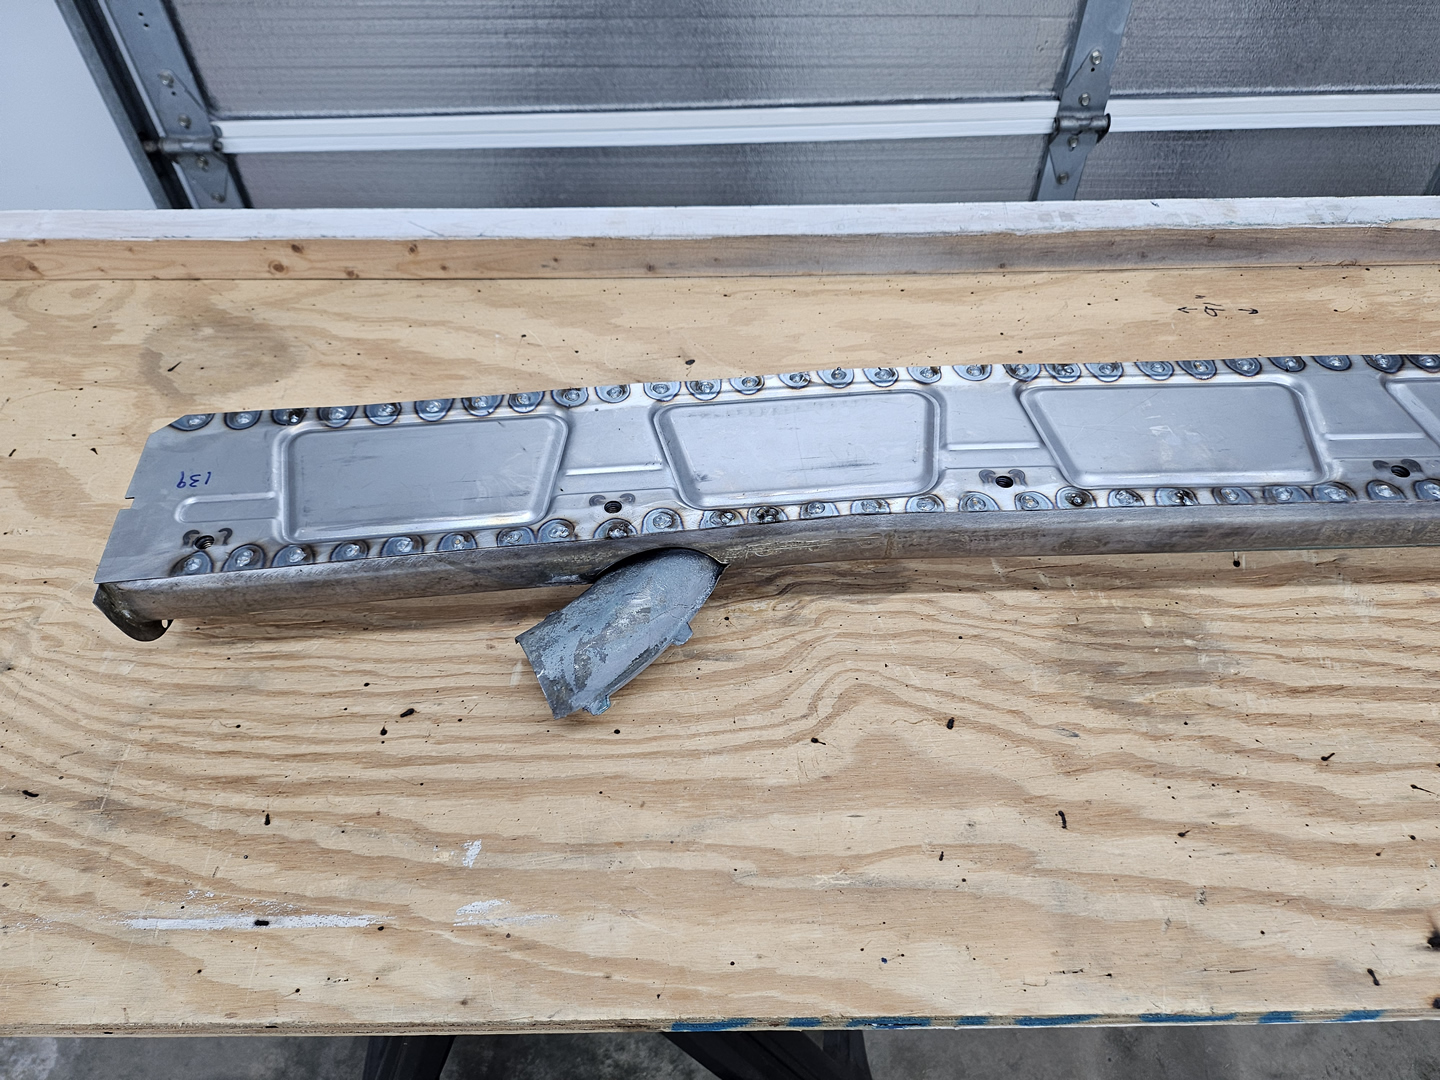
Next, I welded on the passenger side bottom plate. There were 139 spot welds and one seam weld on this one. Now that both bottom plates are welded on, I have many hours of grinding ahead.
|
|
|
|
|
|
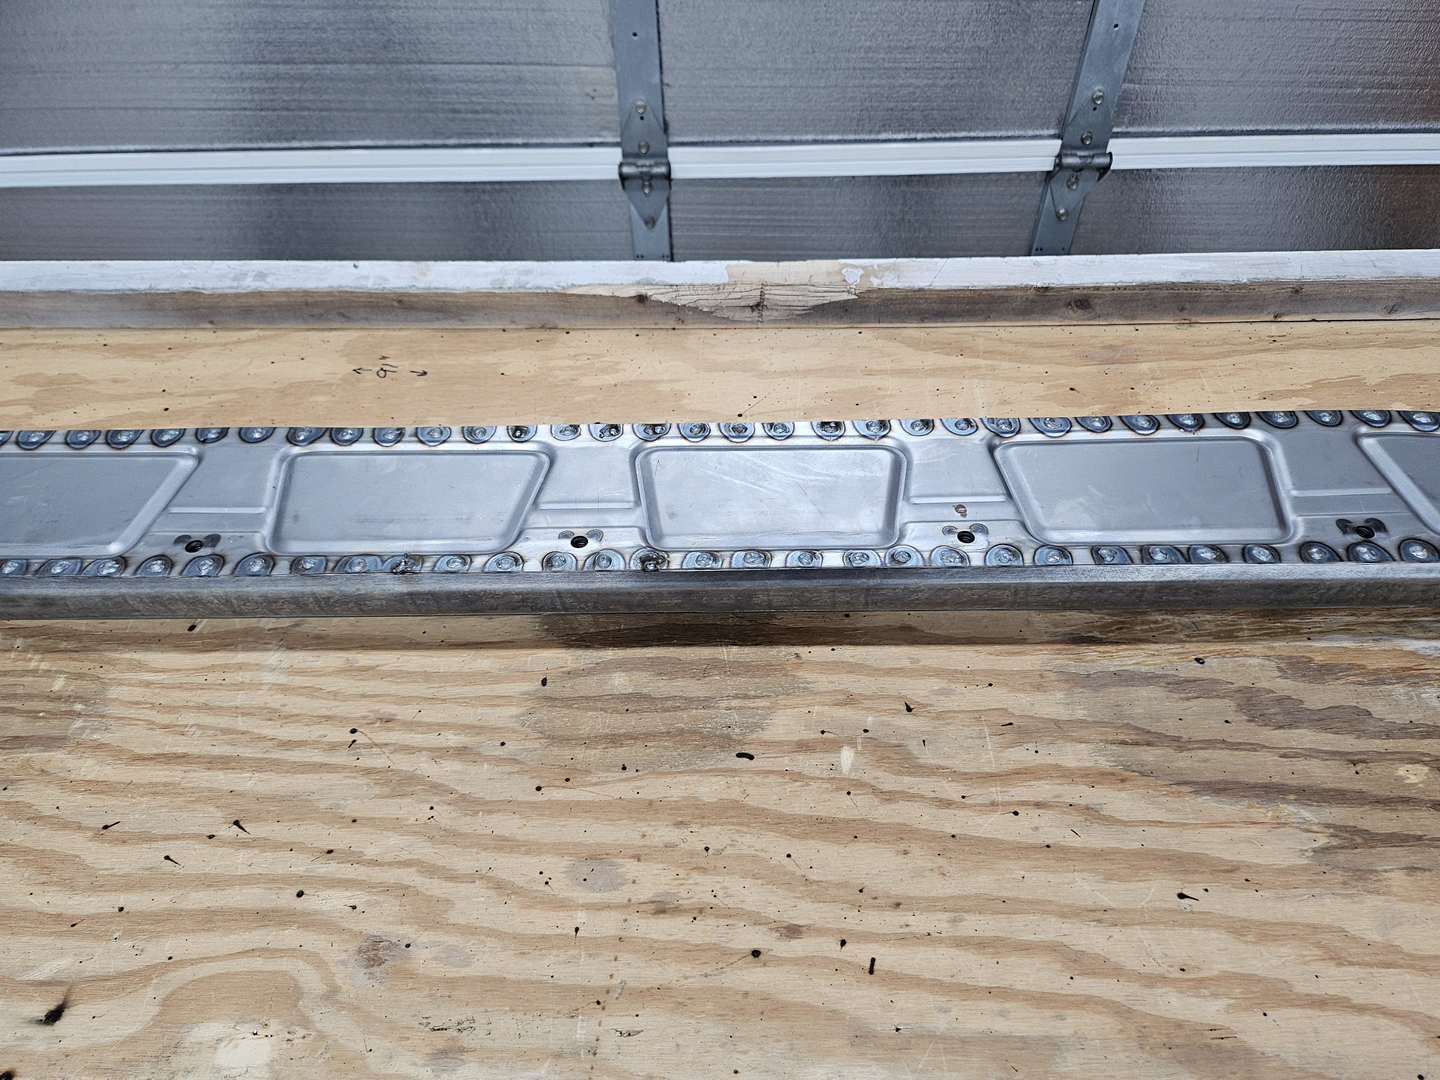
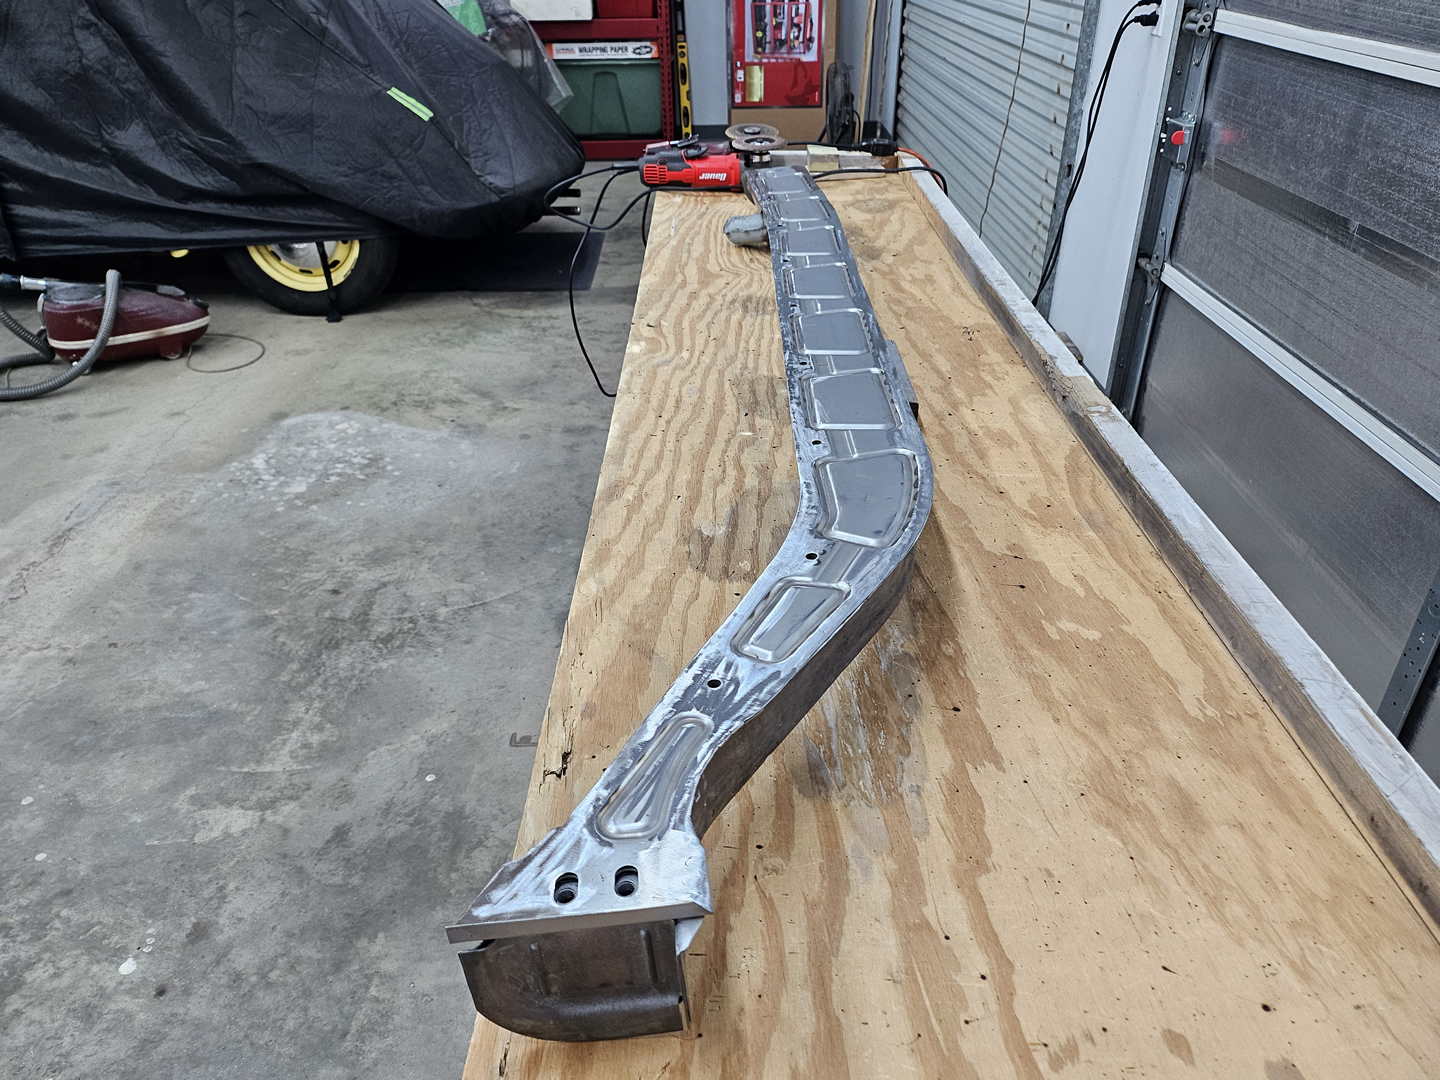
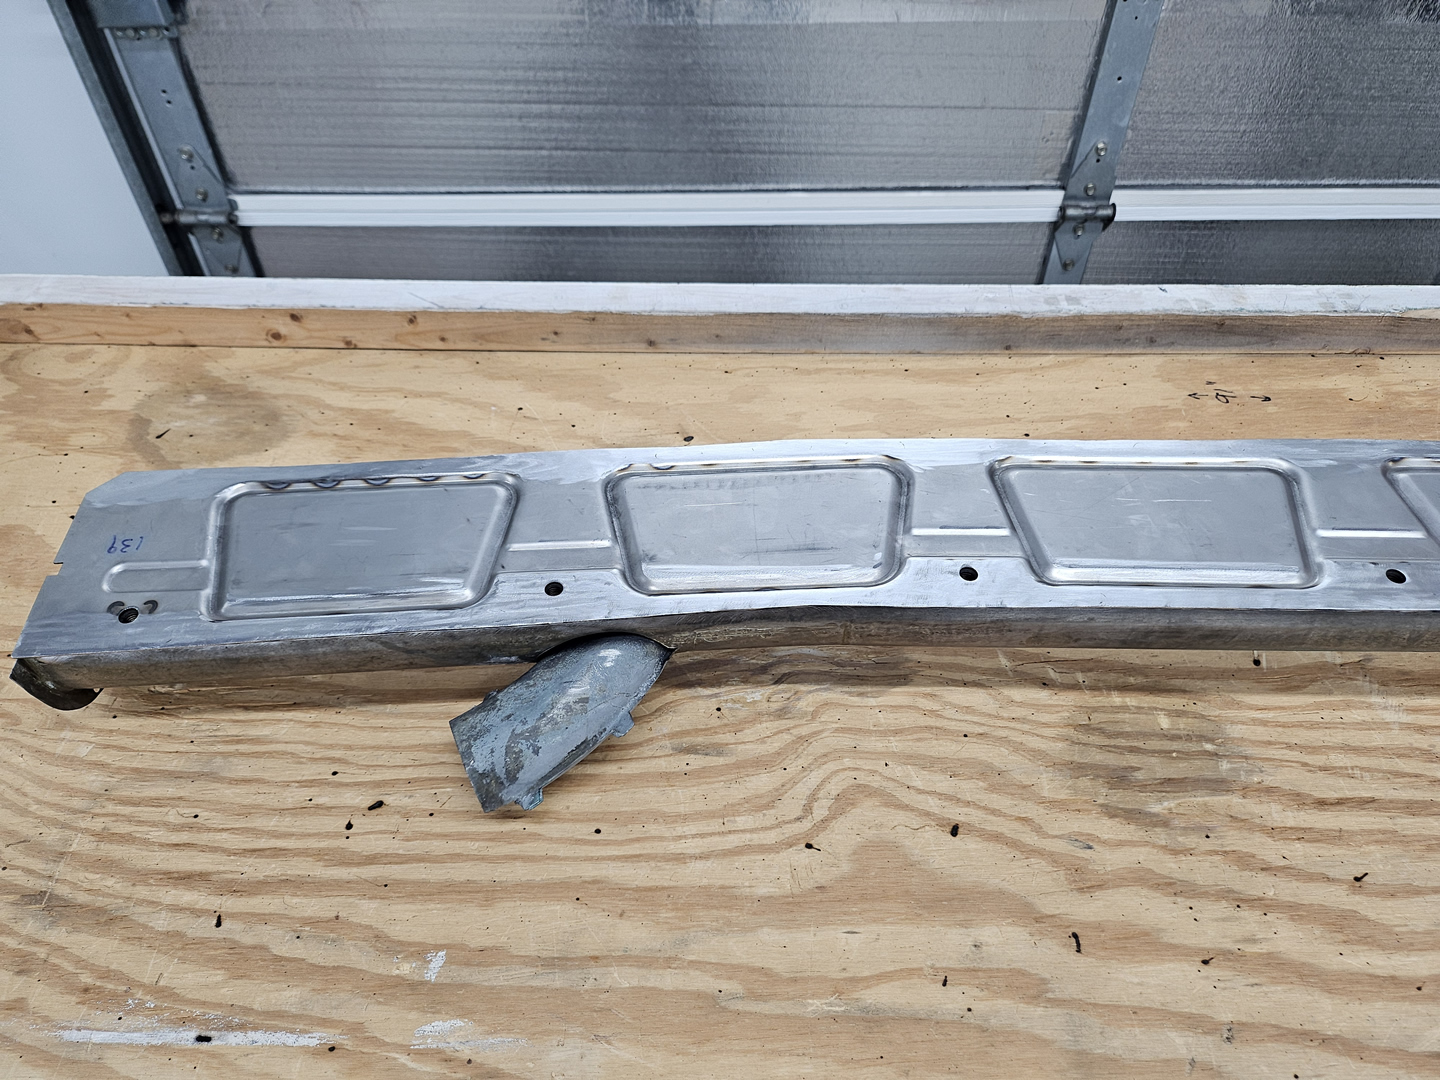
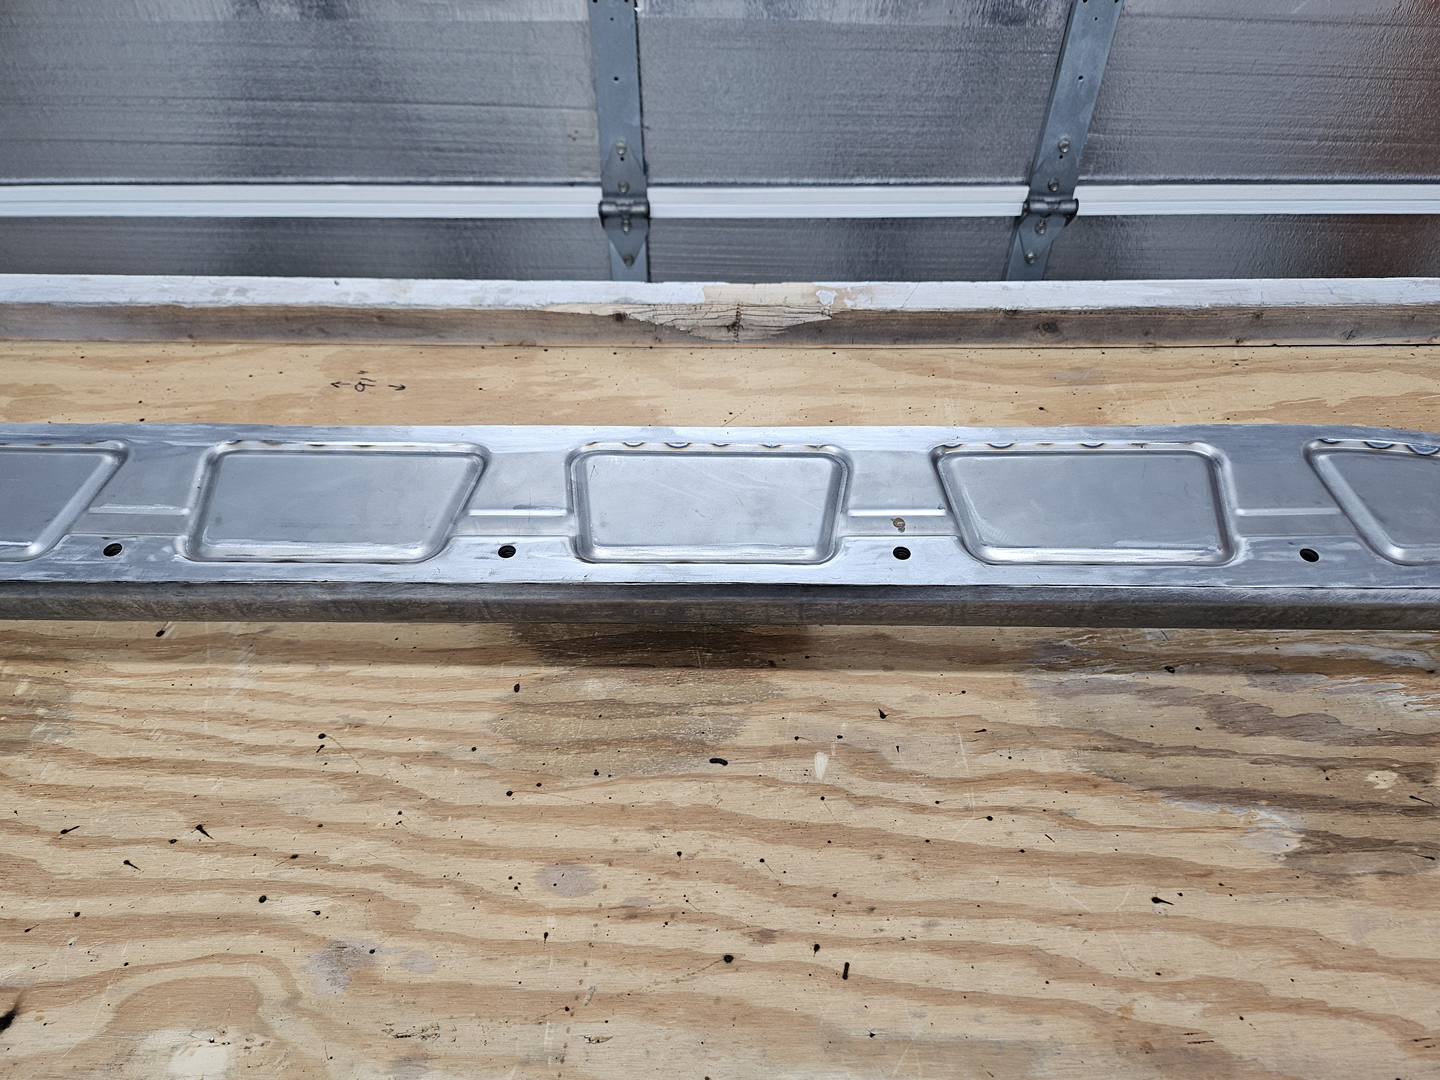
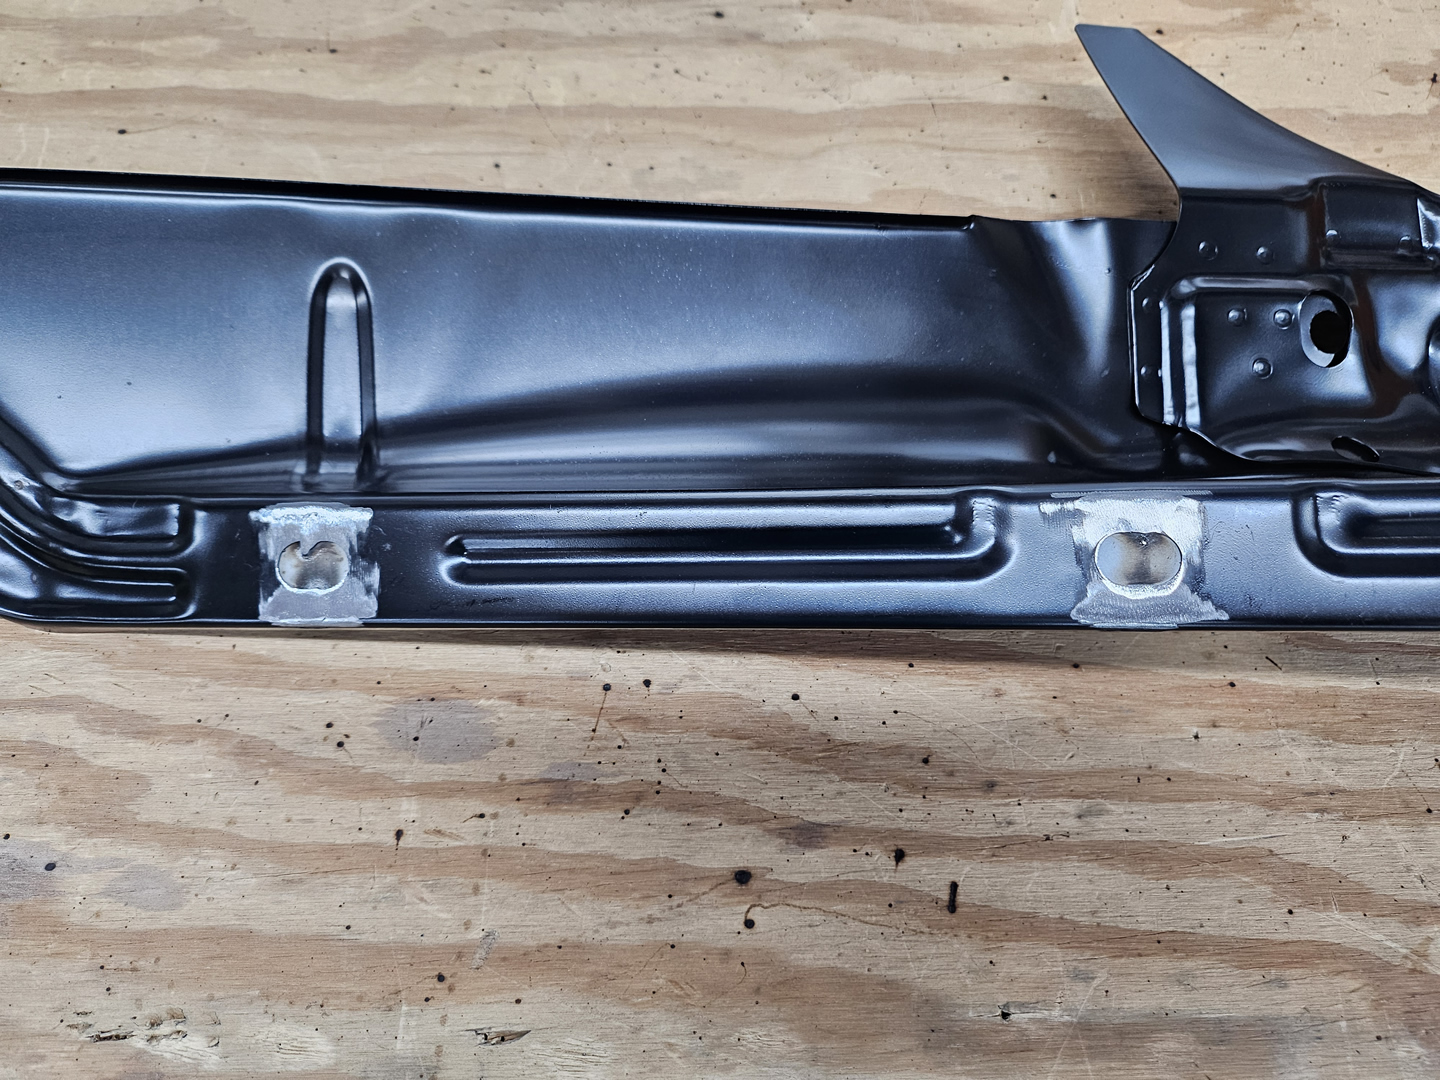
I first ground down the welds on the passenger side heater channel bottom plate.
|
|
|
|
|
|
Then I ground down the welds on the driver side heater channel bottom plate.
|
|
|
|
|
|
Next, I sprayed some primer on the bottom plates and on the heater channel bodies where the bottom plates were welded on. My main concern is to fend off flash rust until they are welded onto the body of the car. The other areas that weren't sprayed have been treated with Ospho.
|
|
|
|
|
|
|
|
|
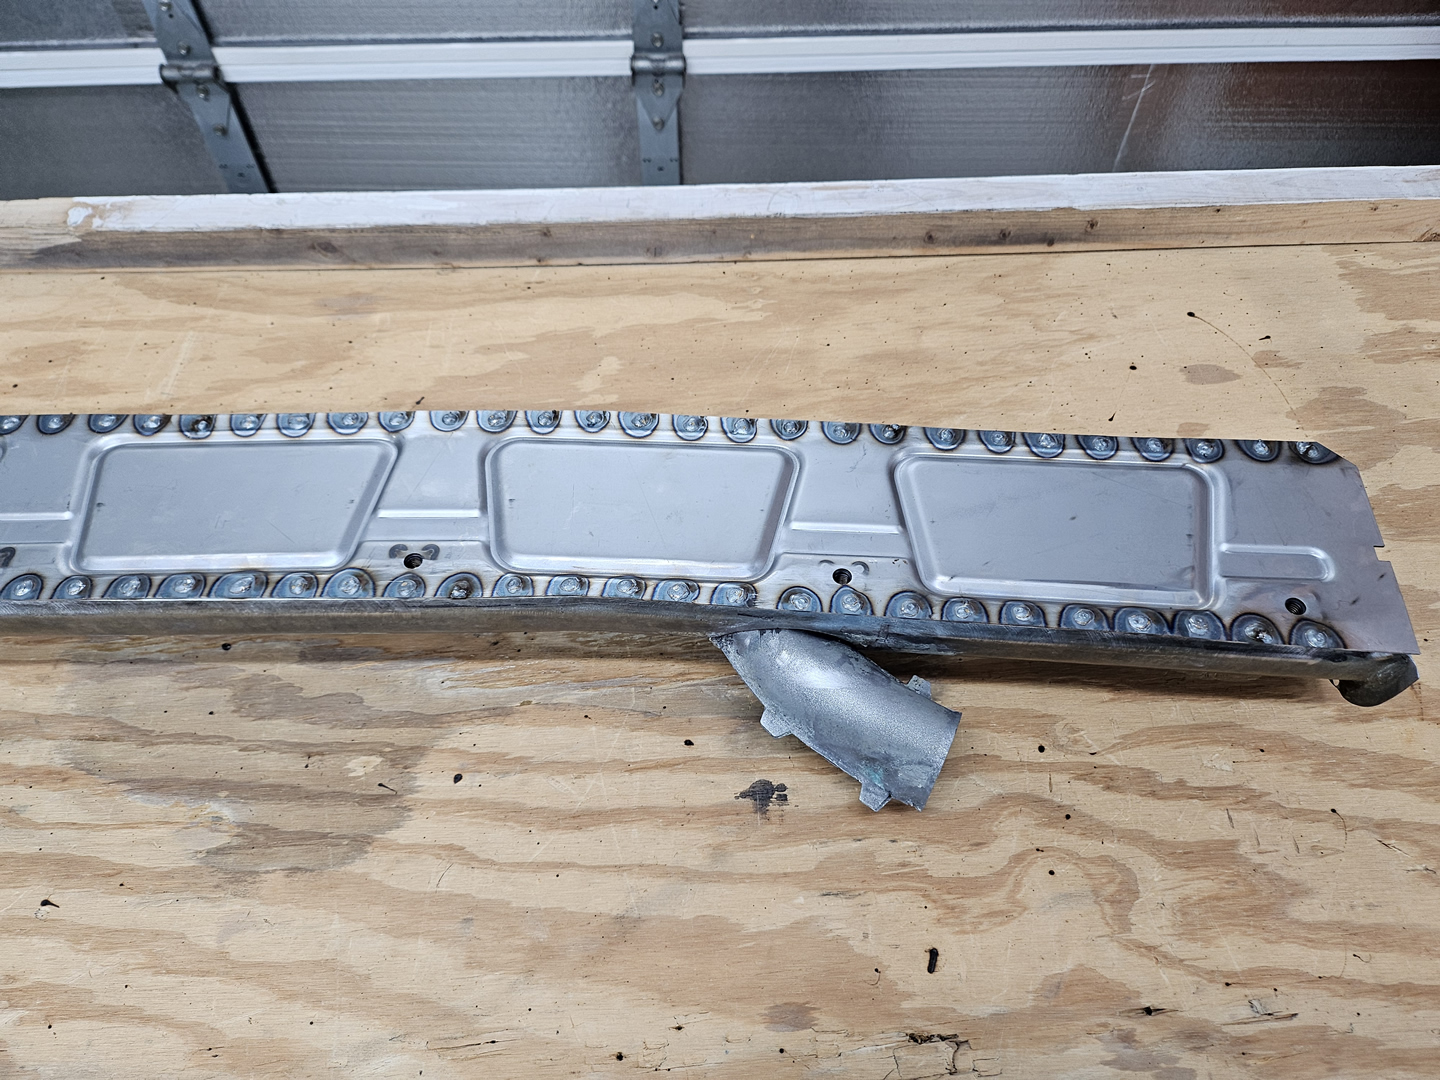
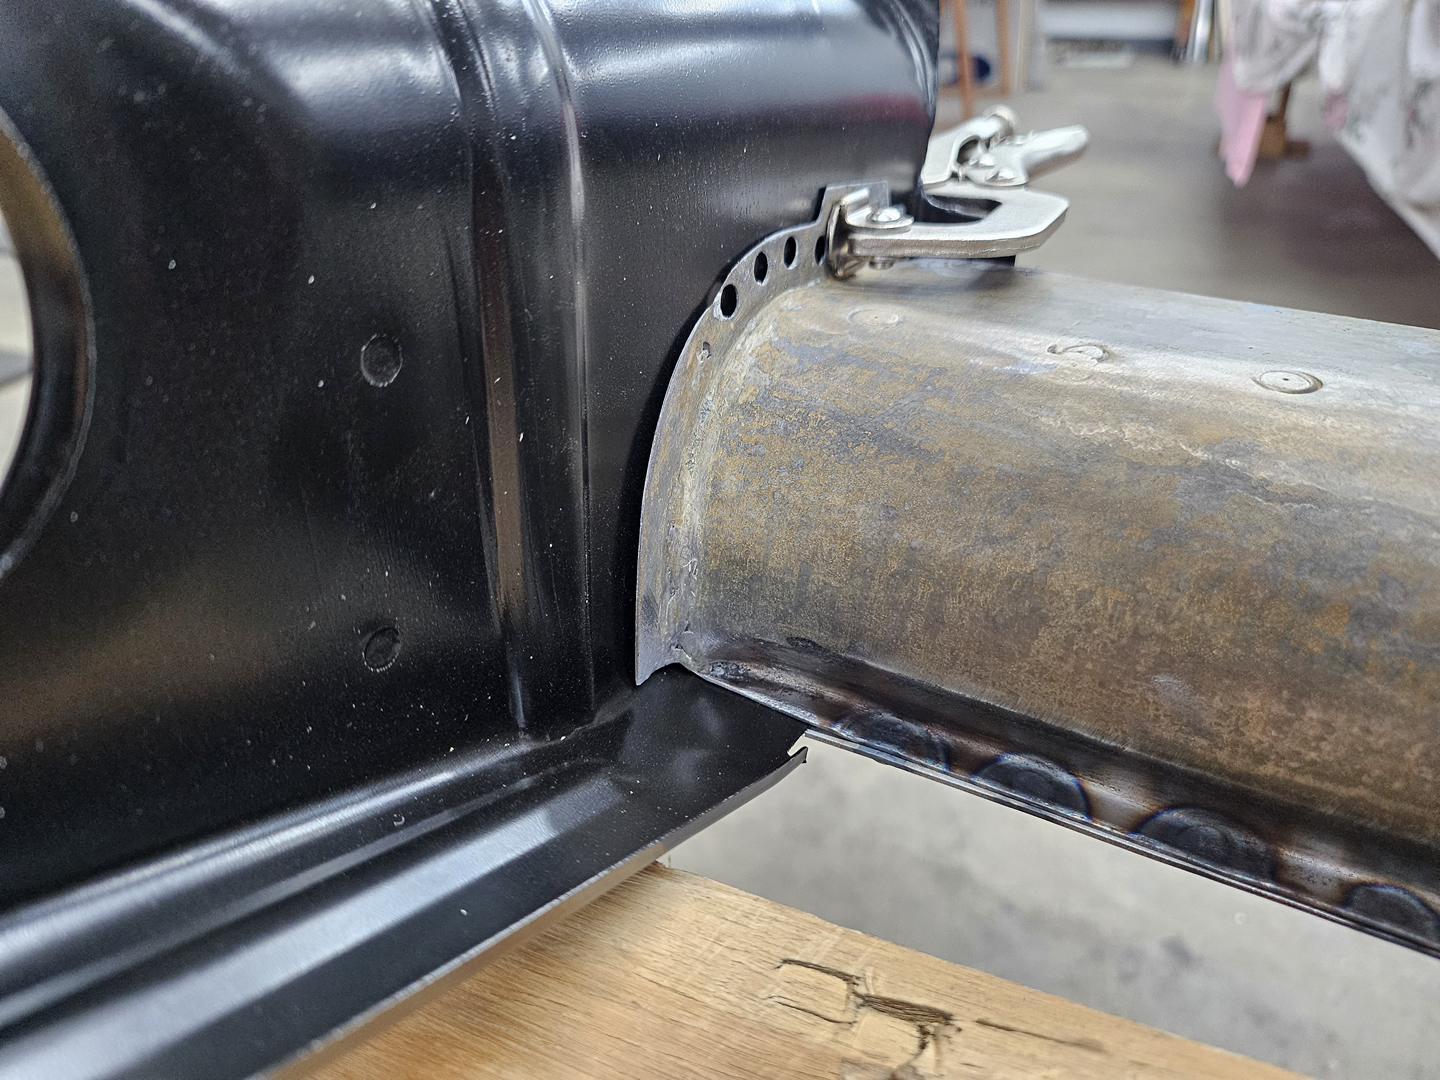
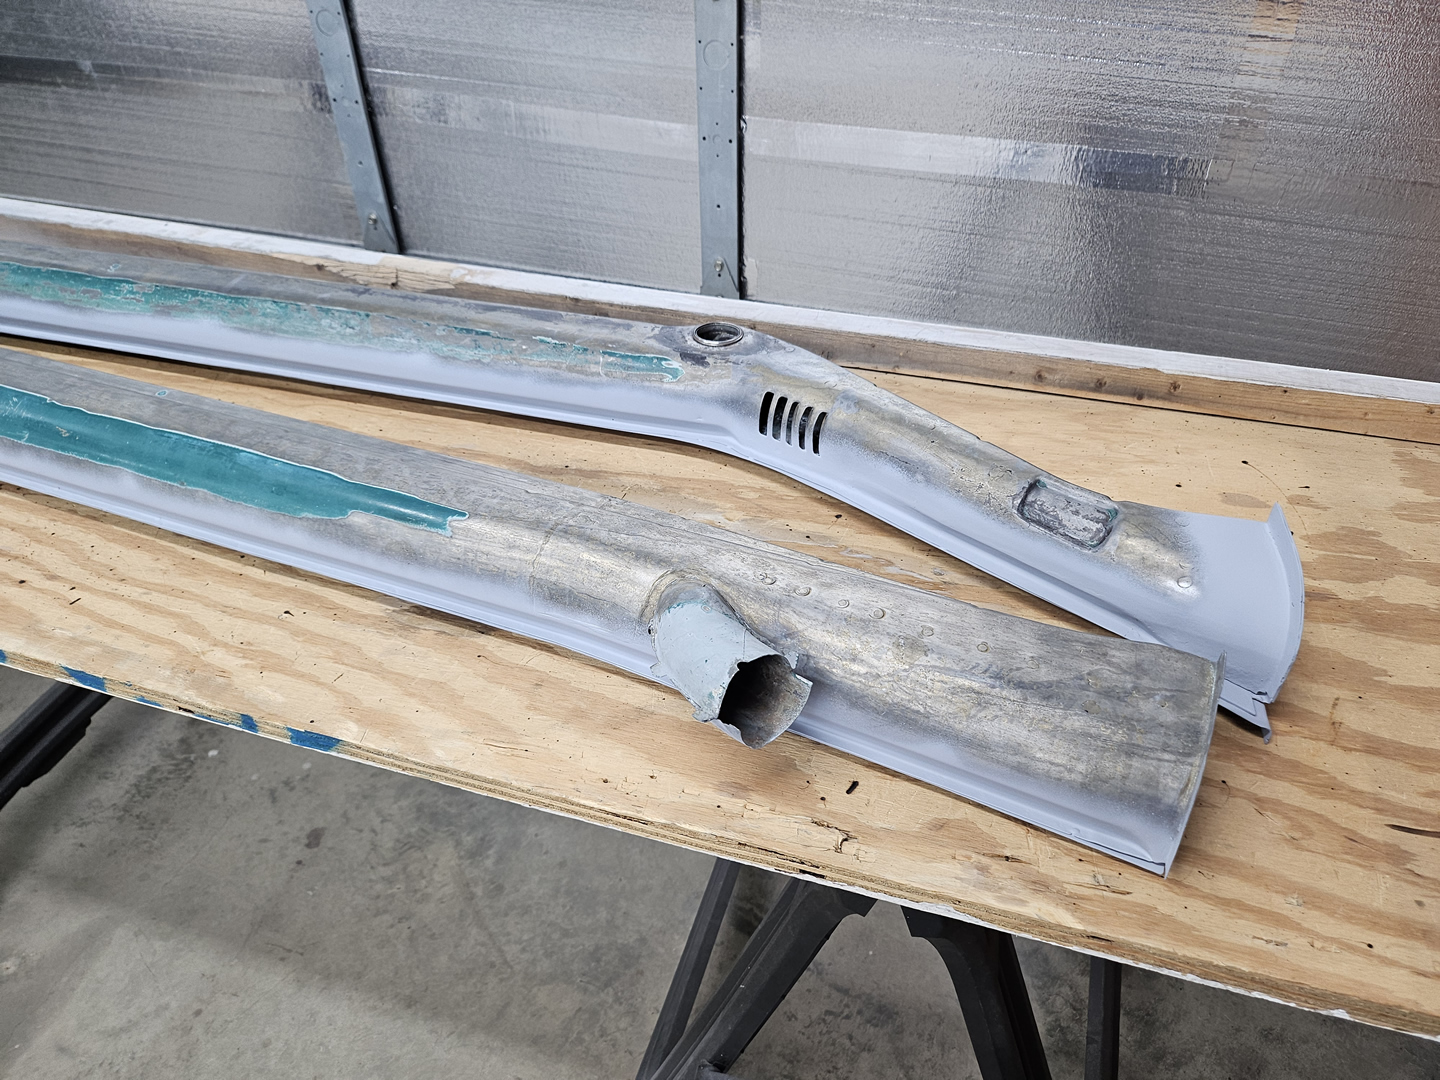
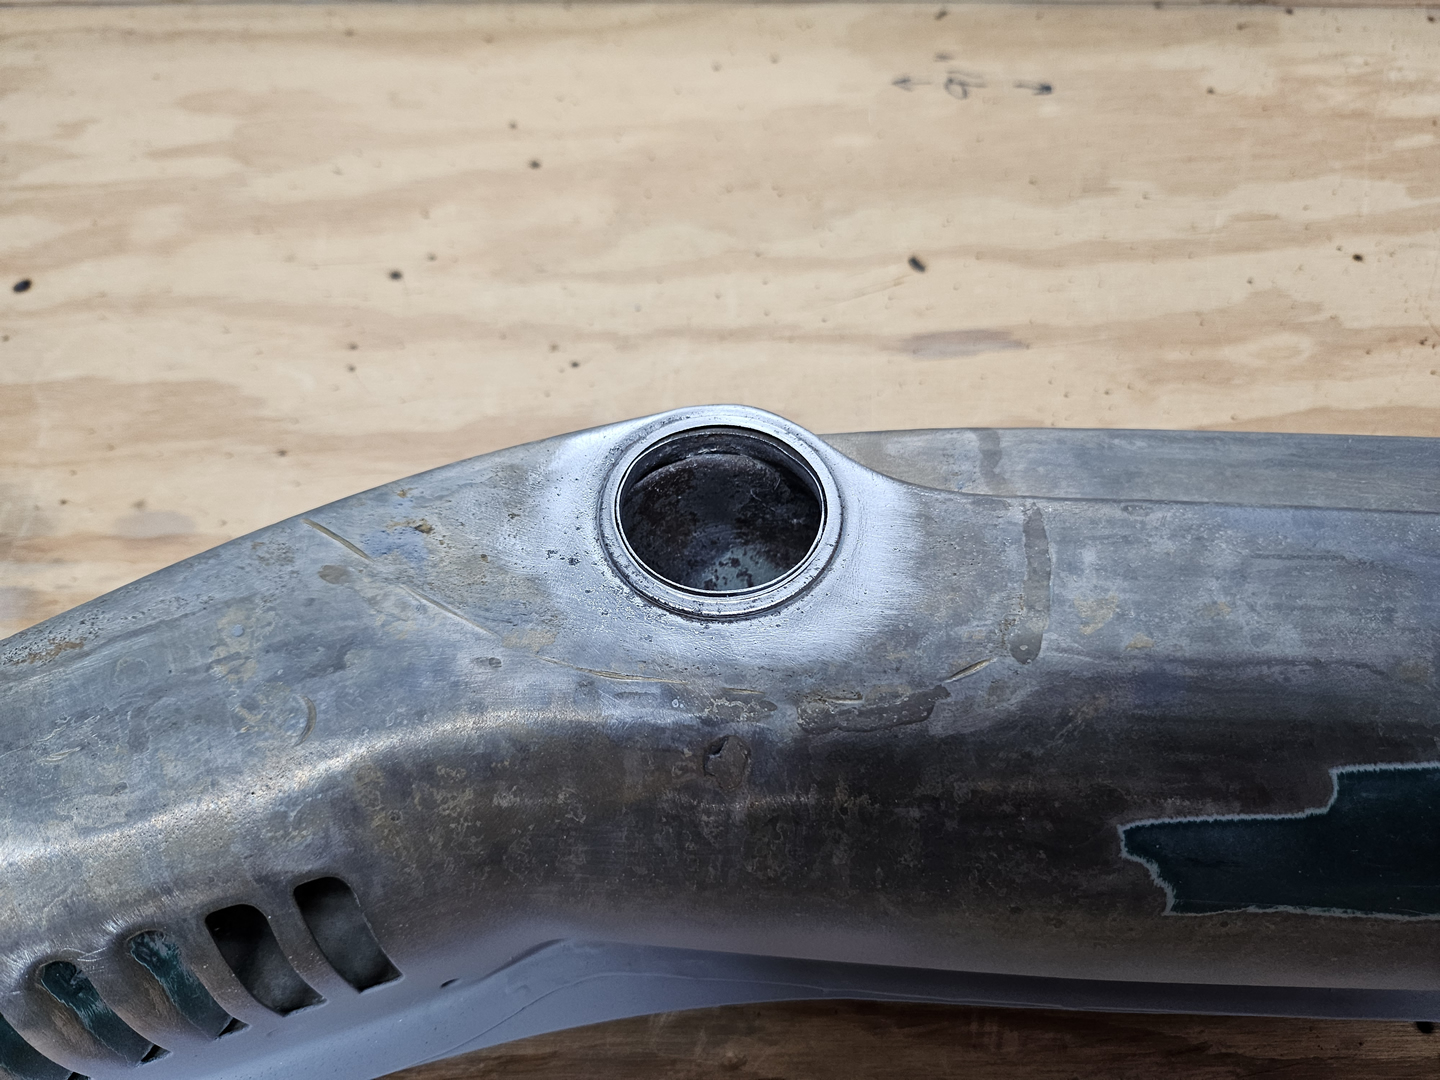
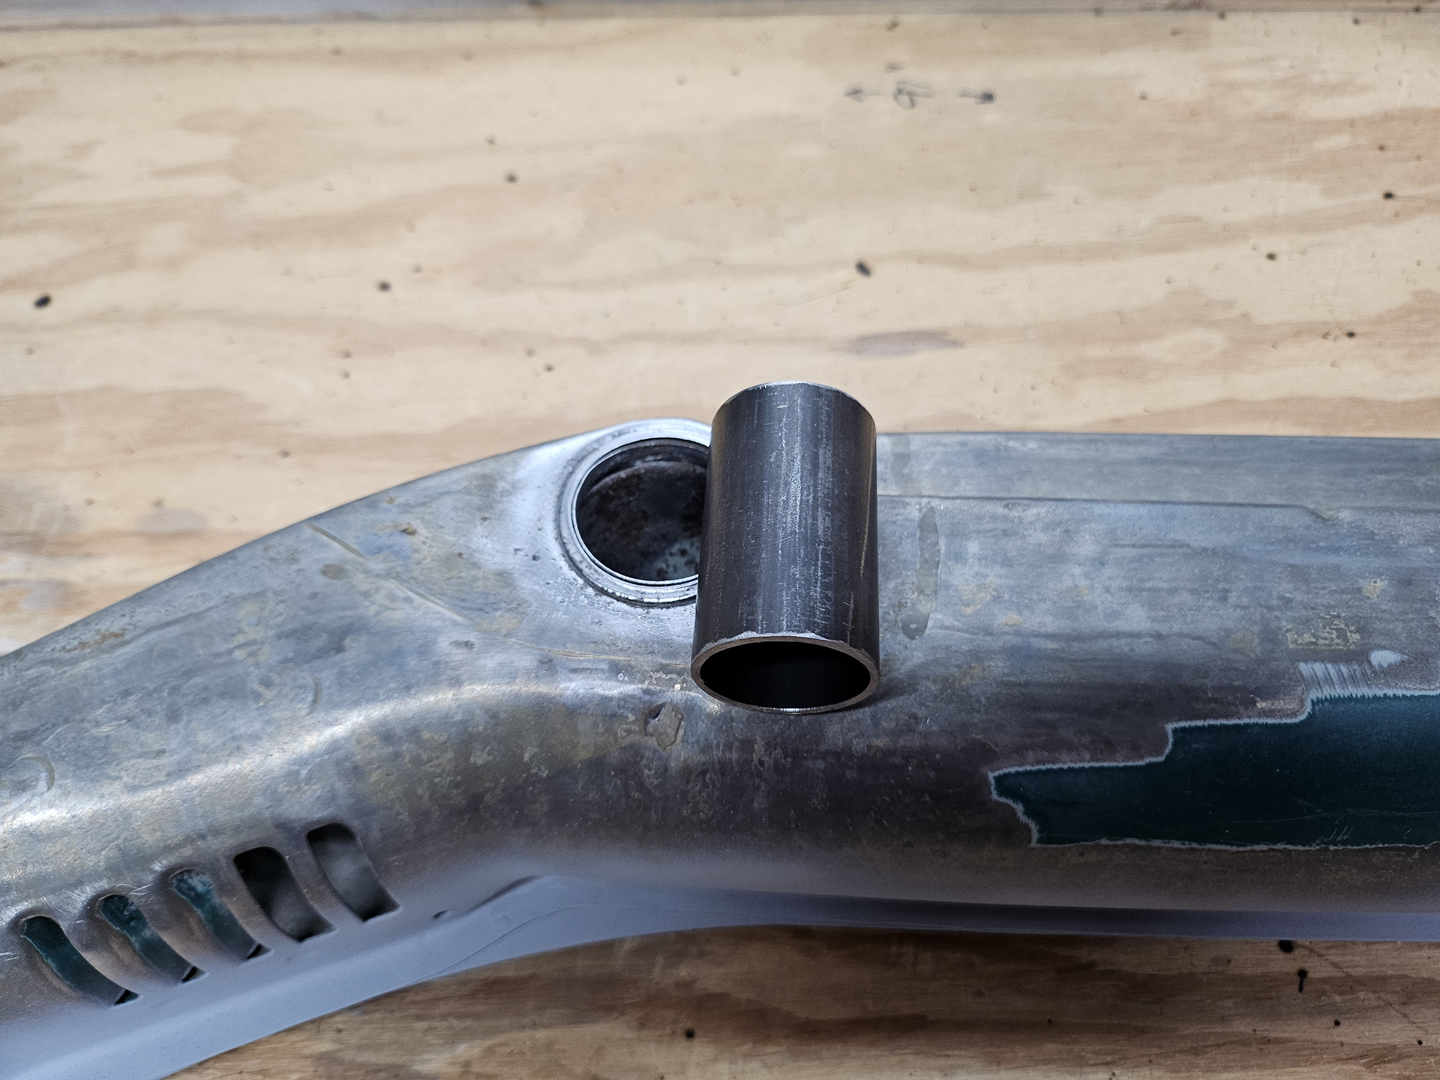
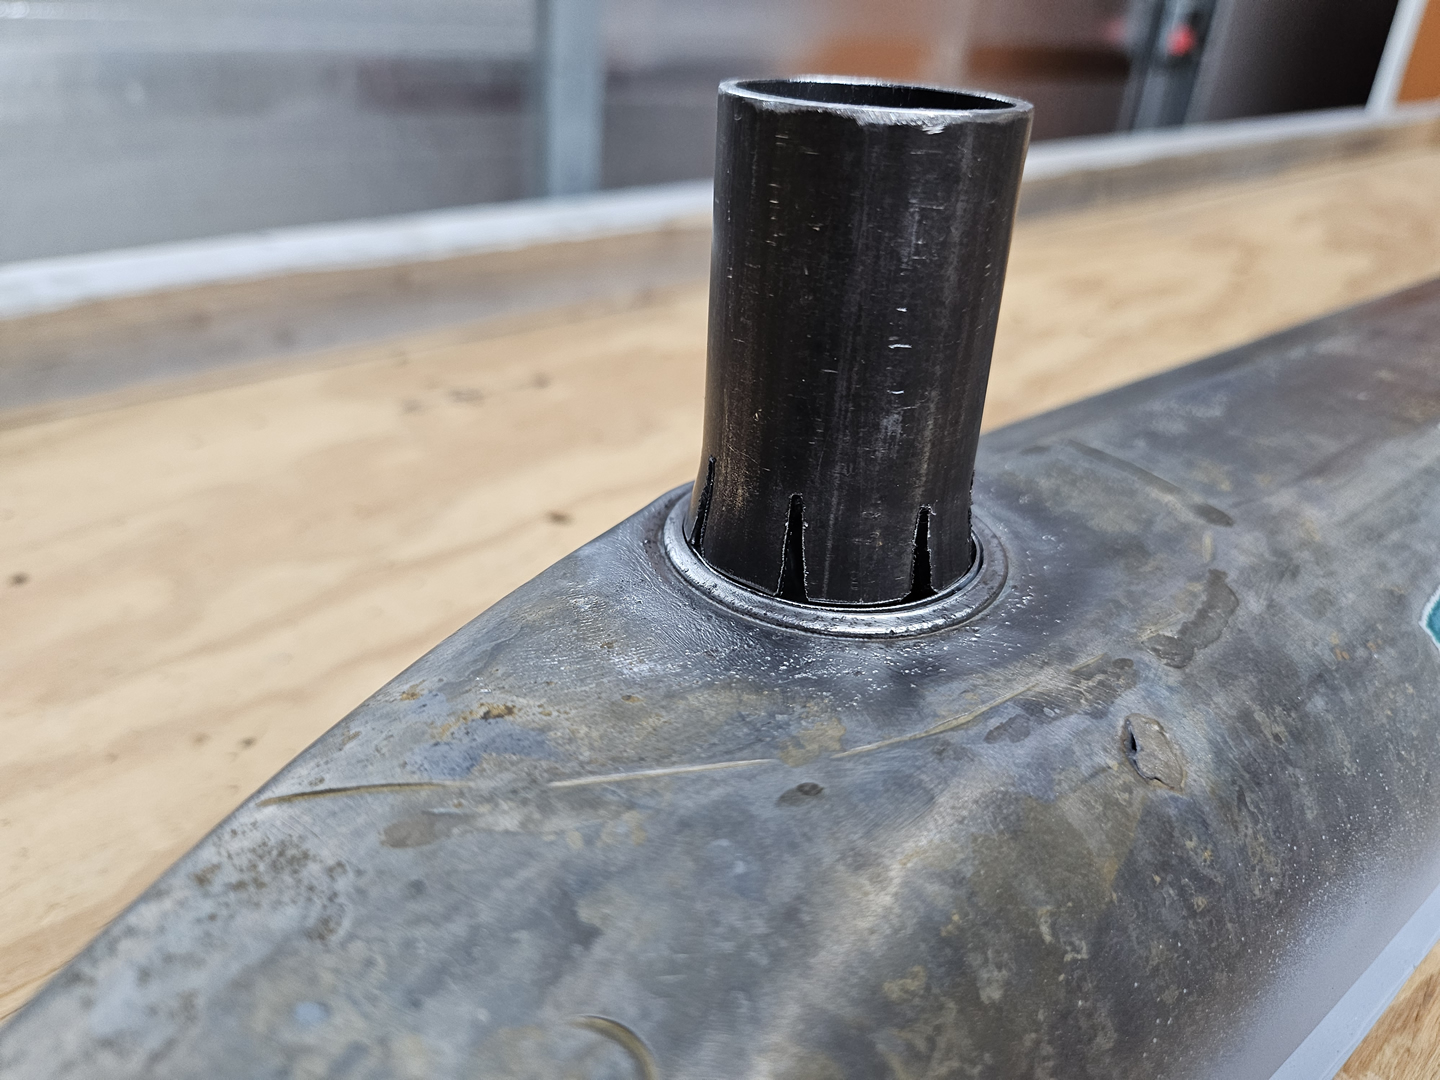
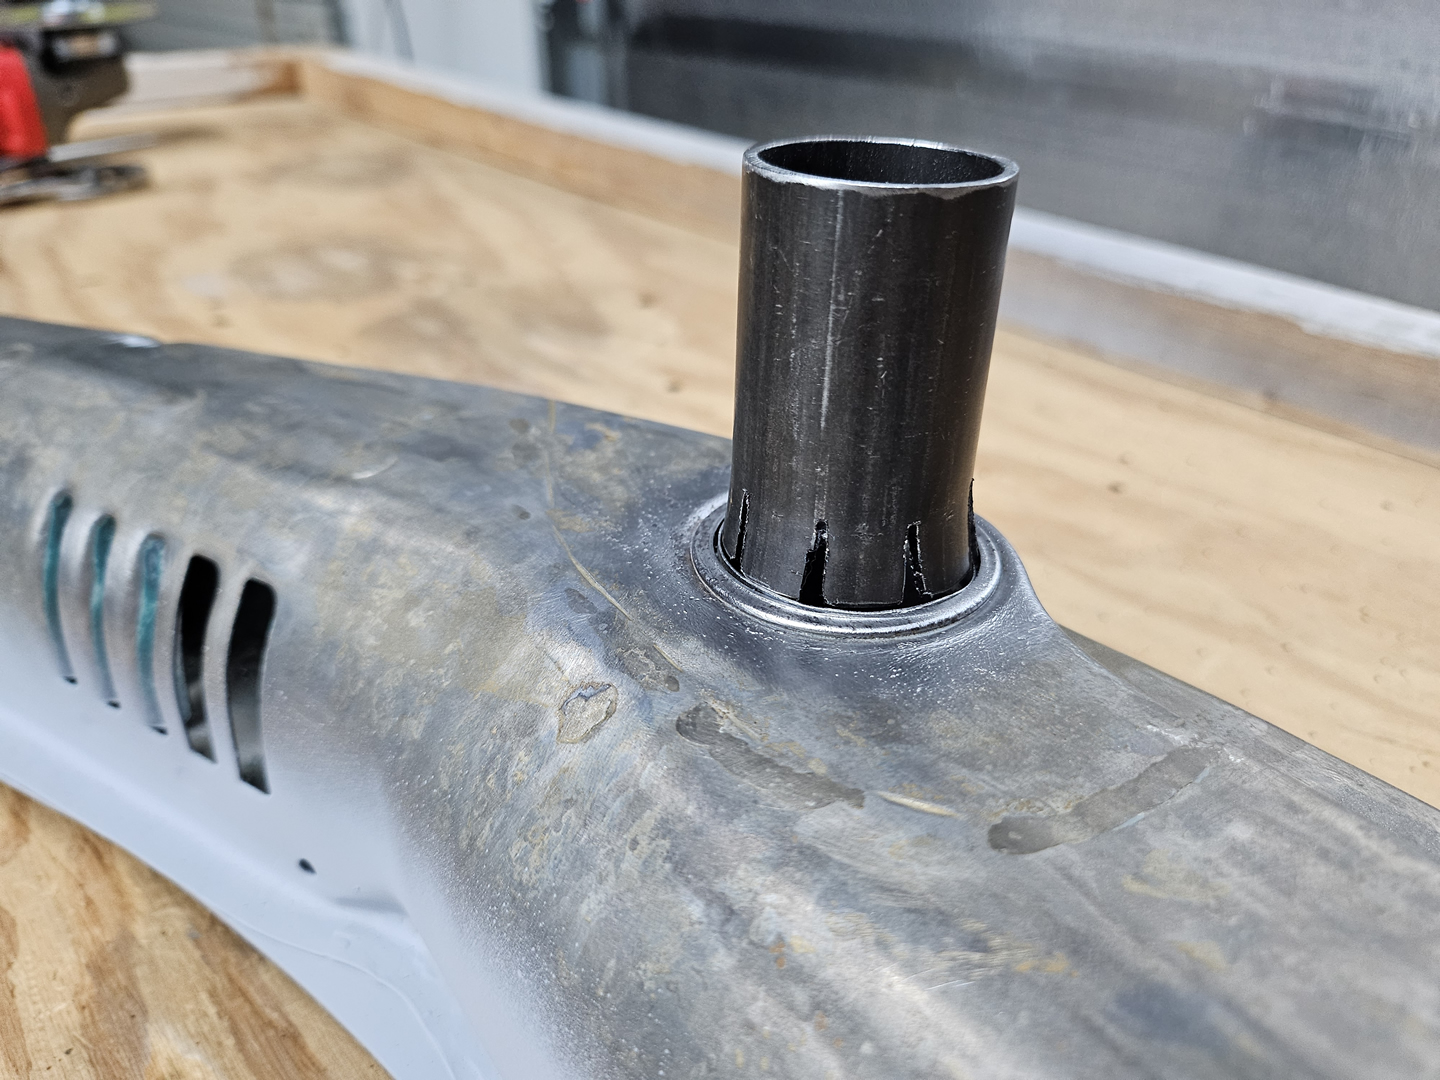
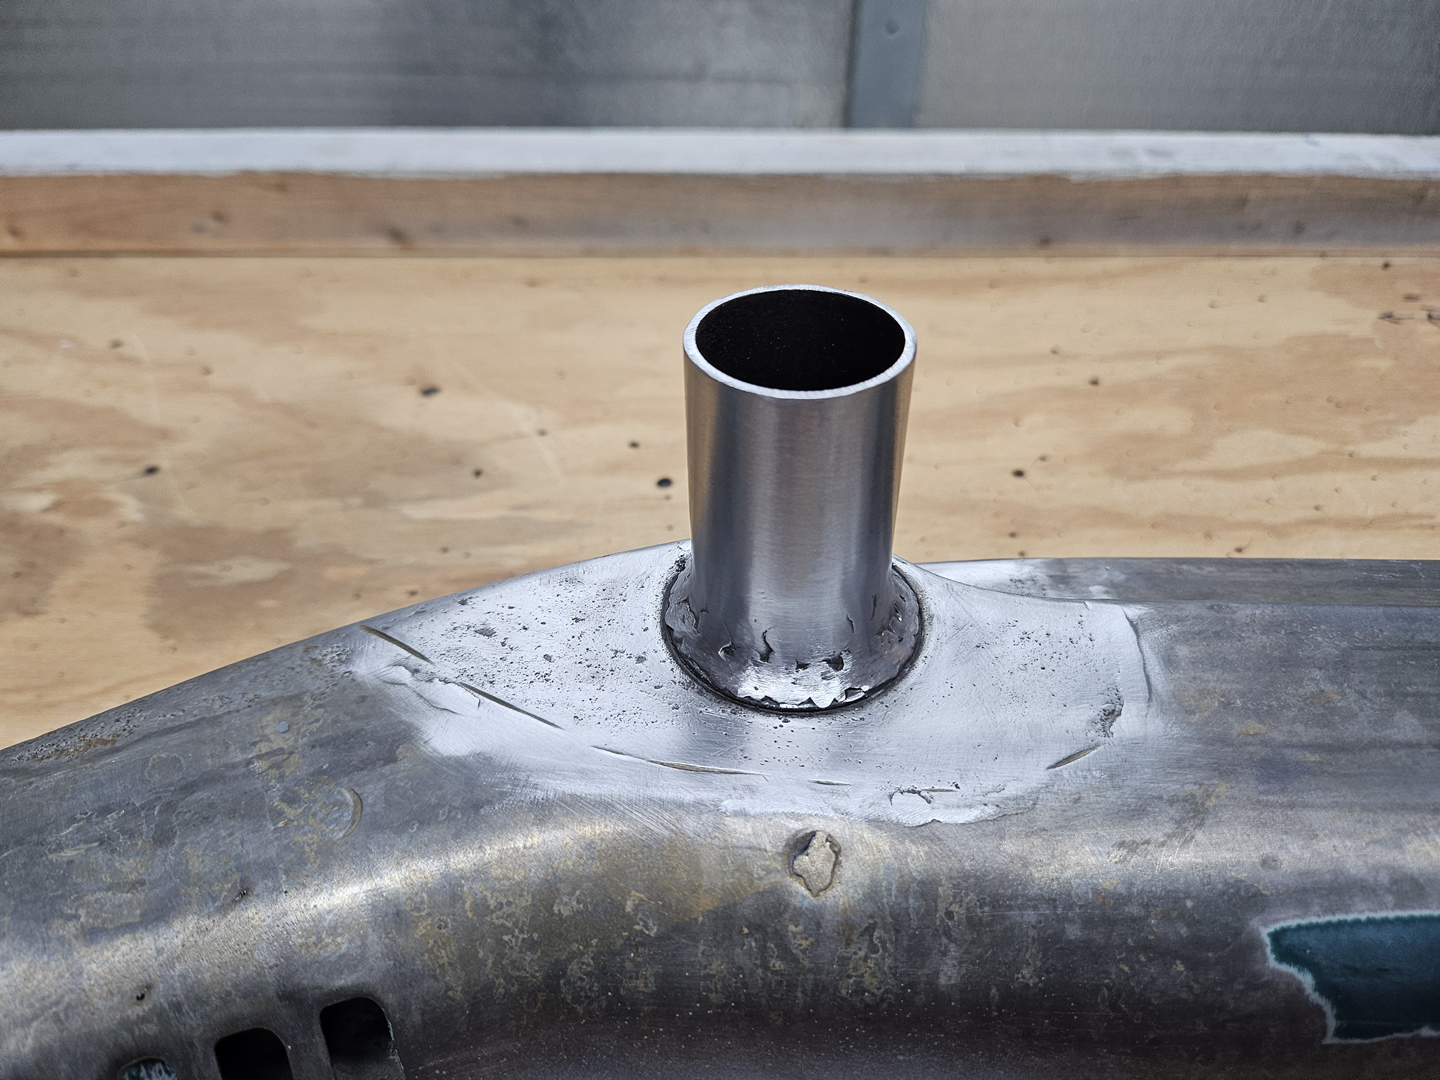
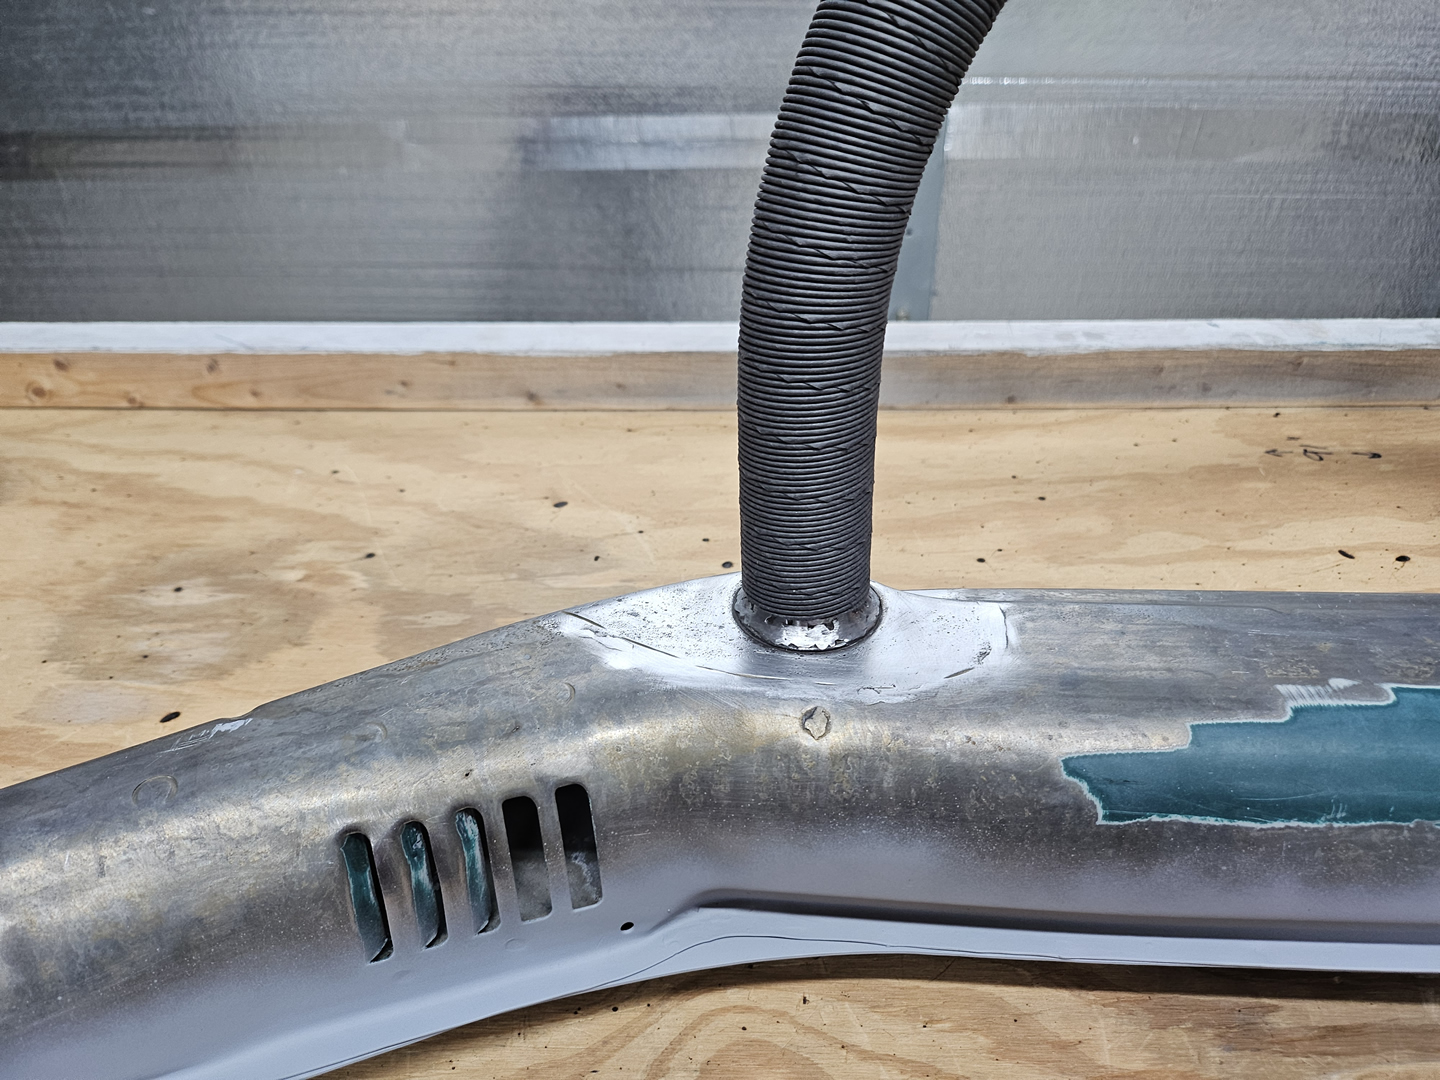
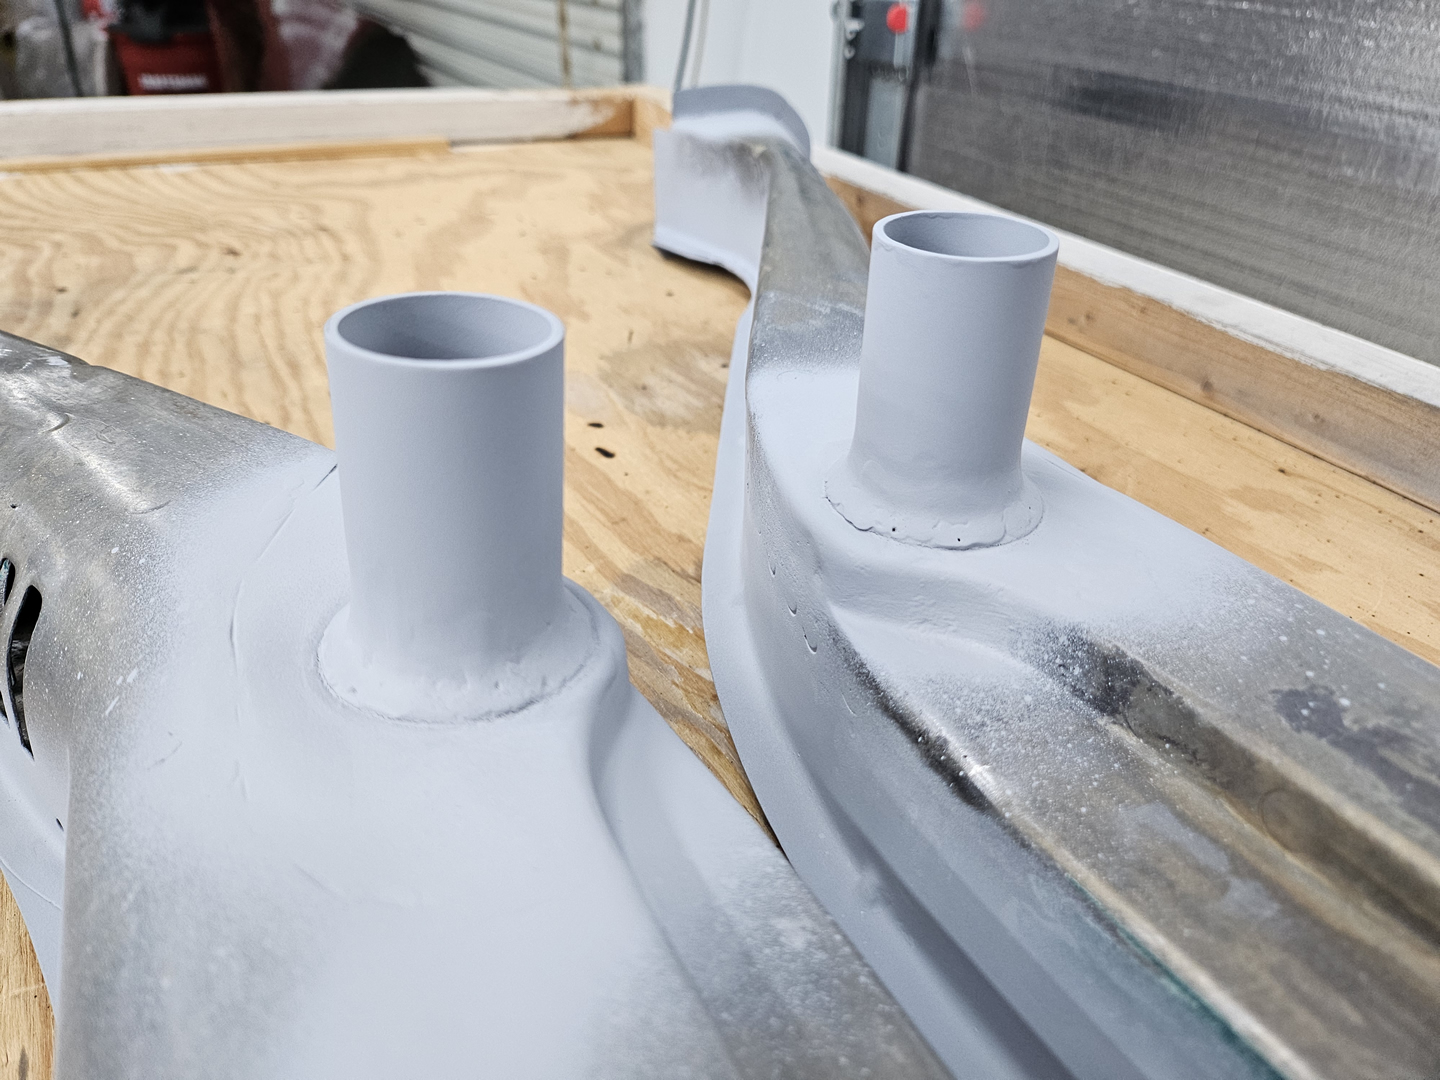
One of the many things on these donor heater channels that were destroyed by the person that sold me the parts were the receivers for the defrost hoses. They were likely rusted and useless, but it would have been nice to have the reference pieces to go by. When he removed them from the donor car, he cut the receivers almost flush to the heater channel. The original hose receivers were around 36mm on the internal diameter and the hose fit inside of it. The hoses sold now for this year range are 32mm on the internal diameter, so I needed to use pieces of pipe that were 32mm (1-1/4") on the outside diameter so that the hose will fit over them. This is quite a bit smaller than the heater pipe openings on the channels, so I had to cut relief cuts on the ends to be welded and then bend each segment out to flare it to match these openings. I then welded them all the way around the piece, and also welded up the cuts I made in them. I ground down the welds and then sprayed some primer in the welded areas. By the way, the defrost vents that connect to the defrost hoses on the top side also fit inside these new size hoses. The original size hoses that were much larger were placed over the vent connectors and then the crimped flat on the sides to compensate for the size difference.
|
|
|
|
|
|
|
|
|
|
|
|
|
|
I still have the carpet clamping strips that need to be added to the heater channels, but I really need to wait until the channels are being fitted on the body to make sure that they are in the proper position. I need to know just where the A-pillars and B-pillars are going to be placed on the channels to make sure that the gaps on each side of the clamping strips will leave sufficient space for the carpet and upholstery. I may mark the proper positions for the clamping strips when fitting the channels, and then weld them on before the channels are attached to the body.
:heater channel rust repair, threaded plate, threaded plate cage, 111 801 145 AK, 111 801 145, 111-801-145AK, rust repair, heater channel end cap repair, heater channel, defrost hose, bottom plate, defrost hose connector, heater channel repair, heater channel bottom plate
more...
by Garage Weasel on Oct.15, 2024, under Body Work
Next up for repairing and preparing is the donor front firewall. This was cut out from a 1966 Beetle and is very close to the same design as the 1960. The main differences are the absence of a hole for the fuel reserve lever and a hole in the upper left hand side for the wiring harness. Other than these two things, it is exactly the same. To start, I lightly sandblasted the outside areas and treated them with Ospho.
I decided to separate the inner panel from outer panel so that I could better assess the rust damage and simplify the replacement of any needed metal. There was quite a bit of rust on the bottom portions of both of these panels.
I sandblasted the interior of both panels as well as the areas where they will be welded back together once the repairs are completed. The rust on the inner panel was mainly surface rust and there were no areas that needed to be replaced, and the pitting wasn't too deep. The bottom corners of the outer panel were both rust-damaged and distorted by all the welding done when being welded to the heater channels. It's just going to be easier and more feasible to cut out and replace those areas. I will also use patches that are of a little thicker metal to make them last longer and have more strength.
I made patches that covered most of the bottom corners of the outer panel. I welded them on and ground down the welds.
I also welded in a patch to the passenger side flange on the inner panel. This flange was cut through when the firewall was cut from the donor car. I ground down the welds and trimmed it to the correct shape.
Since this firewall was originally for a 1966 Beetle, it had a hole on the upper left side of the outer panel so that a segment of the wiring harness could pass through it. The 1960 model harness doesn't route through the firewall, so I welded in a patch to close it up. I also filled in several unneeded screw holes and carpet nail holes on this panel.
I prepared the inner and outer panels for welding by spraying the weld areas with U-POL Weld #2 Zinc Weld Through Primer, and the interior areas with Eastwood Matte Black Rust Encapsulator.
After the panels were welded together and the welds ground down, I sprayed the outer areas with primer to protect the firewall until I get ready to fit and install it.
:front firewall, firewall, front cross panel, 111 805 451, rust repair
more...
by Garage Weasel on Oct.23, 2024, under Body Work
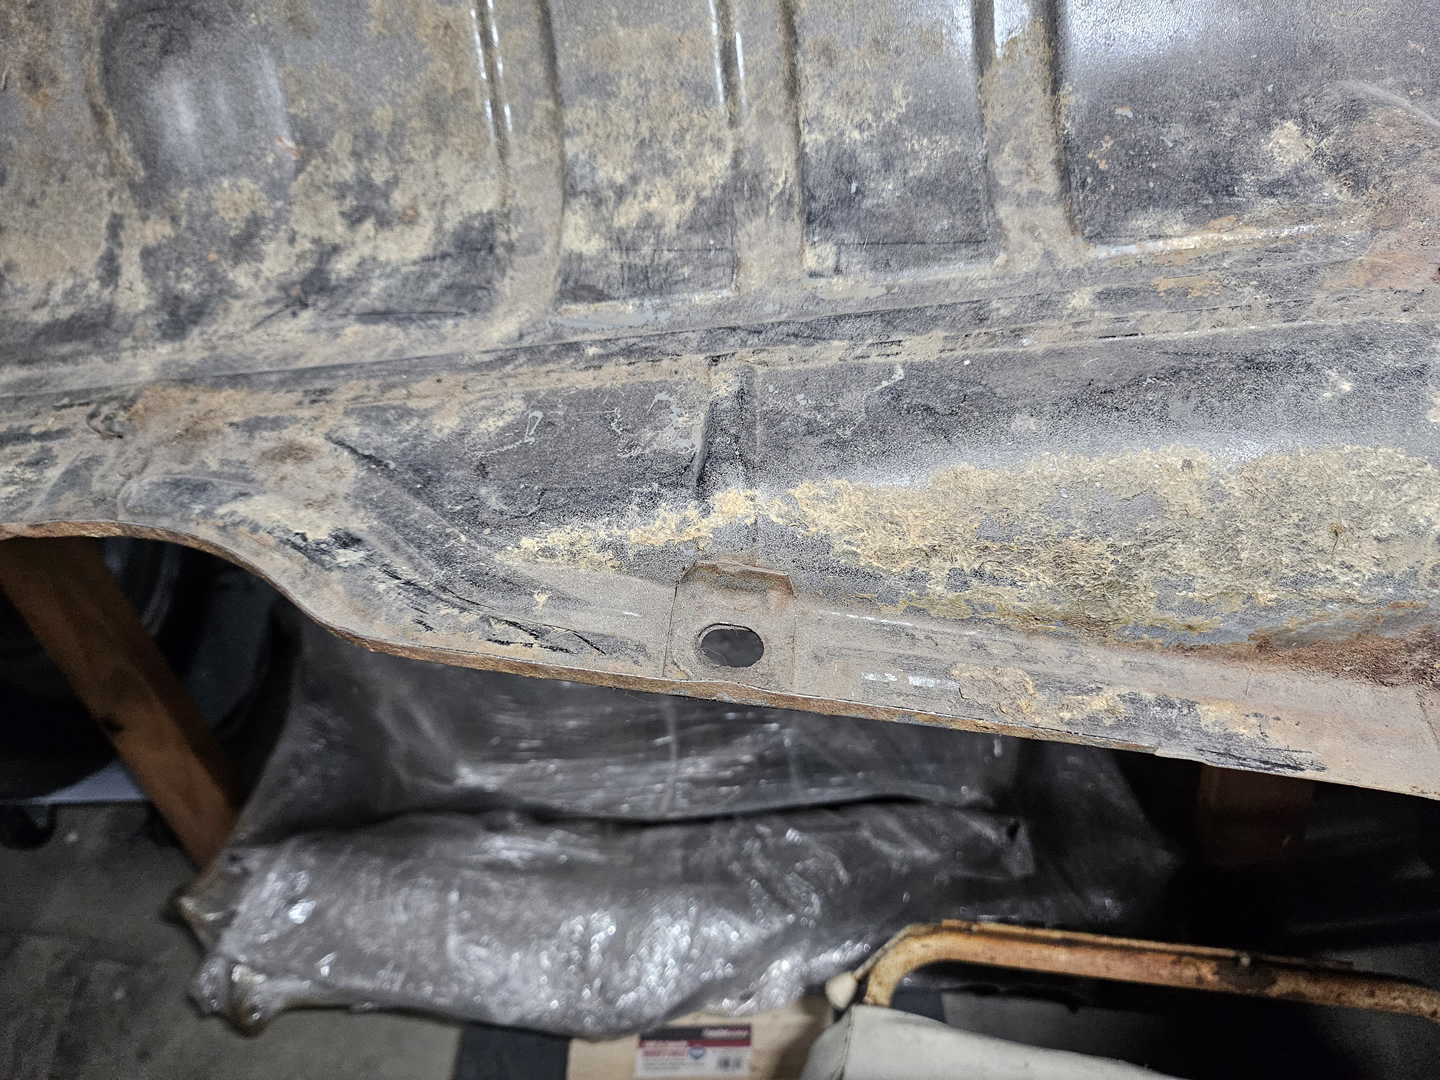
The outside corners on both rear cross members are rusted away, so I purchased new rear cross members from Wolfsburg West. These are very close to the original cross members on the car. The only thing that I wanted to change on them is to add a support plate over the holes where the bolts go through to the cross braces on the chassis. The originals had a plate like this, and it should be a fairly easy modification.
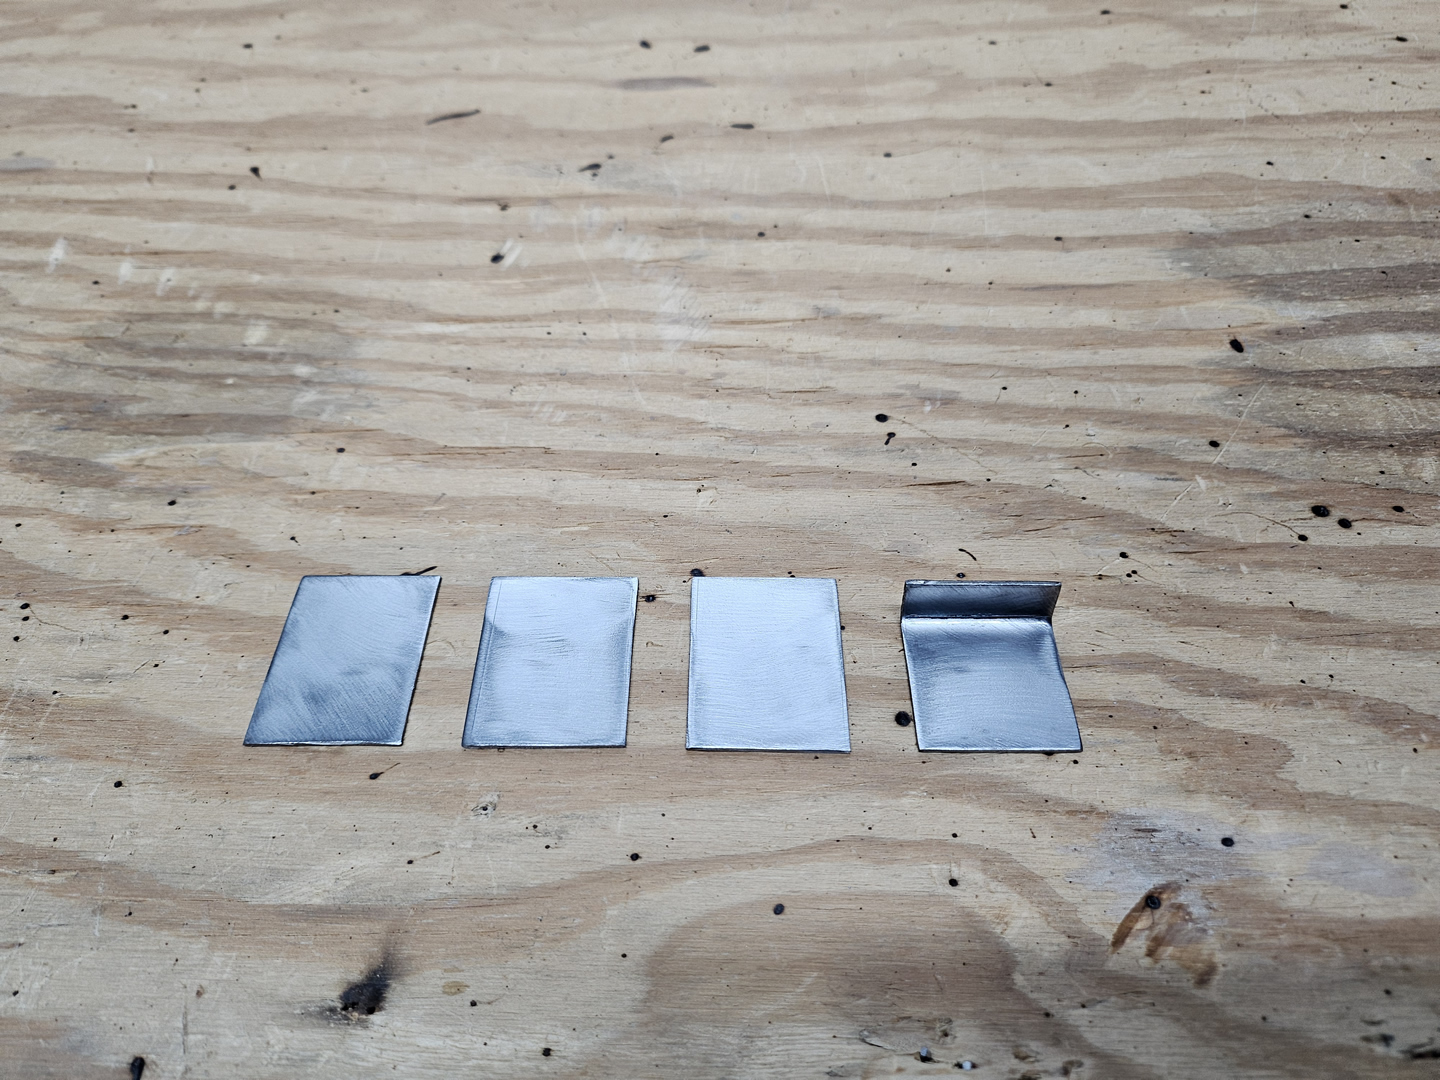
I cut out four pieces of 18-gauge steel to match the size of the original and bent them to match as well. I also dog-eared the tops of the pieces to remove the sharp edges. I drilled out two spot weld holes on each piece just in front and behind of the existing bolt hole. I then sprayed the areas between the plates with U-POL Weld #2 Zinc Weld Through Primer. Once centered, I welded the plates on and then ground down the welds.
I then cut out holes in the new plates and sprayed the weld areas with primer. The new cross member should now be ready for the fitting process.
:111-801-202, rear cross member, cross member, 111801201, 111801202, 111-801-201
more...